How to verify an ISO13485 medical machining factory
Publication Date
author
Choosing an iso13485 medical machining factory is not only a sourcing step. It directly affects compliance, patient safety, product performance, and recall exposure.
A certificate alone does not prove machining discipline. Real verification requires evidence of process control, traceability, risk management, validation, and stable output under production conditions.
This guide explains how to verify an iso13485 medical machining factory with engineering rigor. The goal is to reduce qualification risk and support defensible supplier decisions.
What an ISO13485 medical machining factory should actually demonstrate
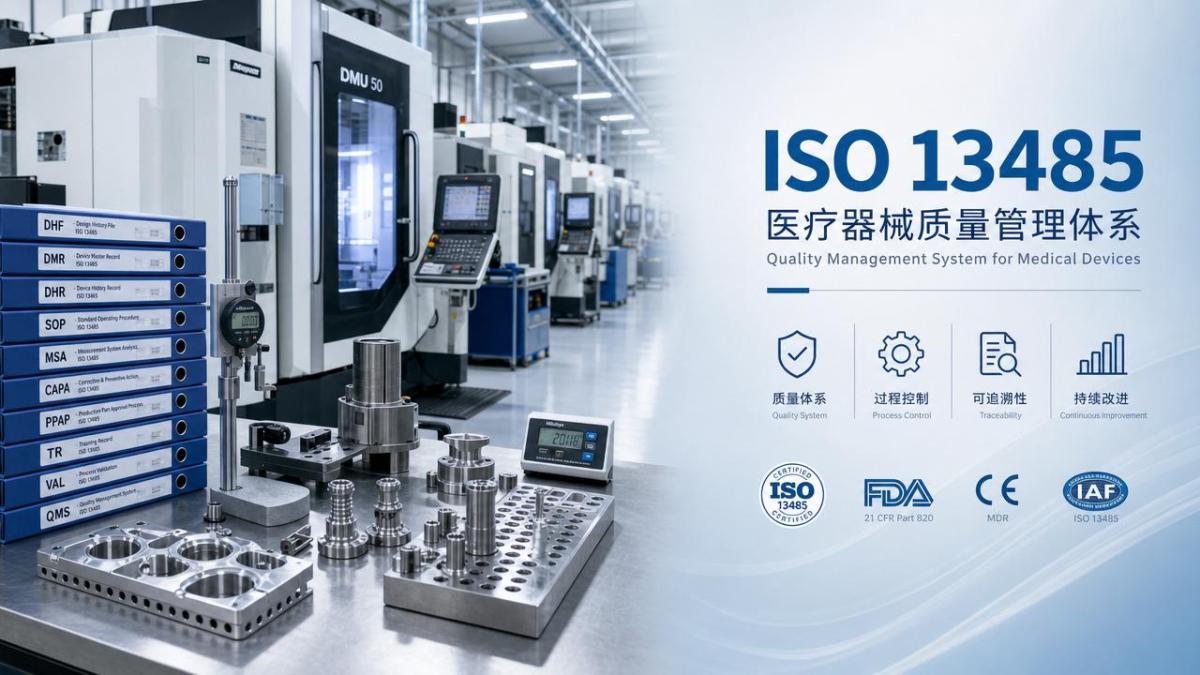
ISO 13485 is a quality management standard for medical device organizations. In machining, its value appears in controlled execution, documented evidence, and repeatable product quality.
An iso13485 medical machining factory should show more than registration status. It should connect customer drawings, process plans, inspection records, and change control into one traceable system.
Verification starts by asking a simple question. Can the factory prove that every critical dimension, material lot, and special process is controlled from quote to shipment?
For precision medical parts, the answer must be supported by records. Verbal assurance is not enough, especially for implantable, surgical, or diagnostic applications.
Core elements to confirm
- Valid ISO 13485 certificate, scope, site address, and issuing body
- Documented quality manual, procedures, and controlled revision system
- Risk-based process controls for machining, cleaning, handling, and packaging
- Material traceability from receiving through finished lot release
- Calibration, maintenance, validation, and nonconformance management
Why verification standards are tightening across medical machining
Medical supply chains face stricter scrutiny than many general industrial programs. Regulators and OEM quality teams increasingly examine process evidence, not just supplier declarations.
Complex geometries, tighter tolerances, and mixed-material assemblies raise risk. A weak control point in machining can create hidden defects that escape final inspection.
That is why an iso13485 medical machining factory is often assessed on system maturity, inspection capability, and reaction discipline when variation appears.
The most reliable verification framework for an ISO13485 medical machining factory
A strong assessment combines desktop review, on-site audit, sample evaluation, and post-audit evidence closure. Skipping any layer increases blind spots.
1. Confirm certification authenticity and scope
Check the certificate date, expiration, site name, and accredited registrar. Confirm that the listed scope covers machining activities relevant to your medical components.
A valid certificate with an unrelated scope is not enough. The registered activities should align with CNC milling, turning, finishing, inspection, or assembly where applicable.
2. Review the quality system before the visit
Request high-level procedures for document control, training, purchasing, nonconformance, CAPA, calibration, and traceability. Review whether revision history is clear and current.
A capable iso13485 medical machining factory should provide controlled documents without confusion. Delays, mismatched revisions, or incomplete forms often indicate weak discipline.
3. Audit process control on the shop floor
Observe how routers, work instructions, tooling, fixtures, offsets, and inspection checkpoints are managed. The actual process should match the documented process.
Pay attention to first article control, in-process inspection frequency, and handling of critical dimensions. Look for evidence that operators react consistently to drift.
4. Test traceability from raw material to shipment
Pick one shipped lot and walk it backward. Verify material certs, receiving checks, production traveler, inspection data, final release, labeling, and packaging records.
Then reverse the exercise. Start with a raw material lot and confirm which finished parts were produced from it. Strong traceability should work in both directions.
5. Validate measurement system capability
Inspection quality is central to any iso13485 medical machining factory. Confirm CMM capability, gauge selection, calibration status, environmental control, and method repeatability.
Ask how measurement uncertainty is handled for tight tolerances. If the factory cannot explain the metrology strategy, dimensional compliance may be overstated.
Operational value of a properly verified supplier
A well-verified iso13485 medical machining factory improves more than audit confidence. It reduces variability, supports cleaner transfers, and shortens investigation time during issues.
It also creates stronger engineering feedback. Process capability data, tooling behavior, and nonconformance trends become usable inputs for design refinement and risk control.
- Lower probability of undocumented process changes
- Faster root-cause analysis when deviations occur
- Better lot confidence for regulated end-use applications
- More reliable scale-up from prototype to production
- Reduced hidden cost from scrap, rework, and delays
Typical medical machining scenarios and what to inspect
Not every part category carries the same verification emphasis. Assessment should reflect the device function, tolerance sensitivity, cleanliness requirement, and downstream validation burden.
Practical warning signs during supplier verification
Even a certified site can present elevated risk. The warning signs usually appear in execution gaps rather than formal presentations.
Common red flags
- Scope mismatch between certificate and actual operations
- Missing lot genealogy or incomplete material certification
- Outdated work instructions at machines
- Calibration labels that do not match records
- Inspection reports without clear acceptance criteria
- Frequent rework with weak CAPA closure
- Subcontracted special processes with poor oversight
If several red flags appear together, the iso13485 medical machining factory may still be immature in operational control, even if audit paperwork looks acceptable.
A disciplined checklist for final approval
Final approval should be based on weighted evidence. This helps avoid decisions driven by price, presentation quality, or isolated sample success.
- Verify certificate validity, registrar credibility, and exact scope.
- Review quality procedures and confirm revision control.
- Audit machining control, setup discipline, and inspection checkpoints.
- Test forward and backward traceability on actual lots.
- Check metrology capability for the tightest required dimensions.
- Assess subcontractor control for finishing, coating, or sterilization-related steps.
- Review nonconformance history, CAPA effectiveness, and closure time.
- Approve with documented gaps, actions, owners, and deadlines.
Verification of an iso13485 medical machining factory should end with evidence closure, not with the site visit itself. Open issues need dates, owners, and objective proof.
A structured approach creates stronger supplier confidence and protects downstream programs from preventable disruption. In medical machining, disciplined verification is part of product quality.
For the next step, build a qualification package that combines audit questions, sample part review, traceability testing, and process capability requirements before commercial approval.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 04, 2026How Should You Compare 5-Axis CNC Machine Accuracy Claims?How do I compare 5-axis CNC machine accuracy claims? Learn how to assess standards, thermal stability, TCP accuracy, and real-world test evidence.Dr. Marcus Vance
 Oct 03, 2026Is Edge Computing Necessary for Real-Time Quality Inspection?Is industrial edge computing necessary for real-time quality inspection? Explore how latency, data volume, reliability, and control integration shape the right architecture.TSV Data Lab
 Oct 02, 2026What Documents Prove a Precision Machining Supplier Can Hold Tolerance?What documents prove a precision machining supplier can hold tolerance? Explore certificates, FAI reports, calibration, SPC, and traceability evidence to qualify suppliers with confidence.Dr. Marcus Vance
 Oct 01, 2026Can a Machining Supplier Meet Aerospace Fatigue Testing Requirements?Can a machining supplier meet aerospace fatigue testing requirements? Learn the traceability, process control, and test evidence needed for reliable aerospace parts.Dr. Marcus Vance
 Sep 30, 2026Which Industrial Robot Specifications Matter for High-Precision Assembly?Which industrial robot specifications matter most for high-precision assembly? Explore repeatability, accuracy, stiffness, vibration, calibration, and force control for reliable yields.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026How Do You Verify Servo Motor Torque Under Continuous Load?How do I verify servo motor torque under continuous load? Learn RMS torque checks, torque-speed limits, thermal derating, and real-machine testing.Chen Wei (Automation Lead Engineer)
 Oct 02, 2026ZD330 Software Configuration: Verifying Cut-List Import Before PurchaseZD330 software and machine configuration: verify cut-list imports, data mapping, labels, and workflow before purchase to reduce errors and choose with confidence.Victor Lin (Chief Software Architect)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)