
Sub-Pixel Recognition Accuracy: Useful Metric or Sales Noise?
Publication Date
author
In vendor evaluations, machine vision sub-pixel recognition accuracy is often presented as a decisive advantage—but does it reflect measurable performance or polished sales language? For business assessment teams comparing sensors, optics, and edge AI platforms, the real question is whether this metric translates into repeatability, tolerance control, and lower qualification risk. This article examines what the number actually means, where it matters, and how to separate engineering value from marketing noise.
For most procurement and business assessment teams, the short answer is this: machine vision sub-pixel recognition accuracy is useful, but only when it is tied to a defined test method, a controlled application context, and a measurable business outcome. On its own, it is not a reliable buying shortcut. In many cases, it is a narrow laboratory metric that says little about real production stability.
That distinction matters because vendor claims around machine vision sub-pixel recognition accuracy often sound precise enough to inspire confidence. A number such as 1/10 pixel or 1/20 pixel appears objective, technical, and comparable. Yet without context, it can mask major differences in lighting robustness, lens distortion, vibration sensitivity, calibration drift, software tuning, and edge processing latency.
For business evaluators, the better question is not “What sub-pixel number does the vendor advertise?” but “Under what conditions does that number reduce inspection escapes, improve tolerance control, or shorten qualification cycles?” That shift in framing separates engineering value from sales noise.
What business evaluators are really trying to find out
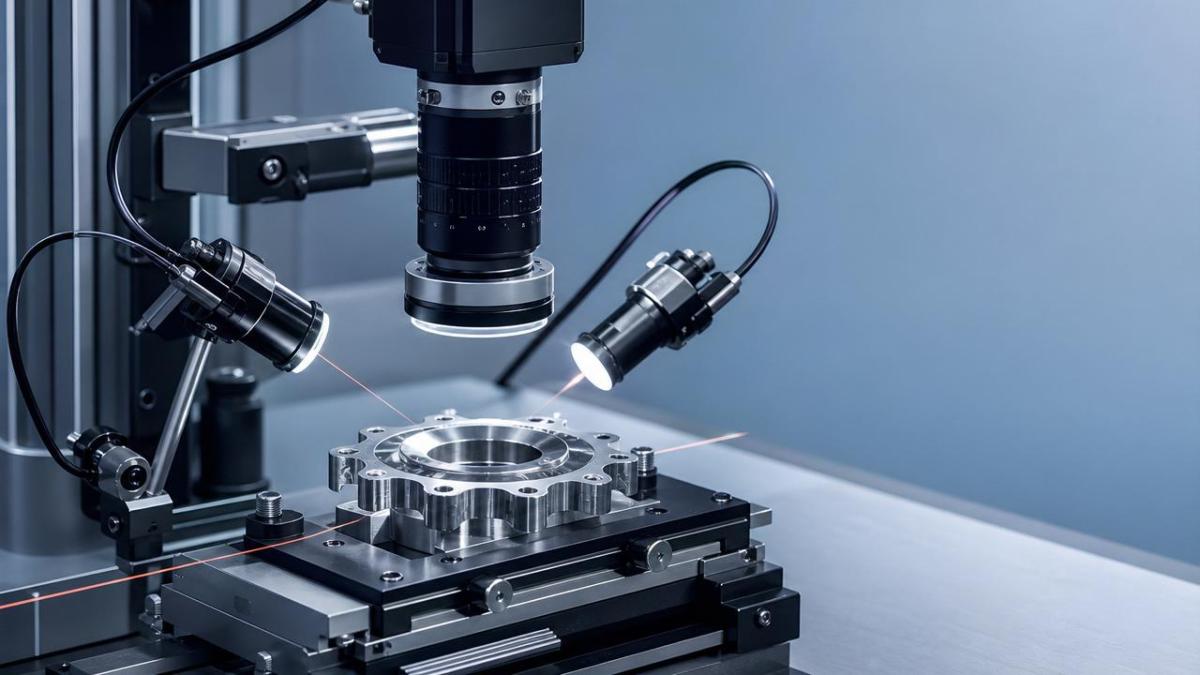
When commercial teams, procurement managers, and technical sourcing leaders research machine vision sub-pixel recognition accuracy, they are usually not seeking an academic definition. They want to know whether a claimed precision advantage will lower operational risk, support a customer specification, or create a competitive edge in manufacturing quality.
In practice, their core concerns are straightforward. Can this vision system measure consistently enough for the target tolerance band? Will it remain stable across shifts, operators, lighting changes, and production speed? Will it integrate with existing automation and edge AI infrastructure without creating hidden support costs? And can the supplier prove all of that with transparent data rather than selective screenshots?
That is why sub-pixel metrics should be evaluated as one layer in a broader decision framework. They may indicate strong algorithmic capability, especially in edge detection, centroid calculation, pattern matching, or contour fitting. But business value emerges only when those capabilities survive the realities of production.
What machine vision sub-pixel recognition accuracy actually means
At a basic level, a machine vision system works with digital pixels. If one pixel corresponds to a certain physical area on the inspected object, the system’s raw image resolution is limited by that pixel grid. Sub-pixel recognition refers to software methods that estimate position, edges, centers, or dimensions more finely than one full pixel step.
For example, if a feature boundary falls between adjacent pixels, image processing algorithms can model grayscale transitions and estimate the boundary location with greater precision than the underlying sensor pitch alone would suggest. That is why vendors may claim 0.1 pixel, 0.05 pixel, or even smaller recognition increments.
Technically, this can be real. Modern machine vision systems often do achieve sub-pixel interpolation in controlled conditions. The problem is not that sub-pixel recognition accuracy is fictional. The problem is that the number is frequently presented as if it were equivalent to end-to-end measurement accuracy in production, which it is not.
A useful distinction for non-specialist evaluators is this: sub-pixel recognition is usually an estimate of feature localization capability within the image-processing chain. It is not automatically the same as system accuracy, measurement uncertainty, or process repeatability at the part level.
Why the number can be meaningful in some applications
There are legitimate cases where machine vision sub-pixel recognition accuracy matters a great deal. In precision alignment, semiconductor inspection, fine-feature metrology, robotic guidance, PCB assembly verification, or high-end dimensional inspection, better feature localization can directly improve process performance.
If a production line depends on detecting edges, holes, corners, fiducials, or surface markers with very fine positional sensitivity, then sub-pixel algorithms can help reduce error in part placement, trajectory correction, or dimensional estimates. In these cases, a vendor with demonstrably better sub-pixel performance may offer real value.
It can also matter when physical pixel resolution cannot be increased economically. A team may face constraints around field of view, camera distance, bandwidth, or computational load. In such situations, improved sub-pixel processing can be a cost-effective way to extract better usable precision from existing imaging conditions.
For business teams, the practical takeaway is that the metric is most relevant when the inspection task is fundamentally position-sensitive and when downstream cost is driven by micron-level or sub-millimeter deviations. If those conditions do not apply, a stronger sub-pixel claim may not materially affect return on investment.
Where sub-pixel claims become marketing noise
The most common misuse of machine vision sub-pixel recognition accuracy is presenting it as a universal proof of superiority. Vendors may quote an impressive number without explaining whether it was achieved on a static target, in a controlled lab, with ideal contrast, under optimized exposure, and after manual tuning by application engineers.
That matters because real-world image quality is shaped by far more than pixel interpolation. Optical distortion, depth-of-field limits, sensor noise, motion blur, illumination non-uniformity, surface reflectivity, thermal drift, and mechanical vibration can all overwhelm the benefit of an excellent sub-pixel algorithm.
A supplier can therefore advertise very strong machine vision sub-pixel recognition accuracy while still delivering weak production performance if the complete system is poorly engineered. This is especially common when cameras, lenses, lighting, software, and mounting conditions are evaluated separately rather than as a measurement chain.
Another warning sign is when a vendor highlights sub-pixel precision but avoids discussing gauge repeatability, false reject rates, false accept rates, calibration intervals, or process capability under production speed. Those metrics are usually closer to the outcomes business evaluators actually care about.
The difference between interpolation precision and measurement truth
One of the biggest sources of confusion in supplier comparisons is the gap between computational precision and physical accuracy. A vision system can estimate an edge location to a fraction of a pixel, but if the lens introduces distortion or the part is tilted, that estimate can still be wrong in physical space.
In other words, a system may be precise in the sense that it repeats the same estimate, yet inaccurate in the sense that the estimate does not match the true dimension or position. For business decisions, this distinction is critical because production risk depends on both repeatability and correctness.
Imagine a vendor claiming 1/20 pixel recognition. That sounds exceptional. But if the system is deployed in a factory with variable ambient light, inconsistent fixturing, and moderate vibration, the effective measurement variation may be many times larger than the advertised figure. The procurement team may have bought a mathematically elegant algorithm, not a robust measurement solution.
That is why buyer-side qualification should always connect sub-pixel claims to uncertainty budgets, calibration strategy, environmental controls, and acceptance thresholds. The value of the metric lies in its contribution to a validated system, not in its standalone numerical appeal.
What to ask vendors before treating the metric as decision-grade
Business assessment teams do not need to become computer vision scientists, but they do need a disciplined questioning framework. The first question should be how the claimed machine vision sub-pixel recognition accuracy was measured. Was it based on a static test target, a certified artifact, a simulation, or a production-representative part? What lighting, lens, exposure, and working distance were used?
Second, ask whether the figure represents repeatability, accuracy, or algorithmic localization capability. Many claims blur these categories. A trustworthy supplier should define the metric clearly and provide a test protocol rather than a brochure phrase.
Third, request performance data under application-like conditions. This includes throughput rate, temperature range, expected vibration, part surface variation, contamination levels, and operator variability. A result that looks excellent at low speed in ideal contrast may degrade sharply in real deployment.
Fourth, ask for system-level evidence. This may include gauge R&R studies, Cpk impact, false positive and false negative rates, calibration drift over time, and correlation against traceable metrology equipment. These data points help translate a technical claim into commercial risk language.
Fifth, assess implementation burden. Some systems achieve impressive sub-pixel results only with extensive tuning, controlled lighting enclosures, premium optics, or frequent recalibration. If maintaining the claimed performance requires high ongoing engineering effort, the headline specification may not represent total value.
How to compare suppliers without being misled by a single number
A strong vendor comparison process should treat machine vision sub-pixel recognition accuracy as one criterion among several weighted factors. The right weighting depends on your use case, but most business teams should compare suppliers across at least five dimensions: measurable accuracy in production, repeatability over time, robustness to variation, integration cost, and support maturity.
Start with the application requirement, not the vendor metric. Define the actual tolerance window, defect classes, throughput target, and acceptable escape rate. Then ask which technical characteristics most influence those outcomes. In some cases, lighting design or lens quality may matter more than a more aggressive sub-pixel claim.
It is also useful to normalize proposals into a common framework. For example, compare each vendor on tested part types, environmental assumptions, calibration method, maintenance frequency, software explainability, and evidence quality. A supplier with a weaker marketing number may prove stronger once the evaluation emphasizes validated operating performance.
Whenever possible, insist on a pilot or benchmark using your own parts, conditions, and pass-fail criteria. For high-stakes sourcing, lab metrics should never be the sole basis for award decisions. Real qualification data almost always reveals whether a performance claim is structurally meaningful or mostly presentation polish.
When a strong sub-pixel metric should influence the purchase decision
There are scenarios in which this metric deserves serious weight. If the application involves small features near the limit of image resolution, if part placement or dimensional acceptance depends on very fine edge localization, and if the vendor can demonstrate stable results in representative conditions, then machine vision sub-pixel recognition accuracy may be a real differentiator.
It should also receive more attention when the economic cost of tiny deviations is high. Aerospace assemblies, medical device components, advanced electronics, and tightly toleranced automation cells can all justify deeper scrutiny of localization performance. In these environments, even modest improvements in repeatable feature detection can reduce scrap, rework, or qualification delays.
However, even in these advanced cases, the metric should influence decisions only when it is linked to traceable value. Better alignment yield, lower inspection uncertainty, fewer customer complaints, faster commissioning, or reduced need for secondary checks are the kinds of outcomes that justify premium pricing.
A practical decision rule for business assessment teams
If you need a simple rule, use this one: trust machine vision sub-pixel recognition accuracy only when it is accompanied by a clearly defined test method, a production-relevant validation dataset, and evidence that it improves a business-critical outcome. If any of those three elements is missing, treat the claim as preliminary, not decision-grade.
This rule helps business teams avoid two common mistakes. The first is overvaluing a polished technical number that has little operational consequence. The second is undervaluing a genuinely strong supplier because the team lacks a framework to interpret the metric properly. A structured evaluation avoids both extremes.
In practical sourcing terms, the right question is not whether sub-pixel recognition is real. It is whether this supplier’s claimed capability survives your environment, your throughput, your tolerance requirements, and your maintenance reality. That is the standard that protects capital allocation and qualification timelines.
Conclusion: useful metric, but never enough by itself
Sub-pixel recognition accuracy is neither meaningless hype nor automatic proof of superiority. It is a legitimate technical metric that can signal strong machine vision capability, especially in demanding inspection and alignment tasks. But in vendor evaluations, it becomes valuable only when translated into system-level performance and business-level outcomes.
For procurement and business assessment professionals, the safest position is balanced skepticism. Do not dismiss the metric, because in the right context it can matter. But do not accept it at face value either, because machine vision sub-pixel recognition accuracy by itself does not guarantee repeatability, tolerance control, or lower qualification risk.
The suppliers worth trusting are usually the ones that can connect the number to transparent test conditions, measurable production performance, and a credible path to deployment. In a market crowded with confident language, that is how engineering truth stands apart from sales noise.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























