
CAD/CAM Interoperability Checklist: How to Compare Data Loss, Toolpaths, and Post Output
Publication Date
author
CAD/CAM Interoperability Checklist: How to Compare Data Loss, Toolpaths, and Post Output
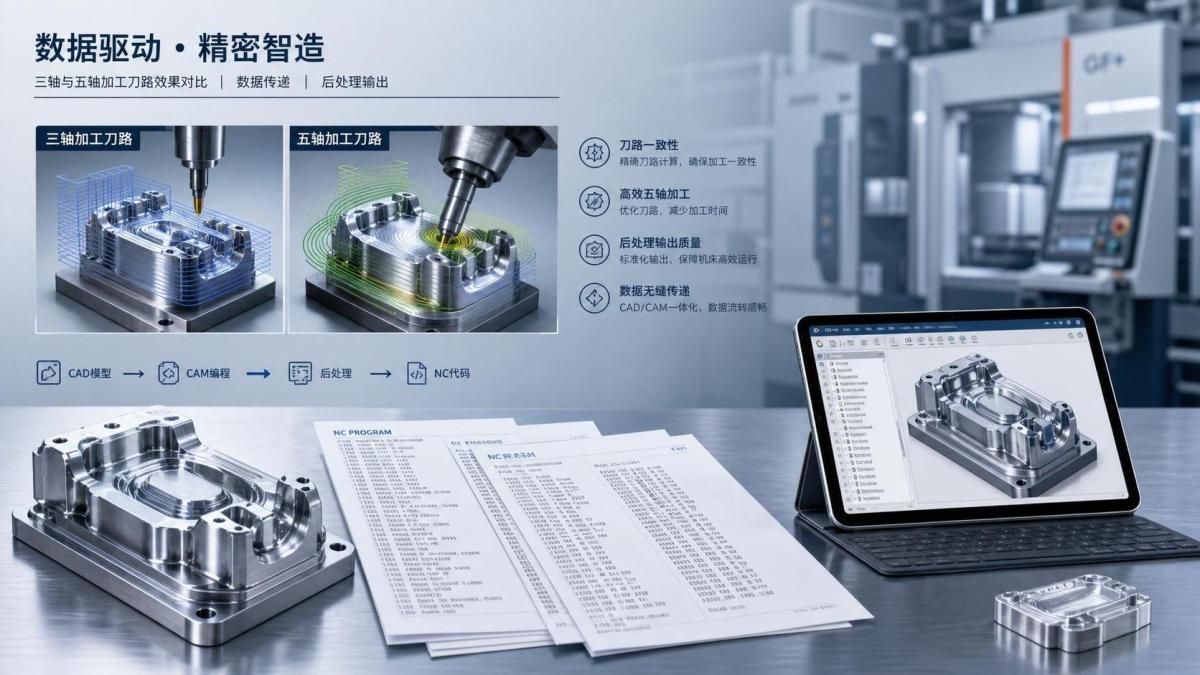
For project leaders comparing digital manufacturing stacks, cad cam interoperability is not a soft feature. It shapes revision accuracy, machining stability, and delivery confidence.
A clean demo file proves very little. Real value appears when models change fast, suppliers use mixed software, and NC output must stay predictable.
That is why cad cam interoperability should be tested like an engineering variable. It needs evidence, not marketing language.
This checklist focuses on three decision points: data loss, toolpath consistency, and post output quality. Together, they expose where digital manufacturing workflows actually break.
From TSV’s perspective, the goal is simple. Compare systems using measurable production truth, then shorten qualification cycles with fewer hidden surprises.
Why CAD/CAM Interoperability Matters More During System Selection
In many teams, software evaluation starts with features, license cost, and user familiarity. Those matter, but they do not reveal interoperability risk.
The bigger issue appears later. A model opens, but face IDs shift. A toolpath regenerates, but lead-in behavior changes. A post runs, but code differs by machine.
This is where cad cam interoperability becomes a schedule issue, not just a technical issue. Every mismatch creates extra review, manual edits, and supplier back-and-forth.
For precision machining, that cost compounds fast. Minor translation errors can affect tolerances, cycle time, fixture assumptions, and process repeatability.
A stronger selection process asks one practical question: when data crosses systems, what changes, what breaks, and what must be rebuilt?
Start With the Right Interoperability Test Pack
Do not compare platforms using only one polished part. That hides real interoperability behavior.
Build a small test pack with parts that reflect real complexity. Include both geometry and process variation.
- Prismatic part with many feature edits across revisions
- Freeform surface part with tight blend continuity
- Multi-axis part with indexed and simultaneous moves
- Assembly-driven component with external references
- Part requiring machine-specific post customization
Also include revision scenarios. A strong cad cam interoperability review must test how updates propagate, not just how first import behaves.
This matters even more when internal teams and contract manufacturers use different CAD kernels or CAM environments.
Checklist Part 1: Compare Data Loss Before You Compare Features
Data loss is the first filter. If the geometry arrives damaged or stripped, downstream automation loses value immediately.
Check geometry fidelity
Review surfaces, trimmed edges, blends, holes, and small radii. Look for gaps, face healing, tolerance drift, and missing features.
Measure imported geometry against the source model. Use deviation analysis, not visual inspection alone.
Check semantic data retention
A modern cad cam interoperability workflow should retain more than shape. It should preserve manufacturing intent where possible.
- Feature recognition reliability
- PMI and GD&T readability
- Layer, color, and naming conventions
- Coordinate systems and datum references
- Material and metadata transfer
Check revision survivability
This is often the hidden failure point. A system may import version A well, then break associativity after version B.
Test whether operations stay attached after design edits. If re-selection becomes manual, the real workflow cost rises sharply.
Checklist Part 2: Verify Toolpath Consistency Under Change
Once geometry survives transfer, the next question is whether machining intent survives too. That is the core of practical cad cam interoperability.
Compare regeneration behavior
Regenerate identical operations after import and after revision. Record any changes in step-over, linking motion, stock awareness, or cut ordering.
Small changes can alter machine load, surface finish, or cycle time. Those are not cosmetic differences.
Check high-risk strategies
Some strategies are more sensitive during translation. Test them first instead of last.
- Rest machining based on in-process stock
- 3D finishing on blended surfaces
- Hole-making with feature automation
- 5-axis swarf, morph, and curve-driven paths
- Template-based operations reused across parts
Measure consistency, not just success
A toolpath that calculates is not automatically acceptable. Compare cut length, air time, retract count, and expected cycle time.
If two platforms produce different outcomes from the same source, document whether the difference improves or degrades process stability.
Checklist Part 3: Compare Post Output Like a Production Control Variable
Post output is where many evaluations become too shallow. Yet post behavior decides whether digital plans survive the shop floor intact.
Review code structure and readability
Check sequence clarity, modal control, safe starts, tool change logic, work offset calls, and comments useful for operators.
Good cad cam interoperability should reduce manual edits at the machine. If programmers still patch code often, the workflow is weaker than it looks.
Test machine-specific edge cases
Use real controllers and machine configurations. Generic simulation is useful, but it does not replace production output checks.
- Rotary limits and unwinding logic
- Canned cycle formatting
- Polar or cylindrical interpolation
- High-speed smoothing codes
- Subprogram handling and memory constraints
Track post maintenance burden
Selection teams often miss this. Ask how many machines need custom posts, who owns updates, and how validation is documented.
A cheaper platform with unstable posts can become more expensive over a year of engineering support.
A Practical Scoring Model for CAD/CAM Interoperability
To avoid subjective debate, score each platform against the same weighted criteria. Keep the framework simple enough to repeat.
This approach keeps cad cam interoperability tied to business impact. It also helps procurement and engineering teams discuss tradeoffs using the same evidence base.
Common Decision Mistakes to Avoid
Several selection errors appear again and again, especially in mixed-supplier environments.
- Treating file import as proof of full cad cam interoperability
- Testing only native files and ignoring neutral formats
- Skipping revision scenarios during evaluation
- Comparing toolpaths without controller-level post checks
- Ignoring manual repair time in total cost analysis
More clearly now, the selection problem is not which platform looks strongest in a demo. It is which platform stays reliable when complexity increases.
Final Checklist for a Better Selection Decision
Before making a final decision, confirm these points in writing.
- Use a representative test pack, not a single showcase model.
- Measure geometry deviation and semantic data retention.
- Test revision updates and associativity failures.
- Compare toolpath changes using time and motion metrics.
- Validate post output on target controllers and machines.
- Score results with agreed weights before vendor discussion.
The strongest cad cam interoperability choice is usually the one that removes rework across the whole chain, from design release to machine execution.
At TSV, that is the standard worth using: parameters first, assumptions last, and every decision anchored to observable manufacturing behavior.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 08, 2026AGV vs. AMR: Which Is Better for Frequently Changing Routes?Which is better for changing routes? Compare AGVs and AMRs for flexible navigation, docking precision, traffic control, and faster facility reconfiguration.Chen Wei (Automation Lead Engineer)
 Oct 07, 2026How Much Does an Automated Guided Vehicle Cost in 2026?How much does an automated guided vehicle cost in 2026? Explore AGV price ranges, hidden deployment costs, and smart buying factors for stronger ROI.Chen Wei (Automation Lead Engineer)
 Oct 06, 2026Are Collaborative Robots Safe Enough to Operate Without Fencing?Are collaborative robots safe enough to work without fencing? Explore risk assessment, safeguarding options, and practical guidance for safer, productive cobot cells.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026What Causes Machine Vision Systems to Miss Small Defects?What causes machine vision systems to miss small defects? Discover how lighting, optics, motion, and AI thresholds affect detection—and prevent costly escapes.TSV Data Lab
 Oct 04, 2026How Should You Compare 5-Axis CNC Machine Accuracy Claims?How do I compare 5-axis CNC machine accuracy claims? Learn how to assess standards, thermal stability, TCP accuracy, and real-world test evidence.Dr. Marcus Vance
 Oct 03, 2026Is Edge Computing Necessary for Real-Time Quality Inspection?Is industrial edge computing necessary for real-time quality inspection? Explore how latency, data volume, reliability, and control integration shape the right architecture.TSV Data Lab
 Oct 02, 2026What Documents Prove a Precision Machining Supplier Can Hold Tolerance?What documents prove a precision machining supplier can hold tolerance? Explore certificates, FAI reports, calibration, SPC, and traceability evidence to qualify suppliers with confidence.Dr. Marcus Vance























