
Precision Machining for Aerospace Alloys: Where Costs Drift
Publication Date
author
In precision machining for aerospace alloys, cost drift rarely starts on the invoice. It begins earlier, inside tolerance chains, metallurgy variation, tool life instability, and qualification complexity.
For programs built on titanium, Inconel, aluminum-lithium, and nickel-based materials, even minor process shifts can change total cost exposure. Precision machining for aerospace alloys is therefore a margin-control discipline, not only a manufacturing task.
That reality matters across the broader industrial landscape. Capital planning, supplier benchmarking, engineering validation, and risk governance all depend on understanding where machining economics quietly move.
When aerospace alloy projects look stable but costs are already drifting
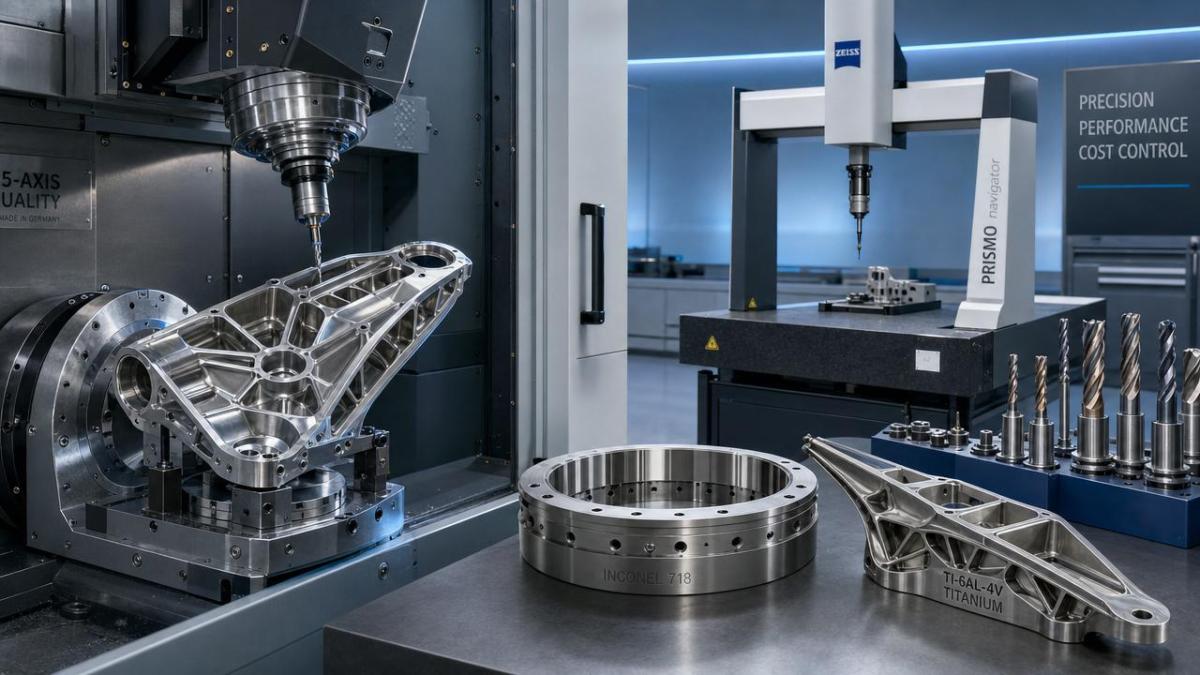
In precision machining for aerospace alloys, visible unit price is often the last indicator. Earlier signals appear in scrap rates, inspection time, setup repetition, and unplanned process adjustments.
A titanium bracket and an Inconel ring may share similar drawing complexity. Their cost behavior differs sharply once cutting heat, chatter sensitivity, and post-machining inspection are included.
This is why data-led evaluation matters. TechStat Vanguard emphasizes engineering truth because machining economics become reliable only when tied to measurable process variables.
The first decision point is not “What is the quoted price?” It is “Which cost layers are exposed by this alloy, geometry, tolerance band, and approval path?”
Scenario one: tight-tolerance structural parts shift cost through tolerance stacking
Structural aerospace components often combine thin walls, deep pockets, and positional tolerances that leave little process freedom. In this scenario, cost drift usually starts with tolerance stacking.
Each datum relationship narrows machining latitude. More in-process inspection follows. Additional fixturing, slower feeds, and greater thermal stabilization time become necessary.
Core judgment points in this scenario
- Whether tolerance zones are functional or inherited from legacy drawings
- Whether multiple setups create cumulative geometric variation
- Whether clamping distortion changes final feature alignment
- Whether CMM time is proportionate to part value
In precision machining for aerospace alloys, over-controlled dimensions can inflate total cycle cost without improving mission performance. Functional tolerance review often delivers larger savings than negotiating machine hourly rates.
Scenario two: heat-resistant alloys move costs through tool wear and machine time
Nickel alloys and high-temperature aerospace materials create a different pattern. Here, precision machining for aerospace alloys becomes dominated by heat management, chip control, and tool degradation.
Quoting errors often happen when tool replacement assumptions are too optimistic. A small variance in insert life can materially alter cost per accepted component.
Where cost drift appears fastest
- Unexpected tool wear from inconsistent material hardness
- Longer spindle occupation because feed rates must be reduced
- Extra deburring and surface integrity checks
- Rework caused by burrs, microcracks, or heat-affected edges
This scenario rewards process transparency. Tool life curves, coolant strategy, and spindle load history provide stronger cost evidence than broad claims about high-performance capability.
Scenario three: flight-critical parts carry hidden qualification and traceability costs
Some parts are not expensive because they are difficult to cut. They are expensive because every operation must be proven, recorded, and auditable.
In flight-critical programs, precision machining for aerospace alloys includes document control, raw material pedigree, first article inspection, process validation, and change management discipline.
A shop with attractive machining rates may still produce higher lifecycle cost if traceability records are incomplete. One missing heat lot linkage can trigger quarantine, delay, and repeated verification.
Core judgment points in this scenario
- Material certification continuity from mill to finished part
- AS9100 process discipline and revision control maturity
- Nonconformance handling speed and containment logic
- Repeatability of FAI results across batches
How different application scenarios change precision machining for aerospace alloys
The same keyword can describe very different economic realities. Precision machining for aerospace alloys behaves differently across prototypes, low-volume certified runs, and recurring production.
Scenario-based recommendations for controlling cost drift early
Cost control in precision machining for aerospace alloys works best when matched to the operating scenario. Generic sourcing rules usually miss the technical cause of drift.
Recommended actions before committing budget
- Map which dimensions are flight-critical, assembly-critical, or legacy-only.
- Request tool life assumptions by alloy, feature type, and batch size.
- Separate machining cost from inspection, certification, and documentation cost.
- Review scrap and rework history by material family, not only by total average.
- Check whether process capability was demonstrated on similar geometry.
- Validate traceability workflow before scaling production volume.
These actions fit TSV’s benchmark-first philosophy. Parameters, not adjectives, reveal whether a machining source can hold margin under real aerospace conditions.
Common misreads that distort aerospace machining decisions
Several recurring mistakes make precision machining for aerospace alloys appear cheaper than it will be in practice. Most are caused by incomplete engineering visibility.
- Assuming expensive alloy automatically means the material is the dominant cost.
- Comparing quotes without aligning inspection scope and documentation depth.
- Ignoring fixture redesign when geometry changes late in development.
- Treating first-pass yield as stable before enough batch data exists.
- Believing machine count equals process capability for hard-to-cut alloys.
Another common issue is mixing prototype economics with production economics. A process that is acceptable for validation parts may fail financially once repeatability requirements harden.
A practical next step for evaluating precision machining for aerospace alloys
The most effective next step is to build a scenario-based review sheet. Include alloy type, tolerance class, geometry risk, expected lot size, certification needs, and allowable process variability.
Then compare machining options against evidence. Use tool consumption data, dimensional capability records, FAI consistency, and traceability response speed as the decision baseline.
For organizations navigating precision machining for aerospace alloys, this approach reduces trial-and-error cost and shortens technical qualification cycles. It also aligns with TSV’s core principle: engineering truth should drive commercial confidence.
When costs drift, they rarely drift randomly. They follow process physics, quality rules, and data gaps. See those drivers clearly, and aerospace machining decisions become far more defensible.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























