
Why aerospace tolerance standards are tighter than many drawings show
Publication Date
author
In aerospace manufacturing, the numbers printed on a drawing often tell only part of the story. Real-world compliance depends on aerospace machining precision tolerance standards shaped by process capability, material behavior, inspection uncertainty, and flight safety margins. For quality and safety leaders, understanding why actual tolerance control is often tighter than nominal requirements is essential to reducing risk, preventing hidden nonconformities, and qualifying suppliers with confidence.
Why do aerospace tolerance standards run tighter than the drawing suggests?
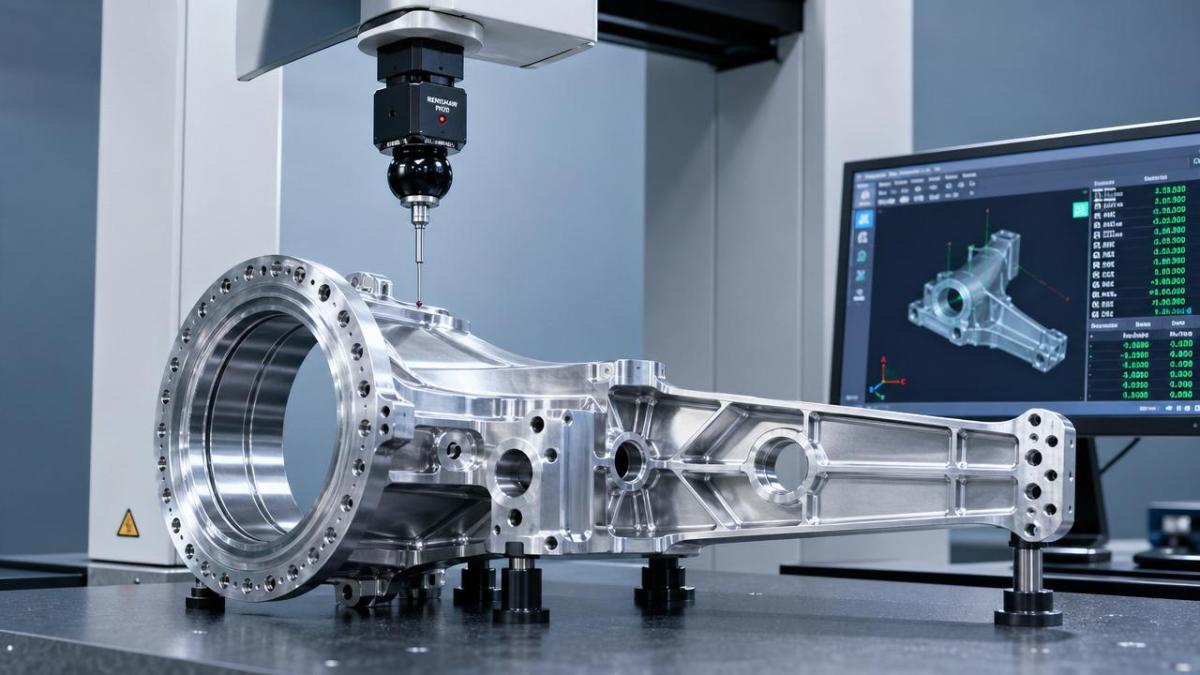
A drawing defines allowable variation, but aerospace machining precision tolerance standards are rarely managed at the drawing limit alone. In practice, suppliers, quality engineers, and safety managers often establish internal control bands that are narrower than the nominal tolerance zone. This is not overprocessing. It is a risk-control response to stacked variation, inspection uncertainty, and the severe consequence of field failure.
For example, a dimension shown as ±0.05 mm may still be manufactured to an internal target of ±0.02 mm or tighter, depending on feature criticality, material stability, finishing steps, and assembly sensitivity. The drawing states acceptance. The process plan defines survivable production. That difference is where many supplier disputes, audit findings, and escape events begin.
What drives the tighter real-world control window?
- Critical-to-function features often influence load path, sealing, vibration behavior, or alignment with downstream assemblies, so nominal tolerance is not the full safety picture.
- Process drift during long production runs can push parts toward the edge of tolerance even when first articles look compliant.
- Measurement system uncertainty consumes part of the acceptance band, especially for thin-wall parts, complex curves, and high-value machined bores.
- Secondary operations such as anodizing, coating, grinding, peening, or heat treatment can shift geometry after the main machining step.
- Aerospace compliance frameworks such as AS9100 expect robust control of process capability, traceability, and nonconformity prevention, not simple pass-fail inspection at shipment.
This is exactly why TechStat Vanguard emphasizes data over marketing language. For quality and safety teams, the right question is not “Can the supplier meet the print?” but “What statistical margin, measurement discipline, and process evidence support repeatable conformance under production conditions?”
How aerospace machining precision tolerance standards affect quality risk
In commercial aerospace, UAV platforms, structural subassemblies, and mission-critical sensor mounts, tolerance is not an isolated geometric issue. It is a systems risk variable. A feature that technically passes inspection may still elevate assembly force, induce residual stress, shorten fatigue life, or reduce sensor alignment accuracy. Quality teams therefore need to connect dimensional control with downstream safety outcomes.
The table below summarizes why printed drawing tolerance and effective production tolerance are often different in aerospace machining precision tolerance standards.
For safety managers, the key lesson is simple: print compliance is necessary, but process capability evidence is what protects airworthiness, mission reliability, and supplier accountability. This is especially true when multiple precision features accumulate within one assembly path.
Common hidden risk points
- A supplier quotes to the drawing but does not disclose the capability index achieved on critical dimensions.
- First article results are strong, yet no evidence exists for stability across lot-to-lot production or machine-to-machine transfer.
- Inspection plans focus on nominal dimensions while profile, coaxiality, or datum repeatability remain weakly controlled.
- Heat treatment or coating suppliers are qualified separately, but dimensional change after subcontract processing is not fully modeled.
Which features usually need tighter control than nominal tolerance?
Not every feature requires the same discipline. Quality teams should distinguish between general dimensions and function-critical characteristics. In aerospace machining precision tolerance standards, the gap between drawing tolerance and internal process target is usually largest on features tied to fatigue, sealing, kinematics, thermal expansion fit, and sensor alignment.
Typical high-sensitivity feature categories
- Bearing seats and precision bores, where geometry affects rotation, preload, and wear.
- Mating faces and flange surfaces, where flatness and perpendicularity influence sealing and assembly stress.
- Thin-wall pockets and rib structures, where material release can distort the part after clamping changes.
- Hole patterns tied to datum structure, where positional tolerance affects fastener load sharing and interchangeability.
- Optical, radar, or sensor mounting interfaces, where very small angular or positional deviation can degrade system output.
When TSV reviews aerospace manufacturing data, one recurring pattern appears: suppliers that truly understand precision machining do not treat all tolerances equally. They build feature-specific control strategies, and those strategies often go beyond what inexperienced buyers expect from the print alone.
What should QC and safety teams verify before approving a supplier?
If your procurement team is comparing multiple shops, the most useful filter is not a generic promise of “tight tolerance machining.” It is documented evidence that the supplier can sustain aerospace machining precision tolerance standards through the entire production chain. That includes planning, machining, inspection, subcontract control, and traceability.
The following supplier evaluation table can help quality and safety leaders structure qualification decisions.
A capable supplier should be able to explain not only how a part is machined, but why each critical feature is measured in a certain sequence, how offsets are updated, and which dimensions are treated as process alarms before they become rejects. That level of detail separates controlled manufacturing from sales language.
A practical qualification checklist
- Map critical features to function, not just to drawing balloons.
- Ask which features are held tighter internally than the print and request the rationale.
- Review how the supplier manages tool wear, thermal growth, and machine qualification across shifts.
- Confirm inspection correlation between in-process checks and final CMM results.
- Audit traceability for raw material, special process steps, and revision updates.
Standards, certification, and the difference between compliance and capability
AS9100, customer specifications, GD&T frameworks, and documented first article processes all matter. But certification alone does not prove a supplier can consistently meet aerospace machining precision tolerance standards on difficult geometries. Quality systems establish discipline. Capability data proves execution.
For safety-focused organizations, the strongest approval decisions come from combining formal compliance review with technical benchmarking. This is where a data-driven approach becomes valuable. Rather than accepting broad claims, teams should compare actual process evidence: dimensional spread, rework rate on critical features, inspection repeatability, and dimensional behavior after secondary processes.
What certification can and cannot tell you
- Certification can indicate a structured management system, document control, and audit discipline.
- It cannot by itself confirm robust machining strategy for distortion-prone parts or high-tolerance 5-axis features.
- It can support traceability expectations and nonconformance handling.
- It does not replace evidence from capability studies, measurement validation, or part-family performance history.
That distinction matters in mixed-industry supply chains, where some shops serve medical, industrial, defense, and UAV programs simultaneously. Cross-sector experience can be useful, but aerospace acceptance still requires discipline specific to flight-critical risk and tolerance sensitivity.
Common misconceptions that create nonconformance risk
Many avoidable escapes begin with misunderstanding how tolerance should be interpreted in production. For QC and safety teams, correcting these assumptions can reduce supplier churn, audit friction, and costly rework.
Misconception 1: If it is within print, it is safe
A part can be dimensionally accepted and still carry elevated functional risk if the process is drifting, the datum structure is unstable, or the feature interacts with other stack-up contributors. Acceptance is a snapshot. Capability is a trend.
Misconception 2: Tighter control always means unnecessary cost
Sometimes it does increase cost, but often it lowers total lifecycle cost by reducing scrap, rework, concession requests, assembly delays, and field reliability risk. The right decision is feature-specific. Tighten what protects function and inspectability, not everything indiscriminately.
Misconception 3: The CMM result is the whole truth
Measurement results depend on setup, probing path, fixture repeatability, temperature, and evaluation method. A final report is important, but a robust tolerance strategy also needs correlation between in-process checks and final metrology.
Misconception 4: One successful first article proves production readiness
First article inspection proves that a documented configuration can produce one compliant outcome. It does not automatically prove sustained stability over a long-run schedule, different machines, new operators, or post-processing cycles.
FAQ: What do quality and safety leaders ask most often?
How should we evaluate aerospace machining precision tolerance standards during supplier sourcing?
Start with critical feature mapping. Then review process capability, gauge confidence, special process control, and nonconformance response. If a supplier only discusses machine count or general accuracy claims, the evaluation is incomplete. Ask how they center critical dimensions inside the tolerance band and how they react before drift becomes rejection.
Which documents are most useful when a drawing seems too loose for the application?
Useful documents include control plans, FAI records, inspection plans, process FMEA outputs, key characteristic lists, and any customer-specific requirements tied to critical features. These materials reveal whether the actual production strategy is narrower than the print and whether that tighter strategy is intentional and controlled.
Can internal tighter limits create supplier disputes?
Yes, if they are hidden or poorly documented. The best practice is to distinguish customer acceptance criteria from supplier internal control limits. Internal limits should guide process control, while shipment acceptance should remain tied to approved engineering requirements unless a formal revision or deviation changes them.
When should a safety team escalate dimensional concerns even if parts pass inspection?
Escalation is reasonable when trend data shows drift toward tolerance edges, when assembly force or fit behavior changes, when post-process movement increases, or when repeated rework appears on the same critical feature. A pass result with unstable trend data is a warning sign, not a comfort signal.
Why choose us for tolerance benchmarking and supplier evaluation support?
TechStat Vanguard was built for teams that need engineering truth rather than broad promotional claims. In hard-tech sectors where one tolerance decision can affect fatigue life, assembly success, or certification readiness, we focus on measurable evidence: process windows, benchmark comparisons, inspection logic, and supply chain traceability.
If your organization is reviewing aerospace machining precision tolerance standards, we can help you examine the details that most generic sourcing channels overlook.
- Parameter confirmation for critical dimensions, GD&T strategy, and function-linked tolerance interpretation.
- Supplier selection support based on process capability, inspection maturity, and special process control depth.
- Delivery risk review for new part introduction, first article planning, lot stability, and revision management.
- Customized benchmarking for aerospace, UAV, sensor, and precision machining programs where tolerance performance drives qualification.
- Discussion support for certification expectations, sample validation logic, quotation alignment, and technical comparison between candidate suppliers.
If you are facing unclear print interpretation, unstable supplier capability, or a high-stakes audit and qualification decision, contact us with the dimensions, feature priorities, target materials, expected batch profile, and certification context. TSV can help your team turn tolerance language into a clearer sourcing, inspection, and risk-control strategy.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























