
Precision machining for aerospace components starts with material behavior
Publication Date
author
Precision machining for aerospace components begins long before the first toolpath is programmed—it starts with how materials respond to heat, stress, vibration, and fatigue. For engineers and sourcing teams, understanding material behavior is the foundation for tighter tolerances, longer service life, and lower qualification risk. This article examines why data-driven material analysis is essential to aerospace machining decisions.
For most information researchers evaluating aerospace suppliers, the real question is not whether a machine shop owns a 5-axis CNC or claims aerospace experience. The more important question is whether that supplier understands how a specific alloy behaves during machining, inspection, assembly, and long-term service. In aerospace, material behavior is not a secondary technical detail. It is one of the main drivers of dimensional stability, repeatability, fatigue performance, and certification confidence.
The core search intent behind precision machining for aerospace components is usually practical and comparative. Readers want to understand how machining quality is affected by the materials being cut, what risks emerge when material properties are misunderstood, and how to judge whether a supplier has the process control needed for demanding aerospace parts. They are looking for decision-support information, not broad manufacturing theory.
That is why the most useful approach is to start with a clear conclusion: precision machining succeeds in aerospace when the machining process is built around verified material behavior data. This includes thermal expansion, hardness variation, residual stress, chip formation, work hardening, elastic recovery, and fatigue sensitivity. When these factors are ignored, even advanced equipment and experienced operators can struggle to deliver stable results at aerospace tolerances.
Why material behavior matters more than machine capability alone
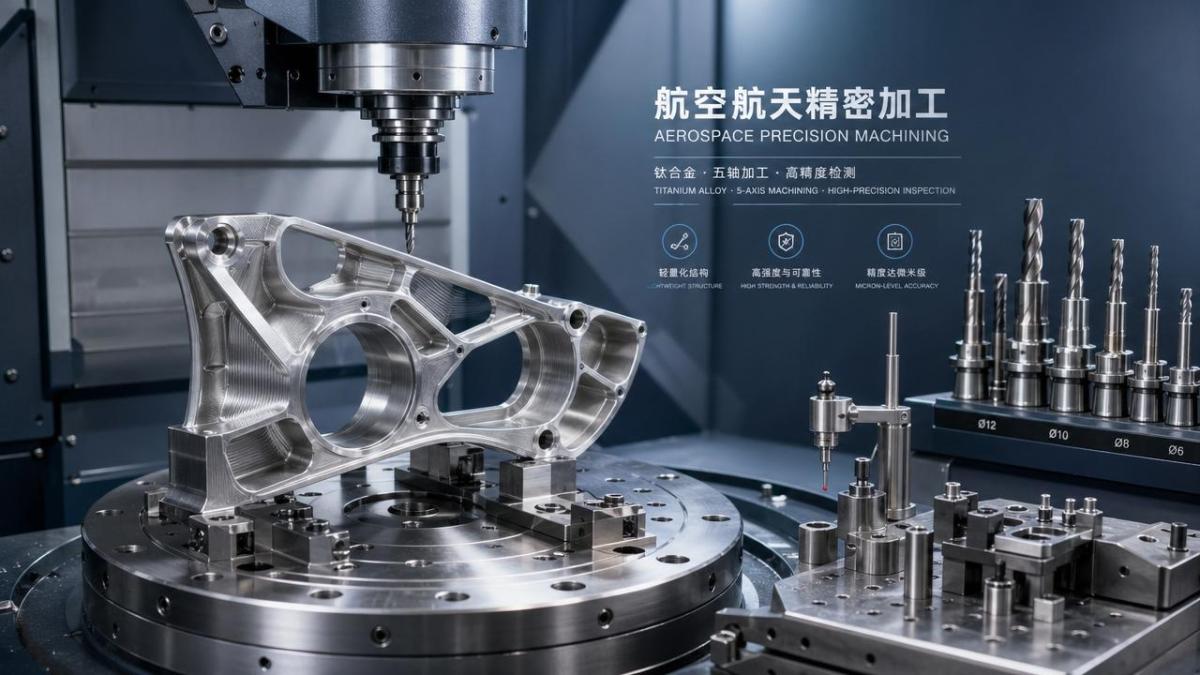
In many sourcing discussions, machine capability becomes the headline metric. Buyers ask about spindle speed, axis count, probing systems, or automation cells. Those factors matter, but they do not explain why one supplier can hold repeatable tolerances on thin-wall titanium brackets while another cannot. The difference often comes from how each supplier models and manages material response throughout the process.
Aerospace materials are selected for high strength-to-weight ratio, corrosion resistance, temperature performance, or fatigue durability. Those same advantages often make them difficult to machine. Titanium alloys generate heat and retain it near the cutting zone. Nickel-based superalloys can cause rapid tool wear and work hardening. Aluminum aerospace grades may be easier to cut, but they can still distort if residual stress is not controlled. Composite-metal hybrid structures introduce another layer of complexity, especially where burr control, delamination risk, or differential expansion must be considered.
For the reader trying to evaluate suppliers or understand process risk, this leads to a simple principle: machine tools create potential, but material knowledge creates consistency. Precision machining for aerospace components depends on turning material data into process decisions. Without that link, quoted tolerances may look impressive on paper while production stability remains weak.
What engineers and procurement teams are really trying to prevent
Information researchers in aerospace typically have a strong risk-prevention mindset. They are not just searching for a general explanation of machining. They want to avoid the failure modes that create cost, delay, and qualification uncertainty. These concerns usually appear in four forms.
First is dimensional drift. A component may pass first-article inspection, then fail to maintain the same dimensional results across lot production because material batches respond differently to cutting forces or thermal loads. Second is hidden structural damage. A part can meet dimensional requirements but still contain undesirable residual stress, microcracks, heat-affected zones, or surface integrity issues that reduce fatigue life.
Third is process instability. If a supplier lacks a stable machining strategy for a given alloy, lead times become unpredictable, scrap rates rise, and rework increases. Fourth is qualification risk. Aerospace programs often require documented traceability, repeatable inspection, and confidence that a process can survive audits, engineering changes, and scaling demands. Weak understanding of material behavior undermines all four areas.
For this audience, the value of a machining partner is not simply “can they make the part once?” It is “can they repeatedly make conforming parts from this material, under documented controls, with evidence that the process protects long-term performance?”
Which material properties have the biggest effect on aerospace machining outcomes
Not every material parameter has equal importance in a machining decision. For aerospace applications, several properties have outsized impact on manufacturability and final part quality.
Thermal behavior is one of the most critical. Materials with low thermal conductivity, such as titanium, tend to concentrate heat near the tool-workpiece interface. This can accelerate tool wear, shift dimensions during cutting, and affect surface integrity. Coefficients of thermal expansion also matter because small temperature changes can influence dimensional measurement and tolerance control, especially on larger or thinner components.
Strength and hardness influence cutting forces, tool selection, and cycle strategy. High-strength alloys may require slower material removal rates, specialized coatings, and more frequent tool monitoring. If hardness varies across a batch or due to prior heat treatment, process consistency can deteriorate quickly.
Elastic modulus and springback affect how thin-wall and complex geometries behave during and after machining. A part may deflect under clamping or cutting load, then recover when unclamped, creating geometric errors that are difficult to predict without prior material behavior data. Residual stress plays a similar role. If the raw stock contains significant internal stress, removing material can cause the part to warp even when the cutting program itself is correct.
Surface response is equally important. Some alloys are more prone to smearing, tearing, or work hardening, which changes the relationship between the tool and the surface being generated. In aerospace parts, surface integrity is not just an aesthetic concern. It can directly influence crack initiation, coating adhesion, sealing performance, and fatigue durability.
How material behavior shapes process planning before production starts
One of the clearest indicators of a mature aerospace machining supplier is what happens before chips are made. A strong supplier does not begin with generic CAM programming and hope experience will fill the gaps. Instead, they build the process around the behavior of the selected material, the part geometry, and the downstream performance requirement.
This usually starts with raw material review. The supplier should understand alloy designation, temper or heat-treatment state, grain direction where relevant, lot consistency, and certification traceability. Material behavior can differ significantly depending on upstream processing history. For a buyer or engineer, it is worth asking whether the supplier adjusts machining parameters based on incoming material condition rather than relying on a single standard setup.
Next comes fixture and clamping strategy. Materials that are prone to distortion require special attention to support points, clamping loads, intermediate stress relief, and sequencing of roughing and finishing passes. On thin-wall aerospace parts, the order of operations often matters as much as the machine itself.
Toolpath design should also reflect material-specific risk. High-heat alloys may need conservative engagement strategies, adaptive toolpaths, balanced chip load, and planned dwell avoidance. Materials with burr sensitivity or edge fragility may require separate finishing logic for critical features. If a supplier cannot explain why a cutting strategy was chosen for that material, that is a warning sign.
Finally, inspection planning must match the part’s sensitivity to temperature, relaxation, and deformation. Dimensional checks taken immediately after machining may not tell the full story if the material relaxes later. Mature suppliers account for this with controlled measurement conditions, in-process probing, post-process stabilization when needed, and feature-specific inspection plans.
Why aerospace tolerances are inseparable from surface integrity and fatigue performance
Many non-specialists treat tolerance and strength as separate topics. In aerospace, they are connected through the way the surface and subsurface are created during machining. A dimensionally acceptable part can still present unacceptable operational risk if the cutting process damages fatigue-critical regions.
Surface roughness is only the visible layer of the issue. Beneath the surface, machining can introduce tensile residual stress, localized hardening, smeared material, recast effects in some special processes, or microstructural alteration caused by excessive heat. These conditions may not be obvious in routine dimensional inspection, but they can influence crack initiation under cyclic loading.
This is why aerospace machining decisions should not rely only on tolerance capability charts. The more useful question is whether the supplier can connect machining parameters to final surface integrity requirements. For rotating parts, brackets under vibration, structural housings, and components exposed to thermal cycling, this relationship becomes especially important.
From a sourcing perspective, suppliers that discuss fatigue only at the material certificate level may be missing the full picture. The certificate describes the bulk material. The machining process helps determine whether the finished part preserves or degrades the performance that the material was chosen to provide.
How to evaluate a supplier’s understanding of material behavior
For information researchers comparing machining partners, the challenge is often practical: what evidence shows that a supplier truly understands material behavior rather than simply marketing aerospace capability? The answer usually lies in the specificity of their process controls and technical communication.
Start by looking for process-material pairing logic. Can the supplier explain how they machine titanium differently from Inconel, or how they control deformation in high-strength aluminum structures? The explanation should include cutting strategy, tool wear management, heat control, fixturing, inspection timing, and risk mitigation for the geometry involved.
Ask about historical data. Reliable aerospace suppliers often maintain internal benchmarks on tool life, dimensional repeatability, scrap causes, and process windows by material type. They may not disclose proprietary details, but they should be able to speak clearly about lessons learned and the variables they monitor. Vague claims such as “we can machine all aerospace alloys” are far less useful than data-backed statements about specific material families and part classes.
It is also important to review quality evidence through a material-behavior lens. AS9100 certification matters, but it is not a substitute for technical depth. Ask whether the supplier has procedures for stress-relief decisions, first-article validation on difficult materials, lot traceability, thermal control during measurement, and handling of fatigue-sensitive surfaces.
Another strong signal is cross-functional involvement. Shops that perform well on aerospace work often involve manufacturing engineers, quality engineers, programmers, and sometimes materials specialists early in the quote or planning stage. That collaboration suggests they are evaluating real process risk, not simply estimating machine hours.
Common mistakes when material behavior is treated as an afterthought
The aerospace sector is full of examples where machining problems were blamed on equipment, operators, or inspection, when the deeper cause was inadequate attention to material behavior. Several mistakes appear repeatedly.
One is assuming the same alloy always behaves the same way. In reality, condition, source, heat treatment, and stock geometry can change machining response enough to affect process capability. Another is prioritizing cycle time over thermal stability too early. Aggressive material removal may look efficient until distortion, accelerated tool wear, or surface damage creates downstream cost.
A third mistake is validating success using only initial dimensional results. If the part warps after unclamping, after coating, or after environmental exposure, the true process capability was never proven. Fourth is underestimating the impact of residual stress in raw stock and semi-finished parts. This is especially risky in pocketed or thin-wall aerospace structures.
There is also a commercial mistake: choosing suppliers based mainly on equipment lists or headline tolerances without examining how those results are achieved. Precision machining for aerospace components is not a commodity service. If material behavior is not being actively modeled and managed, the buying organization may inherit hidden risk even when the initial quote is attractive.
What a data-driven decision framework looks like
For organizations trying to make better sourcing or engineering decisions, the most practical solution is a data-driven framework that links material behavior to machining performance and final application requirements. This approach is especially aligned with the needs of aerospace teams that want to reduce qualification cycles and avoid trial-and-error costs.
The framework begins with the application environment: load profile, temperature range, vibration exposure, fatigue expectations, corrosion conditions, and weight targets. From there, material selection should be assessed not only for functional properties but also for machinability risk. A technically optimal alloy that is poorly matched to the supply chain’s machining capability may create avoidable delays or yield loss.
Next, the process plan should identify the material-sensitive variables most likely to affect quality. These may include thermal buildup, deflection, residual stress release, burr formation, tool wear progression, and post-machining stability. Suppliers should then show how they monitor or control those variables using proven methods rather than assumptions.
The final layer is verification. This goes beyond dimensional inspection to include evidence that the process protects the intended part performance. Depending on the component, that may involve surface integrity analysis, repeatability studies, process capability data, lot traceability, and documented controls for special finishing or post-processing steps.
When this framework is in place, decision-makers can compare suppliers more intelligently. Instead of asking only who can hit the print, they can ask who best understands the relationship between material behavior, process stability, and service performance.
Conclusion: the best aerospace machining decisions start with engineering truth
Precision machining for aerospace components starts with material behavior because aerospace risk starts there too. Tolerances, surface integrity, fatigue life, and production repeatability are all shaped by how a material responds to cutting, heat, stress, fixturing, and inspection. Advanced machine tools matter, but they are not enough on their own.
For engineers, buyers, and technical researchers, the most valuable takeaway is straightforward: judge aerospace machining capability by the quality of the supplier’s material understanding and the data discipline behind their process. Shops that can explain, measure, and control material-driven variables are far more likely to deliver stable quality, lower qualification risk, and better long-term performance.
In a market full of generic claims, engineering truth comes from specifics. Ask how the alloy behaves. Ask how the process adapts. Ask what data proves repeatability. That is where meaningful supplier evaluation begins, and it is the foundation of smarter aerospace manufacturing decisions.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























