
Why aerospace components fail precision targets after setup looks perfect
Publication Date
author
A setup can look flawless on the screen yet still miss the mark on the shop floor. In precision machining for aerospace components, micron-level errors often come from hidden factors such as thermal drift, tool deflection, fixture instability, and material response under load. This article explains why parts fail precision targets after a seemingly perfect setup, helping operators identify the real variables that determine repeatable aerospace accuracy.
Why a “perfect” setup still fails in precision machining for aerospace components
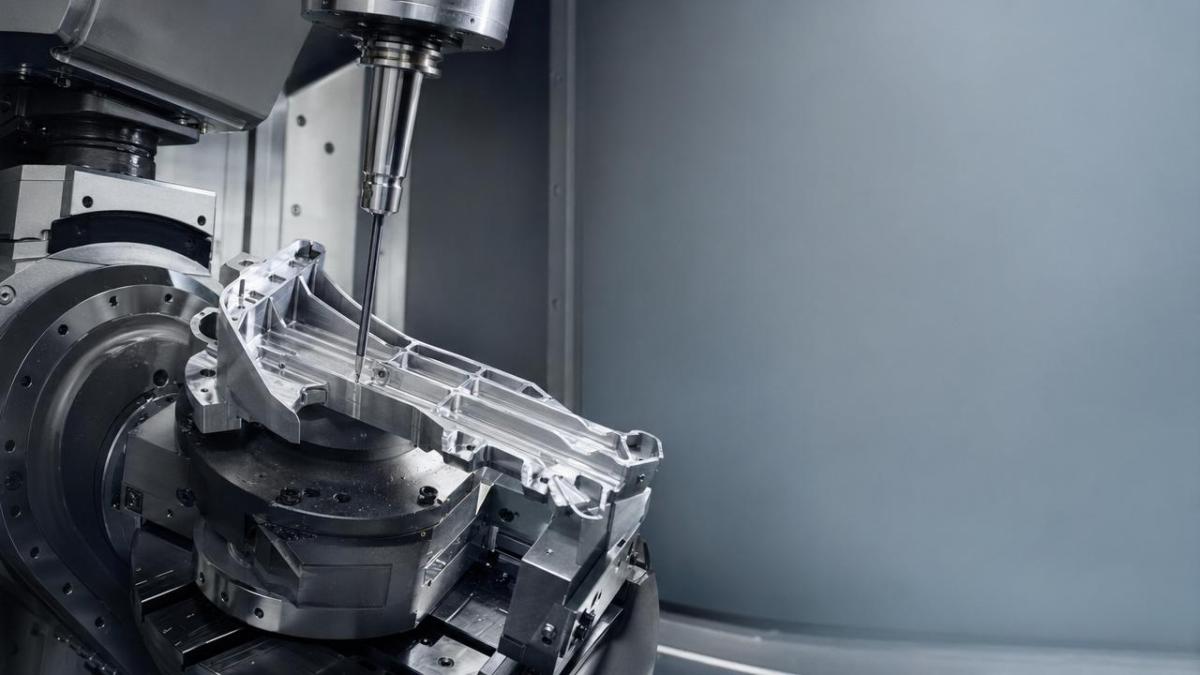
For operators, the most frustrating scrap event is not a visible mistake. It is the part that looks correct in simulation, aligns correctly in setup, passes initial probing, and then drifts out of tolerance halfway through the cycle or between batches. This is common in precision machining for aerospace components because aerospace tolerances are often influenced by system behavior, not just by static setup geometry.
In other words, a machine can be correctly set and still be dynamically wrong. Heat builds up. Spindle growth changes effective Z position. Long-reach tools bend under load. Vacuum or mechanical clamping alters wall geometry. Aluminum, titanium, Inconel, and carbon-filled structures do not react the same way during cutting. If the operator only verifies the starting condition, the process may appear stable while the actual cut is moving.
This is where TechStat Vanguard (TSV) brings practical value. TSV’s engineering-first approach focuses on measurable parameters, traceable process behavior, and benchmark thinking rather than generic claims. For users and operators, that matters because troubleshooting precision machining for aerospace components requires evidence: how much thermal drift, under what spindle load, with which tool stick-out, on what material, across what cycle time.
- Static setup accuracy does not guarantee dynamic cutting accuracy.
- Aerospace parts amplify small errors because of thin walls, deep cavities, and tight GD&T requirements.
- Repeatability is usually lost through interacting variables, not one obvious mistake.
What operators often see on the shop floor
A hole pattern may drift by a few microns after lunch shift. A pocket floor may trend shallow when the machine warms. A thin rib may spring after unclamping. Surface finish may worsen only on one side of the feature. These patterns do not point to a bad setup alone. They point to a process that has not been fully characterized under real cutting conditions.
Which hidden variables usually break aerospace tolerance targets
When troubleshooting precision machining for aerospace components, operators should stop asking only, “Was the setup correct?” and start asking, “What changed once metal removal started?” The table below summarizes the most common hidden variables behind post-setup deviation.
These four variables matter because they often act together. A long tool on a warming spindle cutting a thin-wall titanium bracket in a stressed fixture can pass first-article checks and still fail by the tenth part. In precision machining for aerospace components, process interaction is usually the real source of error.
Thermal drift is not just a machine issue
Operators often associate thermal drift with spindle growth alone, but the larger system matters too. Coolant temperature, fixture mass, part soak time, probing timing, and even the order of operations can affect measurement. If roughing creates heat and finishing starts before the structure stabilizes, dimensions can move after inspection.
Tool deflection hides inside “acceptable” parameters
A CAM program can use reasonable feeds and speeds and still produce inaccurate geometry. In aerospace work, deep cavities and hard-to-reach features often force higher stick-out. Even if the spindle load looks acceptable, deflection may be enough to shift profile, wall thickness, or true position. This is why TSV emphasizes benchmark logic: parameters should be judged against the actual geometry and material condition, not only against a generic tooling catalog range.
How to diagnose failure after setup: a practical operator workflow
When precision machining for aerospace components misses target after setup, random offset correction is risky. It may hide the symptom while leaving the root cause untouched. A more reliable workflow is to separate the failure into machine behavior, tool behavior, fixture behavior, and material behavior.
- Confirm whether deviation is consistent, trending, or position-dependent. A stable offset suggests geometry; a trend suggests heat or wear; a localized error suggests deflection or clamping distortion.
- Compare first-part and later-part data. If the process shifts with runtime, document spindle time, coolant state, and ambient conditions.
- Inspect measurement timing. Measuring immediately after machining and measuring after thermal stabilization can produce different conclusions.
- Review tool path engagement. Cornering load, entry strategy, and finishing allowance may explain why one region fails while another remains accurate.
- Check unclamped geometry where applicable. Thin aerospace structures may distort only after release, especially when stock removal is asymmetrical.
This workflow reduces trial-and-error and aligns with TSV’s data-driven philosophy. Operators do not need more hype. They need traceable process signals that can be repeated, compared, and improved batch after batch.
What data should be recorded every time
- Machine runtime before finishing pass begins.
- Tool number, measured length, stick-out, and cumulative cutting time.
- Fixture configuration, clamp torque or pressure, and support-point changes.
- Material lot, heat treatment condition, and any known residual stress note.
- Measurement timing, gauge method, and whether the part was clamped or free-state.
Comparison guide: setup accuracy vs process capability in aerospace machining
Many operators and even some buyers judge a shop by setup discipline alone. That is necessary, but not sufficient. In precision machining for aerospace components, the stronger indicator is whether the supplier can maintain capability under real production conditions. The table below highlights the difference.
For procurement teams and operators evaluating subcontractors, this distinction is critical. A supplier may produce an excellent first article yet struggle with repeat production. TSV’s benchmark mindset is useful here because it replaces vague supplier claims with verifiable process questions.
Questions worth asking a machining partner
- How is thermal stability controlled before finishing aerospace-critical features?
- How is tool life managed for long-reach finishing tools?
- How is free-state distortion evaluated for thin-wall parts?
- What process data are recorded when capability begins to drift?
What standards and process controls matter most
Precision machining for aerospace components operates under stricter expectations than general industrial work. Although exact requirements depend on part type and customer drawings, operators should be familiar with the practical implications of aerospace quality systems, documented inspection practices, and disciplined process control.
Key control areas to verify
- Traceability: material lot, tooling records, setup revisions, and inspection history should be recoverable.
- Calibration discipline: probes, tool setters, micrometers, bore gauges, and CMM programs must be controlled and current.
- Process validation: high-risk features should be checked by in-process verification, not only final inspection.
- Change control: modified tools, substitute inserts, changed coolants, or updated clamp methods should not be treated as minor details.
Operators may not own the full quality system, but they are the first line of detection. Many tolerance escapes begin as small process changes that nobody logged because the setup looked normal. In aerospace work, normal-looking drift is still drift.
Common misconceptions in precision machining for aerospace components
Several shop-floor beliefs continue to cause avoidable precision loss. Clearing them up helps users make better decisions faster.
“If the first part is good, the process is good”
Not necessarily. First-part approval proves initial geometry. It does not prove thermal stability, wear behavior, or distortion after repeated cycles. Aerospace capability is about sustained repeatability.
“Offsets can fix any drift”
Offsets are useful for controlled compensation, but they are a poor substitute for root-cause analysis. If the real problem is fixture distortion or tool bending, offset changes may correct one feature while pushing another out of tolerance.
“Harder materials are the only precision risk”
Titanium and nickel alloys are difficult, but softer aerospace alloys can be just as risky when the geometry is thin, heat-sensitive, or prone to burr and spring-back. Material behavior must be matched to feature type, not judged by hardness alone.
FAQ: what operators and buyers usually ask
How do I know whether failure comes from the machine or the fixture?
Look at the failure pattern. If multiple features trend together over runtime, thermal machine behavior is likely involved. If one wall, one pocket, or one free-state profile changes after clamp release, the fixture is a stronger suspect. Repeating a cut with altered clamp force or support location often reveals the difference quickly.
What should be prioritized when buying precision machining for aerospace components?
Prioritize evidence of repeatability, not just equipment lists. Ask for process-control logic, inspection flow, material traceability, and how the supplier manages thermal stability, tool wear, and distortion on similar geometry. A modern machine alone does not guarantee aerospace capability.
Are probing systems enough to protect micron-level accuracy?
They help, but probing is only one layer. It confirms position at a moment in time. It does not automatically solve changing cutting forces, fixture movement, tool wear, or post-machining stress relief. Use probing as part of a broader control plan.
Why do thin-wall aerospace parts pass inspection while clamped but fail later?
Because the clamp can temporarily force the geometry into position. Once the load is removed, residual stress and low structural stiffness allow the part to relax. Free-state inspection strategy should be defined early, especially for brackets, housings, frames, and lightweighted structures.
Why choose us for data-backed evaluation and sourcing decisions
TechStat Vanguard supports engineering teams, procurement leaders, and shop-floor users who need more than sales language. Our value is in translating hard-tech complexity into decision-ready benchmarks. In precision machining for aerospace components, that means focusing on tolerance behavior, process evidence, traceability logic, and measurable production risk.
If you are validating a machining partner, narrowing suppliers, or trying to understand why a stable-looking setup still produces unstable parts, we can help frame the right questions and evaluation criteria. That includes practical guidance on parameter confirmation, supplier selection logic, aerospace machining benchmarks, process risk review, delivery-cycle discussion points, and what to request when sample validation is required.
- Consult us for parameter review when tolerance failures appear after otherwise correct setup.
- Consult us for supplier comparison if you need a clearer basis for product selection and capability screening.
- Consult us for delivery and process-risk evaluation when deadlines are tight and rework is expensive.
- Consult us for certification and documentation checkpoints when aerospace compliance and traceability matter.
- Consult us for quote-stage technical clarification so cost discussions are based on real process requirements, not assumptions.
In advanced manufacturing, attractive claims do not protect tolerances. Verified parameters do. That is the gap TSV is built to close.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























