
What 5-axis CNC machining fatigue test reports can actually reveal
Publication Date
author
For technical evaluators, 5-axis CNC machining fatigue test reports can reveal far more than a supplier’s headline claims. When read correctly, they expose how part geometry, toolpath strategy, material behavior, and process stability affect real-world durability, risk, and consistency. This article explains which data points matter most—and how to turn raw test results into smarter sourcing and engineering decisions.
Why are 5-axis CNC machining fatigue test reports getting so much attention?
Technical evaluators are under pressure to qualify suppliers faster while reducing hidden reliability risk. In that context, 5-axis CNC machining fatigue test reports matter because they move the conversation away from marketing language and into measurable engineering evidence. A supplier may promise tight tolerances, advanced machines, or premium alloys, but fatigue data shows whether those claims survive repeated loading over time.
This is especially relevant in aerospace, robotics, industrial automation, medical hardware, UAV structures, and other high-consequence applications where failure rarely comes from one dramatic overload event. More often, it comes from cyclic stress, microcrack initiation, residual stress concentration, or process inconsistency. A good report can therefore reveal not only the durability of one sample part, but also the maturity of the machining process behind it.
At a deeper level, fatigue performance is a systems issue. It reflects fixture stability, spindle behavior, tool wear control, surface finish strategy, feature accessibility, and the way a supplier handles multi-axis interpolation on complex geometry. That is why 5-axis CNC machining fatigue test reports are increasingly used as part of supplier qualification, design-for-manufacturing review, and risk-based sourcing.
What can these reports actually reveal beyond a pass or fail result?
A pass/fail outcome is the least useful part of many reports. The real value lies in the data trail behind the conclusion. For example, the report may show the load ratio, cycle count, frequency, specimen geometry, stress level progression, crack initiation location, and environmental conditions. Each of these details can change the meaning of the result.
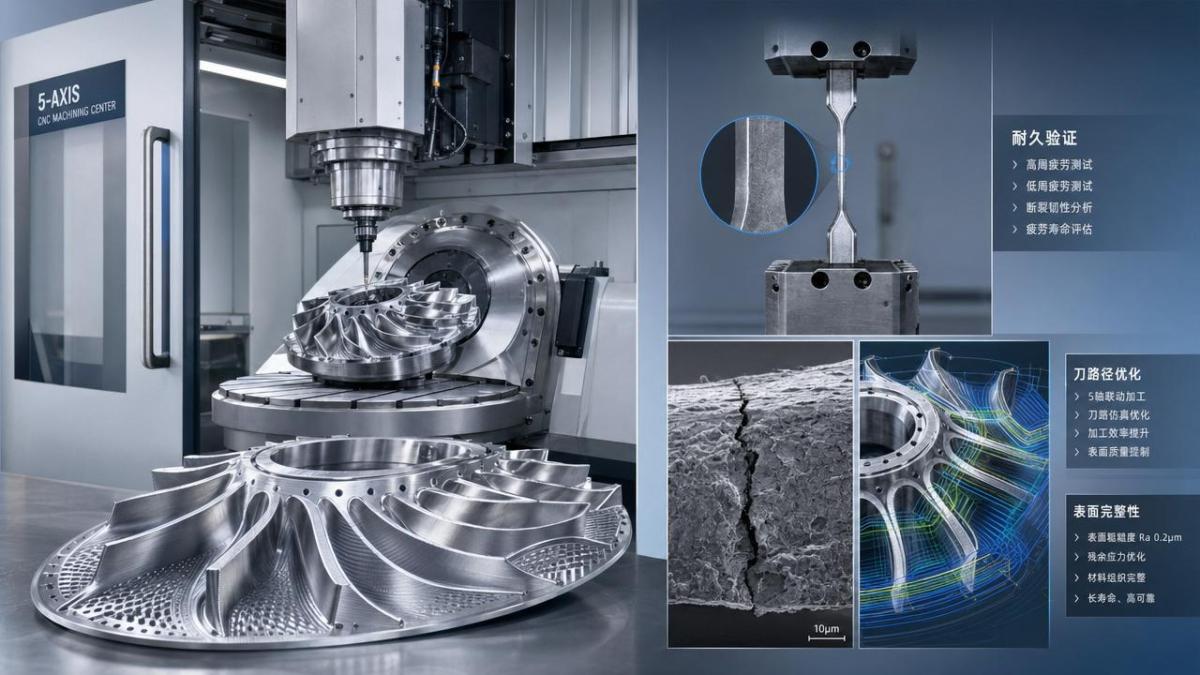
For technical evaluators, the report can reveal whether the machining process left behind fatigue-sensitive features such as cusp marks, sharp tool exit transitions, chatter signatures, recast-like thermal damage, or anisotropic surface texture. In 5-axis machining, the tool orientation and path planning can strongly influence these surface conditions. Two suppliers using the same alloy and nominal dimensions may produce very different fatigue behavior because one controls surface integrity better than the other.
The report may also expose process stability. If one batch shows a tight fatigue life distribution and another shows wide scatter, that variation may indicate inconsistent tool condition, changing cutter engagement, weak workholding, or poor parameter locking across shifts. In sourcing terms, this is often more important than the single best result. A supplier that occasionally produces excellent parts but cannot reproduce them reliably is still a qualification risk.
Which data points in 5-axis CNC machining fatigue test reports deserve the closest attention?
Start with specimen definition. If the test coupon does not reflect the actual machined geometry, feature transitions, wall thickness, corner radii, or surface accessibility of the final part, the fatigue result may look stronger than real service performance. Evaluators should ask whether the specimen was a simplified bar, a representative subcomponent, or the true production geometry.
Next, examine material traceability. The alloy designation alone is not enough. Heat lot, grain direction where relevant, prior processing history, and any heat treatment sequence should be documented. Fatigue behavior can shift significantly when the starting material condition changes, even before machining effects are considered.
Surface integrity data is often the hidden core of the report. Useful reports discuss roughness values, but strong reports go further and include burr control, microhardness near the surface, evidence of tensile or compressive residual stress, and microscopic observations at crack initiation zones. This matters because fatigue commonly begins at the surface, and 5-axis tool access paths can create nonuniform conditions across different faces of the same part.
Also review the loading method. Axial, bending, rotating bending, vibration-based, and combined loading do not tell the same story. If a component in service sees multiaxial stress but the report uses a simpler uniaxial setup, the result may still be useful, but only if its limitations are acknowledged. Technical evaluators should map the test method back to the application instead of accepting the number at face value.
Finally, look for statistical treatment. How many specimens were tested? Was there an S-N curve, confidence interval, Weibull analysis, or simple average only? A fatigue claim based on too few samples can create false confidence. Reports with transparent scatter data are generally more trustworthy than reports that present only one optimized headline figure.
How do you judge whether a report reflects real production capability rather than a one-time lab success?
This is where many sourcing decisions fail. A polished fatigue report may prove that one carefully prepared sample survived a demanding test, but it may not prove that the supplier can repeat that outcome in production volume. To bridge that gap, evaluators should compare test evidence with process control evidence.
Ask whether the tested parts came from the same machines, fixtures, cutting tools, CAM strategy, and inspection sequence used in standard production. If the fatigue specimens were produced in a special engineering run with extra polishing, reduced feed rates, hand blending, or nonstandard operator intervention, then the report reflects a best-case demonstration rather than production reality.
Batch consistency is another key indicator. If the report includes multiple lots, repeat runs, or before-and-after process changes, you can learn whether the supplier understands causality. For example, a report that shows improved fatigue life after adjusting tool tilt, step-over, and finishing pass strategy is much more informative than one that simply states a final result. It shows the supplier can connect 5-axis machining parameters to fatigue outcomes and optimize deliberately.
For organizations aligned with data-first engineering principles, this distinction is crucial. Engineering truth comes from reproducible parameters, not isolated outcomes. The best 5-axis CNC machining fatigue test reports therefore act as part of a larger validation chain that includes Cpk trends, inspection records, tool life rules, nonconformance history, and corrective action logic.
What are the most common mistakes when reading 5-axis CNC machining fatigue test reports?
One common mistake is focusing only on cycle count without understanding stress amplitude. A part surviving a high number of cycles at a relatively low stress level may be less impressive than a lower cycle count under more demanding loading. Numbers need context.
Another mistake is assuming dimensional accuracy guarantees fatigue strength. Tight tolerance control is important, but fatigue life is heavily influenced by surface integrity, subsurface damage, edge condition, and local geometry transitions. A component can be dimensionally perfect and still fatigue early if machining induced harmful residual stress or micro-notching.
Evaluators also sometimes ignore fixture and orientation effects. In 5-axis machining, changing the setup approach can alter cutter reach, vibration, heat buildup, and finish pattern. If the tested orientation differs from production orientation, the report may not represent ongoing output. Likewise, post-processing such as shot peening, polishing, anodizing, coating, or deburring can radically affect fatigue behavior. If these steps are missing, undocumented, or inconsistent with final production flow, the report may overstate or understate actual performance.
A final mistake is treating all failures as material failures. Fractography often reveals whether cracking initiated at a machining mark, inclusion, pore, edge defect, or design hotspot. Without failure origin analysis, the report may identify that a part failed but not why it failed. For qualification decisions, the “why” is usually the most valuable part.
What quick-reference checklist should technical evaluators use?
The table below summarizes how to read 5-axis CNC machining fatigue test reports more critically during supplier review, process benchmarking, or design validation.
When should a technical evaluator trust the report, and when should they ask for more proof?
Trust increases when 5-axis CNC machining fatigue test reports are specific, traceable, statistically transparent, and clearly connected to the final part configuration. Reports become more credible when they include process windows, not just outputs; when they show both successes and scatter; and when failure analysis is treated as engineering evidence rather than something to hide.
Ask for more proof when the report feels too clean. Missing sample counts, undocumented post-processing, unclear specimen geometry, absent lot traceability, or vague statements about proprietary optimization should all trigger follow-up questions. The same applies if the fatigue result looks exceptional but no corresponding explanation exists in machining strategy or surface condition data.
In practical sourcing workflows, the next step is often not to reject the supplier outright but to request a focused validation package. That package may include representative-part testing, metallography, residual stress data, repeat-batch comparisons, machine capability records, and a side-by-side review of CAM strategy changes. This approach protects engineering teams from both underestimating a capable supplier and overcommitting to one with unstable process control.
What should you confirm before moving toward sourcing, approval, or deeper technical review?
Before using 5-axis CNC machining fatigue test reports as a basis for approval, confirm five things: whether the tested geometry matches the functional risk zones of your part, whether the material condition matches production intent, whether the machining route is reproducible at scale, whether the fatigue method reflects service loading, and whether the statistical evidence is strong enough for your consequence level.
If you need to advance the conversation with a supplier, start with targeted questions instead of broad requests. Ask which exact surfaces were finish-machined in the final pass, how tool wear limits are controlled, whether edge preparation was manual or standardized, how many lots were included in the fatigue dataset, and where cracks initiated in failed samples. These questions quickly reveal whether the supplier truly understands the relationship between 5-axis machining and fatigue performance.
For technical evaluators, the goal is not simply to collect more documents. It is to reduce uncertainty. The best use of 5-axis CNC machining fatigue test reports is to turn raw test results into an evidence-based view of supplier capability, long-term durability, and manufacturing truth. If deeper confirmation is needed, prioritize discussion around representative geometry, process repeatability, sample statistics, failure origin, and any post-processing steps that materially influence fatigue life.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026How Do You Verify Servo Motor Torque Under Continuous Load?How do I verify servo motor torque under continuous load? Learn RMS torque checks, torque-speed limits, thermal derating, and real-machine testing.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 29, 2026How MES and OEE work together to identify production lossesMES and OEE work together to uncover hidden production losses, connect downtime, speed, and quality data, and drive smarter shop-floor improvements.Victor Lin (Chief Software Architect)
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab























