
Surface finish standards that change aerospace rework rates
Publication Date
author
In aerospace manufacturing, minor deviations in precision machining surface finish standards can trigger major rework, inspection delays, and safety concerns. For quality control and safety managers, understanding how roughness thresholds, process consistency, and compliance benchmarks affect part acceptance is essential. This article examines the surface finish criteria that most directly influence aerospace rework rates and why tighter data-based standards lead to lower risk and stronger production reliability.
What precision machining surface finish standards mean in aerospace
In practical terms, precision machining surface finish standards define the allowable condition of a machined surface after milling, turning, grinding, honing, or polishing. In aerospace, this is not a cosmetic issue. Surface texture influences fatigue initiation, friction behavior, sealing performance, coating adhesion, corrosion resistance, and dimensional fit. A part may pass dimensional inspection yet still fail acceptance if its surface profile falls outside specified roughness or waviness limits.
For quality control teams, the most common language of these standards includes Ra, Rz, Rt, waviness, lay direction, burr control, and edge condition. For safety managers, these parameters matter because poor finish can create stress concentrators, contamination traps, or leakage paths in critical assemblies. This is why precision machining surface finish standards are deeply tied to process capability, inspection discipline, and airworthiness compliance rather than simple appearance.
Aerospace programs often reference AS9100 quality systems, customer engineering drawings, NADCAP-linked special process requirements, and internal acceptance criteria. Yet the real driver of rework rates is not the existence of a standard alone. It is the accuracy, clarity, and consistency with which that standard is translated into machining parameters, measurement methods, and supplier communication.
Why the industry pays close attention to finish-related rework
Aerospace manufacturing operates within narrow process windows. Components made from titanium, Inconel, aluminum-lithium alloys, and hardened steels are frequently thin-walled, high-value, and difficult to machine. When a surface finish defect appears, the cost impact is often disproportionate. Rework may require additional blending, polishing, re-inspection, cleaning, or even scrapping a near-complete part.
This concern has grown as production cycles shorten and traceability demands rise. Global engineering teams want measurable truth, not vague quality claims. That is why organizations such as TechStat Vanguard emphasize parameter-driven analysis. In a high-risk environment, phrases like “excellent finish” are meaningless unless tied to exact thresholds, measurement cutoff settings, probe calibration, and process repeatability. Parameters do not lie, and in aerospace, tolerances dictate success.
Another reason for heightened attention is that finish-related nonconformance often cascades into other failures. A rough sealing face can cause pressure loss. A poor surface on a bearing journal can accelerate wear. Excessive tool marks on a structural feature can reduce fatigue life. What begins as a finish issue can quickly become a reliability, safety, and certification issue.
The finish criteria that most often change aerospace rework rates
Not all surface specifications carry equal rework risk. Certain finish criteria consistently drive nonconformance in aerospace programs because they are either difficult to machine consistently or easy to misinterpret during inspection.
- Ra threshold accuracy: Average roughness remains the most cited requirement. Rework rises when drawing limits are tighter than process capability or when material behavior changes tool response.
- Rz and peak-valley control: Two parts with similar Ra can have different peak structures. This matters for fatigue-sensitive or sealing-critical surfaces.
- Waviness separation: A surface may meet roughness limits but fail due to broader undulations caused by vibration, machine instability, or fixturing errors.
- Lay direction: Surface pattern orientation affects lubrication retention, aerodynamic behavior, and seal contact performance.
- Burrs and edge breakout: These are among the most common causes of manual rework, especially on holes, slots, and intersecting features.
- Measurement method consistency: Different stylus settings, filters, sampling lengths, or optical systems can produce conflicting results on the same part.
For quality personnel, the lesson is clear: precision machining surface finish standards must specify not only the target value but also the evaluation method. Ambiguity creates preventable rework.
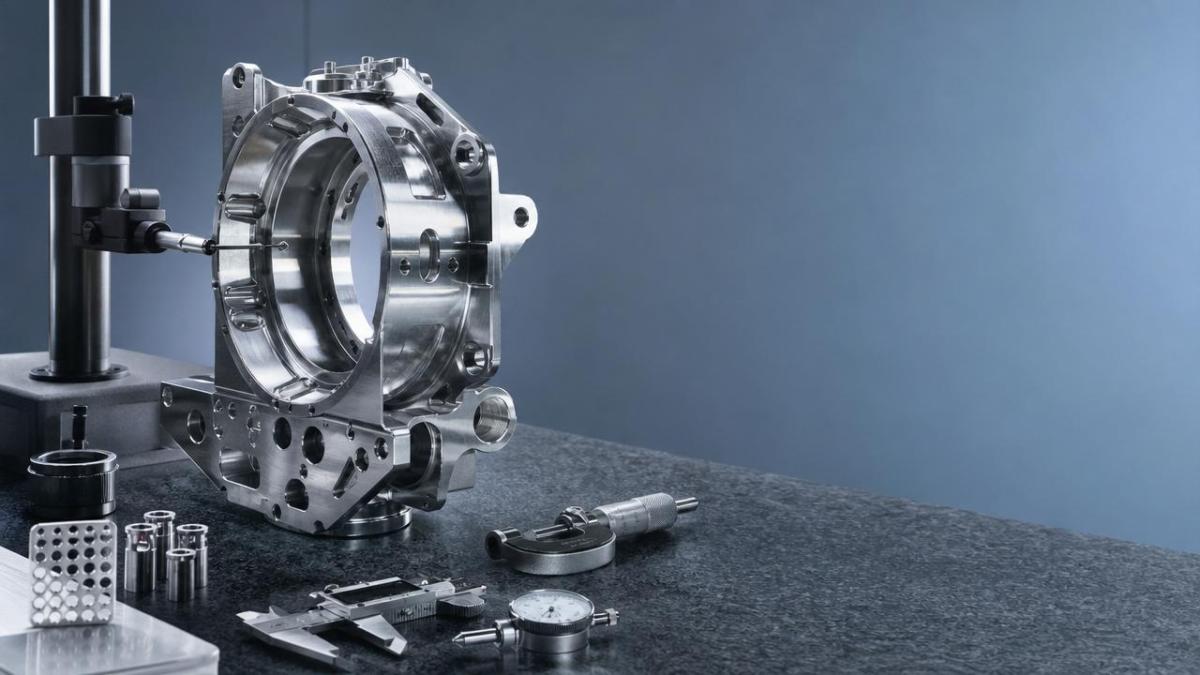
Industry overview: where finish standards matter most
The influence of surface finish varies by component function. The table below shows where finish control usually has the highest effect on acceptance and rework exposure.
Why some finish standards create avoidable nonconformance
Many finish-related rework events are not caused by poor machining alone. They are caused by incomplete specification design. Drawings may state a single roughness value without noting whether it applies before or after coating, whether lay is controlled, or whether hidden internal features require verification by replica, borescope, or alternative metrology. Suppliers then interpret the requirement differently, and incoming inspection discovers the gap too late.
A second issue is mismatch between machine capability and finish expectation. Tight precision machining surface finish standards on difficult alloys can be realistic only if tooling, coolant delivery, spindle condition, fixture rigidity, and toolpath strategy are optimized together. When planners inherit a finish callout without validating process capability data, rework becomes predictable.
Third, inspection inconsistency creates false positives and false negatives. A contact profilometer may react differently on curved features than an optical system. Filter choice can suppress or exaggerate critical peaks. If multiple plants or suppliers are involved, the same part may be accepted in one location and rejected in another. For quality managers, standardization of measurement protocol is as important as the finish target itself.
Business value for quality control and safety management teams
For quality control teams, strong precision machining surface finish standards reduce defect escape, support supplier qualification, and improve first-pass yield. Better finish governance also shortens root-cause analysis because the acceptance logic is traceable. Instead of debating subjective appearance, teams can compare verified process and metrology data.
For safety managers, the value is risk containment. Surface anomalies may not always cause immediate failure, but they can reduce fatigue margin, weaken pressure integrity, or accelerate field wear. When finish criteria are data-based and enforced consistently, the organization lowers both operational risk and documentation risk. This is especially important in regulated sectors where auditability matters as much as the part itself.
At the enterprise level, fewer finish disputes mean less production friction across design, manufacturing, sourcing, and inspection. That aligns with TSV’s broader vision of using engineering truth to cut through noise. In hard-tech supply chains, reliable parameters are the bridge between capability claims and operational trust.
Common aerospace scenarios and the right finish focus
Practical guidance for lowering rework through better standards
A practical surface finish strategy should begin upstream, not on the shop floor after a rejection. First, define function-based finish requirements. A fatigue-critical face, a sealing groove, and a cosmetic exterior should not inherit the same callout by habit. Match the requirement to the engineering purpose.
Second, pair every precision machining surface finish standard with a measurement rule. Identify parameter type, cutoff, sampling length, instrument type, and access method for difficult features. This reduces interpretation gaps across internal teams and external suppliers.
Third, connect finish targets to process capability data. If a supplier can repeatedly hold the requirement only with special tooling or low throughput, planners should know that before release. Capability evidence is more useful than broad quality promises.
Fourth, monitor trend data instead of only pass-fail outcomes. Rework rates often rise gradually as tools wear, spindle balance changes, or coolant performance drifts. Control charts for roughness and waviness can reveal instability before a batch fails.
Fifth, train inspectors and machinists together. Finish quality is one of the few areas where manufacturing technique and inspection interpretation are tightly linked. Shared understanding reduces conflict and improves corrective action speed.
A data-based path forward
The aerospace sector will continue tightening expectations around traceability, repeatability, and supplier verification. In that environment, precision machining surface finish standards should be treated as operational risk controls, not secondary drawing notes. The organizations that reduce rework most effectively are usually the ones that define surface requirements clearly, validate them with real capability data, and enforce one measurement language across the supply chain.
For quality control and safety managers, the next step is to review where current finish callouts are ambiguous, where inspection methods vary, and where historical rework clusters around a small number of surface-related features. That review often reveals quick wins: clearer engineering notes, tighter metrology discipline, better tool-life monitoring, and stronger supplier alignment.
In aerospace, lower rework is rarely the result of stricter language alone. It comes from measurable engineering truth applied consistently. When precision machining surface finish standards are built around function, process data, and verification discipline, organizations gain more than compliance. They gain reliability, predictability, and trust across the entire production chain.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























