
Aerospace CNC Turning Factory and First Article Risks
Publication Date
author
Choosing an aerospace cnc turning factory is never just about price or capacity—it is about controlling first article risks before they become quality escapes, compliance failures, or safety liabilities. For quality and safety leaders, the real question is whether a supplier can prove dimensional stability, process discipline, and traceable inspection data from the very first part.
In aerospace programs, the first article is not a paperwork milestone. It is the earliest hard evidence that a process can repeatedly produce parts within tolerance, with documented control over material, tooling, inspection, and change history. A weak first article can trigger delayed approvals, nonconforming product reports, supplier corrective actions, and downstream assembly risk that may take 2 to 12 weeks to unwind.
For quality managers and safety officers, supplier selection therefore starts with a more technical question: can the aerospace cnc turning factory demonstrate stable turning performance on demanding alloys, maintain inspection traceability lot by lot, and detect process drift before it creates an escape? In a data-driven sourcing environment, the answer should come from measurable controls rather than marketing claims.
Why First Article Risk Matters in Aerospace CNC Turning
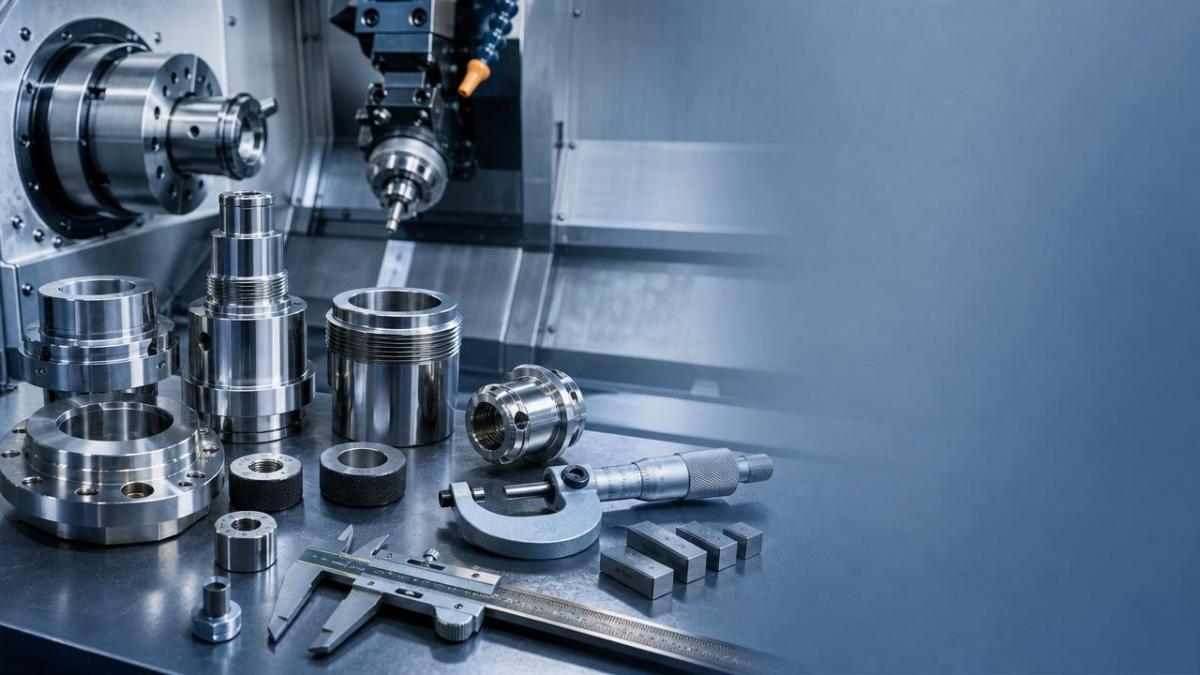
A first article inspection, often linked to AS9102 workflows, validates more than a single finished dimension. It checks whether the manufacturing route, machine setup, cutting parameters, workholding, inspection method, and documentation chain all align with drawing intent. In an aerospace cnc turning factory, this matters because turned parts often include tight concentricity, runout, surface finish, thread integrity, and material traceability requirements that are safety-relevant.
Even a simple shaft, sleeve, or fitting can contain 8 to 20 critical characteristics. If only 1 or 2 are unstable during first article approval, the supplier may still ship visually acceptable parts that later fail in assembly, leak tests, fatigue service, or final audit review. For organizations managing regulated supply chains, that is not only a quality issue but also a compliance exposure.
Typical First Article Failure Modes
The most common problems are rarely dramatic machine crashes. More often, they are subtle process weaknesses hidden behind a passing dimensional report. Safety and quality teams should screen for these recurrent failure patterns before supplier approval:
- Dimensional variation between the first 3 to 5 pieces and the next 20 pieces
- Tool wear compensation applied without controlled revision records
- Mismatch between ballooned drawing features and inspection reports
- Unclear gage calibration status or incomplete measurement system records
- Material heat lot data separated from part serial or batch identification
- Surface integrity issues such as burrs, chatter, or smeared threads on difficult alloys
These issues become more severe when the turned part is used in hydraulic, fuel, flight-control, actuator, sensor housing, or UAV propulsion systems, where dimensional deviation of even ±0.01 mm to ±0.03 mm can influence fit, preload, sealing, or vibration behavior.
What Quality and Safety Teams Should Verify Early
Before approving a new aerospace cnc turning factory, it is useful to separate commercial questions from process-critical questions. The table below highlights the difference between surface-level supplier claims and deeper indicators of first article readiness.
The key conclusion is simple: first article risk is usually visible before the first shipment if the buyer asks the right technical questions. The best aerospace cnc turning factory does not just send a clean report; it shows how that report was produced, verified, and protected from undocumented change.
How to Assess an Aerospace CNC Turning Factory Beyond Capacity Claims
A supplier may have modern CNC lathes, attractive lead times, and competitive pricing, yet still struggle with aerospace risk control. For quality and safety functions, audit depth matters more than brochure depth. A practical assessment should review four layers: machine capability, process control, inspection system, and engineering response speed.
1. Machine and Process Capability
Ask what the factory routinely turns, not just what it can quote. There is a major difference between producing general industrial bushings and repeatedly machining aerospace stainless, titanium, Inconel, or aluminum parts with thin-wall features and critical runout. On complex parts, thermal growth, tool pressure, and chucking distortion can shift a feature from nominal to out-of-spec within 15 to 30 pieces.
A disciplined aerospace cnc turning factory should be able to explain how it controls cutting data, insert life, coolant strategy, and first-off approval. If spindle warm-up, tool life offset, and setup verification are not formalized, first article acceptance may not predict production stability.
Practical audit checkpoints
- Verify whether first-off approval is documented before batch production starts.
- Check whether critical dimensions are measured every 5, 10, or 20 pieces depending on risk level.
- Review how tool wear limits are defined for key features such as diameters, grooves, and threads.
- Confirm whether setup changes trigger reinspection and revised process notes.
2. Inspection and Measurement System Maturity
Inspection quality is not determined by owning a CMM alone. The real question is whether the factory uses the right measurement method for each characteristic and can prove repeatability. A turned aerospace part may require micrometers, bore gages, thread gages, profilometers, roundness checks, and CMM verification in a layered plan rather than a single end-of-line check.
For first article approval, pay special attention to measurement system consistency. If two inspectors can produce different values on the same feature, the reported conformity has limited value. In practical terms, buyers should expect controlled calibration intervals, clear gage identification, and defined methods for borderline results.
The table below can be used as a fast qualification tool when comparing candidate suppliers.
When a factory meets the preferred column consistently, first article approval becomes a stronger predictor of production reliability. That reduces the chance that quality escapes are discovered only after plating, assembly, or customer receipt, where correction cost can rise by a factor of 3 to 10.
Key Risk Controls Before First Article Approval
The safest procurement path is to define first article expectations before the first chip is cut. Many supplier problems start because the drawing is clear, but the control plan is not. Quality and safety teams can reduce this gap by aligning on a short list of mandatory controls during quotation review or technical kickoff.
Pre-production controls that matter most
- Confirm critical-to-quality features, such as sealing diameters, perpendicularity, runout, and thread class.
- Define whether first article requires 1 part, 3 parts, or a representative setup run.
- Agree on raw material condition, certificate format, and heat-lot linkage requirements.
- State whether special processes, deburring criteria, and surface finish acceptance need photo standards.
- Clarify packaging protection for machined surfaces, especially if cosmetic damage may hide edge defects.
These steps are particularly important in cross-border programs, where time zone delays can add 24 to 72 hours to each clarification loop. A data-first aerospace cnc turning factory will welcome this level of definition because it reduces assumptions and protects both parties during approval.
Common sourcing mistakes that increase first article risk
One frequent mistake is selecting a supplier based on machine count rather than demonstrated process window. Another is approving a first article based only on dimensional pass/fail without reviewing how the data was collected. A third is allowing undocumented substitutions, such as alternative inserts, revised clamping, or changed inspection sequence, during the first production run.
For safety-related parts, avoid compressing approval time by skipping layered checks. Saving 3 days at first article can cost 3 weeks later if the lot requires containment, rework, or customer notification. Stable launch discipline is usually faster than reactive recovery.
A practical 5-step approval model
- Drawing and specification review with characteristic prioritization.
- Process route confirmation covering machine, tools, workholding, and inspection plan.
- First-off verification and documented setup release.
- First article package submission with dimensional and traceability evidence.
- Controlled pilot batch review before full release.
This model helps turn first article from a one-time event into a staged risk reduction process. For aerospace supply chains, that distinction matters because a conforming part is not the same as a controlled process.
What a High-Confidence Supplier Relationship Looks Like
The best aerospace cnc turning factory is not necessarily the one with the lowest quote or shortest nominal lead time. It is the one that can show disciplined escalation, transparent data, and repeatable behavior under engineering change. In practice, high-confidence suppliers share bad news early, isolate suspect inventory quickly, and support root-cause closure with evidence rather than opinion.
Signals of long-term reliability
Look for response patterns over at least 2 to 3 sourcing interactions. Does the supplier return technical questions with measured answers? Can it explain why a tolerance is routine, challenging, or high risk? Does it propose additional inspection for a feature that may drift after 50 pieces? These behaviors show engineering maturity that directly supports quality and safety outcomes.
This is where a data-centered approach aligns with TSV’s broader hard-tech philosophy: parameters matter more than adjectives. If a supplier can define inspection frequency, dimensional thresholds, containment timing, and revision control discipline, buyers gain a more reliable basis for supplier qualification and internal risk review.
Questions worth asking before final supplier approval
- Which 5 dimensions or features on this part do you consider most likely to drift, and how will you monitor them?
- What is your standard turnaround for nonconformance containment: 24 hours, 48 hours, or longer?
- How do you link material certificates, part lots, and inspection records during shipment?
- What triggers a repeat first article after tooling, setup, or revision change?
- Can you provide sample documentation showing in-process checks, not just final results?
These questions help quality managers move beyond generic RFQ comparison and toward risk-based sourcing. For aerospace programs, that shift can protect schedule, audit readiness, and field safety at the same time.
Selecting an aerospace cnc turning factory should be treated as a process control decision, not a commodity purchase. First article risk is where hidden weaknesses become visible: tolerance instability, weak traceability, unclear inspection methods, and unmanaged change. Suppliers that can define controls in measurable terms are better positioned to support compliant, safe, and repeatable aerospace production.
If your team is qualifying new machining sources, reviewing first article readiness, or tightening supplier risk criteria, now is the right time to compare process evidence rather than marketing language. Contact us to discuss your sourcing scenario, request a tailored evaluation framework, or learn more solutions for qualifying a high-confidence aerospace cnc turning factory.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























