
5-Axis CNC Machining Center Specs That Change Real Output
Publication Date
author
For procurement teams, comparing a machine by brochure claims alone is a costly mistake. The right 5-axis CNC machining center specifications directly shape throughput, tolerance stability, surface finish, and long-term operating cost.
This guide cuts through vague marketing language to highlight the metrics that truly affect output, helping buyers evaluate equipment with engineering clarity and sourcing confidence.
What Procurement Teams Are Really Searching For
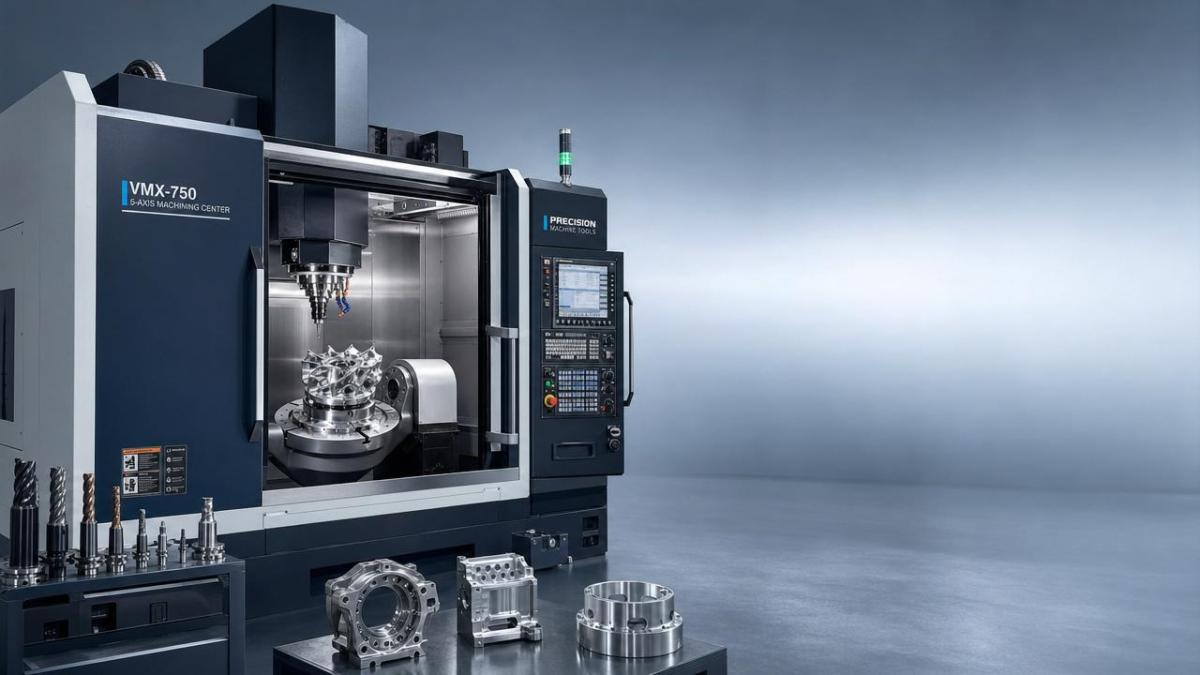
When buyers search for 5-axis CNC machining center specifications, they are rarely looking for a generic feature list. They want to know which specs change delivered part quality, cycle time, uptime, and total ownership cost.
The core search intent is commercial and technical at the same time. Procurement needs a reliable way to compare machines, screen suppliers, reduce qualification risk, and avoid expensive mistakes hidden behind polished brochures.
For this audience, the most important questions are practical. Which specifications actually improve output? Which numbers are easy to manipulate? Which tests should be requested before issuing a purchase order?
That means the article should focus less on basic 5-axis definitions and more on evaluation logic. Buyers need measurable criteria, not promotional language, especially when the machine may support aerospace, medical, tooling, or high-mix precision production.
Start With the Specs That Directly Change Output
Not all published specifications have equal value. Some strongly affect production reality, while others are too abstract to support a sourcing decision. Procurement should prioritize the parameters that influence speed, stability, accuracy, and utilization.
The most decision-critical 5-axis CNC machining center specifications usually fall into six groups: structural rigidity, axis kinematics, spindle performance, positioning accuracy, thermal stability, and automation readiness.
If a machine looks strong on paper but weak in one of these six areas, output often suffers. The result can be slower cycle times, more scrap, unstable tolerances, frequent intervention, or hidden maintenance costs.
Rigidity and Machine Structure Matter More Than Cosmetic Speed Claims
Procurement teams often notice spindle rpm and rapid traverse first because they are easy to compare. In actual production, however, machine structure and rigidity usually have a greater impact on real metal removal performance.
Ask how the machine base is built, what material is used, and how vibration is controlled. A rigid casting, stable column design, and strong trunnion or swivel head architecture support better finishes and more predictable tolerances.
This is especially important for titanium, stainless steel, Inconel, hardened steel, and complex aerospace alloys. High advertised cutting speed means little if chatter, deflection, and thermal drift force operators to reduce feed or add finishing passes.
Useful procurement questions include static stiffness data, vibration damping measures, maximum table load under dynamic movement, and evidence from heavy-cut benchmark tests rather than no-load demonstration videos.
Axis Configuration and Kinematics Influence More Than Reach
One of the most misunderstood 5-axis CNC machining center specifications is axis architecture. A machine may be head-head, table-table, or head-table, and each configuration changes access, stability, work envelope, and collision risk.
Procurement should not evaluate travel dimensions in isolation. The usable working volume under simultaneous 5-axis motion is what matters, especially for parts with deep cavities, angled features, or complex fixture requirements.
Ask for the actual interference map, B-axis and C-axis limits, rotary acceleration, and whether the machine can maintain stable contouring near axis reversals. Weak rotary behavior often reduces surface quality on demanding geometries.
A large nominal envelope can still deliver disappointing output if fixture space is constrained or tool access is poor. In sourcing reviews, insist on sample parts similar to your geometry, not only generic demonstration components.
Spindle Specs Should Be Read as a System, Not a Single Number
Spindle rpm alone does not determine machining capability. Procurement should evaluate spindle power curve, continuous torque, peak torque, bearing design, taper type, and thermal control as an integrated performance system.
For aluminum and high-speed finishing, higher rpm may be valuable. For steel, titanium, and deep roughing, torque at usable speed ranges often matters more than maximum rpm printed on a brochure.
Ask whether the supplier is quoting peak power or continuous power. Peak values can sound impressive but may not reflect what the machine sustains over long production runs. That difference directly affects throughput and cycle reliability.
Also review tool interface standards such as HSK or BT, pull-stud quality expectations, and spindle warm-up requirements. These details affect repeatability, tool life, and maintenance intervals more than many buyers initially expect.
Accuracy, Repeatability, and Volumetric Performance Need Context
Many brochures list positioning accuracy and repeatability, but procurement should always ask how those values were measured. A single axis test under ideal conditions is not the same as volumetric accuracy during real 5-axis interpolation.
For precision work, request standards-based measurement details, ball bar data, laser calibration records, and if possible, volumetric compensation capability. These reveal whether the machine can maintain geometry across the full work zone.
The distinction between positioning accuracy and process capability is critical. A machine may return to a point consistently but still struggle to hold part features under load, thermal variation, and simultaneous multi-axis motion.
If your applications involve aerospace brackets, orthopedic components, turbine parts, or mold surfaces, ask for proof tied to actual contouring performance, not only static positioning numbers measured in ideal lab conditions.
Thermal Stability Is Often the Hidden Divider Between Good and Great Output
Thermal behavior is one of the most important and least understood 5-axis CNC machining center specifications. Over a long shift, heat from the spindle, drives, coolant, and ambient environment can shift dimensions significantly.
Machines intended for serious precision work should include thermal compensation strategies, spindle cooling, stable structural design, and ideally some evidence of drift performance over time rather than only startup accuracy.
Procurement should ask how quickly the machine reaches thermal equilibrium, what compensation systems are built in, and how dimensional stability changes during continuous production, not just during short demonstration cuts.
This matters because real factories do not run under laboratory conditions. If the machine drifts after lunch, after a tool change sequence, or during extended roughing, output quality and inspection yield will suffer.
Tool Change, Chip Management, and Automation Readiness Drive Utilization
Procurement teams focused only on cutting specs often miss the factors that shape machine utilization. In many plants, output is limited less by spindle capability than by setup delays, poor chip evacuation, and manual handling bottlenecks.
Review automatic tool changer capacity, tool-to-tool time, chip-to-chip time, broken-tool detection options, probing support, pallet systems, and compatibility with robotic loading or unattended operation.
Chip control is especially important in deep-pocket or high-volume work. Weak coolant delivery, poor chip flushing, or ineffective conveyor design can increase intervention frequency, surface defects, and spindle load variability.
For procurement, this is where business value becomes visible. A machine with slightly lower headline speed but stronger automation and reliability can produce more sellable parts per shift than a faster but interruption-prone alternative.
Control System Capability Affects Programming Efficiency and Risk
The machine control should be evaluated as a production asset, not just a user interface. For 5-axis work, the control influences post-processing, interpolation quality, smoothing, collision prevention, and operator learning curve.
Ask which control platform is used, what simultaneous 5-axis functions are standard, and whether advanced features require expensive software unlocks after purchase. Hidden software costs can distort the true sourcing comparison.
Procurement should also involve manufacturing engineers early. A machine with poor CAM compatibility, weak support for look-ahead processing, or limited data capture may increase programming time and reduce process confidence.
If your organization is building a connected factory environment, verify data export capability, alarm logging, remote diagnostics, and integration with MES or maintenance systems. These are no longer optional in high-accountability production.
Serviceability and Spare Parts Access Are Core Specifications in Practice
Official spec sheets rarely present service risk clearly, yet downtime cost can exceed any price difference between machines. Procurement should assess maintainability with the same rigor used for spindle or accuracy metrics.
Key questions include regional service coverage, spare parts lead times, preventive maintenance intervals, remote troubleshooting support, and whether critical components are proprietary or widely supportable in your region.
Ask for installed base references in similar industries, mean response times, and examples of common failure modes. A strong machine with weak service backing may create serious operational exposure after the warranty period ends.
For buyers managing multi-site sourcing, standardizing around serviceable platforms can reduce training burden, spare inventory complexity, and recovery time during breakdown events.
How to Compare 5-Axis CNC Machining Center Specifications Without Getting Misled
A disciplined sourcing process is the best defense against inflated claims. First, convert your application into a weighted evaluation sheet covering materials, part sizes, tolerance class, finish requirements, batch profile, and unattended production needs.
Second, ask every supplier to respond using the same technical template. This makes it easier to compare continuous spindle power, actual dynamic accuracy, thermal measures, tool capacity, and automation options on equal terms.
Third, request proof. That may include sample cuts, cycle time studies, calibration records, customer references, and documented results on similar parts. Procurement should treat unsupported claims as unverified, not assumed fact.
Finally, calculate value at the part-output level. The right question is not only what the machine costs, but how many conforming parts it can produce per shift, per operator hour, and per maintenance cycle.
Red Flags in Brochure Language
Some warning signs appear repeatedly in machine sourcing. Be cautious when a supplier promotes maximum values without clarifying test conditions, quotes peak power only, or avoids discussing thermal drift and volumetric accuracy.
Other red flags include unusually broad tolerance claims without measurement method, strong demo finishes on soft materials only, and vague statements such as “high rigidity” or “excellent dynamic response” without numbers.
Procurement should also watch for optional features presented as standard capability. A machine may appear competitively priced until probing, cooling systems, software modules, or pallet functions are added back into the real configuration.
In hard-tech procurement, ambiguity is risk. The more expensive the machine and the tighter the quality requirement, the less room there is for marketing language to replace engineering evidence.
What a Good Procurement Decision Looks Like
A strong sourcing decision aligns machine specifications with the output economics of your actual parts. That means choosing the platform that best supports process stability, acceptable cycle time, quality yield, and maintainable uptime.
For some buyers, that will mean prioritizing high-speed contouring and automation for aluminum structures. For others, it will mean torque, rigidity, and thermal control for difficult alloys and long-run precision work.
The best procurement teams do not ask which machine has the longest feature list. They ask which 5-axis CNC machining center specifications most directly improve delivered output under their real production constraints.
That shift in perspective is where sourcing quality improves. It shortens qualification cycles, reduces unpleasant surprises after installation, and builds a much stronger case for investment approval.
Conclusion
In 5-axis machine procurement, the specifications that change real output are rarely the most advertised ones. Structural rigidity, kinematics, sustained spindle performance, volumetric accuracy, thermal stability, automation readiness, and service support matter most.
For procurement professionals, the goal is not to buy the most impressive brochure. It is to secure a machine that produces conforming parts predictably, efficiently, and at a sustainable operating cost over years of use.
If you evaluate 5-axis CNC machining center specifications through that lens, you will make better comparisons, ask sharper supplier questions, and reduce both technical and commercial risk.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























