
Machine vision lens specifications that change inspection results
Publication Date
author
Machine vision lens specifications are not minor details—they directly shape measurement accuracy, defect detection, and overall inspection reliability. For technical evaluators comparing imaging systems, understanding how resolution, distortion, working distance, and sensor matching interact is essential to reducing false rejects, missed defects, and costly validation cycles. This article breaks down the lens parameters that truly change inspection results.
Why a checklist approach works better than a feature list
When teams review machine vision lens specifications, they often receive brochures full of focal length labels, megapixel claims, and marketing language that does not translate into pass/fail inspection performance. A checklist approach is more useful because it forces evaluators to connect every parameter to a production outcome: measurement uncertainty, defect contrast, depth tolerance, cycle time, and maintenance burden.
For TechStat Vanguard’s engineering-first audience, the lens should never be evaluated in isolation. It is one part of an imaging chain that includes sensor size, pixel pitch, illumination geometry, object motion, environmental vibration, and software tolerances. The right machine vision lens specifications reduce validation risk because they make the imaging chain predictable, repeatable, and measurable.
Start here: the first six checks before comparing models
- Define the smallest feature that must be detected or measured. A scratch, edge burr, printed code, or solder void sets the true optical requirement.
- Confirm the sensor format and pixel size. Many machine vision lens specifications look acceptable until sensor matching reveals corner blur or reduced effective resolution.
- Calculate required field of view and working distance together. Evaluating focal length without the real mechanical envelope creates integration problems later.
- Separate detection from metrology tasks. A lens that is fine for presence/absence inspection may fail dimensional measurement because distortion is too high.
- Check lighting and aperture constraints early. Resolution on paper can collapse if the lens must be stopped down to manage depth of field, forcing longer exposure.
- Review environmental factors such as temperature drift, vibration, dust, and washdown exposure. Stable specifications matter more than peak specifications.
Core machine vision lens specifications that most strongly change inspection results
1. Resolution and MTF: the difference between visible detail and reliable detail
Resolution is usually the first item people check, but technical evaluators should look beyond a simple megapixel label. A lens may claim support for a high-resolution sensor while still delivering weak contrast at the spatial frequencies that matter for your feature size. This is where MTF, or modulation transfer function, becomes critical. MTF indicates how well the lens preserves contrast at fine detail levels.
Inspection result impact: poor MTF causes fuzzy edge transitions, unstable sub-pixel fitting, and reduced confidence in OCR, code reading, and defect segmentation. In practice, this means more false rejects on borderline parts and more missed defects on low-contrast surfaces.
Judgment standard: ask for MTF data across center and edge image zones, not only nominal sensor compatibility. If the application depends on dimensional measurement at the edge of the frame, edge MTF matters as much as center sharpness.
2. Distortion: the hidden variable in measurement accuracy
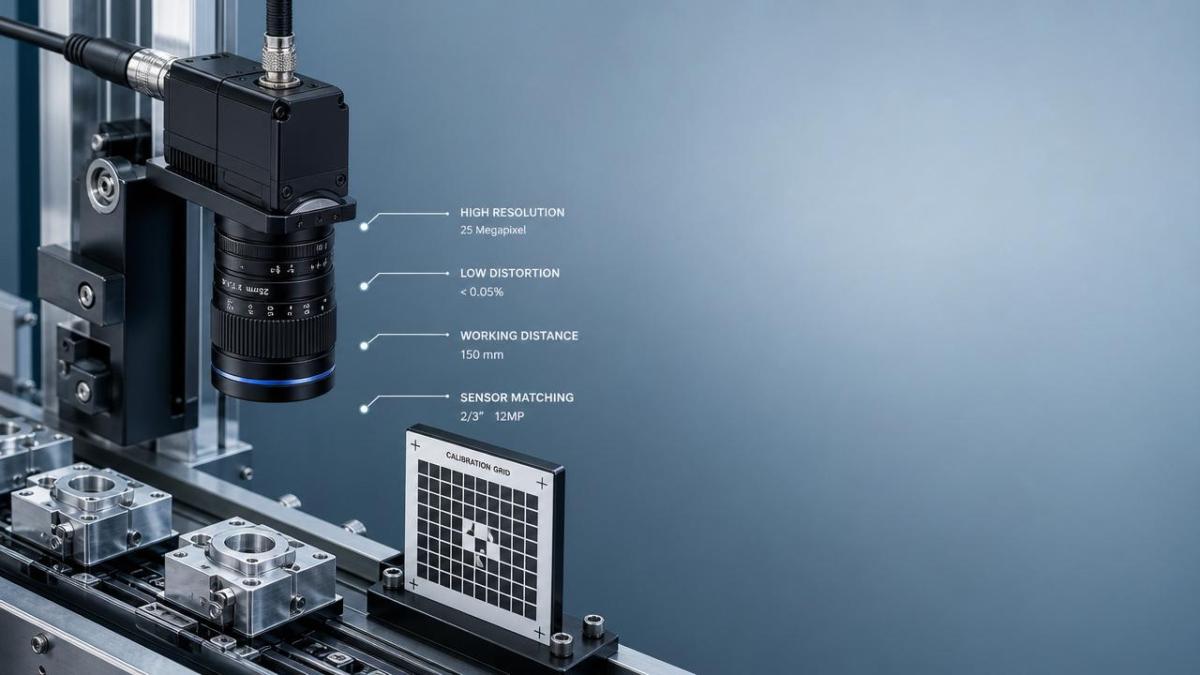
Among all machine vision lens specifications, distortion is one of the most underestimated. Barrel or pincushion distortion may be acceptable in basic detection, but it becomes a direct source of measurement error when coordinates must map accurately across the field. Even if software calibration compensates for some distortion, heavy correction can increase complexity and sensitivity to setup drift.
Inspection result impact: distorted geometry changes measured distances, especially away from the optical center. This matters in gauging holes, lead pitch, connector position, seal bead width, and flatness references. For precision applications, low-distortion or telecentric optics are often worth the higher initial cost because they reduce downstream compensation work.
3. Working distance and field of view: fit the mechanics before the optics fail the project
A common evaluation mistake is selecting by focal length alone. The actual machine vision lens specifications must support the required field of view at the real working distance allowed by guards, conveyors, robot tooling, and safety covers. A lens that performs well in the lab may become unusable when there is no physical room for the camera head or lighting stack.
Inspection result impact: if the field of view is too tight, the part does not fit; if too wide, pixel density drops and small defects disappear. If the working distance is forced too short, perspective effects, lighting shadows, and contamination risk usually increase.
4. Sensor matching: image circle, pixel size, and corner performance
Machine vision lens specifications must always be read against the sensor. The lens image circle must fully cover the sensor, but coverage alone is not enough. Pixel size determines how demanding the lens is. Smaller pixels reveal optical weaknesses faster, especially in the corners. A lens that is “compatible” with the sensor format may still leave effective resolution unused.
Judgment standard: confirm sensor format, pixel pitch, and target magnification together. Request sample images of calibrated grids or actual parts, captured at the intended aperture and working distance, not idealized bench settings.
5. Aperture and depth of field: balance sharpness, light, and speed
Aperture affects depth of field, diffraction, and light throughput. Stopping down increases usable depth, which helps when parts vary in height or tilt. However, too small an aperture can introduce diffraction softening, reducing fine detail. It also demands stronger illumination or longer exposure, which can create motion blur in high-speed lines.
Inspection result impact: the wrong aperture strategy turns a theoretically good lens into a practical failure. For moving parts, exposure time often becomes the limiting factor, so the best lens choice is the one that keeps enough sharpness without forcing impractical lighting power.
6. Telecentricity: essential for metrology, optional for many detection tasks
Not every application needs a telecentric lens, but when object height variation changes apparent size, conventional optics can undermine measurement credibility. Telecentric machine vision lens specifications matter in semiconductor packaging, precision machining, medical components, battery tabs, and other tasks where dimensional repeatability is more important than low cost.
Inspection result impact: telecentric optics suppress perspective error and stabilize magnification over depth changes. If parts shift vertically but the measurement must remain constant, this is a key screening criterion.
7. Chromatic correction and flare resistance: often ignored until contrast collapses
Multi-material assemblies, reflective metals, glossy labels, and mixed-spectrum lighting expose another weakness in machine vision lens specifications: chromatic aberration and flare control. Color fringing reduces edge precision, and flare lowers local contrast. In defect inspection, contrast loss can be more damaging than slight blur because segmentation thresholds become unstable.
Quick evaluation table for technical reviewers
How priorities change by inspection scenario
Technical evaluators should not rank all machine vision lens specifications equally. Priority changes with the task.
- Dimensional metrology: prioritize low distortion, telecentricity, stable magnification, and calibration repeatability.
- Surface defect inspection: prioritize MTF, flare resistance, contrast preservation, and compatibility with structured or dark-field lighting.
- High-speed presence/absence checks: prioritize aperture efficiency, exposure margin, vibration tolerance, and practical integration cost.
- Code reading and OCR: prioritize center-to-edge sharpness, low field curvature, and stable focus across part height variation.
- Robotic guidance: prioritize working distance flexibility, distortion control, and robustness to changing object position.
Commonly missed risk items that distort evaluation results
Several risks repeatedly appear in supplier comparisons. First, test images are often captured under ideal illumination with static targets, while production lines introduce motion, contamination, and variable reflectivity. Second, teams compare machine vision lens specifications without defining acceptance thresholds for the full system. Third, software calibration is treated as a cure-all, even though unstable mechanics and temperature drift can erode calibration validity. Fourth, evaluators may overlook mount precision and locking mechanisms, which affects focus stability over time.
Another common issue is buying for “future resolution.” Selecting a lens only because it may support a larger future sensor can be wasteful if current lighting, compute throughput, and process tolerances do not justify it. Better inspection results come from balanced engineering, not isolated optical overdesign.
Execution checklist before final approval
- Document the smallest defect size, measurement tolerance, line speed, and allowable false reject rate.
- Lock sensor model, pixel size, and illumination method before final lens ranking.
- Request production-like sample images at actual working distance, aperture, and exposure time.
- Verify edge performance, not only image center performance.
- Run repeatability tests across temperature and shift-to-shift startup conditions.
- Check whether calibration residuals remain acceptable after maintenance or lens replacement.
- Compare total validation effort, not just unit price, because weak optics often increase engineering hours.
FAQ for teams reviewing machine vision lens specifications
Is a higher megapixel lens always better?
No. If MTF, lighting, and motion control are not matched, higher pixel counts may add cost without improving detection reliability.
Can software calibration fix distortion completely?
Calibration helps, but it does not eliminate all practical issues. Heavy correction increases dependence on setup stability and may not fully protect metrology accuracy under drift.
When is a telecentric lens justified?
When dimensional repeatability is critical and object height variation would otherwise change apparent size, telecentric optics are often justified despite higher cost.
Practical next step for specification review
The most effective way to evaluate machine vision lens specifications is to convert them into a decision sheet tied to inspection outcomes. Before moving forward with a supplier or system integrator, prepare five items: target defect size, tolerance requirements, sensor format and pixel size, mechanical working distance limits, and real production lighting conditions. Then ask for evidence under those exact conditions, including edge sharpness, distortion data, repeatability results, and calibration behavior.
If your team needs to confirm parameter suitability, integration risk, validation timeline, budget trade-offs, or supplier credibility, start the conversation with measurable thresholds rather than general performance claims. That approach aligns with TSV’s core principle: parameters do not lie, and the right machine vision lens specifications will show their value in inspection results long before they appear in marketing language.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























