
Why Surface Finish Can Ruin Precision Aerospace Components
Publication Date
author
In aerospace manufacturing, a flawless surface is never just cosmetic—it directly affects fatigue life, sealing performance, and dimensional stability. For quality and safety teams, overlooking surface finish can turn qualified parts into hidden failure risks. This is why precision machining for aerospace components must go beyond tolerance control and address surface integrity as a critical engineering parameter.
Why quality and safety teams should use a checklist first
For inspectors, supplier quality engineers, and safety managers, surface finish failures are dangerous because they often hide behind otherwise acceptable dimensions. A bore can measure within tolerance, a flange can pass coordinate inspection, and a structural bracket can look visually clean—yet the part may still carry machining marks, smeared material, micro-tears, or residual stress patterns that shorten service life.
A checklist-based review is the most practical way to control that risk. It helps teams verify not only roughness values such as Ra or Rz, but also the broader surface integrity package: lay direction, waviness, burr condition, recast layers, contamination, and post-process changes after anodizing, shot peening, grinding, or coating. In precision machining for aerospace components, this structured review is often the difference between a part that passes receiving inspection and a part that performs safely in flight.
First-pass checklist: what to confirm before approving any aerospace part
Before digging into detailed measurement data, quality teams should confirm the following high-priority items. These checks create a fast screening process for machined housings, brackets, valve bodies, turbine-adjacent parts, UAV structures, and sealing interfaces.
- Verify whether the drawing defines only roughness, or also includes waviness, lay direction, edge break, and no-burr requirements. Many failures begin with incomplete specification language.
- Confirm the functional role of the surface: fatigue-critical, sealing-critical, sliding contact, aerodynamic, adhesive bonding, or cosmetic secondary face. Acceptance criteria should match function.
- Check whether the measurement method matches the geometry. Stylus profilometers may miss small radii, deep grooves, or internal channels where optical methods or replicas are more reliable.
- Review whether machining, grinding, polishing, blasting, coating, or heat treatment changed the surface after the last qualified inspection step.
- Confirm that the supplier’s process capability is linked to the actual material grade. Titanium, Inconel, aluminum-lithium alloys, and carbon steel do not respond to cutting in the same way.
- Check whether residual burrs, feather edges, smeared material, or embedded abrasive particles are possible at intersections, slots, ports, and threads.
- Require traceable records showing tool condition, coolant control, inspection sampling frequency, and rework history for each batch or serialized part.
This first-pass list is especially useful when evaluating vendors that claim strong precision machining for aerospace components but provide limited data on actual surface integrity performance.
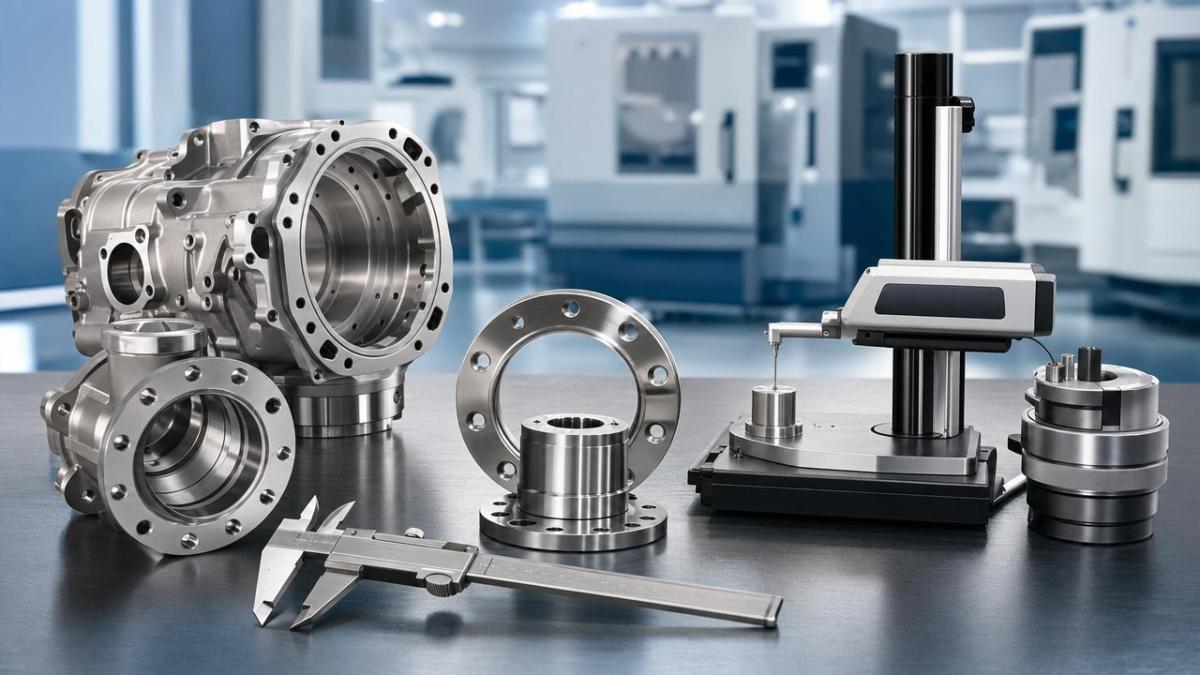
Core surface finish checks that directly affect airworthiness risk
1) Roughness values are necessary, but never sufficient
Ra is the most common drawing callout, but relying on Ra alone can be misleading. Two surfaces can share the same average roughness while having very different peak spacing, valley depth, and crack initiation behavior. Safety teams should ask whether Rz, Rt, or bearing area parameters are also relevant. On sealing faces, valley depth may matter more than average roughness. On fatigue-loaded parts, sharp peaks can become initiation points even when Ra appears acceptable.
2) Lay direction must match function
The direction of machining marks can either support or undermine performance. Circular lay on sealing surfaces may trap leakage paths. Longitudinal tool marks on highly stressed members may accelerate crack growth depending on load direction. On bearing seats or actuator components, incorrect lay can change friction behavior and wear stability. In precision machining for aerospace components, this is a common oversight when dimensional compliance is treated as the only release criterion.
3) Burrs and edge condition are safety items, not cosmetic details
Small burrs can break loose and contaminate hydraulic circuits, fuel systems, or sensor cavities. Sharp edges can damage seals during assembly or create local stress concentration. Inspectors should verify whether the edge break requirement is defined numerically and whether deburring methods leave rollover, tearing, or dimensional loss. This matters especially on ports, threads, intersecting holes, and thin-wall aluminum or titanium features.
4) Thermal damage and smeared metal can hide beneath a “smooth” appearance
Grinding burn, white layer formation, and metal smearing may create surfaces that look refined but perform poorly under cyclic load. These conditions can alter hardness, create tensile residual stress, and reduce fatigue strength. For critical parts, a smooth appearance should never replace metallurgical verification when the process route includes aggressive finishing or difficult-to-machine alloys.
5) Surface condition after coating or anodizing must be rechecked
A surface that passed pre-treatment inspection may shift after anodizing, plating, conversion coating, thermal spray, or paint masking. Coating thickness, porosity, adhesion, and local buildup can affect fit, sealing, and mating force. For quality personnel, the practical rule is simple: if the final function depends on the final surface, the final surface must be measured after the final relevant process.
How to judge surface finish by component type
Not every aerospace feature should be inspected the same way. A useful quality plan links the surface requirement to the actual service condition.
This component-based approach helps teams prioritize inspection effort instead of applying the same acceptance logic to every machined feature.
Common blind spots in precision machining for aerospace components
Many nonconformities are not caused by missing instruments, but by incomplete review habits. The following blind spots repeatedly appear in supplier audits and internal investigations:
- Accepting a generic “surface finish OK” statement without parameter values, measurement location, cutoff setting, and instrument type.
- Inspecting only easy-to-access flat surfaces while ignoring radii, undercuts, groove roots, and internal transitions where cracks tend to start.
- Treating reworked or hand-polished areas as equivalent to original machine-generated surfaces without additional validation.
- Failing to account for material pullout in difficult alloys, especially in drilled holes or interrupted cuts.
- Using a sampling plan that is too light for low-volume, high-criticality aerospace production.
- Separating dimensional inspection from process review, which hides tool wear trends and recurring chatter signatures.
- Ignoring packaging and handling damage after final inspection; a correct finish can be ruined by contact, rubbing, or poor protection in transit.
Execution guide: how to strengthen inspection and supplier control
If your organization wants better control over precision machining for aerospace components, the most effective improvements are procedural rather than cosmetic. Start with process discipline and evidence quality.
Build drawing clarity
Review whether engineering drawings distinguish critical-to-function surfaces from general machining surfaces. Add clear notes for roughness, lay, forbidden defects, edge conditions, and post-coating acceptance where needed. Vague callouts invite inconsistent interpretation across suppliers.
Link inspection plans to process steps
Final inspection should not be the only control point. Insert verification after rough machining, after finishing, and after any surface-altering special process. This helps isolate when a defect was introduced and reduces the cost of scrap or rework.
Use risk-based sampling for critical features
For fatigue-critical or sealing-critical surfaces, use tighter sampling or 100% verification where justified. Surface failures are often low-visibility but high-consequence, which means a standard volume-based sampling plan may not be enough.
Audit the supplier’s finishing logic, not only the machine list
A supplier may own advanced 5-axis CNC systems and still struggle with stable surface finish if tool path strategy, insert selection, spindle dynamics, coolant delivery, or deburring discipline are weak. During qualification, ask for actual evidence: capability studies, roughness distribution by material, surface defect examples, and traceability from lot to lot.
Train inspectors to recognize defect signatures
Quality systems improve when people can identify chatter, smear, torn grain, abrasive embedment, and coating overbuild early. Visual standards, comparator images, and defect libraries are practical tools that make inspection more repeatable across shifts and sites.
FAQ for quality and safety decision-makers
Is a low Ra value enough to approve a critical aerospace part?
No. Low Ra alone does not confirm correct lay, absence of burrs, acceptable waviness, or freedom from thermal damage. Approval should reflect total surface integrity, not one number.
When should surface finish be escalated as a safety issue?
Escalate immediately when the feature affects pressure sealing, fatigue life, rotating balance, hydraulic cleanliness, bearing fit, or adhesive bonding. These areas can convert minor-looking defects into major reliability events.
What documents should a supplier provide?
At minimum, request drawing-linked inspection records, measurement method details, process routing, special process certificates where relevant, nonconformance history, and evidence of capability for the specific material and geometry involved.
What to prepare before the next supplier review or internal improvement meeting
To improve outcomes quickly, quality and safety teams should prepare a short but disciplined information package. Include the part families with the highest functional risk, the specific surfaces tied to fatigue or sealing performance, known field or assembly issues, current drawing callouts, and any gaps in measurement method consistency. This enables a focused review instead of a generic discussion about “machining quality.”
For organizations sourcing precision machining for aerospace components, the next conversation with a supplier should not begin with price alone. It should begin with parameters, process windows, inspection evidence, post-process controls, and defect prevention logic. If you need to confirm suitability, lead time, validation scope, or production readiness, prioritize these questions: Which surfaces are function-critical? How are they measured? What changes after finishing or coating? What defect modes have appeared before? What controls prevent recurrence? That is how quality teams turn surface finish from a hidden liability into a managed engineering standard.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























