
Why Medical Device Parts Often Need 5-Axis CNC Instead of 3-Axis
Publication Date
author
When medical device geometries become smaller, more intricate, and less forgiving, 3-axis machining often reaches its limits. This is why 5-axis CNC machining for medical devices is increasingly essential for producing complex contours, tighter tolerances, and cleaner surface finishes in a single setup. For engineers and sourcing teams evaluating process capability, understanding this shift is key to reducing risk, improving consistency, and meeting strict regulatory expectations.
For information-focused buyers, supplier qualification teams, and design engineers, the real question is not whether 5-axis machining sounds advanced. The real question is where 3-axis capability stops delivering measurable process control, and where 5-axis CNC machining for medical devices becomes the lower-risk manufacturing route.
At TSV, the discussion is best framed through engineering fundamentals rather than marketing language. In medical manufacturing, success is often determined by a few decisive variables: tolerance stack-up, surface finish stability, tool access, setup count, burr control, and traceable repeatability across low-to-medium production volumes. Those variables often explain why 5-axis capability is selected for spinal implants, orthopedic components, surgical instruments, endoscopic parts, and precision housings.
Where 3-Axis Machining Reaches Its Limits in Medical Device Production
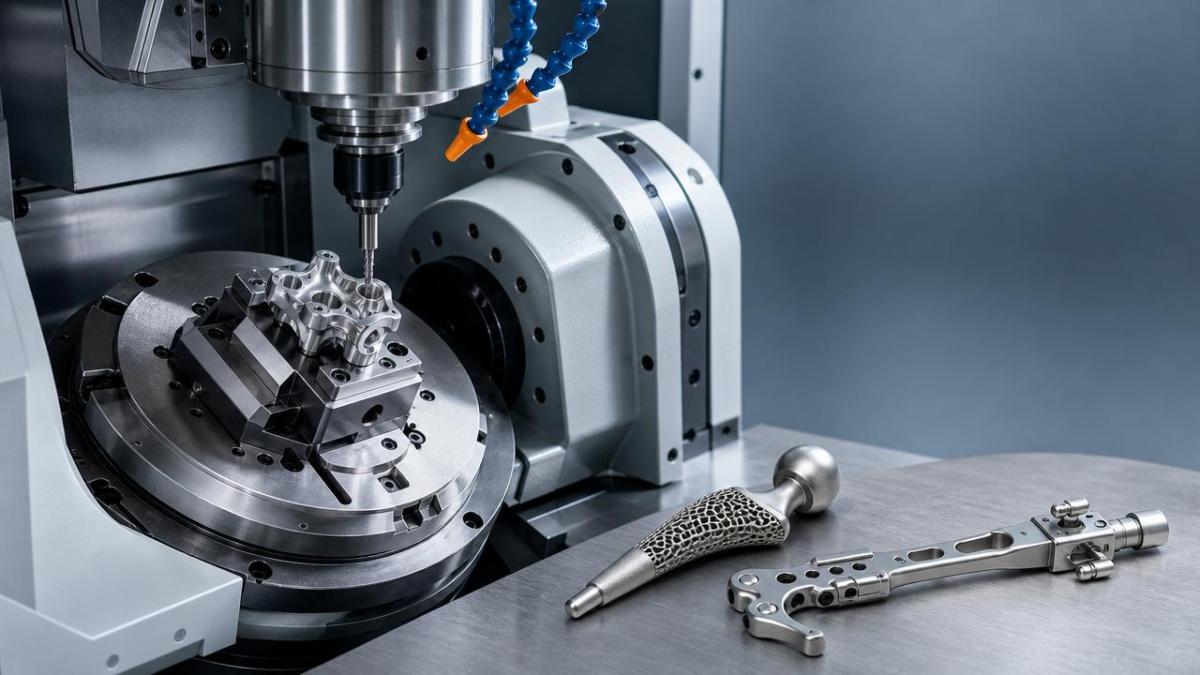
A 3-axis machine moves along X, Y, and Z directions. That is sufficient for many flat or moderately contoured components, especially fixtures, simple blocks, or non-critical external features. However, many medical device parts include undercuts, freeform surfaces, compound angles, and miniature internal features that cannot be reached efficiently from only one spindle orientation.
In practice, 3-axis machining often requires 2 to 6 separate setups for complex parts. Every additional setup increases the probability of positional error, datum drift, handling damage, and inspection burden. For medical parts where tolerances may fall within ±0.005 mm to ±0.02 mm on critical features, setup reduction is not just a productivity benefit. It is a control strategy.
Geometry complexity is the first threshold
Many implantable and surgical components are no longer simple prismatic forms. Bone plates, acetabular cups, spinal cages, and instrument tips often require blended radii, multi-angle pockets, lattice-adjacent finishing, and edge conditions that must remain consistent around the entire part. On 3-axis equipment, these features may require repeated refixturing or custom tooling, increasing cycle variability.
Typical signs that 3-axis is becoming inefficient
- More than 3 setups are needed to complete one part
- Critical surfaces sit on different compound angles
- Tool overhang exceeds stable cutting limits for small-diameter tools
- Manual deburring time exceeds 15% to 20% of total part time
- Inspection failures cluster around repositioned datums
These signs are especially relevant in ISO 13485-aligned manufacturing environments, where process repeatability and documented control matter as much as nominal dimensions. A part that is technically machinable on 3-axis equipment may still be a poor production choice if repeatability drops across 30, 100, or 500 units.
The table below outlines where the practical gap between 3-axis and 5-axis capability becomes significant for medical device applications.
The key conclusion is that 5-axis CNC machining for medical devices is rarely chosen just for speed. It is typically chosen because the geometry, tolerance chain, and finishing requirements make 3-axis production more fragile, less repeatable, or more labor-intensive than acceptable.
Tolerance stack-up becomes a commercial issue
For procurement teams, the setup count also affects cost of quality. A part that needs 4 setups often needs more in-process checks, more fixture verification, and more operator judgment. That can lengthen first-article approval by 1 to 3 days and increase nonconformance risk during ramp-up. In regulated sectors, every extra intervention has documentation implications.
This is why advanced buyers evaluate not only unit price, but also process architecture. A supplier quoting a lower piece price on 3-axis equipment may still create higher total cost if scrap rates rise from 1% to 4%, or if post-machining polishing adds 20 to 40 minutes per part.
Why 5-Axis CNC Machining for Medical Devices Solves the Core Engineering Problems
The value of 5-axis machining lies in its ability to rotate the tool or the part during cutting, enabling more optimal approach angles. In medical applications, that means tighter control over surface finish, wall integrity, edge quality, and dimensional consistency. For intricate titanium or cobalt-chrome parts, this can make the difference between a stable validated process and a marginal one.
Single-setup machining improves repeatability
One of the strongest reasons to adopt 5-axis CNC machining for medical devices is single-setup completion. By machining multiple sides and angles in one clamping cycle, the process reduces re-datum errors and operator handling. For small parts with dimensions under 50 mm, even tiny clamping variation can affect concentricity, true position, or edge break quality.
In many cases, reducing setups from 4 to 1 can shorten cumulative tolerance exposure and simplify in-process inspection. It also helps preserve traceability because fewer manual transitions occur between operations. For medical OEMs and contract manufacturers, that matters during process validation and lot release review.
Better tool orientation protects delicate features
Five-axis motion allows shorter effective tool reach and improved cutter contact. That is especially important when machining thin walls, narrow channels, or sculpted transitions in stainless steel, PEEK, titanium, or implant-grade alloys. A reduction in tool overhang by even 20% to 30% can significantly improve cutting stability and reduce chatter marks.
Practical engineering gains from 5-axis processing
- Fewer setups and less manual repositioning
- More consistent surface finish on freeform contours
- Lower risk of burr formation in hard-to-reach edges
- Improved access for micro tools below 3 mm diameter
- Reduced need for secondary blending and polishing
These gains are not universal for every part. A simple rectangular housing with drilled holes may still be more economical on 3-axis equipment. But once geometry includes organic surfaces, angular undercuts, or deep cavity transitions, 5-axis often becomes the more predictable route.
The next comparison shows how 5-axis capability aligns with common medical device manufacturing objectives.
From a sourcing perspective, the most important takeaway is that 5-axis CNC machining for medical devices improves process robustness. That robustness often translates into fewer corrective actions, more stable validation outcomes, and shorter qualification cycles for complex components.
Which Medical Device Parts Most Commonly Require 5-Axis Capability
Not every medical part requires simultaneous 5-axis motion, but many categories benefit from 5-axis positioning or full 5-axis contouring. The deciding factors are usually geometry complexity, part size, material behavior, and the number of critical surfaces that must remain relationally accurate within one setup.
Common application categories
- Orthopedic implants with curved load-bearing surfaces
- Spinal components with angled pockets and precise edge conditions
- Surgical cutting guides and reusable instruments
- Minimally invasive device housings and articulated parts
- Dental abutments and small precision implant interfaces
For example, a surgical instrument jaw may require parallelism, edge preparation, micro-feature consistency, and smooth exterior blending in a part under 80 mm long. Producing that profile on 3-axis equipment may be possible, but only through multiple fixtures and higher manual finishing input. On 5-axis equipment, the process can often be consolidated while preserving feature relationships.
Materials also affect the 3-axis versus 5-axis decision
Medical materials such as titanium alloys, 17-4 PH stainless steel, cobalt-chrome, and engineering polymers all respond differently to cutting forces and heat. Harder alloys amplify the penalty of poor tool access. The more difficult the material, the more valuable optimized tool orientation becomes. This is particularly true when surface integrity and burr minimization are critical acceptance criteria.
Buyers should also note that some hybrid workflows combine additive manufacturing with subtractive finishing. In those cases, 5-axis machining is frequently used to finish functional interfaces, threaded zones, and anatomical contours after printing. That makes 5-axis capability relevant not only for fully machined parts, but also for post-processing precision zones.
How to Evaluate a Supplier for 5-Axis Medical Machining
Selecting a supplier for 5-axis CNC machining for medical devices should go beyond a machine list. The real evaluation must connect machine capability with process discipline, inspection strategy, documentation readiness, and material-specific experience. A 5-axis machine alone does not guarantee stable outcomes.
Five qualification checkpoints for sourcing teams
- Ask how many setups the supplier plans for the part and why.
- Review whether critical features are machined in one clamping cycle.
- Confirm inspection methods for contoured surfaces, positional features, and burr criteria.
- Check experience with the target material and feature scale, especially tools under 2 mm.
- Assess documentation alignment with medical quality workflows, including first-article and traceability support.
A competent supplier should be able to explain trade-offs in cycle time, fixture strategy, cutter engagement, and surface finish path planning. If the discussion stays at a generic level such as “high precision” or “advanced machine,” the sourcing risk remains high. Serious engineering dialogue should include measurable ranges, likely constraints, and validation logic.
The table below can be used as a practical supplier review framework during RFQ and technical clarification.
For medical programs, a strong supplier answer should be specific enough to support internal review by engineering, quality, and procurement within the same cycle. That can reduce RFQ back-and-forth by 1 to 2 rounds and shorten technical alignment before pilot production.
Common sourcing mistakes to avoid
One common mistake is assuming 5-axis always means higher total cost. For simple parts, that may be true. For complex parts, the opposite is often true once fixturing, inspection time, scrap exposure, and manual finishing are included. Another mistake is treating prototype success as evidence of production readiness. A supplier may make 3 good parts manually, yet struggle to hold consistency across 200 parts without a more robust process plan.
A third mistake is not defining critical-to-function features clearly in the drawing package or RFQ notes. If contour zones, edge breaks, or cosmetic surfaces are left ambiguous, even a capable 5-axis supplier may optimize the wrong variables. Better technical communication usually produces better machining outcomes than simply requesting “tight tolerance everywhere.”
Decision Guidance for Engineers and Procurement Teams
When deciding between 3-axis and 5-axis manufacturing, the most reliable method is to compare risk concentration points. If the part contains 3 or more critical surfaces on different orientations, if burr control is hard to maintain, or if setup count exceeds 3, the probability of favoring 5-axis rises sharply. The same applies when lot consistency is more important than nominal prototype feasibility.
A practical decision filter
- Choose 3-axis when geometry is simple, access is direct, and tolerance concentration is limited.
- Choose 5-axis when multiple angled features must relate tightly in one setup.
- Prioritize 5-axis when manual finishing threatens dimensional consistency.
- Escalate to 5-axis review when micro tools, deep cavities, or sculpted surfaces are involved.
For teams building supplier shortlists, this approach is more useful than comparing machine counts alone. It aligns manufacturing capability with the true performance drivers of the part: dimensional stability, surface condition, validation readiness, and repeatable delivery.
Medical manufacturing is unforgiving because geometry, quality documentation, and process consistency are tightly linked. That is why 5-axis CNC machining for medical devices has moved from a niche capability to a practical requirement for many advanced parts. It reduces setup-related variation, improves access to complex features, and supports cleaner, more repeatable production pathways for regulated applications.
For engineers, the benefit is better alignment between design intent and manufactured reality. For procurement teams, the benefit is lower process risk and more credible supplier evaluation. If you are reviewing a complex implant, instrument, or precision medical component, now is the right time to assess whether 5-axis capability should be part of your specification baseline. Contact us to discuss your part geometry, review machining feasibility, or get a more data-driven sourcing framework for your next medical device program.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























