
Where 5-axis CNC saves time in medical device machining
Publication Date
author
For project leaders in regulated manufacturing, time savings only matter when they do not compromise tolerance, traceability, or validation. That is exactly where 5-axis CNC machining for medical devices delivers measurable value. By reducing setups, shortening lead times, and improving geometric consistency on complex parts, it helps teams move faster from design review to qualified production while keeping engineering decisions grounded in data.
What 5-axis CNC machining means in a medical device context
In simple terms, 5-axis machining allows a cutting tool or workpiece to move across five different axes in one coordinated process. Compared with traditional 3-axis or even indexed 4-axis methods, this approach can reach complex surfaces, angled features, contoured geometries, and deep cavities with fewer interruptions. In medical manufacturing, that matters because many parts are small, complex, and highly regulated. They often require tight tolerances, clean surface transitions, and reliable repeatability across prototypes, pilot runs, and validated production lots.
For project managers and engineering leads, the importance of 5-axis CNC machining for medical devices is not only technical. It is operational. Every extra setup introduces additional risk: fixture variation, manual handling, dimensional drift, longer inspection time, and more chances for nonconformance. When the same part can be machined in one clamping instead of three or four, the benefit is not abstract. It appears in scheduling stability, scrap reduction, and faster release to the next manufacturing or validation stage.
Why the industry pays attention to time savings now
Medical device programs are under pressure from multiple directions. Product teams are expected to shorten development cycles. Quality teams must maintain documented traceability and process capability. Procurement and supplier management teams need confidence that a machining partner can scale from low-volume NPI work to repeatable production without changing the process window. In this environment, time savings are valuable only when they are predictable, measurable, and compatible with ISO 13485 quality requirements.
This is where a data-driven view becomes useful. TechStat Vanguard consistently emphasizes measurable engineering truth over marketing language, and that principle applies directly here. The real question is not whether 5-axis equipment looks advanced. The real question is where 5-axis CNC machining for medical devices reduces cycle time, setup count, inspection burden, and process variation in a way that supports qualification and delivery performance.
Where the time savings actually come from
Time reduction in medical machining usually comes from several linked mechanisms rather than one dramatic change. First, 5-axis machining minimizes repositioning. Complex parts that once needed multiple fixtures can often be completed in a single setup. Second, shorter tool paths and better tool orientation improve cutting efficiency, particularly on sculpted surfaces or angled features. Third, improved access can reduce the need for secondary processes, manual blending, or custom workaround fixtures. Finally, better geometric continuity often lowers the burden on final inspection and rework.
These gains become more important as part complexity rises. A straightforward rectangular housing may not justify full simultaneous 5-axis machining. But once a device includes compound curves, undercuts, intersecting bores, or anatomy-matching surfaces, the cost of conventional setups increases quickly. In those cases, 5-axis CNC machining for medical devices can save time not only on the spindle, but across the entire project workflow.
Medical device part categories that benefit most
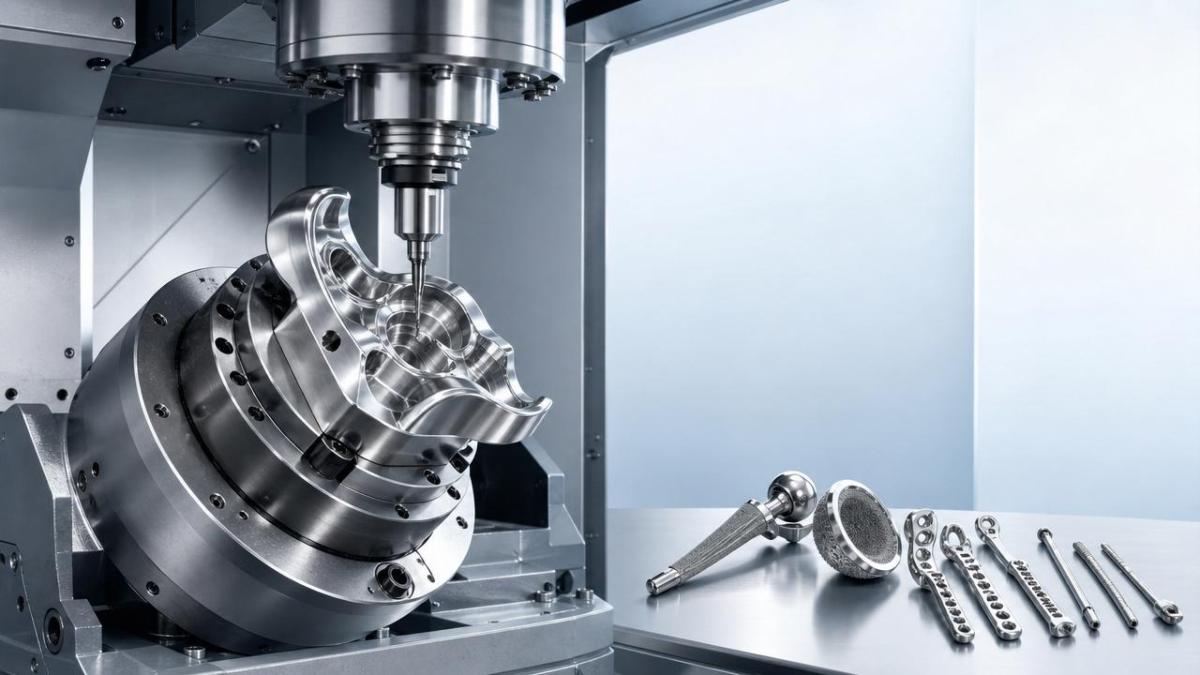
Not every component needs five-axis capability, but several medical part families frequently justify it. Orthopedic implants are a common example because they combine freeform surfaces with demanding surface and dimensional requirements. Surgical instrument components also benefit, especially when they include long slender forms, articulated interfaces, or angled features that are hard to reach consistently. Robotic-assisted surgery components, imaging support assemblies, and custom guides can also gain from more efficient machining access and reduced setup complexity.
Another important category is low-to-mid volume, high-mix production. In this environment, setup time has a disproportionate effect on total lead time. If a supplier can move rapidly between qualified part families without rebuilding a complicated fixture chain every time, the project schedule becomes easier to control. That is why 5-axis CNC machining for medical devices is often attractive not just for flagship implant parts, but also for precision support hardware used in diagnostic, therapeutic, and laboratory systems.
Business value beyond machine cycle time
A common mistake is to evaluate 5-axis machining only by spindle hours. For project leaders, the broader business case is usually stronger. When setup count decreases, planners gain scheduling flexibility. When fixture complexity drops, engineering change implementation becomes faster. When geometric consistency improves, first article inspection and validation documentation tend to move more smoothly. In regulated environments, that can compress the path from drawing release to approved production without weakening quality controls.
This matters especially during product introduction. NPI timelines often suffer from small delays that accumulate: fixture revisions, alignment issues, repeated inspections, and avoidable rework. 5-axis CNC machining for medical devices helps remove several of these failure points at once. The value is often felt in fewer engineering loops, quicker supplier feedback, and more stable readiness for process verification builds.
Materials, tolerances, and surface quality considerations
Medical devices are frequently machined from stainless steel, titanium, cobalt-chrome, aluminum, engineering polymers, and specialty materials with demanding behavior under cutting loads. Five-axis capability can improve tool engagement and access, but it does not eliminate material-specific challenges. Titanium, for example, still requires disciplined thermal management, stable tooling, and process control to avoid chatter or premature wear. Thin-wall polymer components still need careful fixturing and balanced cutting forces.
Surface integrity is another factor. Time savings are only meaningful if the finished part meets functional and regulatory expectations. On implant-adjacent or instrument-contact surfaces, burr control, edge condition, and micro-finish can be as important as nominal dimensions. A capable supplier should therefore connect 5-axis efficiency to metrology data, tool wear monitoring, and validated finishing steps rather than presenting speed as an isolated benefit.
What project managers should evaluate before choosing the process
From a management perspective, the key question is fit. Not all parts require simultaneous five-axis motion, and not all shops with 5-axis machines have the same programming depth, metrology capability, or medical quality maturity. A sound evaluation should start with part geometry, tolerance stack-up sensitivity, annual volume, revision frequency, and downstream validation needs. If a component requires multiple datum-critical relationships, freeform geometry, or repeated engineering updates, the case for 5-axis CNC machining for medical devices becomes stronger.
It is also wise to ask for evidence in engineering terms. Useful data points include achievable tolerance ranges by material, historical Cp or Cpk performance on comparable features, inspection strategy, toolpath simulation practices, and how the supplier manages first-off approval through production release. This aligns with TSV’s larger philosophy: procurement confidence should be built on benchmarkable technical facts, not adjectives.
Practical implementation advice for regulated programs
To capture the full benefit, teams should involve manufacturing engineering early. If designers understand how tool access, datum selection, and setup strategy affect machining efficiency, many preventable delays disappear before release. Design for manufacturability reviews are especially useful for parts with blended radii, deep pockets, internal features, or strict cosmetic requirements. Small geometry changes can sometimes unlock major savings in machining stability and inspection simplicity.
Second, align the machining plan with quality documentation from the start. For medical programs, that means linking process choices to traceability, inspection plans, and validation expectations rather than treating machining as an isolated supplier task. Third, segment parts by true complexity. Reserve full 5-axis strategies for components that actually benefit, while simpler parts may remain more economical on other platforms. This prevents overengineering the process while still applying 5-axis CNC machining for medical devices where it creates the greatest return.
Common misconceptions to avoid
One misconception is that 5-axis automatically means faster in every situation. In reality, programming complexity, machine availability, and tooling choices still matter. Another is that advanced equipment alone guarantees medical-grade consistency. It does not. Repeatability depends on a full process system that includes fixturing discipline, calibration, inspection capability, and documented control methods. A third misconception is that time savings should be measured only at the machining center. For regulated products, the real comparison should cover total project time from release to accepted lot.
A measured path forward
For engineering and project leaders, the case for 5-axis CNC machining for medical devices is strongest when it is framed as a system-level efficiency tool. It saves time by reducing setups, improving access to complex geometry, lowering variation between operations, and supporting smoother inspection and validation workflows. Those gains are most valuable on parts where precision, complexity, and regulatory accountability intersect.
If your team is assessing machining strategy for implants, instruments, robotic surgery hardware, or other precision medical components, start with the data: geometry complexity, tolerance criticality, setup count, and inspection burden. When those factors point in the same direction, 5-axis CNC machining for medical devices becomes more than a manufacturing option. It becomes a practical way to protect schedule, quality, and engineering confidence at the same time.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























