
Aerospace machining AS9100 compliance is harder than the certificate suggests
Publication Date
author
In aerospace supply chains, aerospace machining AS9100 compliance often looks straightforward on paper—but business evaluators know the certificate alone rarely reveals true process discipline, traceability depth, or risk control capability. This article examines why compliance is harder than it appears, and what procurement and technical teams should verify beyond the badge when qualifying precision machining partners.
Why does aerospace machining AS9100 compliance attract so much attention?
For business evaluators, the appeal is obvious: AS9100 is one of the clearest signals that a supplier understands aerospace quality expectations. It suggests a structured quality management system, documented controls, corrective action discipline, and awareness of regulatory and customer requirements. In sectors where a dimensional error, undocumented process change, or material mix-up can trigger field failure, scrap, or contract loss, those signals matter.
However, aerospace machining AS9100 compliance becomes strategically important not because the certificate is rare, but because the consequences of shallow compliance are expensive. A machine shop may hold certification and still struggle with revision control, subcontractor oversight, first article inspection quality, or process capability on hard-to-machine alloys. For procurement teams, this means the certificate is an entry condition, not proof of execution maturity.
That distinction is especially relevant in precision machining benchmarks. Aerospace programs depend on repeatable tolerances, complete lot traceability, calibrated measurement systems, and disciplined nonconformance handling. The business question is not “Does the supplier have AS9100?” but “Can the supplier consistently deliver aerospace-level machining under actual schedule and technical pressure?”
What does the certificate prove—and what does it not prove?
A valid AS9100 certificate proves that an accredited audit process found the company’s management system aligned with the standard at the time of audit. It generally indicates documented procedures, internal audit routines, management review activity, risk-based thinking, and a controlled quality framework. That is meaningful. It reduces screening friction and provides a baseline for supplier qualification.
But aerospace machining AS9100 compliance does not automatically prove deep technical competence in every machining scope. It does not guarantee superior 5-axis programming, stable fixturing strategy, burr control in thin-wall parts, distortion management after heat treatment, or process control on titanium, Inconel, aluminum-lithium, or other aerospace materials. It also does not guarantee the same maturity across shifts, product families, or subcontracted special processes.
In practice, evaluators should separate three layers: management-system compliance, process capability, and program execution reliability. A shop may score well on the first layer while remaining uneven on the other two. This is why advanced buyers increasingly pair document review with manufacturing audits, engineering interviews, and traceability sampling before awarding complex aerospace work.
Why is aerospace machining AS9100 compliance harder in real machining operations than it seems?
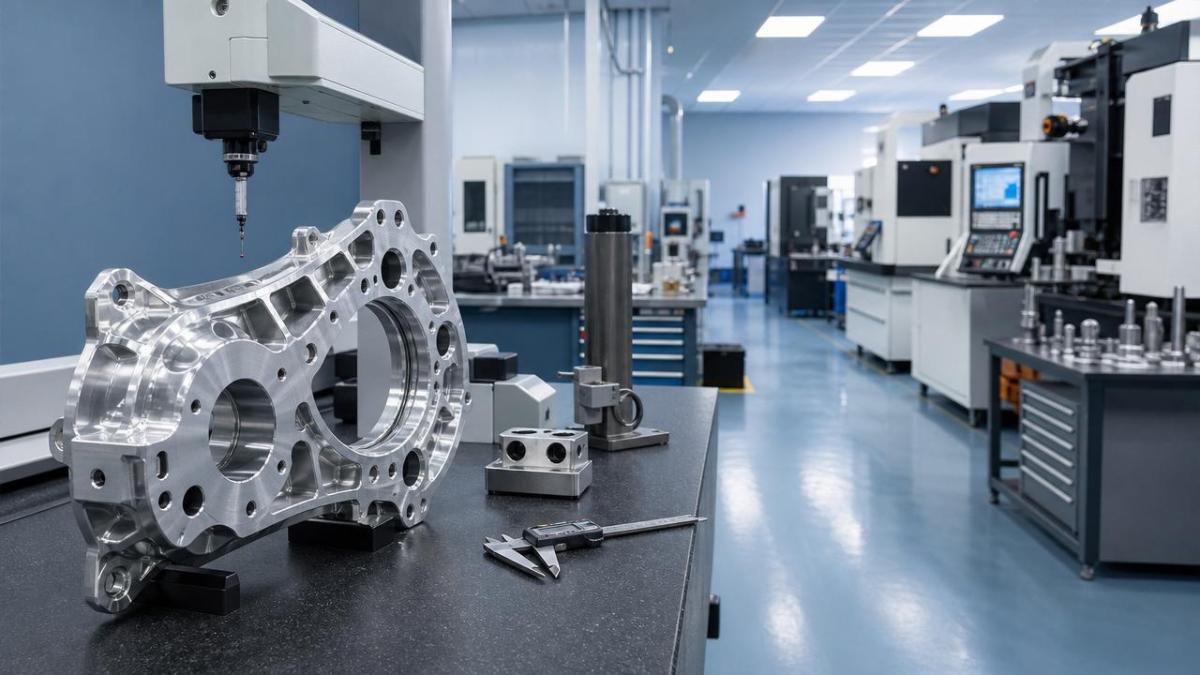
Because aerospace quality is not achieved through paperwork alone. It is achieved when documentation, machining practice, inspection method, and operator behavior remain aligned over time. That sounds simple until one looks at what actually happens on the shop floor. Tool wear changes hole quality. Fixture deflection affects flatness. Coolant variables influence surface integrity. Part orientation changes CMM repeatability. A last-minute engineering change can invalidate work instructions if document release is not fast and disciplined.
This is where aerospace machining AS9100 compliance becomes difficult. The standard expects control, but aerospace parts often involve low volume, high mix, difficult materials, and demanding lead times. Such conditions create process variability. The better suppliers manage that variability with planning, validation, in-process inspection, and containment logic. Weaker suppliers rely on final inspection to catch problems late, which is costly and risky.
Another challenge is traceability depth. In aerospace, traceability is not just a label on a box. Evaluators may need to confirm raw material heat number, certificates of conformity, machining traveler history, inspection results, NCR records, and links to outsourced special processes. If any of those links are incomplete, the supplier may be formally certified yet operationally fragile.
What should business evaluators verify beyond the AS9100 badge?
The most effective approach is to verify execution evidence, not only policy statements. Start with the part family that matters to your program. A supplier may be excellent at simple turned hardware yet far less mature with thin-wall milled housings, flight-critical brackets, or geometrically complex structural parts. Ask for representative evidence tied to similar tolerances, materials, and process routes.
First, review traceability completeness. Can the shop retrieve a sample shipped part and connect it to raw material certificates, in-process inspections, final inspection reports, machine routing, and any special processing records? Fast retrieval suggests process control is built into operations rather than reconstructed for audits.
Second, test their change-control discipline. How are drawing revisions released to programmers, setup technicians, inspectors, and operators? How are obsolete instructions removed? In aerospace machining AS9100 compliance, revision lag is one of the most dangerous hidden failure modes because a shop can appear organized while still allowing outdated shop-floor usage.
Third, assess inspection maturity. Do they only provide pass/fail reports, or do they understand process capability, measurement uncertainty, and characteristic risk? A strong aerospace machining partner can explain how critical dimensions are monitored, when in-process checks occur, and how they reduce measurement variation on complex geometry.
Fourth, examine nonconformance and corrective action behavior. Ask for anonymized examples. Did the supplier identify root cause at fixture design, tooling strategy, CAM path, operator instruction, or incoming material level? Did they implement preventive action and verify effectiveness? Corrective action quality often reveals whether the company is genuinely data-driven.
Fifth, check subcontractor governance. Many aerospace parts depend on external heat treatment, coating, surface finishing, or NDT. Weak oversight here can undermine otherwise solid machining performance. Evaluators should confirm approval criteria, revalidation logic, incoming verification, and how nonconforming outsourced work is contained.
What are the most common misconceptions about aerospace machining AS9100 compliance?
One major misconception is that certification equals low risk. In reality, it means the supplier has a quality framework that should reduce risk if properly maintained. Risk still depends on process complexity, staff competence, equipment condition, metrology capability, and management response under pressure.
A second misconception is that all certified shops operate at the same level. They do not. The gap between a minimally compliant supplier and a high-discipline aerospace machining organization can be wide. Both may hold the same certificate, yet one may run robust FAI packages, digital traveler control, and rigorous process validation, while the other struggles with inconsistent operator documentation and reactive firefighting.
A third misconception is that audit results fully mirror day-to-day behavior. Audits sample. Production reality is continuous. Business evaluators should remember that aerospace machining AS9100 compliance is partly about culture: whether teams escalate issues early, protect product integrity, and resist shipping pressure when quality evidence is incomplete.
Finally, some buyers assume that if a supplier passes first article inspection once, long-term consistency is assured. Yet FAI is only one checkpoint. Sustainable compliance depends on continued process control, reinspection discipline after changes, and stable execution across batches, operators, and machine availability constraints.
How can procurement and technical teams compare suppliers more effectively?
A practical way to compare suppliers is to combine certificate review with a structured evidence scorecard. This is especially useful when several shops all claim aerospace machining AS9100 compliance. The differentiator is not the existence of the claim, but the depth of objective proof supporting it.
Consider rating suppliers across five dimensions: process capability, traceability integrity, inspection robustness, special process control, and responsiveness to nonconformance. Then add commercial metrics such as lead-time realism, communication quality, and capacity transparency. This helps business evaluators avoid over-weighting one impressive presentation or one clean audit package.
- Ask for a recent FAI package from a comparable part, with redacted customer data if necessary.
- Request a mock traceability exercise on a completed part number.
- Review the control plan for critical characteristics and in-process checkpoints.
- Examine one corrective action case for depth, timing, and recurrence prevention.
- Verify how outsourced special processes are approved, monitored, and documented.
For organizations aligned with TSV’s data-first philosophy, supplier comparison should rely on measurable evidence rather than broad claims such as “high quality” or “aerospace grade.” Parameters, traceability records, inspection logic, and demonstrated control under change are far more predictive than sales language.
If a supplier seems compliant, what early warning signs still indicate hidden risk?
Several warning signs deserve attention. One is slow or incomplete document retrieval. If the supplier cannot quickly produce revision history, calibration status, material certs, or inspection evidence, their aerospace machining AS9100 compliance may be more superficial than operational. Another red flag is overreliance on final inspection with little in-process control. That often means defects are discovered too late.
Watch for vague answers about difficult materials or tolerance stacks. Strong suppliers can discuss process windows, tooling wear effects, fixture repeatability, and how they manage thermal or geometric distortion. Weak suppliers often answer in generalities. Also be careful when a shop outsources many critical steps yet offers limited visibility into those partners. In aerospace, external process opacity quickly becomes qualification risk.
Another subtle risk is cultural: a tendency to frame quality issues as isolated mistakes rather than system signals. Mature organizations investigate whether training, programming, setup verification, metrology methods, or supplier inputs contributed to the issue. That systems mindset is essential for resilient aerospace machining AS9100 compliance.
What should teams clarify before moving toward sourcing, qualification, or cooperation?
Before advancing with any supplier claiming aerospace machining AS9100 compliance, procurement and engineering teams should align on several practical questions. Which part families are in scope? What tolerances and critical characteristics drive risk? Which special processes are internal versus outsourced? What evidence must be provided at FAI, production release, shipment, and deviation approval stages? How quickly must traceability data be retrievable during customer audit or field investigation?
It is also wise to confirm capacity and escalation behavior. A supplier may be technically sound under stable volume but vulnerable under schedule compression or engineering change churn. Ask how they protect revision control, inspection bandwidth, and concession handling when workload spikes. The answer often reveals whether compliance is embedded in operations or dependent on heroic effort.
In the end, the certificate should open the conversation, not close it. For business evaluators, the real objective is confidence that the supplier can convert specification into repeatable, traceable, audit-ready aerospace output. If you need to confirm a specific program, tolerance range, process route, lead time, quote basis, or collaboration model, prioritize discussion around traceability depth, comparable part evidence, critical characteristic control, outsourced process governance, and response protocol when deviations occur. Those questions will reveal far more than the badge alone.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























