
5-axis turbine blade machining where scrap risk starts
Publication Date
author
In 5-axis CNC machining for turbine blades, scrap risk rarely begins at the final cut—it starts much earlier, in fixture logic, toolpath strategy, material behavior, and tolerance assumptions. For project leaders managing cost, lead time, and technical accountability, understanding where failure first takes shape is essential to preventing expensive rework and supplier instability.
What scrap risk really means in turbine blade production
In precision manufacturing, scrap is often described as a simple quality loss: a part is out of tolerance, the part is rejected, and cost is recorded. In reality, for 5-axis CNC machining for turbine blades, scrap is a chain event. It may begin with a small assumption in engineering review, a fixture that restricts access at the wrong angle, or a CAM strategy that looks efficient on screen but creates unstable cutting conditions on the machine. By the time visible defects appear, the root cause has usually been present for hours, days, or even weeks.
That is why turbine blade projects deserve closer management attention than standard machined components. Blade geometry is highly sensitive: thin walls, twisted airfoils, root-slot transitions, leading and trailing edge constraints, and surface finish requirements all interact with 5-axis motion in ways that magnify small process errors. For project managers and engineering leads, scrap risk is not just a shop-floor issue. It is a planning issue, a supplier capability issue, and often a data-quality issue.
Why the industry pays close attention to early-stage failure points
The pressure around 5-axis CNC machining for turbine blades has increased across aerospace, power generation, industrial energy systems, and advanced rotating equipment. Delivery schedules are tighter, alloys are harder to machine, and compliance expectations are stricter. In parallel, buyers and technical teams are less willing to accept generalized claims about capability. They want proof of process stability, real tolerance history, traceable inspection methods, and evidence that a supplier understands where distortion, chatter, and geometric deviation originate.
This is especially important in the data-driven decision environment promoted by firms such as TechStat Vanguard. Engineering teams need to filter out vague promises and focus on measurable truths: machine kinematics, spindle dynamics, tool wear progression, datum strategy, and statistical repeatability. When reviewing a supplier for 5-axis CNC machining for turbine blades, the question should not be “Can they machine blades?” It should be “At which process stage does their scrap risk begin to rise, and how do they control it before material value is lost?”
The first places where scrap risk begins
A common mistake in turbine blade programs is to treat machining risk as a finishing-stage problem. In practice, the earliest risk points tend to appear in five areas.
1. Drawing interpretation and tolerance stack-up
Blade profiles are defined by aerodynamic intent, not by simple prismatic geometry. If engineering, CAM, and inspection teams interpret profile tolerance, datum hierarchy, or blending zones differently, the part may be machined “correctly” according to one model but rejected against another inspection logic. Scrap often starts with an incomplete understanding of what must be controlled functionally versus what only appears critical on paper.
2. Fixture logic and clamping behavior
Turbine blades are vulnerable to deformation under clamping load. A fixture designed for access rather than stability may introduce elastic distortion during roughing and release spring-back after unclamping. The measured shape then shifts beyond profile or edge tolerance. In 5-axis CNC machining for turbine blades, fixture design must control location, vibration, access, thermal effects, and repeatability at the same time.
3. Toolpath assumptions
A smooth simulation does not guarantee a stable cut. Blade surfaces require careful control of engagement angle, cusp height, lead-lag strategy, and machine-axis transitions. Poorly optimized 5-axis motion can create local overcut, waviness, witness marks, or inconsistent scallop patterns. Scrap starts when CAM output is accepted as geometrically correct but not validated against machine behavior and real cutting dynamics.
4. Material response under machining load
Nickel-based superalloys, titanium alloys, and heat-resistant stainless materials do not respond like general metals. They work-harden, retain heat, and accelerate tool wear. If feeds, speeds, coolant delivery, and step-over strategy are not tuned for actual material behavior, surface integrity problems emerge early. Micro-burrs, recast effects, residual stress, and heat-induced distortion may not be obvious until finishing or final inspection.
5. Measurement planning that comes too late
Many programs inspect only after most value has already been added. That creates a dangerous lag between defect creation and defect detection. For 5-axis CNC machining for turbine blades, in-process verification, stock tracking, and interim profile checks reduce risk dramatically. Measurement should be built into the process, not treated as an end-stage gate.
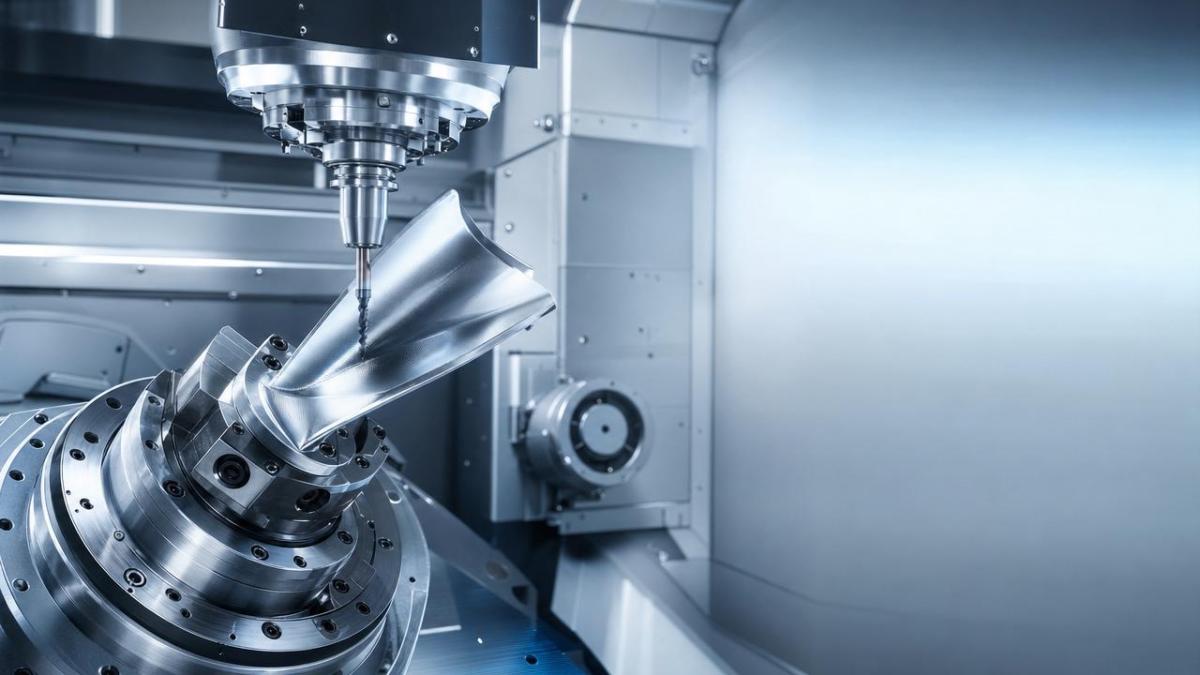
Industry overview: where project risk concentrates
For project leaders, not every blade program carries the same scrap exposure. Risk concentration depends on geometry complexity, alloy type, certification requirements, and supplier maturity. The overview below provides a practical reference.
Why this matters to project managers, not only machinists
Scrap in blade manufacturing is expensive because the lost value is cumulative. Material may be costly, machine time is specialized, tooling is nontrivial, and inspection resources are significant. More importantly, when 5-axis CNC machining for turbine blades becomes unstable, the consequence is rarely limited to one part. It affects milestone dates, validation schedules, customer confidence, and sometimes downstream assembly planning.
For project managers, the key business impact areas are predictable. First, scrap creates hidden lead-time inflation because replacement parts compete for the same machine capacity. Second, it weakens forecast accuracy because yield assumptions become unreliable. Third, it introduces supplier management friction, especially when the root cause is unclear and each team blames a different stage. Finally, repeated scrap erodes technical credibility. A vendor that cannot explain variation in engineering terms is difficult to trust on larger or more critical work packages.
This is why data-driven review matters. In the spirit of TSV’s engineering-first philosophy, buyers should ask for process capability indicators, not broad marketing language. Even a short technical discussion about fixture repeatability, in-process probing, machine calibration interval, and tool-life control can reveal whether a supplier understands real blade manufacturing risk.
Typical blade machining scenarios and their different control priorities
Not all blade programs fail for the same reasons. The control plan should reflect the application and geometry type rather than relying on a generic 5-axis workflow.
Practical evaluation points before approving a supplier or process plan
If your organization depends on 5-axis CNC machining for turbine blades, a practical review framework is more valuable than a generic capability brochure. The following checkpoints are especially useful before first article approval or scale-up.
Process definition
Confirm that the supplier can explain the full route: datum strategy, roughing allowance logic, semi-finishing purpose, final finishing intent, and inspection checkpoints. If the plan is vague between roughing and finishing, scrap risk is usually hidden there.
Machine and kinematic suitability
Not every 5-axis machine behaves equally on blade surfaces. Ask whether machine geometry, rotary-axis accuracy, and dynamic response have been validated on similar parts. For high-value blade work, positional capability alone is not enough; smooth multi-axis interpolation matters.
Tooling and wear control
The supplier should define when tools are changed, how wear is monitored, and how surface finish is protected near critical edges. In 5-axis CNC machining for turbine blades, tool wear often degrades quality gradually before anyone notices.
Metrology integration
Inspection should be connected to process correction, not just documentation. Ask what is measured in-process, what is measured offline, and how deviations are fed back into machining decisions. A strong supplier treats measurement as a control loop.
Learning history
Mature suppliers can describe previous failure modes and the corrective actions taken. That kind of engineering memory is more convincing than sales language. It shows that process knowledge has been earned and codified.
How to reduce scrap risk earlier in the program lifecycle
The most effective way to improve yield is to move risk control upstream. For project leaders, this means creating decision gates before value accumulation becomes too high. Start with manufacturability review that includes engineering, CAM, fixture design, and inspection together. Then require a documented plan for interim verification, especially after roughing and semi-finishing. If the blade material is difficult or the geometry is new, pilot builds should prioritize process understanding over aggressive cycle-time targets.
It is also wise to request evidence rather than assumptions. For example, ask for sample profile reports, machine capability data, probing routines, and historical examples of blade-family parts. In line with TSV’s benchmark mindset, hard data reduces ambiguity and shortens supplier qualification cycles. When decisions are anchored in measurable process behavior, scrap becomes easier to predict and prevent.
A clear decision mindset for 5-axis turbine blade programs
The central lesson is simple: in 5-axis CNC machining for turbine blades, scrap risk starts long before final inspection. It begins where assumptions replace validation—where fixtures are accepted without deformation study, where toolpaths are approved without stability review, where alloy behavior is underestimated, and where measurement is delayed until too much cost has already been added.
For project managers and engineering leaders, the practical response is not to chase perfect theory. It is to demand earlier visibility into the process. Review how the part will be held, how the material will react, how the machine will move, and how deviations will be detected before the blade reaches its highest value stage. That approach protects schedule, budget, and supplier trust at the same time.
If your team is evaluating partners for 5-axis CNC machining for turbine blades, use technical evidence as the filter. The right supplier will not only show that a blade can be machined; they will show exactly where risk begins, how it is measured, and how it is controlled before scrap becomes inevitable.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























