
5-axis CNC machining for turbine blades demands more than speed
Publication Date
author
When evaluating 5-axis CNC machining for turbine blades, speed alone is a misleading metric. For technical assessors, the real benchmark lies in profile accuracy, surface integrity, thermal stability, and repeatable tolerance control across complex aerofoil geometries. This article examines why procurement and engineering decisions must be grounded in verified machining data rather than headline cycle times.
Why is 5-axis CNC machining for turbine blades judged by more than cycle time?
In search results and supplier brochures, 5-axis CNC machining for turbine blades is often framed as a race for faster throughput. That framing is incomplete. Turbine blades are not simple prismatic parts; they are high-value aerodynamic components with twisted profiles, thin walls, varying chord thickness, root attachment features, and demanding surface requirements. A machine can remove material quickly and still fail the part where it matters most: airfoil form, edge consistency, subsurface condition, and process repeatability over a production batch.
For technical assessors, speed is only meaningful after process capability is proven. A shorter cycle time has little value if it increases chatter marks, creates thermal distortion, causes uneven stock removal, or pushes the supplier into unstable finishing passes. In aerospace and power-generation contexts, the downstream consequences are serious. Minor profile deviation can affect airflow efficiency, stress distribution, fatigue life, and balancing performance. That is why robust evaluation of 5-axis CNC machining for turbine blades must begin with engineering evidence, not marketing claims.
A mature supplier typically discusses machine kinematics, spindle behavior, fixture strategy, CAM verification, tool wear monitoring, in-process measurement, and final inspection correlation. Those details reveal whether the supplier understands the difference between producing a blade-shaped part and manufacturing a blade that meets design intent under repeatable industrial conditions.
What exactly should technical assessors verify in 5-axis CNC machining for turbine blades?
The evaluation should focus on measurable outputs and the process controls that generate them. For turbine blade work, the most important checks are usually not generic statements such as “high precision” or “tight tolerance.” Instead, assessors should request data tied to the blade geometry and material system being machined.
Key items include:
- Airfoil profile accuracy across multiple section planes, not just a few spot dimensions.
- Surface roughness and waviness on pressure side, suction side, platform, and fillet transitions.
- Leading-edge and trailing-edge consistency, especially where thin features increase machining risk.
- Root feature tolerance, including fir-tree or dovetail geometry where fit and stress concentration are critical.
- Thermal stability during roughing and finishing, especially with nickel-based superalloys or titanium alloys.
- Toolpath repeatability over multiple parts, not only first-article success.
- Inspection method correlation between CMM, scanning, probing, and any optical validation system.
A useful way to assess supplier maturity is to ask whether they can show process capability data by feature family. If a shop can only provide a final pass/fail report, the picture is incomplete. If it can present statistical evidence on profile deviation, surface consistency, and machine compensation trends over a batch, the assessment becomes much more credible.
This kind of evaluation framework is far more useful than comparing spindle speed, feed rate, or machine brand in isolation.
Which technical risks are most often hidden behind “fast” turbine blade machining claims?
The main risk is that high-speed messaging can mask unstable process behavior. In 5-axis CNC machining for turbine blades, speed claims may come from aggressive roughing numbers that do not reflect finishing quality. They may also ignore extra rework, manual blending, or selective part rejection after inspection. A fast quoted cycle can become a slow real-world program once scrap, correction loops, and unplanned tool changes are counted.
Another common issue is overreliance on machine specifications instead of process validation. A supplier may own advanced 5-axis equipment, but that does not guarantee capability on complex blade materials and aerofoil surfaces. Machine rigidity, rotary axis accuracy, thermal compensation, and controller smoothing all matter, yet they still need to be matched with suitable CAM strategy, cutting parameters, coolant delivery, and fixture engineering.
Thin-section distortion is also frequently underestimated. Turbine blades often require a delicate balance between material removal efficiency and dimensional stability. Excess cutting force or heat accumulation can deform the blade during machining, causing the final free-state geometry to drift after unclamping. Shops that truly understand 5-axis CNC machining for turbine blades build their sequence around stress control, staged stock removal, and measured verification between operations.
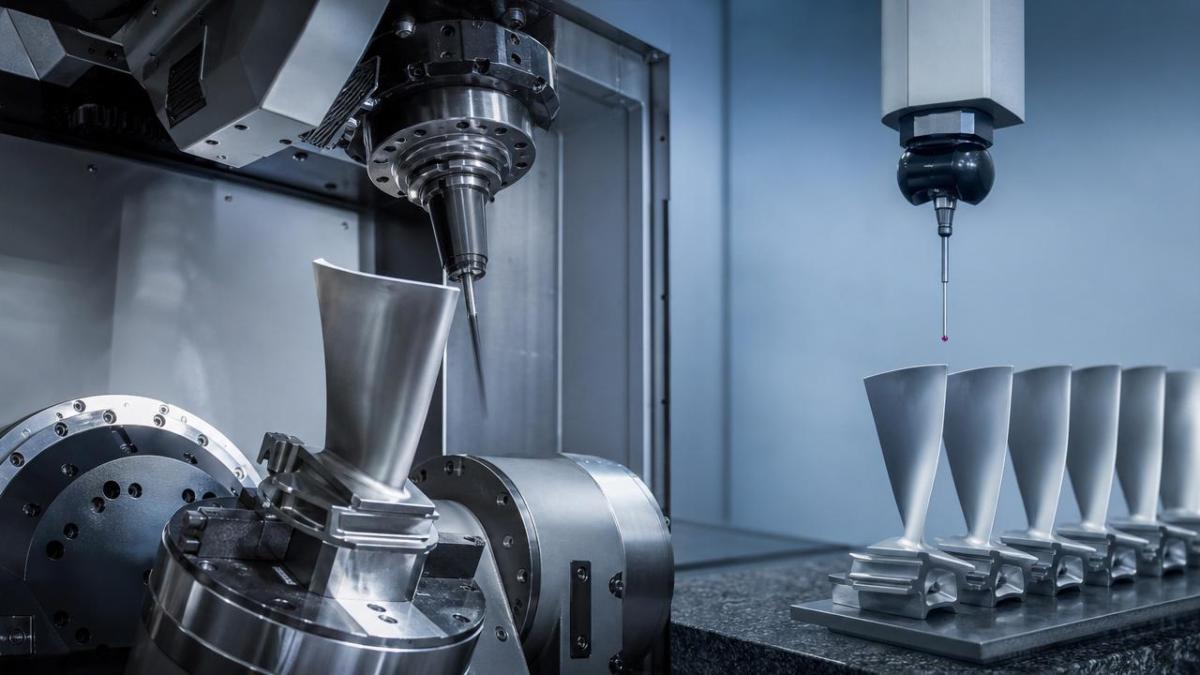
How do material, geometry, and thermal behavior change the assessment criteria?
Not all turbine blades present the same machining challenge. Assessors should avoid generic supplier comparisons and instead match the review criteria to the real application. Blade material strongly influences tool wear, cutting temperature, burr formation, and surface integrity. Nickel-based superalloys demand a different process window than stainless steel, aluminum, or titanium. Likewise, blade geometry can vary in twist, aspect ratio, wall thickness, and platform complexity, all of which affect dynamic stability during cutting.
Thermal behavior is especially important. A supplier may hold tolerance in a short demonstration run but lose consistency during extended production because spindle growth, ambient drift, or unstable coolant temperature alters tool center point accuracy. For this reason, technical assessors should ask how the machining cell controls thermal variables over time. Good answers often include warm-up routines, thermal compensation logic, stable coolant management, and periodic in-process probing to detect drift before final inspection.
Geometry drives another critical issue: line-of-sight and tool accessibility. The value of 5-axis capability lies in orienting the tool to maintain better contact conditions across the airfoil. However, difficult blade surfaces can still generate collisions, overlong tool assemblies, or unstable reach conditions. That means a supplier’s CAM simulation discipline, holder selection, and anti-collision validation process are all part of a serious assessment of 5-axis CNC machining for turbine blades.
How can buyers compare suppliers without being misled by polished presentations?
A reliable comparison starts with standardized questions and a demand for evidence in the same format from every supplier. This is where technical assessors create real value. Instead of asking who is “best,” ask each candidate to respond to the same blade-specific checklist: tolerance map capability, finishing strategy, process capability over batch size, traceability system, inspection method, and corrective action workflow for out-of-tolerance trends.
It also helps to distinguish between prototype competence and production competence. Some suppliers are excellent at one-off development parts but weak at repeatability, documentation, and controlled throughput. Others are optimized for stable series production but less flexible on iterative engineering changes. In 5-axis CNC machining for turbine blades, the right choice depends on whether the program is in R&D validation, pilot build, or qualified production.
When possible, assessors should request a sample evaluation package that includes:
- A first-article inspection report tied to blade CAD or section profiles.
- A brief process flow showing roughing, semi-finishing, finishing, and verification gates.
- Tool life assumptions and how compensation is managed as tools wear.
- Examples of nonconformance handling and root-cause analysis.
- Evidence of standards alignment, such as AS9100-related quality discipline where applicable.
A polished presentation may impress procurement, but standardized data comparison is what protects engineering outcomes.
What are the most common misconceptions about 5-axis CNC machining for turbine blades?
One misconception is that 5-axis automatically means superior quality. In reality, 5-axis motion creates more opportunity, but also more complexity. Poor toolpath strategy, inaccurate post-processing, weak rotary calibration, or inadequate fixture design can still produce inconsistent blades. Capability comes from the full machining system, not from axis count alone.
Another misconception is that the lowest cycle time equals the lowest cost. If fast cutting shortens tool life sharply, increases scrap, or adds hidden benchwork, the real cost per conforming part may rise. Technical assessors should therefore examine total process economics: yield, rework rate, tool consumption, inspection burden, and schedule reliability.
A third misconception is that final inspection can compensate for weak machining control. Inspection is essential, but it should confirm a stable process, not rescue an unstable one. In high-value blade manufacturing, quality is built through process discipline, machine calibration, thermal control, and feature-specific verification. Inspection alone cannot reverse metallurgical damage or repeated geometric instability.
Before approving a supplier or process, what questions should be clarified first?
For technical assessors responsible for sourcing, qualification, or benchmark review, the most effective next step is to convert broad interest in 5-axis CNC machining for turbine blades into a focused technical discussion. Start with the part family, material grade, tolerance zones, batch size, and inspection expectation. Then verify whether the supplier’s demonstrated capability comes from truly comparable blade work or from less demanding freeform components.
Priority questions should include: What profile accuracy is held across the full aerofoil? How is thermal drift controlled over a production shift? What evidence exists for repeatability across multiple parts? What is the strategy for thin-wall distortion and root-feature stability? Which measurement system is used to validate section geometry and surface quality? How are tool wear and process compensation tracked?
These questions move the conversation from generic capability to engineering truth. For organizations aligned with a data-first procurement philosophy, that distinction is decisive. In turbine blade manufacturing, speed matters only after capability, consistency, and verification are established. If you need to confirm a practical sourcing path, a pilot run, a benchmark comparison, or a qualification roadmap, begin by asking for documented machining data, process control evidence, and feature-level validation rather than headline promises. That is how informed teams evaluate 5-axis CNC machining for turbine blades with confidence.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























