
EDM for plastic injection molds: when surface quality beats speed
Publication Date
author
In precision tooling, speed is not always the winning metric. When mold makers prioritize mirror-like finishes, sharp details, and dimensional stability, edm for plastic injection molds often becomes the smarter choice. For quality control and safety professionals, understanding when surface integrity outweighs cycle time is essential to reducing downstream defects, improving part consistency, and validating whether EDM truly supports high-stakes production standards.
Why the conversation is shifting from throughput to surface integrity
A visible change is taking place across mold manufacturing. In the past, procurement and production teams often evaluated machining routes mainly by lead time and hourly cost. Today, that logic is being challenged by tighter cosmetic standards, thinner-wall part designs, higher customer expectations, and more aggressive validation requirements. As a result, edm for plastic injection molds is increasingly discussed not as a slow fallback process, but as a strategic option when defect prevention matters more than pure machining speed.
This shift is especially relevant in sectors where molded parts have direct impact on product appearance, sealing, optical behavior, or assembly consistency. Consumer electronics housings, medical device components, connectors, automotive interior parts, and high-precision packaging tools are all pushing mold makers toward finer detail reproduction and lower risk of surface-related nonconformance. In these settings, a slightly longer toolmaking cycle may be acceptable if it reduces polishing variability, flash risk, sink visibility, or repeated mold corrections later.
For quality control teams, the key industry signal is simple: the cost of poor surface quality is rising faster than the cost of slower machining. Rework, delayed PPAP approval, unstable cavity performance, and customer complaints can easily erase any time saved during rougher or faster machining routes.
What is driving stronger interest in edm for plastic injection molds
Several forces are behind this change, and they are not limited to one industry. First, part geometry is becoming more demanding. Manufacturers want deeper ribs, narrower slots, more complex shutoffs, micro-vents, fine textures, and intricate corner transitions that are difficult to machine consistently with conventional cutting alone. Second, many buyers are shortening product launch windows while still expecting better visual quality. That creates a paradox: teams need faster market entry, yet they cannot afford cosmetic defects or dimensional drift.
Third, mold materials and insert strategies are evolving. Hardened steels, specialty alloys, and replaceable cavity inserts often make non-contact material removal more attractive. EDM can access hard-to-reach features without introducing cutting forces that may distort delicate sections. Fourth, quality systems are becoming more evidence-based. Organizations influenced by stricter internal audits, customer scorecards, and advanced supplier qualification now ask not only whether a mold can be made, but how repeatably its critical surfaces can be controlled.
This is where edm for plastic injection molds earns renewed attention. It supports sharp geometry, controlled cavity detail, and consistent reproduction of complex features, especially when the expected finish quality is part of the product’s functional requirement rather than just its appearance.
A practical trend table: where selection criteria are changing
The decision pattern is no longer “fastest process wins.” More teams are comparing process routes by downstream quality impact.
For quality and safety functions, this table reflects a deeper operational change: process choice is being tied more directly to risk exposure across the full product lifecycle.
When surface quality truly beats speed
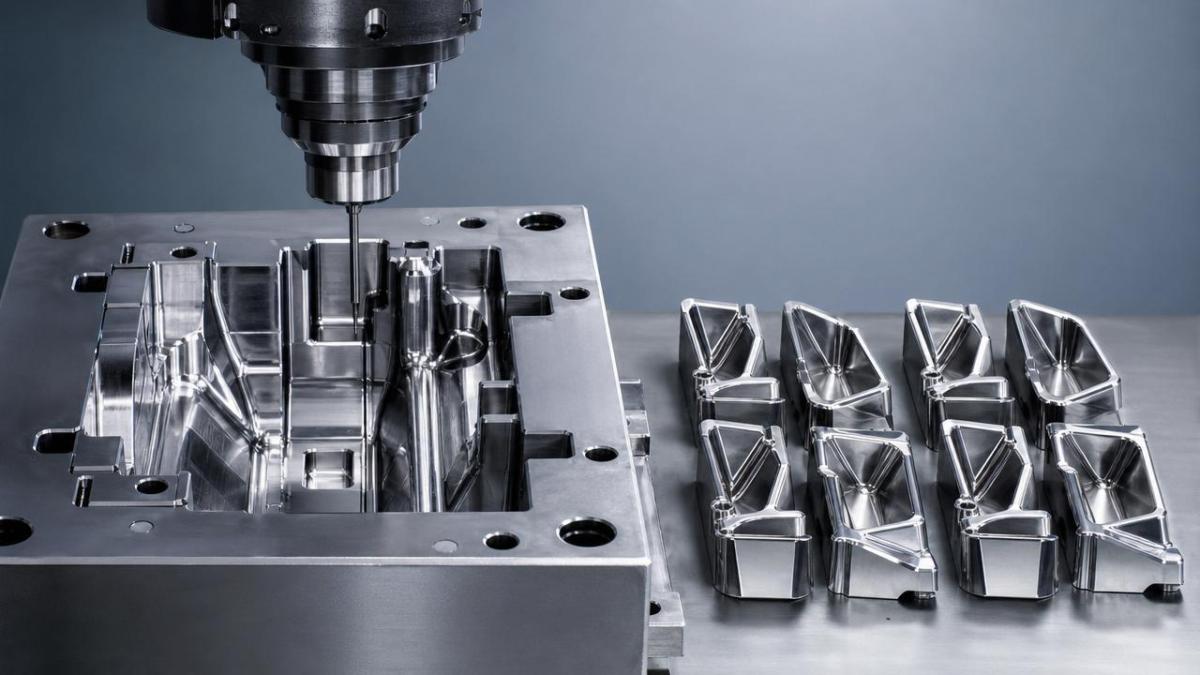
Not every mold should default to EDM-heavy processing. The smarter question is when surface quality creates enough value to justify a slower route. In current market practice, edm for plastic injection molds becomes more compelling in at least five situations.
The first is cosmetic-critical molding. If the final plastic part will be customer-facing and visible under direct light, cavity finish quality can influence perceived product value. The second is tooling with very fine details, where tool deflection, cutter access, or burr control becomes a problem. The third is tight shutoff or sealing areas, where poor surface condition can increase wear, leakage, flash, or inconsistent parting performance. The fourth is thin-wall or precision-fit molded parts, where dimensional stability and edge fidelity influence assembly yield. The fifth is molds intended for textured, polished, or optical-adjacent surfaces, where substrate integrity before finishing is important.
In all of these cases, speed loses strategic value if it creates hidden defects that appear later during sampling, validation, or volume production. That is the central trend: organizations are moving from process speed metrics to defect-cost awareness.
What quality control personnel should examine beyond the machine choice
For QC personnel, it is not enough to hear that a supplier uses EDM. The meaningful question is whether the EDM process is controlled in a way that supports mold quality objectives. Surface finish, recast layer behavior, micro-crack risk, electrode wear management, flushing effectiveness, and post-EDM finishing discipline all influence final results. A mold made with EDM can perform exceptionally well, but only when parameter selection and inspection logic are aligned.
This is an area where stronger supplier audits are emerging. Teams increasingly ask for evidence of process capability in critical features, not just photos of finished tools. For example, if a cavity relies on edm for plastic injection molds to generate sharp internal corners, QC should verify whether the resulting surfaces are inspected consistently and whether finishing steps preserve geometry rather than wash it out. If the mold supports transparent, glossy, or sealing-related parts, inspection plans should consider both dimensional and surface performance criteria.
Another practical signal is the growing use of cross-functional review before process approval. Tooling, manufacturing engineering, quality, and procurement are collaborating earlier because the process route now has direct consequences for launch timing and nonconformance risk.
Why safety managers should also care about EDM-related process decisions
At first glance, safety managers may see EDM selection as a technical manufacturing detail. In reality, it has wider relevance. Better mold surface quality can reduce unstable molding conditions, limit repeated setup changes, and lower the frequency of urgent corrective interventions on the shop floor. When tools perform more predictably, there is less pressure for rushed manual adjustment, emergency maintenance, or repeated polishing during active production windows.
There is also a supplier-side safety angle. EDM operations involve dielectric fluids, electrical discharge systems, debris control, and maintenance routines that must be managed carefully. For safety professionals evaluating mold partners, the issue is not simply whether EDM is used, but whether it is used within a disciplined environmental health and safety framework. Clean process control, documented maintenance, fire prevention measures, and proper handling of consumables all indicate operational maturity.
In other words, edm for plastic injection molds should be reviewed as part of a broader quality-and-safety system, not as an isolated machining method.
How procurement expectations are evolving
Procurement behavior is changing alongside technical expectations. Buyers used to compare mold suppliers heavily on quoted lead time, nominal machine capacity, and unit tool cost. Now, more sophisticated procurement teams are asking whether a supplier can justify the process route for specific critical features. This is a healthier purchasing pattern, especially in precision applications.
For example, a lower quote may reflect a machining path that minimizes EDM usage but increases polishing labor or correction risk later. A higher quote that includes carefully planned edm for plastic injection molds in selected cavity zones may actually reduce total program cost by improving first-shot quality and reducing approval delays. This is one of the biggest market shifts: purchase decisions are gradually moving from visible price comparison to hidden-risk evaluation.
A stakeholder impact view for current decision-making
Signals that EDM may be the better strategic choice
Several practical signals suggest that edm for plastic injection molds deserves stronger consideration. One is repeated mold trials caused by cosmetic issues rather than dimensional errors alone. Another is a pattern of polishing rework that changes geometry or delays release. A third is difficulty holding consistency in deep or narrow cavity features using only conventional cutting. A fourth is customer feedback that emphasizes finish repeatability, edge sharpness, or visual uniformity across lots. A fifth is internal concern that mold corrections are becoming more expensive than original process optimization.
These signals matter because they indicate the root problem may not be machine productivity, but mismatch between process selection and quality demand. In that context, EDM is not slower in a business sense if it prevents weeks of downstream disruption.
How organizations should respond without overcorrecting
A smart response does not mean moving every feature to EDM. Overuse can raise cost and time unnecessarily. Instead, companies should identify quality-critical zones where surface outcome, geometry fidelity, or tool stability have disproportionate impact on molded part performance. Those zones deserve a process-by-process review.
A practical approach includes four actions. First, classify mold features by quality consequence, not just by machinability. Second, request suppliers to explain why edm for plastic injection molds is or is not selected for each critical area. Third, link toolmaking decisions to measured launch outcomes such as first-shot acceptance, number of mold corrections, and cosmetic defect rate. Fourth, involve quality and safety personnel earlier in supplier evaluation, especially for programs with strict validation or high field-risk exposure.
This aligns with the broader industrial trend highlighted by data-driven organizations such as TSV: technical decisions should be anchored in measurable outcomes, not marketing claims or simplistic assumptions about faster always being better.
FAQ: common judgment questions from quality and safety teams
Does EDM automatically deliver a better finish?
No. edm for plastic injection molds can support excellent surface quality, but final results depend on parameter control, electrode condition, flushing, finishing practices, and inspection discipline. Capability matters more than the label of the process.
Is slower toolmaking always a bad trade-off?
Not if slower tooling reduces rework, trial loops, scrap, customer complaints, or validation delays. The better question is whether the process reduces total quality risk across the program.
What should be checked during supplier qualification?
Review process rationale for critical surfaces, evidence of inspection control, finishing methods after EDM, records of mold correction history, and safety management around EDM operations.
When is EDM less necessary?
For simpler geometries, lower cosmetic expectations, and non-critical surfaces, faster conventional machining may remain the best value. The trend is selective use, not universal use.
Final judgment: focus on risk, not just rate
The strongest industry change is not that EDM is replacing every other moldmaking method. It is that decision-makers are becoming more precise about where speed helps and where it quietly harms quality. In programs where appearance, sealing, detail sharpness, or dimensional stability carry high business risk, edm for plastic injection molds is gaining importance because it supports a more controlled path to acceptable outcomes.
For QC personnel and safety managers, the next step is practical: identify which mold features in your current or upcoming programs are truly quality-critical, then ask whether the chosen process route reflects that reality. If your organization wants to judge the impact of this trend on its own tooling strategy, focus on three questions: which defects are most expensive after launch, which surfaces drive those defects, and which suppliers can prove that their EDM process control supports repeatable mold performance.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)























