How to Choose a Space-Saving Vision Inspection System for Tight Production Lines
Publication Date
author
Anyone who has tried to fit an inspection station into a crowded production line knows the same problem: the machine looks fine on paper, but once it reaches the floor, there is nowhere to place the camera, no clean path for lighting, and barely enough room to open a panel for maintenance. The line still needs to move, the product still needs to be inspected, and the team still needs access when something drifts out of alignment. That is where a space saving vision inspection system becomes a practical decision rather than a nice-to-have feature.
The challenge is not simply finding a smaller unit. A compact system that blocks access, creates unstable image quality, or slows changeovers can be more disruptive than a larger setup with a clearer layout. If you are working around a tight footprint, the real question is how to choose a system that fits the machine, the inspection task, and the maintenance rhythm without forcing the whole line to bend around it.
Start with the space you actually have, not the brochure footprint
One common mistake is to compare only the listed dimensions of the controller, camera, and light source. On a production line, the usable space is affected by brackets, cable bends, airflow, cover opening angles, and the space needed to reach the lens later. A system that technically “fits” can still be awkward if it sits too close to moving parts or forces operators to reach over guarded areas.
Before looking at models, map the inspection point in three layers: the physical envelope, the service envelope, and the cable route. The physical envelope is the obvious machine space. The service envelope is the room you need to clean, replace parts, and adjust focus. The cable route matters more than many teams expect, because a tight bend or a poor exit direction can create repeated strain and make future changes messy.
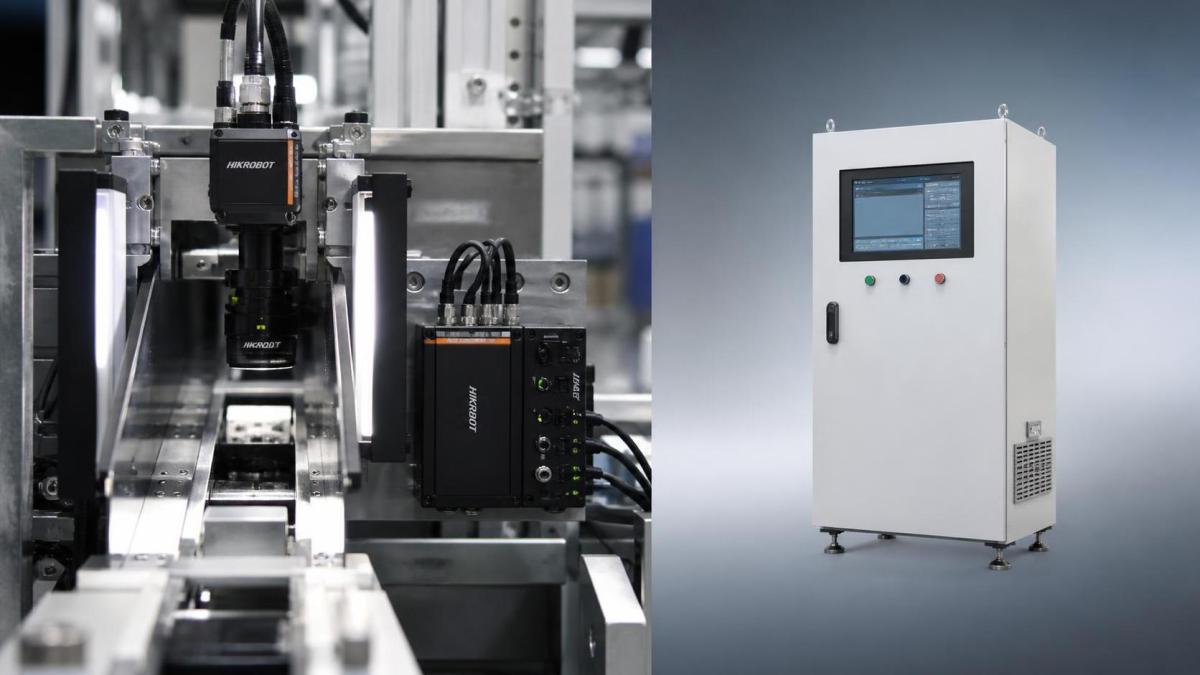
In compact layouts, a smaller head is useful only if it does not create a larger headache elsewhere. Wall-mounted controllers, remote lighting, and separated processing modules can reduce congestion around the inspection point. A good space saving vision inspection setup should leave the production line easy to work on, not just possible to install.
Match the inspection method to the part, not the other way around
Some inspection jobs need a wide field of view. Others need close-up defect detection, edge verification, code reading, or position checking. The space requirement changes depending on which of those is the real priority. For example, if you only need presence/absence or alignment checks, you may not need a large multi-camera arrangement. If fine surface defects or small features matter, a compact lens and lighting package may be more important than trying to shrink every component equally.
The useful question is: what failure would cause the most trouble if the system missed it? That answer helps determine whether you need high-resolution imaging, controlled lighting, multiple angles, or a simpler single-station setup. Many engineers discover that the tightest space is not the main problem; unclear inspection goals are. Once the inspection task is defined properly, the hardware can be narrowed to a system that does enough without taking over the machine.
Also consider product variation. If part sizes, surface finishes, or reflectivity change often, a rigid compact setup can become fragile in practice. A space saving vision inspection system should still offer enough adjustment range to handle those changes without forcing a mechanical redesign every time the product shifts.
Look at throughput and stability together
Space constraints can tempt teams to choose the simplest possible system, but a compact system that cannot keep pace with the line will still cause trouble. The inspection cycle needs to fit within the line speed, including trigger timing, image capture, processing, and communication with the PLC or control system. If any of those steps is shaky, operators may see intermittent alarms or inconsistent rejection behavior.
Stability matters just as much as raw speed. In a tight production line, vibration, heat, and changing ambient light can influence image quality. A smaller system may be more sensitive if it sits too close to press motion, conveyors, or transfer arms. That does not mean compact systems are a bad choice. It means they should be evaluated under real operating conditions, not only in a quiet demo setup.
When possible, test the system against the conditions it will face: part presentation differences, lighting changes during shift handovers, dust, and maintenance interruptions. If the image quality drops every time the machine cycles nearby, the issue is not the inspection algorithm alone. It may be the mounting position, the light angle, or the need for a more isolated enclosure.
Make maintenance access part of the selection criteria
Teams sometimes optimize so hard for compactness that the first lens cleaning becomes difficult. That usually shows up later as a slow, frustrating problem: small contamination, drifting focus, or a cable that has to be removed just to reach a screw. A well-chosen system should support routine maintenance without forcing a line stop longer than necessary.
Check whether focus, illumination adjustment, and replacement of common wear parts can be done from the front or side. Ask how often calibration is needed and whether that process requires tools that are hard to use in a crowded cabinet. If the answer depends on removing guards or moving other equipment, the system may be too cramped for the environment, even if the vision function itself is acceptable.
Maintenance access is also tied to future changes. Production lines rarely stay frozen. Product dimensions, inspection rules, and downstream equipment tend to evolve. A compact system with some modularity is easier to keep useful over time than one that fits perfectly only for the current layout.
Use integration effort as a real decision factor
A vision system can save physical space but consume control space if integration is messy. Wiring, I/O mapping, communication with the host machine, and software setup all matter. If the system needs unusual adapters or a long tuning process just to communicate with the line, the compact form factor may not be worth the added complexity.
For smaller production footprints, it helps when camera, lighting, processor, and interface options can be arranged in a way that keeps the cabinet clean. That does not mean every function must be bundled into one box. Sometimes separating the processing unit from the inspection head makes the whole arrangement easier to fit and service. The point is to reduce physical congestion without creating confusion in controls.
When comparing options, ask a simple question: how much effort will it take to install, validate, and later modify this system in the same space? A solution that looks compact but is hard to integrate often costs more line time than a slightly larger but cleaner setup.
A practical way to narrow the choice
If you are deciding between several compact systems, use a simple sequence. First, confirm the minimum inspection requirement. Second, measure the real installation and maintenance space, not just the open gap near the machine. Third, check whether the optics and lighting can handle the part surface and presentation. Fourth, review cycle time and communication. Last, consider how easy it will be to service the system after the line is running.
This is usually where the best option becomes clearer. The right choice is not the smallest unit on the list and not the most feature-heavy one either. It is the system that balances footprint, image reliability, and access in a way that fits the actual production environment.
For teams evaluating a space saving vision inspection system, the strongest decision is usually the one that respects both the inspection requirement and the physical reality of the line. If the layout is tight, the margin for poor mounting, difficult maintenance, or unstable lighting is even smaller. Choosing carefully at the start avoids the kind of field adjustments that consume more time than the inspection task itself.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)
 Sep 18, 2026Selecting UAV Aerospace Structural Parts for Strength, Weight, and Fatigue LifeUAV aerospace structural parts guide: compare strength, weight, stiffness, fatigue life, joints, and traceability to select reliable flight-ready components.Elena Rostova (UAV Systems Researcher)
 Sep 17, 2026Selecting Commercial Drone Payloads for European Inspection ProjectsCommercial drone payloads Europe: learn how to select RGB, thermal and LiDAR systems for compliant, reliable inspection data and better project outcomes.Elena Rostova (UAV Systems Researcher)