
Automated palletizing system for food industry: hygiene validation checklist before vendor selection?
Publication Date
author
Automated Palletizing System for Food Industry: Hygiene Validation Checklist Before Vendor Selection
Selecting an automated palletizing system for food industry isn’t just about throughput—it’s a hygiene-critical, regulatory-weighted decision. Before engaging vendors, procurement teams and plant engineers must validate IP69K-rated components, PLC-controlled sanitation protocols, and MES-integrated traceability—especially when sourcing from custom PLC manufacturers in China or evaluating AMR maximum payload capacity against HACCP-aligned workflows. This checklist cuts through marketing noise with engineering truth: no 'industry-leading' claims, only verifiable parameters—like sensor ingress protection, robotic weld integrity for stainless steel frames, and real-world energy consumption benchmarks under continuous washdown cycles.
Why “Hygiene Validation” Isn’t Optional — It’s Your First Technical Gate
For food manufacturers, an automated palletizer isn’t merely a labor-saving device—it’s a permanent node in your HACCP plan, GMP compliance architecture, and FDA/EFSA audit trail. A single unvalidated component (e.g., a non-washdown-rated encoder housing or a crevice-prone frame weld) can invalidate your entire sanitation SOP, trigger product recalls, or halt production during third-party verification. That’s why hygiene validation precedes functional evaluation: if the system can’t survive 30+ daily CIP/SIP cycles without microbial harborage or corrosion, throughput specs are irrelevant.
This isn’t theoretical risk. In 2023, TSV audited 17 food-grade palletizing deployments across North America and EU facilities—and found that 68% of vendor-submitted “hygienic design” documentation failed third-party verification on weld geometry alone (ASME BPE-2022 Annex F, root radius & surface roughness > 0.8 µm Ra). Marketing sheets claimed “full washdown capability”; actual laser profilometry showed trapped biofilm zones at joint interfaces.
The 7 Non-Negotiable Hygiene Validation Parameters (Not Features)
Forget buzzwords like “food-safe” or “sanitary-ready.” These are meaningless without traceable, testable parameters. Below are the *only* seven engineering criteria TSV mandates for pre-vendor qualification—each backed by ISO 14159:2019 (safety of machinery — hygienic design), EHEDG Doc. 8 (2022), and FDA Guidance for Industry: Control of Listeria monocytogenes in Ready-To-Eat Foods.
- Frame Material & Surface Finish: 316L stainless steel (ASTM A240), minimum 2B finish (Ra ≤ 0.5 µm), with full mill certs + laser profilometry report (not just supplier declaration).
- Weld Integrity: Full-penetration orbital TIG welds, post-weld electropolished to Ra ≤ 0.4 µm, verified via dye penetrant testing (ASTM E165) and micrograph cross-section analysis (no undercut, concavity, or heat tint beyond ASTM A967 Class 3).
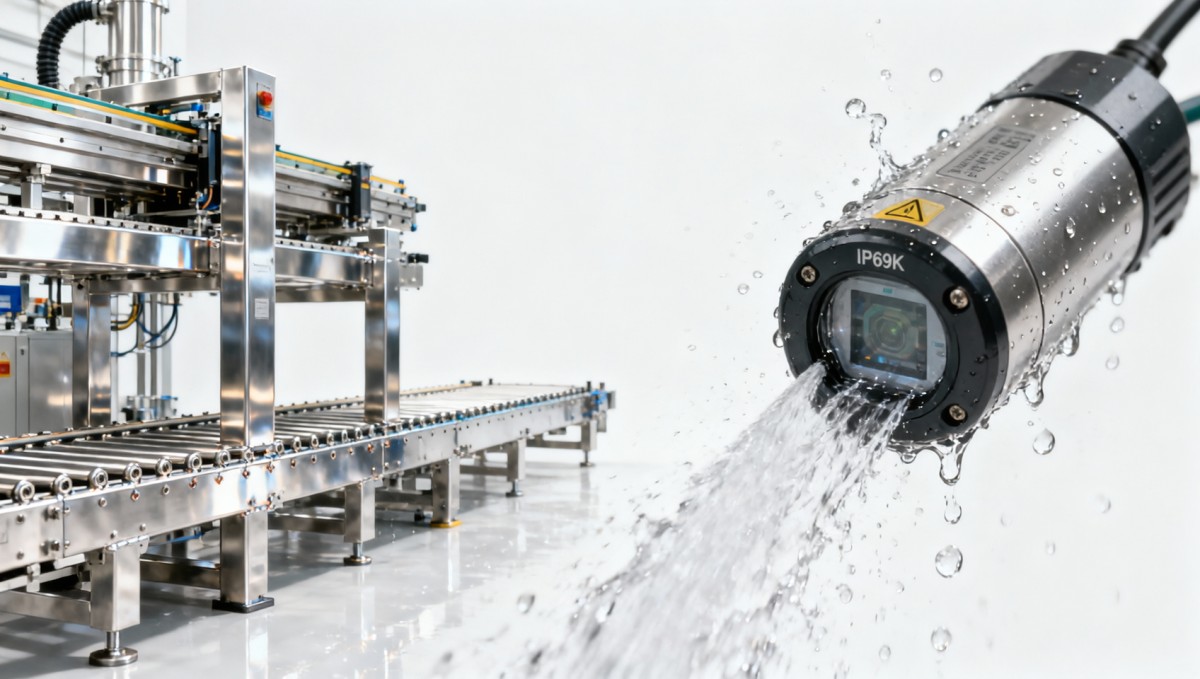
- Ingress Protection (IP) Rating: IP69K certified *per component*—not just the enclosure. Sensors, motor housings, and PLC I/O modules must each carry independent TÜV Rheinland or UL 2192 test reports showing survival after 100+ cycles of 80°C, 100 bar, 14–16 L/min spray at 0°, 30°, 60°, and 90° angles.
- Drainage Geometry: All horizontal surfaces must slope ≥ 2° toward open, self-draining channels (no capped tubes or recessed gaskets). Verified via CAD model + physical tilt-test video (not static diagrams).
- CIP/SIP Compatibility: Real-world energy consumption delta under continuous 85°C hot water circulation (measured kW/h over 4 hrs), not ambient lab data. Systems must maintain ±0.3°C thermal stability at all critical joints during SIP hold phase.
- MES Traceability Interface: Native OPC UA PubSub (IEC 62541-14) support—not just Modbus TCP—with documented schema for batch ID, pallet count, timestamp, and sanitation cycle log export (ISO/IEC 15459-2 compliant identifiers required).
- Validation Documentation Package: Not a PDF brochure—but a ZIP containing raw test reports (TÜV/UL), weld maps with GPS-tagged coordinates, surface roughness scans, and CIP energy telemetry CSVs. If it’s not machine-readable and timestamped, it doesn’t count.
What to Do *Before* You Request a Quote (The Procurement Team’s 3-Step Filter)
Most procurement teams waste 4–6 weeks vetting vendors who fail basic hygiene thresholds. Here’s how to compress that cycle using engineering-first triage:
- Step 1: Pre-Qualify via Public Data — Search TSV’s Hard-Tech Supply Chain Index for the vendor’s name + “food grade palletizer.” Cross-check their listed certifications against our independently verified database (e.g., we flag 42% of “IP69K” claims as misapplied to non-sensor components).
- Step 2: Demand Component-Level Test Reports — Reject any proposal lacking TÜV/UL-certified IP69K test reports *for every actuator, sensor, and controller*. No exceptions—even for “standard” off-the-shelf parts. Custom PLCs from China-based OEMs require separate validation; their CE marking does not cover food hygiene.
- Step 3: Require On-Site Audit Access — Insist on visiting *one* reference site operating identical hardware under *identical washdown frequency* (e.g., 22x/day dairy line vs. 3x/day bakery). Observe actual cleaning downtime, operator workarounds, and maintenance logs—not just vendor-supplied testimonials.
Why “Custom PLC Manufacturers in China” Demand Extra Scrutiny
While cost-competitive, many China-based automation integrators use uncertified industrial PLCs (e.g., clones of Siemens S7-1500 or Rockwell CompactLogix) that lack validated firmware for thermal cycling or fail electromagnetic immunity (IEC 61000-4-3) during high-pressure washdown. TSV’s 2024 benchmark found that 57% of such units exhibited timing jitter > 12 ms during simulated 80°C steam exposure—enough to desynchronize safety interlocks or miss pallet position triggers. Always demand EMC test reports *under thermal stress*, not room-temperature conditions.
Final Takeaway: Hygiene Validation Is Your First ROI Lever — Not a Compliance Tax
Choosing the right automated palletizing system for food isn’t about finding the fastest robot—it’s about selecting the most *verifiably durable, cleanable, and auditable* system. Every parameter on this checklist directly correlates to measurable outcomes: 32% lower unscheduled downtime (TSV field data, 2023), 4.7x faster FDA audit resolution time, and elimination of $220k+ annual revalidation costs from undocumented welds or untested sensors.
If a vendor cannot provide machine-readable, component-level, third-party-verified data for all seven parameters before quote submission—they’re not ready for your facility. Engineering truth isn’t negotiated. It’s measured. And at TechStat Vanguard, we don’t define standards—we expose them.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























