Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That Matter
Publication Date
author
An industrial vision inspection supplier should be selected on evidence that the complete system can make the required quality decision at production speed. Camera resolution, model accuracy, and a successful demonstration provide only partial evidence. Acceptance should depend on agreed defect definitions, representative parts, measured error rates, and proof that rejected parts actually leave the production flow.
For procurement, the strongest approach is to agree on acceptance tests before comparing final bids. This exposes differences in scope and makes performance commitments enforceable. A supplier that detects a defect on a stationary sample may still struggle with changing surface finishes, inconsistent presentation, or the time available to trigger a downstream reject mechanism.
Define the inspection boundary before asking for a guarantee
A useful acceptance specification starts with the quality decision: which conditions make a part unacceptable, and under what circumstances must the system identify them? “Detect scratches” leaves too much room for disagreement. Scratch width, length, contrast, location, and relationship to a functional surface can all change the inspection task.
Separate cosmetic judgments from functional requirements. A visible mark may be acceptable on one surface and disqualifying on another. If human inspectors disagree about borderline samples, resolve that disagreement before using those samples to score the supplier. Otherwise, the acceptance test measures an unsettled quality policy as much as machine performance.
For each required inspection, establish:
- The reject condition: the defect type, severity boundary, relevant location, and applicable drawing or quality requirement.
- The operating envelope: product variants, material finishes, permitted positioning variation, line speeds, and environmental conditions.
- The decision required: pass/fail, defect classification, dimensional result, or routing to a separate review process.
- The response to uncertainty: what happens when an image is missing, visibility is obstructed, or the system cannot issue a valid decision.
Some defects will be inaccessible to the proposed optical arrangement. A camera cannot reliably judge a concealed surface merely because its software recognizes similar defects elsewhere. Require suppliers to identify visibility limits and explain whether additional views, controlled positioning, or another inspection method is necessary. An explicit exclusion is more useful than an undefined promise of complete coverage.
Where dimensional inspection is involved, add a separate measurement acceptance requirement. Specify the reference method, allowable measurement error, and repeatability across the working range. A system can classify obvious defects correctly while lacking the measurement capability needed for a tight dimensional tolerance.
Make the sample set capable of challenging the supplier
The acceptance sample set should contain acceptable parts across legitimate process variation and defective parts across the conditions the system must detect. Include defects near the acceptance boundary, difficult locations, and combinations of defects where relevant. Testing only severe defects establishes little about the system’s ability to protect the actual quality limit.
Good parts deserve equal attention. Changes in supplier lots, machining texture, molded color, oil residue, print appearance, or permitted surface variation may resemble defects. If these conditions belong within normal production, they belong in the test. Otherwise, an apparently sensitive system may achieve detection performance by rejecting too much saleable output.
Establish a reference classification for every sample through the agreed quality process. Where necessary, use independent measurement or specialist review. Preserve the sample identity and reference result separately from the supplier’s output so that disagreements can be investigated without rewriting the original evidence.
Artificial defects can help explore system limits, but they need justification. A machined notch, digitally altered image, or manually applied mark may produce different optical behavior from the production defect it represents. Record which samples are natural, which are constructed, and what each is intended to demonstrate. Do not let an easy-to-image substitute silently become the contractual definition of a difficult defect.
Give the supplier development samples, then reserve a separate set for acceptance. Freeze the relevant software, model, recipes, exposure settings, and decision thresholds before scoring begins. If the supplier tunes the system after seeing a failed acceptance sample, treat the subsequent run as a new test and assess whether fresh held-out samples are needed.
Repeatedly presenting the same defective part does not provide the same evidence as testing many independent defective parts. Repetition helps assess consistency. Independent samples help assess coverage of defect variation. Both are useful, but the acceptance report should distinguish them.
Replace “accuracy” with separate error limits
Overall accuracy can hide the failure procurement most needs to understand. If most test parts are good, a system can appear highly accurate while missing an unacceptable share of defects. Require results by defect category and, where relevant, by product variant or difficult operating condition.
- Miss rate: defective parts incorrectly accepted, divided by the defective parts tested.
- False reject rate: acceptable parts incorrectly rejected, divided by the acceptable parts tested.
- No-decision rate: inspections that fail to produce a valid result, reported separately with their physical routing outcome.
Set limits according to the consequences. A missed safety-related defect and a cosmetic false reject carry different costs. Suppliers should demonstrate that the agreed detection threshold and false reject limit can be met together, using the same locked configuration. Separate demonstrations at different sensitivity settings do not prove that both requirements are achievable in production.
Sample size must support the claim being purchased. Zero misses in a small test does not establish zero risk. As an illustration, with zero misses across 300 independent, representative defective samples, the approximate one-sided 95% upper confidence bound on the miss probability is still about 1%. This statistical interpretation depends on the sampling assumptions; it does not prove equivalent performance for untested defect types or operating conditions.
For rare defects, obtaining enough representative samples may be difficult. Address that limitation openly in the purchasing plan through staged qualification, additional validation, or continued containment. A short demonstration cannot substantiate an extremely low escape-rate guarantee merely because no failures appeared.
Test the complete decision at production speed
A laboratory image test answers whether the inspection method can recognize the sampled conditions. Production acceptance must also answer whether the installed system can acquire the image, process it, associate the result with the correct part, and complete the required action before the available window closes.
Measure timing from the agreed production trigger to the point at which the result is usable by the line control or reject mechanism. Include acquisition, processing, communication, and actuation where they fall within the supplier’s scope. Average processing time alone can conceal occasional delays that cause missed decisions.
Run at the required sustained throughput with realistic part spacing and product mix. Include the fastest permitted operating condition and relevant start-stop behavior. A system that meets nominal speed with generously separated parts may fail when parts arrive close together or when several inspections compete for processing resources.
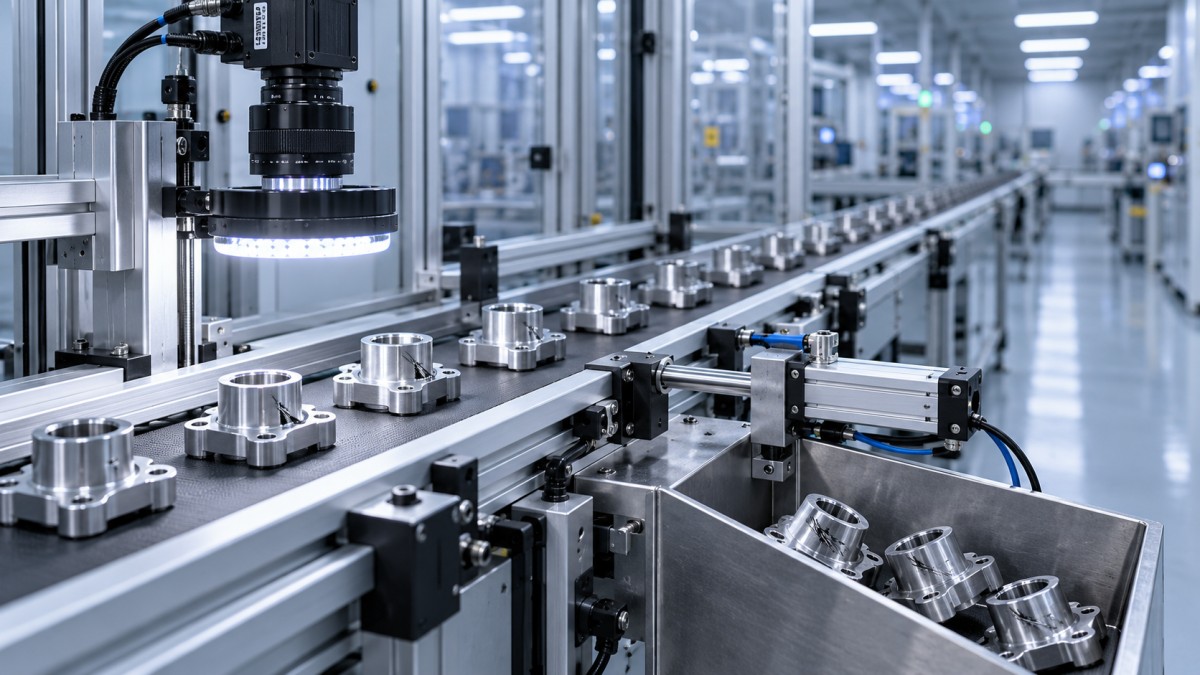
Challenge the physical reject sequence using identified samples. Verify that the defective part is removed, adjacent good parts remain correctly tracked, and a reject confirmation is recorded where required. Then test fault conditions such as a blocked reject path, loss of communication, a missed trigger, or an unavailable camera. The specified safe response should occur without silently releasing uninspected parts.
Repeatability testing should include removing and re-presenting parts, rather than repeatedly processing one stored image. Vary position, orientation, and other permitted presentation conditions. For measurement applications, compare results against the agreed reference and evaluate whether variation consumes too much of the tolerance available for the decision.
Environmental challenges should reflect the installation. Relevant conditions may include ambient light changes, vibration, temperature variation, or gradual contamination of protective windows. Define test conditions and maintenance intervals together: performance demonstrated with freshly cleaned optics cannot establish performance throughout a longer cleaning interval without supporting evidence.
A sustained run should be long enough to expose the risks identified for the application, including warm-up effects, image storage limits, communication interruptions, and operator interventions. Specify the duration and conditions before testing. Report stops, manual resets, bypasses, dropped images, and uninspected parts alongside throughput. A headline parts-per-minute figure loses value if maintaining it requires frequent intervention.
Turn the evidence into purchasing and acceptance terms
Use the same acceptance schedule for shortlisted suppliers. Ask each bidder to state compliance, exclusions, required buyer inputs, and the equipment included in its offer. This makes a lower price interpretable: it may reflect a simpler solution, or it may exclude fixturing, lighting control, reject confirmation, or integration work needed to achieve the promised result.
Divide verification between factory acceptance testing and site acceptance testing. Factory testing can establish inspection capability and integration behavior under controlled conditions. Site testing must address the actual installation, including the production interface, permitted environmental variation, and material flow. Passing the factory test should not automatically close requirements that could only be demonstrated on the buyer’s line.
The contract should identify who supplies and approves samples, who establishes reference classifications, who controls test execution, and who pays for corrective work and retesting. It should also define what happens if the system passes some defect categories but fails others. Conditional acceptance needs explicit restrictions, remaining obligations, and a completion date; otherwise, temporary workarounds can become permanent operating costs.
Connect payment milestones to evidence within the supplier’s control and the agreed division of responsibilities. If the buyer must provide stable fixturing or upstream part presentation, define those interfaces precisely. If the supplier owns complete inspection performance, its scope must include the components and integration needed to deliver it.
Require an acceptance record that preserves sample identities, reference results, system decisions, relevant images, timing records, and the tested configuration. Define access to those records and practical export arrangements. Retest rules should cover changes that could affect performance, such as a replacement camera, altered illumination, software updates, model changes, or new product variants.
Operator handover also belongs in acceptance. Confirm that authorized staff can select the correct recipe, recognize a degraded inspection condition, recover from defined faults, and restore the approved configuration. Uncontrolled threshold changes can invalidate a carefully demonstrated balance between missed defects and false rejects.
When choosing between suppliers, unresolved acceptance exceptions deserve as much attention as the quoted price. A credible offer states what will be detected, under which conditions, with what evidence, and what happens when the system cannot decide. The purchasing decision becomes defensible when those commitments survive testing on the parts and production conditions the buyer actually needs to run.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026How Do You Evaluate Solid-State LiDAR Point Cloud Density?Evaluate solid-state LiDAR point cloud density using valid returns, angular spacing, and real-world coverage. Discover how to compare sensors and choose the right fit for your application.TSV Data Lab
 Oct 22, 2026How Do You Test AMR Navigation Accuracy in a Warehouse?Test AMR navigation accuracy in warehouses with practical methods for localization, path tracking, and docking. Learn to set tolerances and compare robots before deployment.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026How Should You Balance Cobot Payload Against Reach?Explore cobot payload versus reach to choose the right robot. Learn how tooling, load limits, workspace, and cycle time affect performance—and avoid costly selection mistakes.Chen Wei (Automation Lead Engineer)