Comparing Material Options for Procurement: Specs, Costs, and Supply Risks
Publication Date
author
A lower material price can produce a more expensive finished part. Extra machining, unstable dimensions, rejected batches, or a delayed qualification can erase the saving before production begins. Comparing material options for procurement therefore starts with a practical question: which material meets the operating requirements at the lowest credible cost per accepted part?
The answer depends on the exact grade, condition, manufacturing route, and supply arrangements. Aluminum, stainless steel, engineering polymers, and composites each offer useful advantages, but those advantages have boundaries. Procurement-oriented technical content should connect material properties to purchasing decisions: what must appear on the specification, which costs belong in the comparison, and what evidence supports dependable supply.
Define the requirements that can eliminate an option
Begin with the conditions the finished component must survive. A material that fails a mandatory requirement should leave the shortlist before commercial negotiations. Otherwise, an attractive quotation can anchor the decision around an unsuitable option.
Separate mandatory requirements from preferences. Maximum weight may be mandatory for an airborne assembly, while a particular surface appearance may be negotiable. Chemical resistance may control the choice for a fluid-handling component, while stiffness and dimensional stability may matter more for a machine-vision mounting plate.
- Mechanical duty: load direction, stiffness, impact, vibration, fatigue, and allowable permanent deformation.
- Operating environment: temperature range, moisture, chemicals, ultraviolet exposure, and contact with dissimilar materials.
- Dimensional requirements: tolerances, flatness, surface finish, and stability after machining, conditioning, or assembly.
- Manufacturing constraints: machining, molding, forming, welding, bonding, heat treatment, and finishing.
- Documentation requirements: traceability, material certificates, inspection records, and any application-specific approvals.
Specify the conditions behind each requirement. “High strength” does not describe the load case, and “temperature resistant” does not distinguish brief exposure from continuous service under load. Clear requirements make quotations comparable and reduce the space for suppliers to offer different interpretations.
Compare material families without treating them as interchangeable
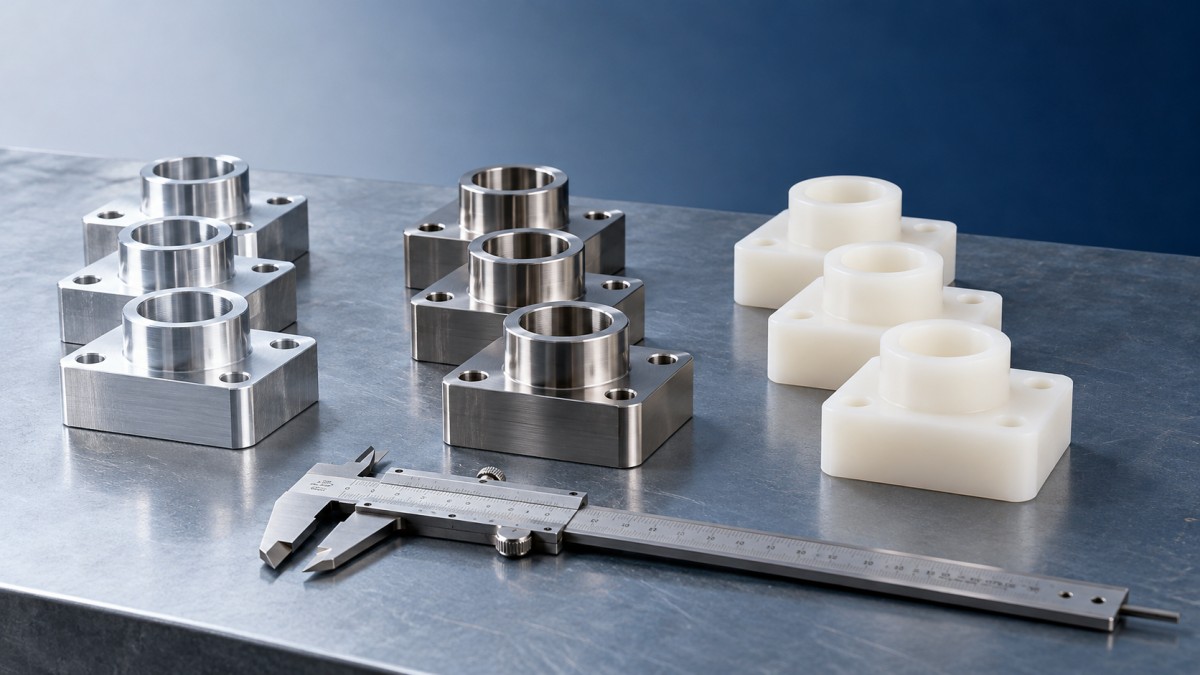
The following comparison provides a starting shortlist. Final selection still depends on the grade and finished-part design; a material family alone is too broad to purchase against.
Strength-to-weight ratio is useful when weight governs the design, but strength and stiffness answer different questions. A bracket can remain below its failure load and still deflect enough to disturb alignment. Replacing steel with aluminum may require a larger section to maintain stiffness, changing the weight saving, machining time, and available installation space.
Polymers require similar care. A short-duration strength value does not describe long-term deformation under sustained load. For composites, fiber orientation and the complete laminate matter: a property measured along the fibers cannot be applied to every loading direction.
Buy a defined material condition, not a familiar name
Descriptions such as “aircraft-grade aluminum,” “medical-grade plastic,” or “carbon fiber” leave major purchasing questions unanswered. A usable specification identifies the material closely enough that two suppliers can quote the same requirement and receiving inspection can distinguish an acceptable delivery from a substitute.
For metals, include the applicable material specification and revision, grade, temper or heat-treatment condition, product form, and required dimensions. Plate, bar, casting, and additive feedstock are not automatically equivalent, even when their nominal chemistry is similar. Processing history can affect properties, internal defects, residual stress, and machining behavior.
For polymers, identify the resin grade and relevant formulation details. Fillers, reinforcement, and additives can change stiffness, wear, electrical behavior, and dimensional stability. Where moisture affects performance, define the conditioning and measurement conditions rather than comparing dry test data with an application exposed to humidity.
For composites, specify the material system together with the manufacturing requirements. Fiber type alone does not define a finished structure. Layup, resin, cure, joints, and inspection criteria all influence whether the delivered part meets its purpose.
Also distinguish supplier capability from material evidence. A quality-management certificate can support assessment of a supplier’s processes, but it does not establish the properties of a particular batch. Connect the delivered lot to the required material certificate and inspection records. At TechStat Vanguard, this distinction between a claim and its supporting evidence is central to useful engineering comparison.
Compare total cost per accepted part
Price per kilogram is a poor comparison when materials have different densities, removal rates, scrap levels, or processing requirements. Ask for costs based on the same drawing, quantity, inspection scope, delivery terms, and acceptance criteria.
A practical comparison includes purchased stock, conversion, secondary processing, inspection, logistics, inventory, and expected quality losses. Keep one-time tooling and qualification costs visible rather than burying them inside a unit price that assumes future orders.
Stock utilization and machining can reverse the ranking
The required stock size may matter as much as the quoted material rate. A part machined from an oversized billet consumes material that never reaches the finished assembly. Available plate thicknesses, cutting allowances, minimum order quantities, and remnant ownership can all change the effective cost.
Machining cost depends on achievable cycle time, tool wear, workholding, chip control, and dimensional stability. A less expensive alloy that needs slower cutting or more finishing passes may lose its advantage. Conversely, paying for a more machinable grade can be worthwhile when conversion dominates the part cost.
Request the assumptions behind the quotation. If a supplier expects unusually high yield, minimal inspection, or a process that has not been demonstrated, the apparent saving rests on unresolved execution risk.
Secondary operations belong in the same comparison
Heat treatment, anodizing, plating, passivation, coating, bonding, and nondestructive inspection can add cost and lead time. They can also affect dimensions and surfaces. Specify whether acceptance applies before or after these operations and identify the surfaces where coating thickness matters.
For molded polymers and composites, include tooling, setup, process development, trimming, and production inspection. Compare alternatives at the expected order volumes and design maturity. A process with substantial tooling expense may become attractive for repeat production, while machining may suit smaller quantities or a design that is still changing.
Where yield is uncertain, compare several plausible outcomes instead of assigning an unsupported rejection rate. A preferred option that becomes uneconomic after modest rework deserves closer investigation before award.
Supply risk depends on the usable supply chain
A material can be widely traded while the required grade, thickness, condition, or qualified processing route remains difficult to obtain. Count sources capable of meeting the complete specification, rather than the number of distributors listing the material family.
Ask where stock originates, which operations are subcontracted, and which facilities are approved for the application. Two suppliers may rely on the same mill, resin producer, heat treater, or coating facility. Their quotations provide commercial choice without necessarily providing independent supply.
Break lead time into stock availability, production scheduling, outside processing, testing, and transport. This reveals whether an alternative source addresses the actual bottleneck. It also helps distinguish material already reserved for an order from availability that depends on a future production run.
Inventory decisions should reflect demand, replenishment variability, storage constraints, and the consequence of a shortage. Buying additional metal stock may be practical for a stable design. The same approach needs more care with shelf-life-controlled resins, prepregs, or materials whose storage conditions affect usability.
Useful commercial protections include agreed notice of material or process changes, traceable lot identification, defined treatment of nonconforming deliveries, and clear ownership of reserved stock. These terms connect the supply promise to something that can be checked.
Treat substitution as an engineering change
A proposed “equivalent” material can meet one headline property while changing machinability, fatigue behavior, corrosion resistance, dimensional stability, or assembly performance. Matching tensile strength alone does not establish interchangeability.
Require a substitution proposal to identify differences against the original specification. The review should cover grade and condition, relevant properties, manufacturing route, environmental compatibility, finishing, and documentation. Where design changes are necessary, include their cost and schedule impact in the commercial comparison.
The qualification scope should follow the function at risk. A cosmetic cover and a flight-critical structural component do not justify the same evidence. A dimensional inspection may demonstrate fit, but it cannot by itself demonstrate fatigue life, chemical resistance, or long-term creep behavior.
Agree who approves the change and what evidence closes the review before substitute material enters production. Verbal acceptance of an “equivalent grade” creates ambiguity precisely when a delivery problem or field failure needs a clear resolution.
Turn the comparison into a purchasing decision
Use mandatory requirements as pass-or-fail gates, then compare the remaining options on total cost, delivery confidence, quality evidence, and switching effort. A weighted score can help organize tradeoffs, but a low price should never compensate for failing an essential operating requirement.
Before issuing the purchase order, close three practical gaps:
- Specification gap: the drawing, material description, quotation, and acceptance requirements identify the same deliverable.
- Cost gap: tooling, finishing, inspection, freight, minimum quantities, and qualification responsibilities are included or explicitly allocated.
- Supply gap: material source, processing route, delivery assumptions, traceability, and substitution controls are understood.
When two materials remain close, investigate the uncertainty most likely to change the decision. That might mean machining a trial batch, testing chemical compatibility, reviewing laminate evidence, or establishing a second qualified source. The best next step is the one that resolves a consequential assumption before it becomes a production commitment.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)
 Oct 17, 2026How Should You Interpret Industrial Robot Repeatability Specs?Decode industrial robot repeatability specifications, understand ISO 9283 test conditions, and avoid costly selection mistakes. Learn how to verify performance for your process.Chen Wei (Automation Lead Engineer)
 Oct 16, 2026How Can You Fairly Compare MTBF Across Industrial Servo Motors?Make a fair industrial servo motor MTBF comparison with matched operating profiles, failure criteria, and confidence bounds. Discover how to assess reliability beyond advertised numbers.Chen Wei (Automation Lead Engineer)
 Oct 15, 2026How Should You Compare TechStat Vanguard 5-Axis CNC Tolerances?TechStat Vanguard 5-axis CNC tolerance comparison: learn how to verify part accuracy, assess inspection evidence, and choose suppliers that reliably meet your drawing requirements.Dr. Marcus Vance
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)