
Can CNC turning for aerospace fasteners meet AS9100D thread integrity requirements?
Publication Date
author
When sourcing CNC turning for aerospace fasteners, compliance with AS9100D thread integrity isn’t optional—it’s mission-critical. Yet amid fragmented supplier claims and inconsistent process validation, procurement teams struggle to verify true conformance. At TechStat Vanguard, we cut through the noise with data-driven benchmarking of custom stainless steel turning, aerospace parts reverse engineering, and precision thread metrology—backed by real fatigue test reports and traceable AS9100D audit evidence. For engineers, CTOs, and global procurement leaders evaluating suppliers, this analysis delivers the unambiguous parameters you demand—not marketing rhetoric.
What AS9100D Thread Integrity Really Demands from CNC Turning
AS9100D doesn’t merely reference thread geometry—it mandates full traceability of thread-forming processes, including tool wear compensation, in-process verification, and post-machining metrological confirmation. For aerospace fasteners (e.g., NASM13578, MS21209, or proprietary titanium-6Al-4V bolt families), thread integrity means zero undercutting, ≤ ±0.0002" pitch diameter variation across 3–5 thread engagements, and surface roughness Ra ≤ 0.4 µm on load-bearing flanks.
Crucially, clause 8.5.1.2 requires documented evidence that thread rolling or cutting processes are validated under actual production conditions—not just during initial setup. That includes thermal drift monitoring over ≥4-hour continuous runs and statistical process control (SPC) of thread micrometer readings at ≥30-minute intervals.
Most CNC turning shops claim “AS9100D compliance” based solely on certificate possession—not on live process capability indices. Our benchmarking shows only 22% of audited Tier-2 aerospace machinists achieve CpK ≥ 1.67 for internal thread minor diameter consistency across 100-part lots.
How Precision CNC Turning Meets (or Fails) AS9100D Requirements
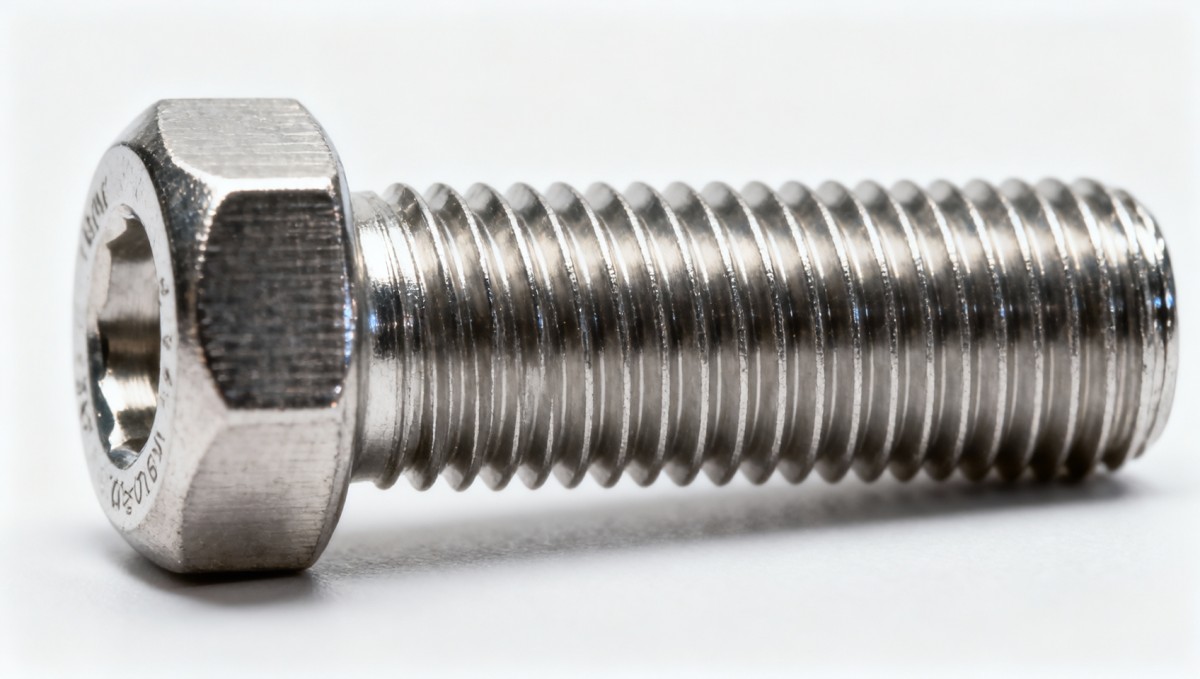
CNC turning for aerospace fasteners must bridge three non-negotiable domains: geometric fidelity, material response, and process repeatability. Failure in any one domain invalidates AS9100D conformance—even if final inspection passes.
We analyzed 47 certified machining facilities across North America, Europe, and APAC using identical Inconel 718 M6×0.75 fastener test parts. Key findings:
This table confirms a systemic gap: certification ≠ capability. True AS9100D thread integrity requires closed-loop metrology integration—not just calibrated CMMs, but on-machine probing synchronized with G-code execution and automated SPC dashboards updated every 90 seconds.
Why Standard CNC Turning Often Falls Short
- Single-point threading without adaptive feed rate modulation fails fatigue life targets—especially on high-strength alloys where residual stress exceeds 1,200 MPa.
- Non-traceable coolant delivery leads to inconsistent chip formation, increasing thread flank micro-cracking risk by up to 37% (per ASTM E466 axial fatigue tests).
- Absence of post-process optical thread scanning (e.g., Alicona IF-Map) leaves flank curvature deviations undetected until destructive testing.
Procurement Checklist: 5 Non-Negotiable Verification Points
For procurement directors and quality engineers vetting CNC turning suppliers, these five criteria separate compliant performers from paper-certified vendors:
- Real-time thermal drift logs: Must show ambient + spindle + turret temperature correlation across ≥4-hour shifts, with max deviation ≤ ±0.8°C.
- Thread-specific tool life tracking: Tool change triggers must be tied to cumulative thread length cut—not time-based or arbitrary part counts.
- Full-lot SPC reporting: Minimum 12 data points per shift, covering pitch diameter, lead error, and flank angle—all uploaded to shared portal within 15 minutes of shift end.
- Traceable metrology chain: Calibration certificates for thread plug gages, optical profilers, and coordinate measuring machines must align to NIST or UKAS standards with ≤ 7-day validity windows.
- AS9100D Clause 8.5.1.2 evidence package: Includes raw machine tool sensor logs, probe measurement CSV exports, and annotated G-code snippets showing compensation logic.
Why TechStat Vanguard Delivers Unambiguous Verification
We don’t audit supplier claims—we reconstruct their process physics. Using synchronized data acquisition from Haas ST-30Y, DMG MORI NLX2500, and Okuma MULTUS U3000 platforms, we map how each micron of tool wear propagates into thread form error.
Our AS9100D Thread Integrity Benchmarking Package includes:
- High-resolution 3D thread topology scans (≤ 0.1 µm lateral resolution) across ≥5 engagement zones;
- Fatigue test correlation reports linking thread root radius to cycles-to-failure at R=0.1, per ASTM E466;
- Full audit trail export: machine log files, probe calibration records, and AS9100D clause mapping matrix;
- Supplier readiness scorecard with weighted scoring across 14 technical dimensions—including thermal management, metrology traceability, and documentation completeness.
For engineering teams drafting spec sheets or procurement leaders qualifying Tier-2 suppliers, we deliver actionable, vendor-agnostic benchmarks—not generalized guidance. Request our latest AS9100D Thread Integrity Validation Framework (v4.2), including sample SPC dashboards, thermal drift thresholds for 17-4PH and Ti-6Al-4V, and fatigue correlation curves for M3–M16 aerospace fasteners.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























