
Surface finish standards become costly when specs are vague
Publication Date
author
Vague callouts in precision machining surface finish standards often trigger hidden cost, rework, supplier disputes, and delayed approvals—especially when project teams assume everyone reads the same spec the same way. For engineering and project leaders, the real risk is not just cosmetic inconsistency, but compromised function, inspection confusion, and sourcing inefficiency. This article explains why unclear finish requirements become expensive, and how data-driven specification language helps prevent avoidable manufacturing failures.
Why do vague precision machining surface finish standards create such expensive problems?
Because surface finish is rarely just a visual preference. In precision manufacturing, finish affects sealing, friction, coating adhesion, fatigue life, cleanliness, optical behavior, and downstream assembly results. When a drawing says “fine finish,” “smooth surface,” or even a single roughness value without method, area, and direction, every supplier fills in the blanks differently. One machine shop may choose a standard milling pass, another may add grinding, polishing, or bead blasting, and a third may stop production to request clarification. All three responses cost time or money.
For project managers, the hidden issue is that vague precision machining surface finish standards multiply uncertainty across the workflow. Quoting becomes inconsistent, process routing changes late, inspection criteria shift from operator to operator, and final acceptance becomes subjective. A part that “looks good” may still fail if the contact surface causes leakage, noise, wear, or unstable sensor readings. That is why unclear finish requirements often become a budget problem, a schedule problem, and a supplier management problem at the same time.
At TechStat Vanguard, the lesson is simple: parameters must carry engineering intent. If a surface requirement influences function, then the specification must say exactly how. Otherwise, project teams pay for interpretation instead of performance.
What does a complete surface finish specification actually need to include?
Many teams assume a roughness number alone is enough. It is not. A complete callout should connect measurement to function and inspection. In practical terms, robust precision machining surface finish standards usually need several elements working together.
First, identify the parameter clearly. Is the requirement Ra, Rz, Rt, or another roughness metric? These values are not interchangeable, and confusion here is a common source of disputes. Second, define where the requirement applies. A sealing face, bearing seat, cosmetic exterior, and hidden mounting plane may all need different finishes on the same part. Third, state the process expectation only when function truly requires it. If grinding is required for flatness and texture consistency, say so. If the result matters more than the process, avoid over-constraining the supplier.
Fourth, include the measurement condition. Cutoff length, sampling length, filter standard, measurement direction, and instrument type can change the reported value. Fifth, clarify whether lay direction matters. On dynamic sealing surfaces or sliding interfaces, the orientation of machining marks can be as important as the roughness average itself. Finally, define acceptance logic: is the finish requirement mandatory over the full surface, a functional zone, or sampled points only?
When these details are omitted, suppliers make assumptions, inspectors use different setups, and nonconformance reports become arguments about interpretation instead of engineering truth. Strong precision machining surface finish standards do not add complexity for its own sake; they reduce ambiguity before cost enters the system.
Which project scenarios are most sensitive to unclear surface finish requirements?
Not every part needs tight control, but certain applications become expensive very quickly when precision machining surface finish standards are incomplete. One high-risk scenario is any sealing surface, whether static or dynamic. If roughness is too high, leakage can occur. If it is too low, lubricant retention or gasket behavior may suffer. Another scenario is bearing fits and sliding contact surfaces, where finish directly affects wear, friction, noise, and thermal behavior.
Medical, aerospace, robotics, semiconductor, and sensor-related parts also deserve careful finish callouts. In these environments, contamination, micro-scratches, reflectivity, and coating consistency may all matter. A machined housing for an edge AI device may need a stable finish for thermal contact. A UAV structural bracket may require controlled finish to support fatigue performance after machining. A robotic actuator component may need a finish that supports both fit and long-cycle durability.
Even in less regulated sectors, cosmetic and customer-facing hardware can trigger commercial risk. If one batch has visible tool marks and the next has polished faces, the end user sees inconsistency even if dimensions pass. Procurement teams then face returns, brand complaints, and pressure to sort suppliers by capability rather than by quote alone.
This is why engineering leaders should not treat surface finish as a late-stage shop-floor detail. It is an early-stage specification decision with direct impact on sourcing efficiency and product reliability.
How do vague finish callouts increase cost across quoting, machining, and inspection?
The cost increase usually starts before any material is cut. When a drawing is ambiguous, suppliers quote defensively. A capable shop may assume the strictest interpretation and add extra process steps, inspection time, and contingency cost. A lower-cost supplier may assume a basic interpretation and win the order, only for the part to fail review later. Either way, the buyer does not receive a clean apples-to-apples comparison.
During production, unclear precision machining surface finish standards often create routing changes. A turned or milled finish may no longer be enough, so parts move to grinding, lapping, superfinishing, or manual polishing. That means more setups, more operator touch time, more queue time, and higher scrap exposure. Manual rework is especially dangerous because it may improve appearance while degrading geometry, edge condition, or consistency.
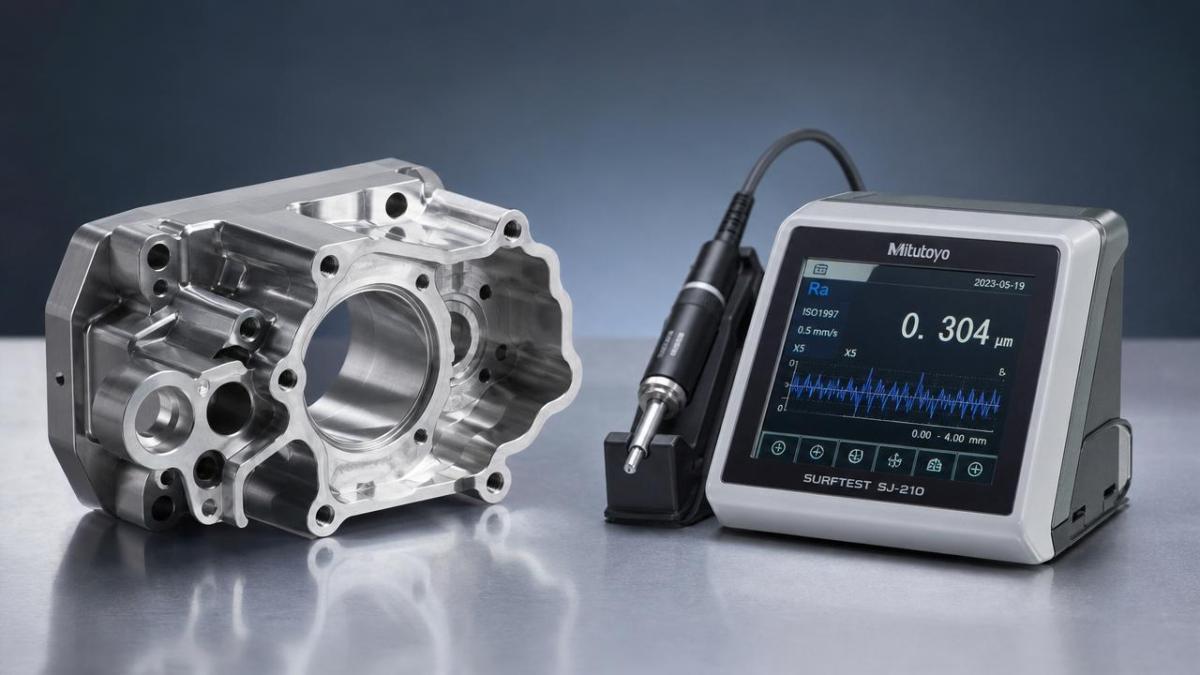
Inspection adds another layer of cost. Surface measurement is sensitive to instrument selection, stylus path, cutoff settings, and operator technique. If the drawing does not define the basis clearly, quality teams may measure multiple times, escalate to engineering, or reject borderline parts that would otherwise function correctly. This causes delays in first article approval, PPAP-style documentation flows, and production release decisions.
The most expensive outcome is not always scrap. It is often the slow erosion of trust between engineering, sourcing, quality, and suppliers. Once disputes become routine, every new order carries administrative drag. In global manufacturing programs, that drag can exceed the cost of the finish itself.
What are the most common mistakes teams make when writing precision machining surface finish standards?
A frequent mistake is using generic phrases instead of measurable requirements. Terms like “smooth,” “high quality,” or “no visible marks” sound simple, but they create subjective evaluation. Another mistake is applying one finish requirement to the entire part when only a few functional surfaces need control. This drives unnecessary cost and may push shops toward slower processes without performance benefit.
Teams also confuse cosmetic finishing with functional finishing. Bead blasting, anodizing, tumbling, polishing, and passivation can affect appearance, but they do not automatically deliver the roughness behavior needed for sealing, friction control, or fatigue-sensitive applications. Similarly, specifying an aggressive finish without checking manufacturability can create avoidable schedule pressure, especially on complex geometries, deep pockets, thin walls, or hard materials.
Another major error is ignoring process capability by material and machine type. A finish that is practical on ground tool steel may be unrealistic on a thin aluminum part fresh off a 5-axis milling cycle without secondary processing. Smart specification writing should reflect actual production pathways. That does not mean lowering standards; it means matching the requirement to what function truly needs and what the supply chain can control repeatably.
Finally, many teams fail to connect finish requirements with inspection planning. If no one defines how the finish will be checked, accepted, and recorded, then the standard exists on paper only. Effective precision machining surface finish standards always travel with a verification strategy.
How can project managers judge whether a finish requirement is strict enough without overspending?
Start with function, not habit. Ask what the surface actually does in service. Does it seal, locate, slide, reflect light, hold coating, transfer heat, resist contamination, or support fatigue life? Once the function is clear, define the minimum finish performance that protects it. This is where data-driven thinking matters. Instead of inheriting a number from an old drawing, trace the requirement to test results, field history, supplier capability data, or benchmark parts.
Next, separate critical surfaces from noncritical ones. A tiered approach is often the most efficient. For example, use a tighter roughness range on sealing and bearing interfaces, a moderate requirement on assembly-related surfaces, and a broad cosmetic criterion elsewhere. This helps procurement compare suppliers more accurately and prevents blanket overprocessing.
It is also wise to review the requirement with both manufacturing and quality before release. Ask whether the specified finish can be produced consistently on the chosen material, geometry, and volume, and whether the inspection method is practical at receiving, in-process, and final stages. If the answer is uncertain, the spec is not ready.
For project leaders managing supplier qualification, a useful rule is this: if the finish requirement could change process routing or acceptance outcome, it should be documented explicitly in the RFQ package and reviewed during technical alignment. Precision machining surface finish standards should not be left for post-award interpretation.
Quick decision guide for project teams
How should teams communicate with suppliers to avoid disputes over surface finish?
The best time to prevent conflict is before the purchase order is placed. During RFQ and technical review, ask suppliers how they interpret the finish requirement, what process route they plan to use, and how they will inspect it. If two suppliers propose very different methods for the same drawing, that is usually a sign the callout is not precise enough.
It also helps to request example measurement reports for comparable parts, especially when introducing a new supplier or moving production across regions. This exposes differences in metrology practice early. For critical programs, teams should align on first article expectations, including which surfaces will be measured, how many readings are needed, and what documentation must accompany shipment.
A mature sourcing process treats precision machining surface finish standards as part of technical governance, not cosmetic detail. Procurement, quality, and engineering should share one language around acceptance. When that happens, supplier conversations become objective and productive. When it does not, every shipment risks becoming a debate.
What should you confirm first before finalizing a drawing, quote, or supplier decision?
Before release, confirm five points. First, what functional surfaces truly require controlled finish? Second, which roughness parameter and measurement settings reflect the real need? Third, does the supplier’s process capability match the requirement on the actual material and geometry? Fourth, is inspection practical and repeatable across internal and external quality teams? Fifth, does the requirement belong in the RFQ, control plan, and first article package so nobody discovers it too late?
For project managers and engineering leads, this discipline reduces rework loops, approval delays, and avoidable quote spread. For organizations focused on advanced manufacturing, it also shortens supplier qualification cycles by replacing vague language with measurable intent. That is exactly the kind of engineering clarity TechStat Vanguard advocates: less marketing language, more operational truth.
If you need to move from a general requirement to a manufacturable standard, the most useful next discussion is not “Can you make it smoother?” It is: which surfaces are critical, what performance are we protecting, how will it be measured, what process will achieve it consistently, and what cost or lead-time impact follows from that choice? Those are the questions that turn precision machining surface finish standards from a hidden cost driver into a controlled engineering decision.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Sep 28, 2026Spindle Runout Measurement in Germany: DIN Standards, Methods, and Acceptance LimitsSpindle runout measurement Germany: explore DIN standards, proven methods, acceptance limits, and audit-ready practices for reliable machining quality.Dr. Marcus Vance
 Sep 27, 2026How to Select Wall-Mount Edge Devices for Space-Constrained Factory NetworksWall mount edge devices for space-constrained factories: evaluate workload, thermal design, power resilience, cable access, and network reliability for smarter deployments.TSV Data Lab
 Sep 26, 2026Machining Tolerance Analysis: How to Set Limits That Meet Function and Cost TargetsMachining tolerance analysis: learn how to set functional limits, control tolerance stacks, reduce inspection risk, and balance precision with production cost.Dr. Marcus Vance
 Sep 25, 2026How to Evaluate an Industrial Infrastructure Data Platform for Multi-Site OperationsIndustrial infrastructure data platform evaluation guide for multi-site operations: compare data quality, edge resilience, interoperability, governance, and scalable proof-of-value criteria.Victor Lin (Chief Software Architect)
 Sep 24, 2026How to Select Machine Vision Optics for Accurate Inspection at Different Working DistancesMachine vision optics selection guide for accurate inspection at every working distance. Compare FOV, pixel scale, DOF, distortion, lighting, and telecentric options.TSV Data Lab
 Sep 23, 2026How to Evaluate a Machine Vision System Integrator for High-Speed Inspection LinesChoose a machine vision system integrator with proven expertise in high-speed inspection, reliable reject timing, robust optics, and measurable acceptance criteria.TSV Data Lab
 Sep 28, 2026When is a SCADA API the right choice for connecting plant systems?SCADA API guide: learn when governed plant data integration improves traceability, security, and scalability—without compromising real-time control.Victor Lin (Chief Software Architect)
 Sep 27, 2026How SCADA data integration improves traceability across production linesSCADA data integration connects production-line data to improve traceability, accelerate quality investigations, and strengthen safety decisions.Victor Lin (Chief Software Architect)
 Sep 26, 2026What to define before starting SCADA integration planningSCADA integration planning starts with clear scope, control boundaries, data models, cybersecurity, and testing. Discover the definitions that reduce risk and costly rework.Victor Lin (Chief Software Architect)
 Sep 25, 2026How a smart factory with Industrial IoT reduces production blind spotsDiscover how a smart factory with Industrial IoT turns real-time machine, quality, and workflow data into actionable insights that reduce production blind spots and delivery risks.Victor Lin (Chief Software Architect)
 Sep 24, 2026When does Industrial IoT make smart manufacturing easier to scale?Smart manufacturing Industrial IoT scales when trusted data, interoperable systems, and secure workflows turn connected assets into measurable gains.TSV Data Lab
 Sep 23, 2026What drives ultra-precision machining cost at 1-micron tolerance?Ultra precision machining cost per part at 1 micron tolerance depends on process, material, metrology, and yield. Learn how to compare quotes confidently.Dr. Marcus Vance
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)























