
Defect Detection Systems Miss Good Parts Too: Here Is Why
Publication Date
author
Even the most advanced machine vision defect detection systems can reject acceptable products, creating hidden costs across production, procurement, and quality control. From solid-state LiDAR point cloud density validation to precision machining dimensional accuracy control and industrial IoT predictive maintenance solutions, false rejects often stem from data quality, tolerance settings, and system integration gaps. This article explains why good parts get missed—and how engineering teams can reduce that risk.
When a defect detection system misses a bad part, the problem is obvious. When it rejects a good part, the damage is quieter—but often just as expensive. False rejects reduce yield, create operator distrust, distort supplier performance data, and can trigger unnecessary process changes. For engineers, buyers, and operations leaders, the key question is not whether automated inspection makes mistakes. It is why those mistakes happen, how often they happen, and whether the system is tuned to the real manufacturing risk.
Why defect detection systems reject good parts in the first place
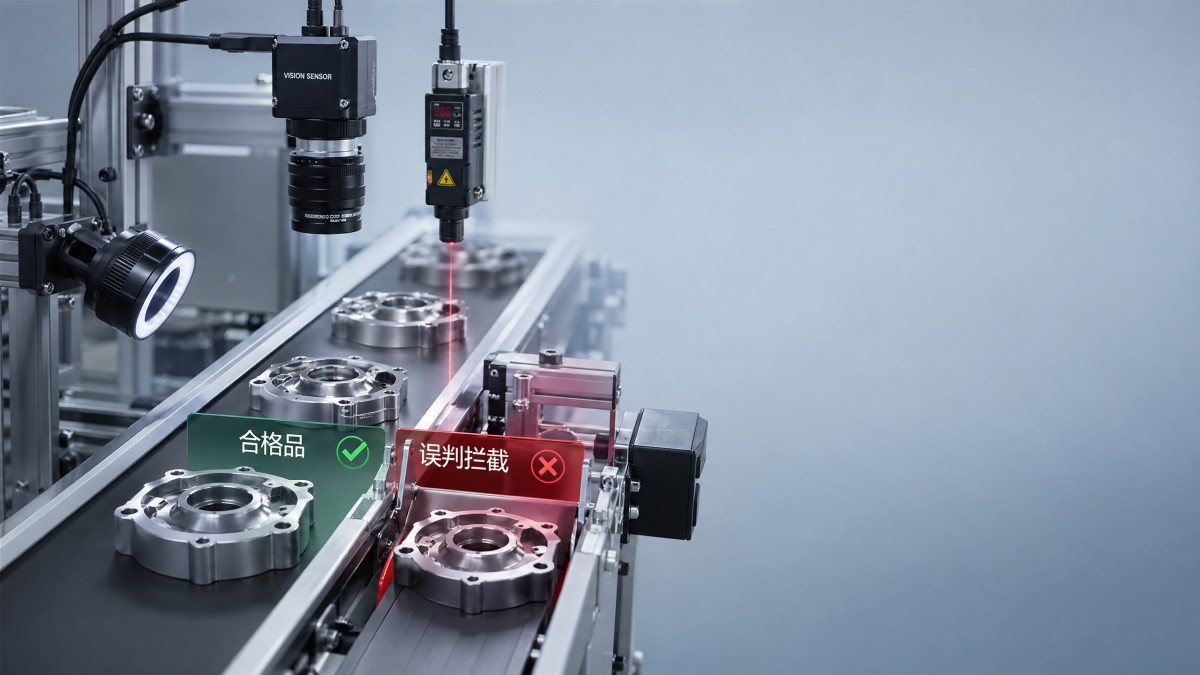
Most false rejects do not happen because the inspection technology is “bad.” They happen because the full inspection chain is narrower, noisier, or less stable than the production reality it is supposed to judge.
In practice, a defect detection system evaluates a part against a model of acceptability. If that model is incomplete, the data is unstable, or the tolerance window is poorly aligned with functional requirements, good parts will be flagged as defective.
The most common root causes include:
- Overly tight thresholds: Inspection limits are often set closer than real engineering requirements.
- Weak training data: Vision or AI models may not have enough examples of acceptable variation.
- Lighting and environmental instability: Small changes in illumination, vibration, dust, or temperature can alter readings.
- Part presentation errors: Orientation, fixture repeatability, or surface reflectivity can confuse the system.
- Sensor resolution mismatch: The system may be trying to classify features near or below its reliable detection capability.
- Poor system integration: Camera, PLC, conveyor timing, edge processor, and MES data may not be synchronized correctly.
- Spec ambiguity: The inspection rule may not reflect the actual functional quality standard.
In other words, false rejects are usually an engineering and systems problem—not just a software problem.
What false rejects really cost manufacturers, suppliers, and buyers
For many organizations, the cost of rejecting good parts is underestimated because it gets spread across multiple departments.
On the production floor, false rejects lower first-pass yield, create reinspection loops, slow throughput, and add operator intervention. A line that appears highly controlled may actually be losing efficiency because inspectors and technicians are spending time sorting parts that were never bad.
For quality teams, false positives create noisy data. If the system reports defects that are not real, process capability analysis becomes less reliable. Engineers may chase the wrong root causes, adjust the wrong process parameters, or escalate supplier issues unnecessarily.
For procurement and supplier management, false rejects can distort vendor scorecards. A capable supplier may appear unstable simply because the incoming inspection system is too sensitive, poorly calibrated, or misaligned with print tolerance intent.
For business decision-makers, the impact is broader: scrap inflation, hidden labor cost, delayed shipments, excess buffer stock, strained supplier relationships, and weaker confidence in automation ROI.
This is why experienced buyers and CTO-level evaluators no longer ask only, “What is the detection accuracy?” They ask more useful questions such as:
- What is the false reject rate by defect class?
- Under what lighting, speed, and part-mix conditions was performance validated?
- How does the system behave near tolerance boundaries?
- Can the vendor separate model confidence from hard-pass/fail logic?
- What is the cost of misclassification in real production conditions?
Why “high accuracy” claims often hide real inspection risk
A published accuracy number can be technically correct and still commercially misleading. Many defect detection systems are validated in controlled test environments with ideal samples, stable lighting, limited product variation, and clean labeling. Real factories rarely operate under those conditions.
Three issues are especially important:
- Class imbalance: Defective parts are often rare, so a system can show high overall accuracy while still mishandling edge cases.
- Undefined acceptable variation: If “good” parts include normal cosmetic, dimensional, or material variation, the model must learn that variation explicitly.
- Metric selection: Accuracy alone is not enough. Teams need precision, recall, false positive rate, false negative rate, and confusion matrices segmented by defect type.
This is particularly relevant in advanced manufacturing sectors such as precision machining, electronics assembly, aerospace subcomponents, and sensor validation workflows. For example, a machine vision system checking machined edges may classify harmless burr-shadow contrast as a defect. A LiDAR-based dimensional validation process may misinterpret sparse point cloud regions caused by angle or reflectivity. An industrial IoT-driven predictive quality workflow may trigger rejection from correlated anomalies that are not causally tied to part failure.
The lesson is simple: performance claims must be tied to the operating window that matters to your process.
Where good parts are most likely to be misclassified
False rejects tend to cluster around specific technical conditions. These are the scenarios where even advanced systems need careful engineering controls:
- Near-threshold dimensional variation: Especially in 5-axis CNC machining, molded parts, and tight-tolerance assemblies.
- Reflective, transparent, or textured surfaces: Common in polished metals, coated parts, glass, and composite materials.
- Variable ambient conditions: Heat, dust, vibration, and line-speed changes affect image consistency and sensor reliability.
- Mixed-model production: Frequent SKU changes can expose weaknesses in classification logic or recipe switching.
- Cosmetic vs functional ambiguity: The system may reject visual anomalies that have no effect on product performance.
- Incomplete golden sample libraries: Acceptable variation is not fully represented in the reference set.
These failure modes matter because they show that inspection is not only about defect sensing. It is about translating engineering intent into a stable decision system.
How to reduce false rejects without letting bad parts escape
The best-performing manufacturers do not solve false rejects by simply loosening all limits. They reduce false positives while preserving true defect capture through a layered approach.
1. Start with functional criticality, not visual perfection.
Separate defects into categories: safety-critical, fit-critical, performance-critical, cosmetic, and non-issues. Inspection strictness should follow actual use risk.
2. Validate tolerances against process capability.
If the inspection system is routinely rejecting parts inside a stable and functionally acceptable production window, the issue may be the threshold strategy rather than the process itself.
3. Improve the “good part” dataset.
For AI and machine vision systems, many teams spend too much time labeling bad parts and too little time modeling acceptable variation. Good-part diversity is essential.
4. Stabilize image and sensor acquisition.
Control lighting geometry, exposure, fixture repeatability, part position, line timing, and environmental drift. Better raw data often reduces false alarms more than algorithm changes.
5. Use confidence-based review layers.
Not every uncertain detection should trigger automatic scrap. A confidence threshold with secondary review can be more economical, especially for high-value parts.
6. Segment rules by defect type and product family.
A single universal pass/fail model is rarely optimal across all materials, finishes, geometries, and SKU variants.
7. Track false reject rate as a core KPI.
Do not evaluate system performance using escaped defects alone. Monitor false positive trends by shift, product, supplier lot, and environmental condition.
8. Close the loop with upstream process data.
Integrate SPC, machine parameters, edge AI analytics, and inspection outcomes. This helps distinguish real quality drift from sensing noise.
What buyers and decision-makers should ask before selecting a defect detection system
If you are evaluating vendors, system integrators, or in-line inspection platforms, the right questions can prevent expensive deployment mistakes.
Ask for evidence in these areas:
- False reject performance: What percentage of acceptable parts are rejected in real operating conditions?
- Application-specific validation: Was the system tested on your material, surface condition, tolerance band, and cycle time?
- Measurement system limits: What is the minimum detectable feature size, repeatability, and gauge capability?
- Environmental robustness: How does performance change with temperature, contamination, vibration, or lighting drift?
- Recipe and changeover control: How reliable is the system in mixed-model manufacturing?
- Data traceability: Can each reject be traced back to image data, sensor readings, and decision logic?
- Human review workflow: Is there an efficient process for reclassification and model improvement?
- Lifecycle support: How often does the model need retraining, recalibration, or optics maintenance?
For procurement teams, this moves the discussion away from vague claims like “smart AI inspection” and toward verifiable engineering performance. For enterprise leaders, it provides a more realistic basis for ROI forecasting and supplier qualification.
A better way to think about inspection performance
A defect detection system should not be judged only by how aggressively it finds anomalies. It should be judged by how reliably it distinguishes meaningful defects from acceptable variation under real production conditions.
That distinction matters across industries—from aerospace structures and electronics assembly to machine vision inspection, solid-state LiDAR validation, and industrial edge AI quality control. Good systems do more than detect. They classify consistently, trace decisions clearly, and align with the economics of manufacturing.
If your current system keeps missing good parts, the answer is usually not to abandon automation. It is to tighten the engineering logic around data quality, tolerance design, validation metrics, and process integration.
In the end, the question is not whether a system can see a difference. It is whether it understands which differences matter.
For manufacturers, operators, buyers, and decision-makers, that is the standard that turns inspection technology from a cost center into a reliable source of process truth.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























