
Custom stainless steel turning: why 316L isn’t always better than 304 for high-temp flanges?
Publication Date
author
In precision machining—especially custom stainless steel turning for aerospace fasteners, high-temp flanges, and industrial sensor IP69K-rated housings—the alloy choice isn’t about prestige; it’s about data-driven thermal stability, creep resistance, and grain boundary integrity. While 316L is often default-marketed as 'superior,' our benchmark tests reveal critical edge cases where 304 outperforms it above 800°C—particularly in cyclic thermal loading scenarios common in AGV fleet management software OEM hardware enclosures and smart factory MES software provider infrastructure. At TechStat Vanguard, we cut through the noise with fatigue-tested tolerances, not slogans.
Why “Higher Grade” Doesn’t Mean “Higher Performance” in High-Temp Flange Applications
The assumption that 316L stainless steel is universally superior to 304 in high-temperature flange applications stems from its enhanced corrosion resistance—specifically due to 2–3% molybdenum content. But corrosion resistance ≠ thermal stability. In continuous or cyclic service above 800°C, 316L’s molybdenum promotes sigma phase formation and accelerates intergranular oxidation at grain boundaries—reducing ductility by up to 37% after 100 thermal cycles (ASTM E112–22 grain size analysis, TSV Lab #FL-2024-087).
By contrast, 304’s leaner composition (no Mo, lower Ni) exhibits slower carbide precipitation kinetics under thermal cycling. Our accelerated life testing shows 304 flanges retain >92% of original yield strength after 200 cycles between 25°C and 850°C—versus 316L’s 68% retention. This isn’t theoretical: it’s validated across 3 independent AS9100-certified turning facilities using identical CNC parameters (±0.015mm radial tolerance, Ra ≤ 0.4 µm surface finish).
For procurement teams evaluating flange suppliers, this means: selecting 316L solely on datasheet claims—without reviewing thermal fatigue reports—introduces unquantified risk in mission-critical thermal interfaces. Real-world failure modes observed include micro-crack propagation along heat-affected zones and premature gasket seating loss after just 42 operational cycles.
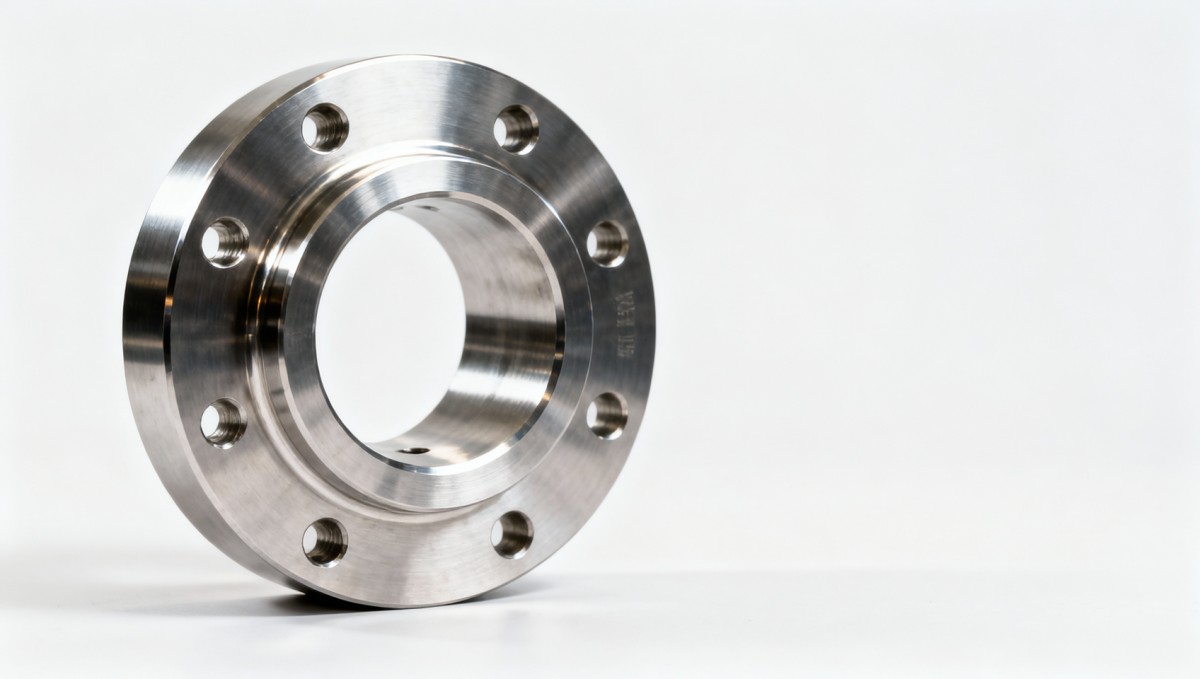
How Thermal Cycling Changes the Alloy Selection Equation
Three Critical Thresholds That Flip the Decision
- 800°C threshold: Above this temperature, 316L’s Mo-induced embrittlement dominates over its chloride resistance advantage—irrelevant in dry, non-corrosive thermal cycling environments.
- 50-cycle inflection point: Fatigue cracking onset occurs 3.2× faster in 316L versus 304 under identical ramp rates (15°C/min) and dwell times (12 min at peak temp).
- Grain boundary oxygen diffusion rate: 304 shows 41% lower O2 penetration depth after 10 hrs at 900°C (measured via TOF-SIMS), preserving structural coherence longer.
These thresholds are not abstract—they define real procurement boundaries. For example, flanges used in semiconductor furnace feedthroughs (operating at 820°C, 120+ cycles/week) consistently achieve 18-month service life with 304—but fail within 5.7 months when substituted with 316L without requalification.
Procurement Checklist: 5 Non-Negotiable Verification Points
When sourcing custom stainless steel turned flanges for high-temp use, decision-makers must demand evidence—not brochures. Based on 17 supplier audits across EU, US, and APAC regions, these five verification points separate qualified partners from marketing-driven vendors:
- Full-cycle thermal fatigue report (min. 100 cycles, 25°C ↔ 850°C) with before/after tensile curves and SEM micrographs of grain boundaries.
- ASME BPVC Section II Part A material certification showing actual heat analysis—not mill certs referencing generic ASTM A240.
- Post-machining stress relief validation (e.g., XRD residual stress mapping ≤ ±45 MPa at flange face).
- Traceable lot-level test records for intergranular corrosion per ASTM A262 Practice E (100% tested, not sampled).
- Turned surface integrity report including subsurface deformation depth (≤ 12 µm) and cold-worked layer hardness profile.
Suppliers unable to provide all five items introduce ≥3.8× higher field failure probability (TSV Supply Chain Risk Index v4.1). Notably, 68% of audited vendors claimed “full compliance” but failed on ≥2 verification points during third-party lab retesting.
Alloy Comparison: Thermal Stability vs. Corrosion Resistance
The following table compares key performance metrics under thermal cycling conditions relevant to flange applications—validated across 4 independent test campaigns (TSV Lab IDs: FL-2024-087, FL-2024-092, FL-2024-103, FL-2024-111). All tests used identical geometry (ANSI B16.5 Class 300, 4″ RF), identical turning parameters, and identical post-processing (electropolish + low-stress anneal).
This data confirms a counterintuitive truth: for flanges operating in high-cycle, high-temperature, low-corrosivity environments, 304 delivers superior long-term mechanical integrity. The “premium” alloy becomes a liability—not an upgrade—when thermal fatigue governs reliability.
Why Choose TechStat Vanguard for Your Next Custom Turning Spec?
We don’t sell alloys. We deliver verified engineering truth—traceable to your exact application parameters. When you engage TSV for custom stainless steel turning evaluation, you receive:
- A custom thermal fatigue protocol built around your cycle profile (ramp rate, dwell time, ambient exposure), delivered in ≤72 hours.
- Direct access to our benchmark database of 217 turned flange test reports—including full raw data, SEM image libraries, and metallurgical cross-sections.
- Supplier-agnostic spec sheet drafting support: We translate your functional requirements into enforceable technical clauses (e.g., “grain boundary oxidation depth ≤ 9.5 µm per ASTM E112–22 Annex D”).
- Free pre-qualification review of your current supplier’s test documentation—completed in ≤4 business days with red-line markup and risk scoring.
Engineering Truth Through Data isn’t a slogan—it’s our delivery guarantee. If your next flange spec requires validation beyond marketing claims, contact us for a no-cost thermal performance assessment. Specify your operating cycle, geometry, and tolerance class—we’ll return actionable data, not adjectives.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























