
5-Axis CNC Machining Titanium Alloys Without Burning Tool Life
Publication Date
author
In aerospace machining process optimization, few challenges are tougher than 5-axis CNC machining titanium alloys without sacrificing tool life, dimensional stability, or surface integrity. This guide cuts through generic advice to examine precision machining dimensional accuracy control, real-world heat management, and proven process strategies that help engineers, buyers, and manufacturing leaders machine titanium faster, safer, and more predictably.
Why does 5-axis CNC machining titanium alloys destroy tools so quickly?
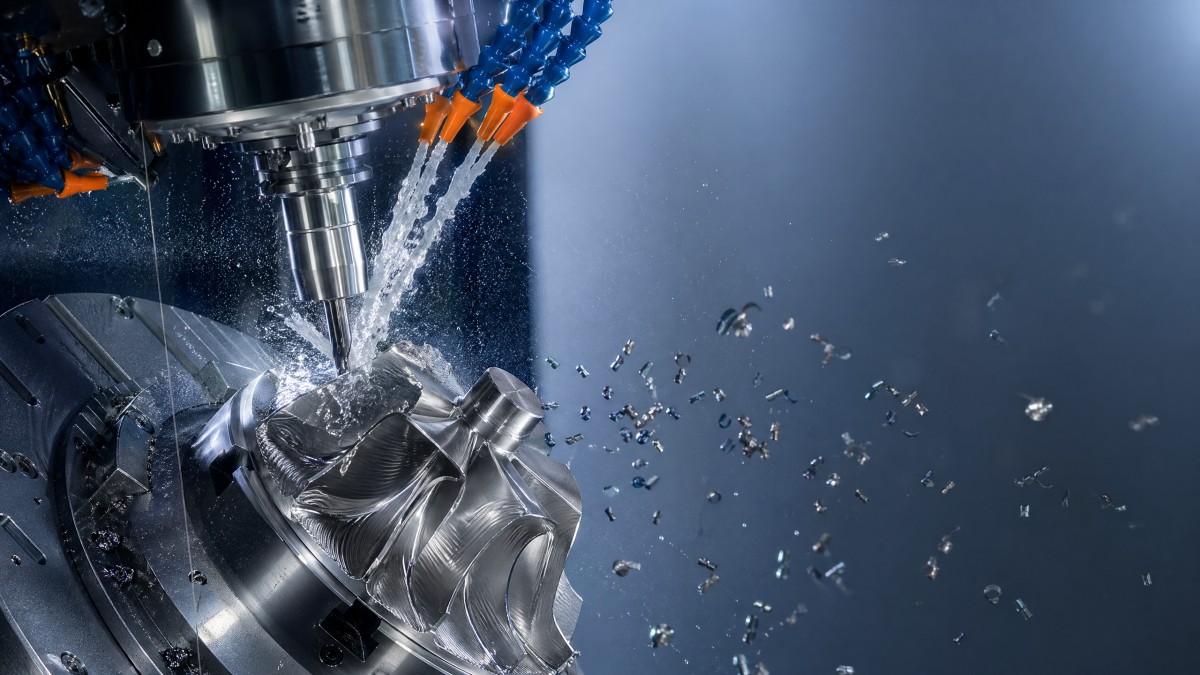
Titanium is not difficult because it is simply “hard.” The real issue is its low thermal conductivity, high chemical reactivity at the cutting zone, and tendency to keep heat concentrated at the tool edge. In 5-axis CNC machining titanium alloys, that means the cutter often absorbs a large share of the thermal load instead of the chip carrying it away. Once edge temperature rises beyond a stable window, flank wear, crater wear, notch wear, and micro-chipping accelerate fast.
For operators, this appears as a familiar pattern: the first few parts look acceptable, then surface color changes, burr formation increases, and tool life collapses before the batch is complete. For procurement teams, the hidden cost is not only carbide consumption. The larger risk is scrap, schedule drift, spindle idle time, and unplanned process adjustments across 2–4 production shifts.
In aerospace and medical-grade work, common titanium families such as Ti-6Al-4V demand stable control of cutting speed, chip thickness, radial engagement, and coolant delivery. A small mismatch between toolpath strategy and machine dynamics can create chatter, recutting, and heat spikes within minutes. On thin-wall parts, the same instability also causes dimensional drift in the range of tens of microns, which matters when tolerance bands move toward ±0.01 mm to ±0.05 mm.
TSV’s engineering-first view is simple: if a supplier says they machine titanium efficiently, ask how they control heat, runout, tool engagement, and in-process verification. General claims are not enough. Parameters, thresholds, and repeatability windows are what separate a stable titanium machining cell from a tool-burning one.
The four root causes most shops underestimate
- Excessive heat concentration at the cutting edge because chip evacuation and coolant access are restricted in deep pockets or closed-angle 5-axis positions.
- Unstable radial engagement caused by poor CAM strategy, especially when toolpaths alternate between light skimming and sudden full-width entry.
- Tool assembly error, including holder imbalance, runout above practical process limits, or overhang that reduces stiffness during long-reach machining.
- Machine-tool mismatch, where spindle torque, coolant pressure, rotary axis smoothness, and look-ahead control do not support continuous titanium cutting.
When these four factors interact, tool life does not decline gradually. It often falls off a cliff. That is why titanium process planning should be treated as a system problem rather than a simple feeds-and-speeds problem.
Which process variables matter most for heat, tool life, and dimensional accuracy?
In practical 5-axis CNC machining titanium alloys, three priorities dominate process stability: thermal control, engagement consistency, and machine-tool rigidity. Shops that focus only on spindle speed often miss the real source of failure. A lower cutting speed does not automatically save tool life if chip thinning, step-over, or axial depth are poorly balanced.
For information researchers and technical buyers, the best way to compare suppliers is to ask for the process window they can hold across roughing, semi-finishing, and finishing. A serious supplier should discuss at least 3 process stages, explain why different flute geometries are used, and show how coolant strategy changes between open surfaces and deep cavities.
The table below summarizes common process variables that influence tool life and precision machining dimensional accuracy control. These are not fixed recipe values, because alloy condition, machine power, holder type, and geometry all matter. However, they are reliable evaluation dimensions for supplier qualification and internal process review.
The key takeaway is that no single parameter rescues a weak process. Titanium responds best when the entire cutting system is tuned. If one supplier can explain this interaction clearly and another only offers a price per part, the first one is usually lower risk over a 20-piece validation lot or a 200-piece qualified batch.
How to think about roughing, semi-finishing, and finishing
Roughing should prioritize controlled material removal and predictable thermal behavior. High-efficiency strategies with light radial engagement often outperform traditional slotting because they lower peak tool load. In titanium, constant engagement matters more than aggressive headline metal removal rates.
Semi-finishing is where many quality issues start. If residual stock becomes uneven, finishing passes must absorb variation, which pushes a light tool into unstable load conditions. On complex aerospace contours, leaving consistent stock can be more important than shortening cycle time by 5–8%.
A practical control sequence
- Confirm machine condition, spindle health, holder selection, and tool overhang before programming begins.
- Use CAM strategies that maintain smooth engagement and minimize abrupt direction changes on rotary axes.
- Verify residual stock after roughing, then adjust semi-finishing to equalize finishing load.
- Monitor wear by tool class and feature type rather than replacing all tools on a fixed time rule.
For decision-makers, this sequence is useful because it turns titanium machining capability into auditable checkpoints instead of vague supplier promises.
How should buyers compare suppliers for 5-axis CNC machining titanium alloys?
Procurement errors often come from comparing quotes without comparing process risk. A low quoted part price can hide expensive instability: short tool life, frequent setup corrections, inconsistent first article results, or poor repeatability between shifts. For titanium alloy parts, especially those used in aerospace, UAV, robotics, and medical-adjacent systems, buyers should evaluate process depth, not marketing language.
A useful procurement model is to score suppliers across 5 core dimensions: machine capability, process engineering, quality control, documentation discipline, and communication responsiveness. If a supplier cannot explain how they manage distortion, in-process inspection, and tool wear tracking, it is difficult to trust their delivery promise even if their sample looks good.
The following comparison table helps teams review candidate suppliers in a structured way. It is especially helpful during RFQ review, new supplier qualification, or transition from prototype to serial production over a 4–12 week sourcing cycle.
For enterprise decision-makers, the strongest signal is disciplined transparency. Suppliers who openly discuss tolerance stack-up, wall thickness sensitivity, and process limits are usually more reliable than those who claim they can do everything without constraints.
What procurement teams should ask before issuing a PO
- What tolerance bands are critical, and which features require in-process verification rather than end-of-line inspection only?
- What is the expected lead time for prototype, pilot batch, and repeat batch orders, such as 7–15 days for prototypes or 2–6 weeks for more complex series work?
- How is tool wear monitored on titanium parts with long cycle times or thin-wall features?
- Can the supplier support documentation commonly requested in regulated or aerospace-adjacent supply chains?
These questions improve sourcing accuracy and shorten supplier qualification cycles, which fits TSV’s core mission: replacing vague claims with measurable engineering truth.
Which standards, risks, and common misconceptions deserve attention?
Titanium parts often sit inside high-consequence applications. That does not mean every project needs the same certification path, but it does mean buyers should align machining expectations with the end-use sector. In aerospace-related programs, AS9100-aligned quality systems may matter. In medical-device-adjacent supply chains, ISO 13485-related documentation discipline may influence supplier screening even when the machining scope itself is only one step in the manufacturing chain.
A common misconception is that slower cutting automatically protects tools. In reality, overly conservative settings can increase rubbing, raise localized heat, and reduce chip evacuation quality. Another misconception is that 5-axis machining alone guarantees better titanium performance. Axis count helps with access and tool orientation, but poor toolpath strategy still causes wear and dimensional instability.
A third mistake is to judge a supplier from one demonstration sample. Titanium machining must be evaluated across repeatability, not a single part. Ask whether the supplier can hold process stability through at least 3 indicators: consistent surface finish, predictable tool wear behavior, and dimensional repeatability across multiple setups or shifts.
For researchers and operators, the practical lesson is clear: stable titanium machining is built on disciplined controls, not heroic last-minute adjustments. That is why TSV emphasizes benchmark thinking, traceability, and parameter-based comparison rather than promotional language.
FAQ: the questions most teams ask
How can I reduce tool wear in 5-axis CNC machining titanium alloys?
Start by stabilizing engagement, holder rigidity, and coolant access. Then review whether roughing and finishing are using the same logic when they should not be. In many shops, tool life improves more from consistent chip load and lower runout than from simply reducing speed by 10–15%.
What should I prioritize: cycle time or tool life?
Prioritize total process economics. A cycle shortened by 8% is not beneficial if tool changes double, scrap rises, or dimensional correction adds inspection time. For titanium, the best process is usually the one with predictable output over the full batch, not the fastest first part.
Are titanium alloy parts always expensive to machine?
They are often cost-sensitive, but not all cost comes from the material. Programming complexity, feature accessibility, tolerance level, wall thickness, documentation requirements, and batch size all affect the final price. A well-engineered process can reduce hidden cost even if the hourly machine rate is higher.
How do I validate a machining supplier before full production?
Use a staged approach: technical review, sample part, pilot batch, then scaled release. During validation, examine 4 items closely: dimensional repeatability, surface integrity, documentation accuracy, and responsiveness to engineering change requests.
Why consult TSV when evaluating titanium machining capability?
TechStat Vanguard exists for teams that need engineering truth rather than sales adjectives. In precision machining benchmarks, that means focusing on tolerance logic, thermal behavior, process repeatability, and supply-chain credibility. If you are comparing 5-axis CNC machining titanium alloys across suppliers, countries, or quality tiers, the real challenge is not finding claims. It is filtering noise and identifying which claims are technically defensible.
TSV supports that decision process with a data-driven mindset shaped by advanced manufacturing, aerospace systems, automation, and hard-tech sourcing realities. We look at the questions technical teams and procurement leaders actually need answered: Which parameters matter? Which tolerances are realistic? Which supplier statements are measurable? Which process risks should be escalated before RFQ approval?
If your organization is qualifying a new titanium machining partner, optimizing an existing process, or preparing a sourcing package for complex 5-axis components, contact TSV for structured support. You can consult on parameter confirmation, supplier comparison criteria, tolerance review, process risk checkpoints, likely lead-time ranges, documentation expectations, sample evaluation logic, and custom benchmarking needs for aerospace, UAV, robotics, or other precision manufacturing programs.
The most valuable conversations usually begin before production trouble starts. Bring your drawing package, material grade, annual volume estimate, quality requirements, and target delivery window. TSV can help you turn those inputs into a sharper technical brief, a stronger procurement framework, and a more confident decision path grounded in data.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























