
Surface Finish Standards in Precision Machining Are Often Misread
Publication Date
author
In precision machining, surface finish standards are often misunderstood, leading to costly errors in precision machining dimensional accuracy control, supplier qualification, and aerospace machining process optimization. For engineers, buyers, and decision-makers, knowing how precision machining surface finish standards actually relate to function, tolerance, and inspection is essential to evaluating 5-axis CNC machining titanium alloys and other critical components with confidence.
This misunderstanding is not a minor documentation issue. In hard-tech procurement, a drawing callout such as Ra 0.8 μm, Rz 3.2 μm, or “32 microinch” can directly affect machining time, tooling strategy, inspection cost, coating performance, fatigue life, and supplier acceptance criteria. When surface finish standards are read loosely, even a part that looks visually excellent may fail its functional requirement or create hidden downstream risk.
For TSV’s audience—research teams, operators, sourcing managers, and executive decision-makers—the priority is not marketing language but technical clarity. Surface roughness must be interpreted together with material, geometry, process route, tolerance stack-up, and end-use environment. That is especially true in aerospace, medical, automation, and UAV supply chains, where a misread finish requirement can add 15%–40% to cycle time or trigger expensive rework after final inspection.
The sections below break down what surface finish standards actually mean, where the most common errors occur, how those errors affect precision machining benchmarks, and what procurement teams should verify before releasing RFQs or approving first articles.
Why Surface Finish Standards Are Commonly Misread
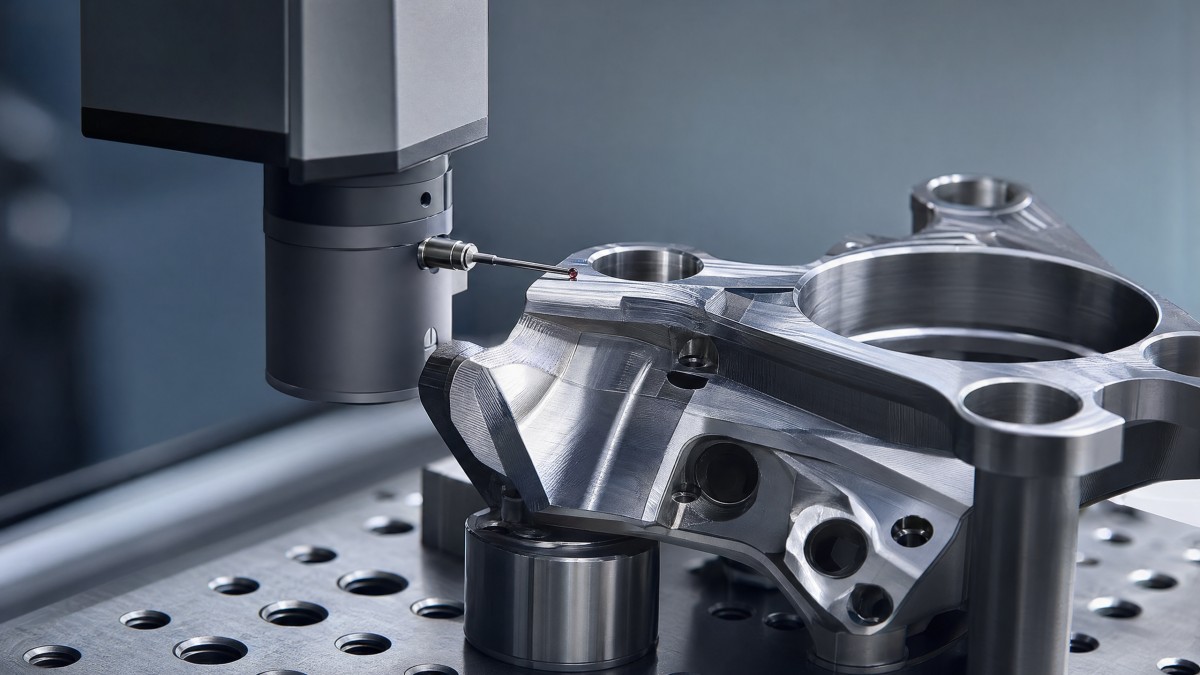
Surface finish is often treated as a simple number on a print, but in reality it is a measurement framework. A roughness value only becomes meaningful when the standard, parameter type, sampling length, measurement direction, and manufacturing method are understood together. Confusion starts when teams assume that all roughness values describe the same thing.
One of the most frequent mistakes is mixing Ra, Rz, and Rt as if they are directly interchangeable. They are not. Ra is an arithmetic average, while Rz focuses on peak-to-valley characteristics over selected sampling lengths. A part that meets Ra 0.8 μm may still miss an Rz-based acceptance requirement if the surface contains isolated peaks or valleys from chatter, tool wear, or unstable feeds.
Another source of error is unit confusion. Global supply chains still exchange drawings in both metric and inch-based conventions, such as Ra 1.6 μm versus 63 µin. These are close in intent but not identical if a supplier uses a different conversion assumption or references a different measurement setup. In cross-border sourcing, that mismatch can delay first article approval by 3–7 days and trigger repeat metrology.
Interpretation also changes by process. A turned shaft, 5-axis milled titanium bracket, ground sealing face, and additively manufactured near-net-shape part do not generate the same surface texture signature. The nominal number may be the same, but the waveform pattern, lay direction, and functionality can be very different. This is why finish standards should never be evaluated in isolation from process capability.
In high-value sectors such as aerospace and advanced robotics, teams also overlook the interaction between surface finish and tolerance. Tight dimensional control such as ±0.01 mm or ±0.005 mm often requires more stable toolpaths, lower vibration, and secondary finishing steps. If a buyer requests a very fine finish without clarifying which surfaces are function-critical, the quote may be padded with unnecessary polishing, grinding, or lapping operations.
Three recurring interpretation gaps
- Drawing symbols are copied from older prints without verifying whether the parameter is still functionally required.
- Inspection teams measure across the wrong lay direction, producing values that differ by 20%–50% from the intended reading.
- Procurement documents specify a finish number but omit the governing standard, cutoff length, or measurement method.
What the symbols usually need to communicate
A well-defined callout should answer at least four questions: which parameter is being used, what limit applies, where on the part it applies, and how it will be verified. If even one of those four points is missing, interpretation risk rises sharply. In complex programs with 20–100 machined features per part, that ambiguity multiplies across the whole qualification package.
How Surface Finish Relates to Function, Tolerance, and Process Capability
Surface finish matters because it influences how a part actually performs, not just how it appears. A finer finish may improve sealing, reduce friction, stabilize bearing contact, or support fatigue performance. But a finer finish is not always better. On bonded surfaces, overly smooth profiles can reduce mechanical keying. On some lubricated systems, a controlled texture can retain oil more effectively than a mirror-like surface.
In precision machining dimensional accuracy control, finish and tolerance interact in practical ways. If a 5-axis CNC titanium component holds a flatness requirement of 0.02 mm and a surface finish of Ra 0.4 μm on the same datum face, the process window is narrower than for a part needing Ra 3.2 μm. Tool wear, thermal drift, machine rigidity, and cutter engagement all become more critical as the combined requirement tightens.
This is especially relevant for titanium alloys such as Ti-6Al-4V, which tend to generate heat and can accelerate tool wear. In practical shop conditions, an as-milled finish may fall around Ra 1.6–3.2 μm depending on toolpath, spindle speed, and step-over. Achieving Ra 0.8 μm or lower repeatedly may require optimized finishing passes, high-stability toolholders, fresh inserts, and in some cases grinding or polishing after machining.
The same logic applies to aerospace machining process optimization. If the function is aerodynamic flow, sealing contact, or fatigue resistance at high-cycle loading, the finish requirement must align with that functional mechanism. If the callout is driven only by legacy habit, then cycle time can increase by 10%–30% with little measurable engineering benefit. Data-driven benchmarking helps separate necessary finish control from decorative overprocessing.
Below is a practical comparison that helps engineering and sourcing teams distinguish surface finish levels by likely process effort and application impact.
The key conclusion is that finish requirements should be specified by function tier, not by habit. If only 2 out of 12 surfaces on a part truly need Ra 0.8 μm, then applying that limit globally increases cost without improving the final assembly. This is one of the clearest opportunities for RFQ refinement and supplier alignment.
A practical decision sequence
- Identify whether the surface is structural, sealing, sliding, bonded, or cosmetic.
- Match the finish requirement to the functional risk of that surface.
- Check whether the specified finish is achievable within the target tolerance and material condition.
- Confirm whether the selected supplier can measure and document the requirement consistently.
Inspection and Measurement: Where Acceptance Problems Usually Begin
Even when the drawing intent is technically sound, inspection often introduces the next layer of misunderstanding. Surface finish values depend on measurement setup. A profilometer reading can shift meaningfully depending on cutoff length, stylus radius, filter setting, and trace direction. For a buyer reviewing supplier capability, asking only “Can you hold Ra 0.8?” is not enough. The more useful question is, “How do you measure, document, and repeat Ra 0.8 across this geometry?”
Measurement access is a major issue on complex 5-axis parts. Deep pockets, blended radii, thin webs, and compound curves are not always suitable for simple stylus access. In those cases, the supplier may rely on process validation, representative coupons, specialty probes, or optical methods. If the RFQ and control plan do not define this early, disputes often appear at PPAP, FAI, or final source inspection.
Another problem is overreliance on visual appearance. A uniform sheen can mislead teams into assuming the finish is acceptable. In reality, chatter marks, smeared material, recast layers after secondary processing, or embedded contamination may still create unacceptable surface conditions. On fatigue-sensitive aerospace components, those defects matter far more than a polished look.
Consistency across lots is equally important. A supplier may produce 3 acceptable samples but struggle to hold the same finish across a 50-part batch when tool wear accumulates. For titanium, nickel alloys, and hard stainless steels, tool life variation can change surface roughness sharply near the end of a cutter cycle. That is why inspection plans should include both first-piece verification and periodic in-process checks.
Key verification items before acceptance
The following table summarizes what engineering and procurement teams should verify before approving a supplier’s finish capability or rejecting a lot based on a roughness reading.
The main lesson is simple: finish inspection is a system, not a spot check. When the standard, instrument method, and access strategy are aligned early, qualification becomes faster and rejection rates usually fall. For high-mix, low-volume precision machining programs, that alignment can save one full review loop per drawing revision.
Inspection planning for critical programs
- Define which surfaces are 100% inspected and which are sampled at fixed intervals such as every 5 or 10 parts.
- Use representative witness coupons when direct access is impossible but process equivalence can be demonstrated.
- Document the instrument type, trace direction, and acceptance rule in the control plan before pilot production.
Supplier Qualification and RFQ Strategy for Precision Machining Surface Finish Standards
From a sourcing perspective, misread surface finish standards usually appear long before production starts. They often begin at the RFQ stage, where drawings are shared without adequate notes, process context, or functional prioritization. A supplier then quotes defensively, adds hidden process buffers, or assumes a finish interpretation that later conflicts with customer expectations. This can distort both price and lead time from day one.
A strong RFQ package should separate critical surfaces from general surfaces. It should also identify any material-specific risks, such as titanium galling, thin-wall vibration, or post-machining treatments like anodizing, passivation, or coating. These downstream steps can change apparent surface condition and sometimes alter the effective functional result. If they are not discussed, the finish requirement may be verified at the wrong process stage.
Supplier qualification should assess both machining capability and metrology maturity. A shop may have excellent 5-axis machines but limited roughness measurement discipline. Another may measure accurately but struggle to hold fine finishes over long cycle runs. The right decision is rarely based on equipment count alone. It depends on process control, inspection repeatability, and openness in communicating capability limits.
For enterprise decision-makers, the cost impact can be significant. Over-specified finish requirements can increase quoted pricing by 8%–25% depending on material and geometry. Under-specified finish requirements can create field risk, warranty exposure, or failed validation testing. A balanced supplier strategy therefore requires engineering review, procurement discipline, and realistic acceptance planning.
RFQ checkpoints that reduce interpretation risk
- State the governing roughness parameter and unit system clearly on the drawing and in the RFQ notes.
- Mark function-critical surfaces separately from default shop-finish surfaces.
- Indicate whether finish is required before or after coating, blasting, polishing, or cleaning operations.
- Request sample inspection reports during supplier qualification, not after award.
- Ask for typical achievable finish ranges by material: aluminum, stainless steel, titanium, and hardened alloys.
Procurement evaluation framework
The table below offers a practical supplier screening structure for buyers managing precision machining programs with finish-sensitive components.
This framework helps turn supplier qualification into an engineering-based filter. For organizations sourcing across multiple regions, it also creates a common language between procurement, quality, and design teams. That alignment is one of the fastest ways to reduce qualification cycles without lowering technical standards.
Common Misconceptions, Implementation Advice, and FAQ
The most expensive misconception is that a lower roughness number automatically means a better part. In reality, “better” depends on function. If the requirement is not function-driven, teams may pay for unnecessary finishing, prolong lead times by 2–10 days, and still miss the real performance variable. Another misconception is that a roughness callout alone guarantees fatigue quality; it does not. Residual stress, micro-notches, burr control, and edge condition also matter.
Implementation should begin with drawing discipline. Review each surface finish requirement during design release or print revision, especially on aerospace brackets, UAV structural nodes, sensor housings, and medical-adjacent precision parts. If only a few surfaces are critical, localize the specification. If the part requires multiple finish zones, define them clearly with notes, views, or feature-based symbols to avoid shop-floor assumption.
For operators and manufacturing engineers, process planning should connect finish targets to machine condition, cutter type, feed per tooth, step-over, coolant strategy, and expected tool life. For buyers, the practical task is to verify whether quoted capability reflects stable production or only best-case sample performance. Those two realities are often very different.
FAQ: How should buyers choose between “standard shop finish” and tighter finish callouts?
Start with function, not appearance. If the feature is non-contact, hidden after assembly, and not fatigue-sensitive, a general finish such as Ra 3.2 μm may be fully sufficient. If it is a sealing, bearing, or flow-critical surface, review whether Ra 0.8–1.6 μm is necessary. Requiring a fine finish on every face usually inflates cost without proportional value.
FAQ: Can the same finish target apply equally to aluminum, stainless steel, and titanium?
No. The same nominal target may demand very different process effort by material. Aluminum often reaches fine milled finishes more easily than titanium or heat-resistant alloys. Titanium may need more conservative parameters and more frequent tooling changes. Buyers should ask for material-specific capability ranges instead of assuming one universal finish rule.
FAQ: When should a roughness requirement be measured before coating versus after coating?
That depends on function. If the coating is part of the working surface, post-coating verification may be necessary. If the machining process itself is the controlled variable, pre-coating measurement may be more meaningful. The requirement should state the inspection stage explicitly, because coating thickness and texture can change the reported value.
FAQ: What are the top warning signs during supplier review?
- The supplier confirms a finish target without asking which parameter or where it applies.
- No one can explain how the value is measured on difficult geometry.
- Quoted lead time is unchanged even though the finish requirement became much tighter.
- Inspection reports show values but not method details, units, or trace direction.
Surface finish standards in precision machining are often misread because too many teams treat them as isolated numbers instead of engineering requirements tied to function, process, and verification. The strongest programs define finish by use case, align it with realistic process capability, and verify it with consistent measurement rules. For engineering teams, sourcing leaders, and executives operating in advanced manufacturing, that approach reduces ambiguity, protects performance, and shortens supplier qualification loops.
If your organization is evaluating precision machining partners, refining RFQ standards, or benchmarking 5-axis CNC machining titanium alloys for critical applications, TSV can help you translate specifications into decision-grade technical criteria. Contact us to discuss your component requirements, request a tailored evaluation framework, or learn more about data-driven hard-tech sourcing and manufacturing benchmarks.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























