How to Evaluate Multi Axis Motion Control for Precision Automation Projects
Publication Date
author
How to Evaluate Multi Axis Motion Control for Precision Automation Projects
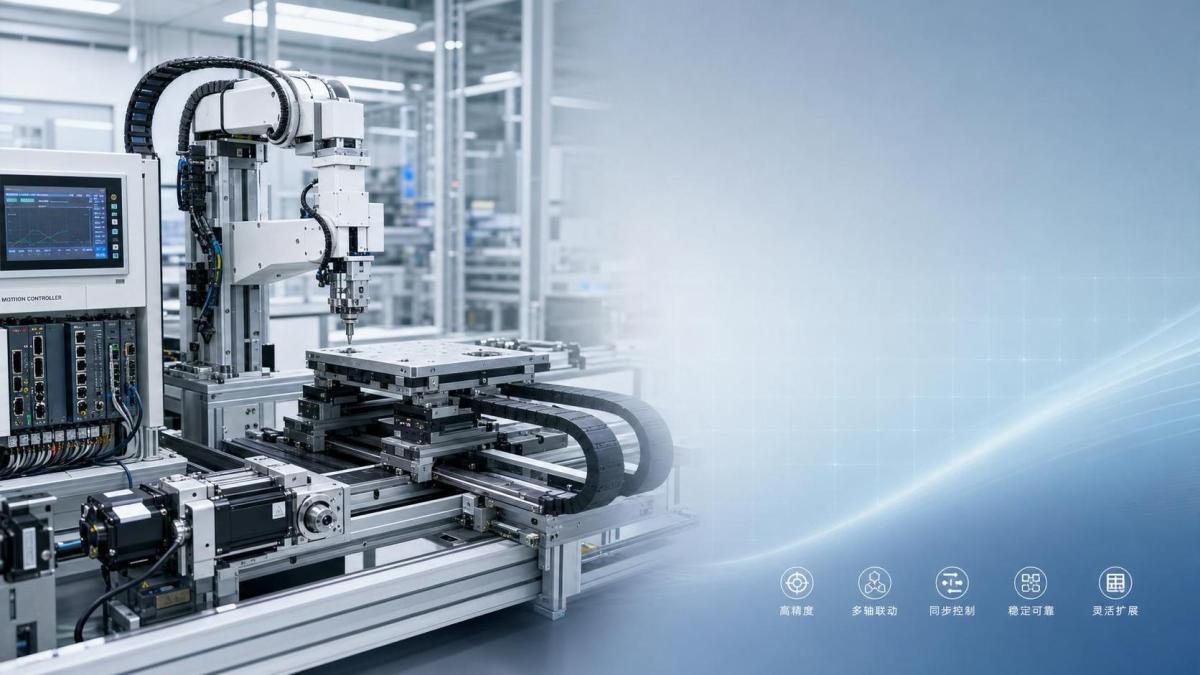
Selecting the right multi axis motion control architecture often decides whether an automation project performs smoothly or stalls after commissioning.
That is why multi axis motion control should be evaluated as a system decision, not just a component purchase.
In real projects, speed claims rarely tell the full story.
What matters more is how the controller, drives, motors, feedback devices, and software behave together under load.
For teams comparing platforms, the smartest approach is to translate performance language into measurable engineering criteria.
That means checking synchronization accuracy, interpolation quality, update rate, safety integration, and future expansion before purchase approval.
This also aligns with the TSV view of engineering truth.
Parameters do not lie, and tolerances always expose weak architecture choices.
Start With Application Reality, Not Vendor Positioning
A strong multi axis motion control evaluation begins with the machine’s actual job.
Pick-and-place, gantry inspection, laser cutting, winding, dispensing, and robotic transfer each stress the control stack differently.
Some applications need ultra-tight contouring.
Others care more about throughput, settling time, or smooth handoff between axes.
Before comparing suppliers, define the core motion profile in plain engineering terms.
- Number of coordinated axes needed now and in later phases
- Required position accuracy and repeatability at the tool center point
- Maximum payload, inertia variation, and center-of-mass shifts
- Motion type, including point-to-point, camming, gearing, or interpolation
- Required cycle time, acceleration profile, and allowable vibration
- Environmental factors such as dust, heat, washdown, or EMI
This step keeps the multi axis motion control decision tied to production risk instead of brochure language.
It also prevents overbuying features that never improve machine output.
Evaluate the Performance Metrics That Actually Matter
Many multi axis motion control platforms look similar until dynamic testing begins.
The key is to review metrics that reveal real machine behavior, not isolated peak values.
Synchronization and interpolation quality
For contouring or coordinated travel, synchronization error matters more than single-axis speed.
Ask how the controller maintains path accuracy during acceleration, deceleration, and abrupt direction changes.
Look for measured contour error, following error, and settling behavior under realistic payload.
Control loop speed and latency
A fast processor alone does not guarantee responsive multi axis motion control.
Check servo update rate, network cycle time, encoder feedback latency, and command execution consistency.
Small delays can become visible in registration, vision alignment, or precision dispensing.
Torque, inertia, and load response
A controller that performs well with a nominal load may struggle with changing product weight or tooling swaps.
Review how the system handles inertia mismatch, peak torque demand, regenerative events, and shock loads.
Repeatability over time
Precision automation is rarely judged on day-one results alone.
The better question is whether multi axis motion control holds repeatability after thermal drift, continuous duty, and maintenance cycles.
Look Beyond Hardware and Review the Full Control Architecture
The most expensive surprises usually appear at the integration stage.
That is why multi axis motion control should be assessed as a complete architecture.
The controller, fieldbus, servo drives, feedback devices, HMI, PLC logic, and safety layer must work as one environment.
In practice, software tools can influence commissioning time as much as motion performance.
- Unified engineering software reduces tuning inconsistency across axes
- Built-in diagnostics shorten troubleshooting during startup
- Simulation tools help validate motion sequences before machine assembly
- Open communication options support vision, MES, and edge analytics integration
- Safety motion functions can reduce panel complexity and certification effort
This is often where data-driven evaluation creates a major advantage.
A platform with average specifications but excellent integration discipline may outperform a faster platform with fragmented tools.
Use a Practical Vendor Assessment Framework
When two systems appear technically close, procurement often moves to commercial comparison too early.
A better path is to score each multi axis motion control option against a weighted decision matrix.
This framework keeps multi axis motion control selection grounded in measurable project outcomes.
It also helps internal teams defend decisions during budget review.
Watch for Common Evaluation Mistakes
Several common mistakes can weaken a multi axis motion control decision even when the shortlist looks strong.
- Using unloaded demonstrations instead of application-specific test conditions
- Comparing peak speed while ignoring path precision and settling time
- Underestimating encoder resolution and feedback quality requirements
- Ignoring cable management, EMI exposure, and thermal behavior
- Treating software licensing and service support as minor details
- Choosing a closed platform that blocks later integration with analytics tools
From recent market shifts, one signal is especially clear.
Automation programs now demand traceable data, not just machine motion.
That means multi axis motion control should also support diagnostics, event history, and performance visibility for continuous improvement.
Build a Decision Process That Survives Real Deployment
The best selection process moves from requirements to proof, then from proof to scale.
A practical roadmap usually works better than a one-time specification review.
- Define critical motion tolerances and productivity targets first
- Shortlist vendors based on architecture fit, not brand familiarity
- Request test data under representative payload and cycle conditions
- Run a pilot or benchmark sequence with measurable acceptance criteria
- Score lifecycle cost, scalability, and support readiness before approval
This process turns multi axis motion control evaluation into a lower-risk engineering decision.
It also reflects the TSV principle that hard-tech decisions should be guided by verified operating truth.
When precision automation projects fail, the cause is often not ambition.
It is usually a gap between claimed capability and validated performance.
A disciplined multi axis motion control review closes that gap before it becomes a production problem.
If the architecture can prove its accuracy, responsiveness, and expandability under real conditions, it is far more likely to deliver stable returns.
Start with the application, challenge every parameter, and let measured data lead the final decision.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Sep 22, 2026Drone Engine-T550CC Applications: Build the UAV Power System Around the MissionAn application guide for Drone Engine-T550CC integration, covering payload planning, airframe matching, cooling, fuel, vibration, test procedures, documentation, and service preparation.Elena Rostova (UAV Systems Researcher)
 Sep 22, 2026How to Evaluate Industrial Edge Computing Vendors for Factory DeploymentIndustrial edge computing vendor evaluation guide for factories: compare latency, protocol fit, reliability, security, and lifecycle support before deployment.TSV Data Lab
 Sep 21, 2026Drone Payload Integration: Matching Power, Data, and Center of Gravity for Reliable FlightsDrone payload integration made practical: balance power, data, center of gravity, and endurance to build safer, more reliable mission-ready flights.Elena Rostova (UAV Systems Researcher)
 Sep 20, 2026Autonomous Navigation Pricing: Cost Drivers and Budget Benchmarks for AMR ProjectsAutonomous navigation price explained: compare AMR cost drivers, software, sensors, integration, safety, and lifecycle budgets to build a scalable project plan.Chen Wei (Automation Lead Engineer)
 Sep 19, 2026How to Scope Automation Integration Services for Multi-System Factory ProjectsAutomation integration services: learn how to scope multi-system factory projects with clear workflows, interface contracts, safety boundaries, and acceptance criteria.Victor Lin (Chief Software Architect)
 Sep 18, 2026Selecting UAV Aerospace Structural Parts for Strength, Weight, and Fatigue LifeUAV aerospace structural parts guide: compare strength, weight, stiffness, fatigue life, joints, and traceability to select reliable flight-ready components.Elena Rostova (UAV Systems Researcher)
 Sep 17, 2026Selecting Commercial Drone Payloads for European Inspection ProjectsCommercial drone payloads Europe: learn how to select RGB, thermal and LiDAR systems for compliant, reliable inspection data and better project outcomes.Elena Rostova (UAV Systems Researcher)
 Sep 16, 2026Machining Tolerance Validation: How to Verify Critical Dimensions Before Production ReleaseMachining tolerance analysis validation: verify critical dimensions, measurement systems, process capability, and tolerance stacks before production release.Dr. Marcus Vance
 Sep 15, 2026AGV Tape Guidance vs Laser Navigation: Which Fits Your Warehouse Layout?AGV tape guidance comparison: discover how tape and laser navigation fit changing warehouse layouts, docking needs, floor conditions, maintenance, and route flexibility.Chen Wei (Automation Lead Engineer)
 Sep 14, 2026How Point Cloud Analytics Improves Asset Inspection Workflows Across GCC ProjectsPoint cloud analytics GCC helps project leaders improve asset inspections with accurate change detection, safer workflows, and faster maintenance decisions.TSV Data Lab
 Sep 13, 2026How Aerospace Manufacturers Can Build a Digital Thread From Design to Certified ProductionDigital manufacturing for aerospace: learn how to build a traceable digital thread from design through certified production, supplier control, and audit-ready compliance.Victor Lin (Chief Software Architect)
 Sep 12, 2026How to Select a Thermal Sensor for Mapping Drones in Surveying ProjectsMapping drone thermal sensor selection made simple: compare GSD, radiometric data, NETD, calibration, and workflow fit for accurate, survey-ready thermal maps.Elena Rostova (UAV Systems Researcher)
 Sep 11, 2026Integrating Photogrammetry Workflows into Digital Twin Projects Without Data BottlenecksPhotogrammetry workflow integration for digital twins: learn how to streamline capture, validation, versioning, and delivery to prevent data bottlenecks.Victor Lin (Chief Software Architect)
 Sep 10, 2026Hard-Tech Supply Chain Procurement: Qualifying Suppliers to Cut Lead-Time RiskHard-tech supply chain procurement guide: qualify suppliers with proven process, traceability, capacity, and change control to reduce lead-time risk.Chen Wei (Automation Lead Engineer)
 Sep 09, 2026Industrial Application Notes: Cost Factors That Shape Automation Project BudgetsIndustrial application notes cost factors explained: uncover the engineering, safety, integration, and commissioning variables that shape accurate automation budgets.Victor Lin (Chief Software Architect)
 Sep 08, 2026Supplier Discovery for Sourcing: How Buyers Can Verify Capability and Supply RiskSupplier discovery for sourcing: learn how to verify supplier capability, traceability, quote assumptions, and supply risk before placing production orders.TSV Data Lab
 Sep 07, 2026What Determines Process Control Systems Pricing? A Buyer’s Cost GuideProcess control systems pricing explained: compare hardware, engineering, integration, cybersecurity, validation, and lifecycle costs to choose the right-value solution.Victor Lin (Chief Software Architect)