
Hard-Tech Supply Chain Procurement: Qualifying Suppliers to Cut Lead-Time Risk
Publication Date
author
A late component delivery rarely begins with a missed shipment. In hard-tech procurement, the failure often starts months earlier when a supplier is approved on the strength of a quotation, a polished capability deck, or a generic certificate list. The part may look manufacturable, the quoted lead time may appear acceptable, and the supplier may have passed a basic commercial screen—yet the first production order exposes an unverified process, constrained material access, or weak change control.
The practical answer is to qualify suppliers against the risks that can interrupt production: process capability, controlled capacity, material and sub-tier traceability, quality-system scope, and the supplier’s ability to communicate deviations before they become delays. Hard tech supply chain procurement should treat lead time as an engineering outcome, not merely a number printed on a quote. A supplier can only sustain its stated lead time when its manufacturing route, inspection resources, critical inputs, and approval workflow are all understood and evidenced.
Why quoted lead times fail after supplier approval
Precision components, automation assemblies, aerospace structures, sensor housings, and edge-computing hardware often have hidden dependencies. A supplier may machine the main part in-house but outsource heat treatment, coating, PCB assembly, non-destructive inspection, or final calibration. Each outside process introduces another queue, logistics handoff, and documentation requirement. If those dependencies are not mapped during qualification, a seemingly short lead time can collapse when the order reaches a bottleneck.
Another frequent issue is the difference between prototype capability and repeatable production capability. A shop may successfully produce one complex five-axis part with senior operator attention, flexible scheduling, and manual inspection. That does not prove it can deliver a production lot under the same tolerances while maintaining traceability and meeting agreed inspection timing. Procurement teams should separate “can make one” from “can repeatedly release conforming units through a controlled process.”
Lead-time risk also rises when engineering changes are loosely managed. A revised drawing, changed firmware version, substitute material, or altered inspection method can leave the supplier using obsolete documentation. In regulated or high-reliability applications, the resulting hold may be appropriate; in poorly controlled environments, the change may be missed entirely. Both outcomes create cost and schedule exposure.
Start qualification with the part’s actual risk profile
A useful supplier review begins before issuing a broad request for quotation. Define what makes the item difficult to source, inspect, or replace. This prevents the qualification process from becoming a generic vendor questionnaire that gives equal weight to irrelevant details.
For each part family or assembly, identify the features that determine supplier suitability:
- Critical dimensions and tolerances: geometric tolerances, surface finish, concentricity, flatness, thread class, optical alignment, or repeatability requirements.
- Material constraints: approved grades, lot traceability, special alloy availability, moisture sensitivity, shelf-life control, or restrictions on material substitution.
- Special processes: welding, brazing, anodizing, heat treatment, coating, clean assembly, conformal coating, balancing, bonding, or environmental sealing.
- Verification requirements: first-article inspection, functional test, calibration records, destructive testing, non-destructive testing, software or firmware revision control, and inspection-report format.
- Failure consequences: whether a late or nonconforming component stops a production cell, delays system integration, creates a field reliability concern, or triggers a requalification effort.
This profile should become the basis for supplier questions and scoring. A CNC supplier capable of holding general dimensional tolerances may not be appropriate for an aerospace bracket requiring tightly controlled material provenance, fatigue-sensitive edge finishing, and documented special-process records. Likewise, an electronics assembler with fast-turn capacity may be unsuitable where component authenticity, controlled storage, and firmware traceability are essential.
Test the manufacturing route, not the marketing claim
When reviewing a candidate supplier, ask for a process route that follows the item from incoming material to shipment. The aim is not to demand proprietary operating details. It is to determine where lead-time and quality risk actually sit. A credible route identifies major stages, internal versus external ownership, inspection gates, and expected handoffs.
For a machined component, the route might include material receipt, cutting, rough machining, stress relief, finish machining, special processing, dimensional inspection, cleaning, marking, packaging, and final release. For an electronics or sensor assembly, it may include incoming inspection, controlled storage, PCB assembly, programming, functional testing, calibration, enclosure integration, burn-in where applicable, and serialized traceability.
Ask specific follow-up questions rather than accepting a statement such as “all processes are controlled.” Useful questions include:
- Which operations are performed at the quoted facility, and which are outsourced?
- Which outsourced process has the longest normal queue, and how is its turnaround monitored?
- What equipment or inspection resource is shared across competing jobs?
- What happens when a critical machine is unavailable or a measurement system is out of service?
- At which point is material lot identity linked to the finished part or assembly?
- Can the supplier show how drawing revisions and approved deviations reach the production floor?
A supplier does not need to promise that disruption will never occur. More useful evidence is a clear explanation of how disruption is detected, contained, escalated, and communicated. Unclear ownership, vague responses about sub-tier processes, or an inability to explain revision flow are stronger warning signals than a modestly longer standard lead time.
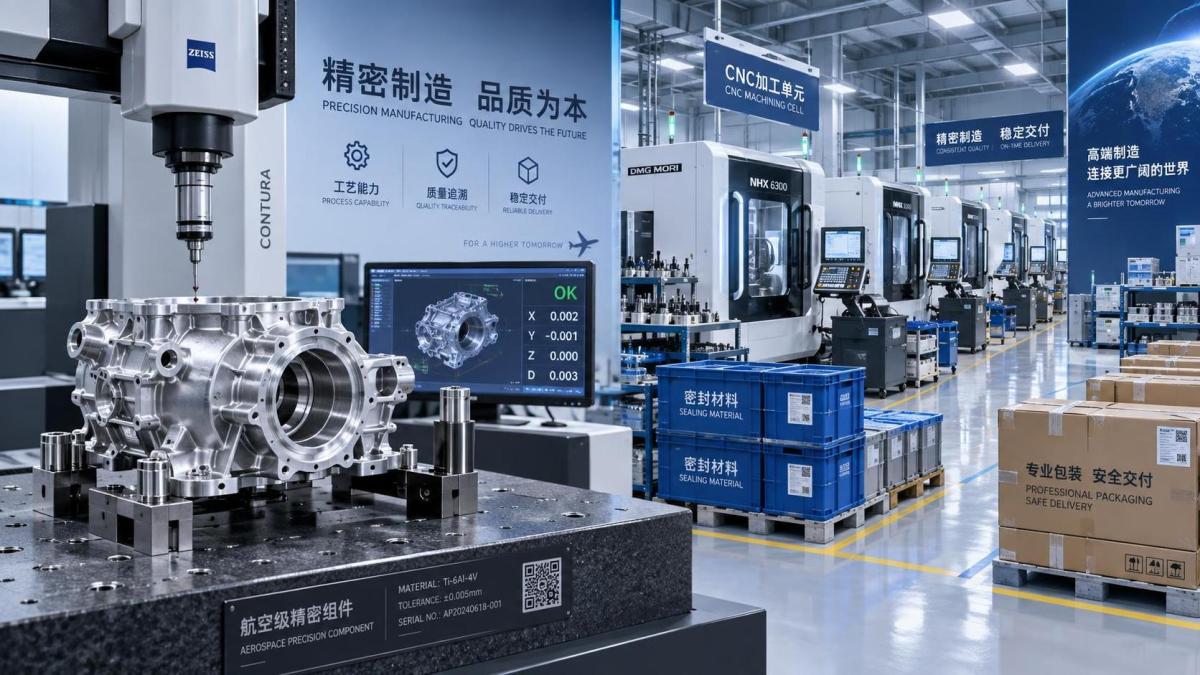
Confirm capability with evidence tied to the requirement
Certificates can support a qualification decision, but they are not a substitute for item-specific evidence. A certification may cover a broad management system while the supplier’s actual scope excludes the required process, site, or product category. Review the stated scope, the legal entity and location covered, and whether the certificate relates to the work being quoted.
Then request evidence that connects directly to the part risk profile. The appropriate level of review depends on the item, but it may include sample inspection reports, anonymized first-article documentation, calibration-control records, process-control plans, equipment lists, or examples of traceability records. For critical assemblies, a technical review involving engineering and quality functions may be necessary before commercial award.
Do not confuse a polished quality document with demonstrated process discipline. A strong review looks for consistency between documents, personnel explanations, and the production route. For example, a supplier that states it maintains complete lot traceability should be able to explain how that identity is preserved after cutting, batching, coating, assembly, and final packaging. The exact mechanism varies by process; the important question is whether it is controlled and retrievable.
Make capacity visible before placing the first production order
Capacity is not simply the number of machines or employees shown in a presentation. It is usable capacity at the required process step, for the required material, tolerance, inspection method, and delivery window. A supplier may have several machining centers but only one capable of a part’s envelope or accuracy requirement. An inspection department may have a coordinate measuring machine, but its programming queue can still delay release.
During qualification, establish the assumptions behind the quoted lead time. Clarify whether the clock starts at purchase order release, approved drawing receipt, material availability, deposit confirmation, or completion of first-article approval. Determine whether quoted lead time includes external processing, final inspection, export paperwork where relevant, and packaging requirements.
For recurring demand, ask the supplier to describe how it reserves or plans capacity. A realistic answer may involve forecast visibility, batch-size rules, order freeze dates, or agreed release schedules. Procurement should be cautious when a supplier offers very short dates without explaining the scheduling basis. An optimistic promise can appear commercially attractive while shifting risk into expediting, partial shipments, or quality escapes later.
Use a staged order to validate operational claims
Where the component is new, technically demanding, or strategically important, the first order should be structured as a learning event rather than treated as proof of long-term performance. A controlled initial release can verify documentation flow, material traceability, inspection format, communication speed, packaging, and actual cycle time. This is not about imposing unnecessary administrative burden. It gives both sides a defined opportunity to expose ambiguities before volume, system integration, or customer commitments increase the cost of correction.
Agree in advance on what constitutes an acceptable first release: required documents, approved inspection points, labeling, revision status, and rules for nonconformance notification. If a deviation is found, the supplier should not silently correct the condition or proceed with an undocumented substitute. The buyer needs timely information to decide whether the issue is acceptable, requires engineering disposition, or warrants a schedule adjustment.
Score suppliers by risk exposure, not by unit price alone
A low unit price can be meaningful only when suppliers are technically comparable and their delivery assumptions are visible. In hard-tech supply chain procurement, the total cost of a delayed part may include line downtime, emergency logistics, repeat inspection, engineering rework, scrapped material, and a new qualification cycle. These costs do not need to be converted into artificial precision to influence the decision. They should be recognized explicitly in the award rationale.
A practical scoring approach assigns more weight to the factors that can stop the program. For a high-complexity part, process evidence and traceability may outweigh a small price difference. For a standardized, noncritical item with multiple approved sources, commercial terms and replenishment speed may deserve greater emphasis. The weighting should follow the item’s failure consequence, not a universal supplier scorecard.
Keep the assessment record concise but decision-ready. It should state the required capability, evidence reviewed, open gaps, owner for each action, and whether the supplier is approved for prototypes, limited production, or ongoing supply. These approval levels matter. A supplier proven for prototype work should not automatically be treated as qualified for serial production, especially when volume changes the process route or reliance on subcontractors.
Build communication rules into the supplier relationship
Supplier qualification is weakened when performance problems are discovered only through a missed due date. Establish the events that require notification: material shortages, failed inspection, process interruption, drawing ambiguity, sub-tier delay, capacity conflict, or proposed substitution. Specify who receives the notice and what information is needed to make a decision. A short message stating “delivery may slip” is less useful than a clear description of the affected operation, expected impact, recovery options, and decision deadline.
Regular performance review should focus on patterns that affect future orders: recurring holds at the same process, repeated documentation corrections, late escalation, or delivery dates that change after purchase order acceptance. A one-time disruption may be manageable. Repeated inability to predict or communicate disruption indicates that the original qualification assumptions need to be revisited.
When supply risk is high, retain the evidence and lessons from each release. Updated process maps, approved inspection samples, packaging instructions, change-control contacts, and known bottlenecks reduce the effort required to place the next order. The goal is not to create paperwork for its own sake; it is to turn each completed order into verified knowledge that makes the next sourcing decision less exposed to surprise.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























