
Aerospace Machining Process Optimization Without Chasing Cycle Time
Publication Date
author
In aerospace machining process optimization, the real objective is not simply to cut minutes from a program. It is to maintain dimensional accuracy, protect material integrity, stabilize surface finish, and deliver repeatable output across complex parts such as titanium structural components, turbine blades, and thin-wall aerospace housings. For engineering teams, buyers, and manufacturing leaders, the practical question is straightforward: which process changes reduce total manufacturing risk without sacrificing throughput where it actually matters?
The short answer is that the best aerospace machining strategies do not worship cycle time in isolation. They optimize the full process window: machine dynamics, tool behavior, fixturing stability, thermal control, in-process verification, scrap exposure, rework probability, and downstream inspection burden. In high-value aerospace work, a slightly longer but more stable process often outperforms a faster but fragile one.
What aerospace teams are really trying to optimize
When people search for aerospace machining process optimization, many are not looking for generic productivity advice. They are usually trying to solve one of four real problems:
- How to improve part quality without creating unacceptable lead times
- How to machine titanium, Inconel, or aluminum aerospace parts with less distortion and tool failure
- How to choose between aggressive cycle time reduction and stable process capability
- How to qualify suppliers or internal processes using engineering evidence rather than sales claims
For aerospace manufacturing, optimization must be judged against mission-critical outcomes: tolerance conformance, fatigue-sensitive surface condition, burr control, geometry retention after unclamping, and process repeatability across batches. A process that is 12% faster but doubles tool wear variability or pushes Cp/Cpk downward is not optimized in any meaningful aerospace sense.
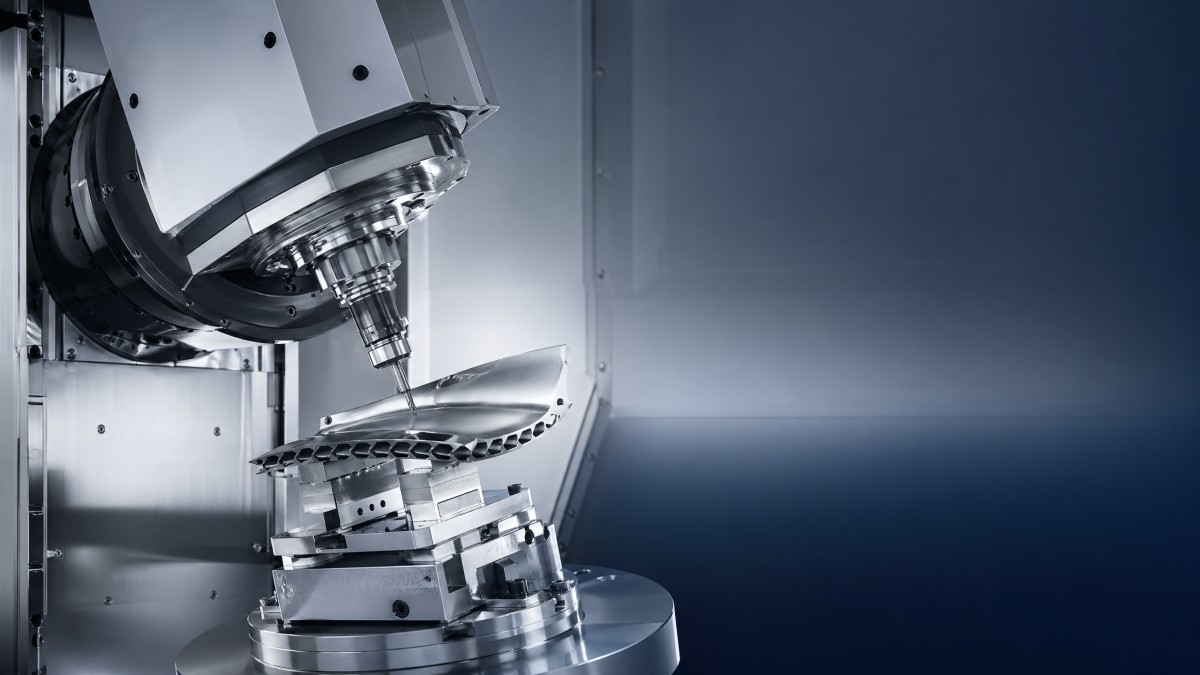
This matters especially in 5-axis CNC machining, where tool orientation, workholding access, cutter engagement, and machine kinematics interact in ways that make “faster” a misleading metric. For turbine blade machining, impeller finishing, or thin-wall titanium pocketing, process stability usually creates more business value than headline cycle time reduction.
Why chasing cycle time alone creates hidden cost in aerospace machining
Cycle time is visible. Quality instability is often delayed, dispersed, and harder to quantify. That is why many organizations over-prioritize speed. But in aerospace, the hidden costs of over-aggressive machining can be severe:
- Higher scrap rates on expensive forgings or near-net-shape parts
- Subsurface damage or heat-affected zones that are not obvious at the machine
- Dimensional drift caused by thermal load and residual stress release
- Shorter and less predictable tool life
- More frequent manual intervention and offset correction
- Longer inspection time due to inconsistent output
- Supplier qualification delays when process capability data is weak
For procurement teams and enterprise decision-makers, this changes the economics. A supplier quoting the shortest machining time may not offer the lowest total cost of ownership. In aerospace programs, schedule reliability, first-pass yield, and documentation discipline often outweigh nominal spindle-hour savings.
For operators and manufacturing engineers, the message is equally practical: if feed, speed, radial engagement, or step-over changes push the process outside a stable window, the resulting rework and troubleshooting usually erase the expected productivity gain.
Which process variables matter more than raw machine speed
If the aim is robust aerospace machining process optimization, several factors deserve more attention than simple cycle time compression.
1. Material-specific cutting strategy
Titanium alloys, nickel-based superalloys, and aerospace aluminum grades behave very differently under load and heat. Titanium, for example, has low thermal conductivity and tends to keep heat near the cutting zone. That makes conservative thermal management, cutter selection, and chip evacuation critical. A strategy that works for aluminum rib machining may be disastrous for a titanium bulkhead.
2. Workholding and part deformation control
Many aerospace components are thin-wall, high-value, and deformation-prone. Over-clamping, poor support location, or unstable fixture design can cause movement during machining or spring-back after release. In these cases, process optimization often starts with fixturing redesign, not code-level cycle reduction.
3. Toolpath consistency in 5-axis CNC machining
Tool orientation changes affect effective cutter diameter, chip thickness, and machine-axis acceleration behavior. A nominally faster 5-axis toolpath may introduce inconsistent cutter engagement or induce machine motion that harms surface finish. Good optimization means smoothing engagement and maintaining predictable cutting conditions.
4. Thermal stability
Thermal effects are a frequent source of dimensional variation in aerospace precision machining. Spindle growth, coolant temperature variation, long cut duration, and heat accumulation in difficult materials all influence actual part geometry. Shops that monitor thermal behavior typically achieve better repeatability than those focused only on metal removal rate.
5. Tool wear progression, not just initial performance
A process should be evaluated over the full tool life curve. Some parameter sets produce excellent first-part results but deteriorate rapidly. In aerospace environments, optimization should favor predictable wear behavior and stable quality across scheduled tool changes.
6. Inspection feedback integration
Inline probing, post-process metrology, and statistical trend tracking are central to robust optimization. If process changes are not linked to dimensional and surface-finish data, improvement decisions remain subjective.
How to optimize aerospace machining without sacrificing part integrity
The most effective approach is to optimize around process capability, not just machine utilization. A practical framework looks like this:
Define the true critical-to-quality features
Not all dimensions and surfaces carry equal functional risk. Separate features into categories such as:
- Flight-critical tolerance features
- Fatigue-sensitive surfaces
- Assembly interfaces
- Cosmetic or non-critical regions
This allows process aggressiveness to be applied selectively. Some regions may tolerate high-efficiency roughing, while others require conservative finishing strategies.
Optimize roughing and finishing separately
One common mistake is applying the same productivity logic across the full operation. Roughing should target controlled material removal with thermal and force management. Finishing should prioritize geometric accuracy, low vibration, and surface integrity. Treating them as separate optimization problems usually gives better results.
Validate with repeatability, not one successful part
A single good part proves little. Aerospace process optimization should be validated across multiple runs, operators where relevant, and realistic tool life stages. The key question is not “Can this process make a good part?” but “Can it make good parts repeatedly within a controlled window?”
Use data to define the safe operating window
Instead of selecting one aggressive recipe, identify the performance band where quality, tool life, and throughput remain stable. This window should be supported by measurable outcomes such as:
- Dimensional capability trends
- Surface roughness consistency
- Tool wear variation
- Spindle load behavior
- Scrap and rework frequency
Account for downstream process effects
Machining decisions influence deburring, coating preparation, non-destructive inspection, assembly fit, and even fatigue performance. A “faster” cut that creates poor edge quality or unstable surface condition can increase total manufacturing effort downstream.
What good process optimization looks like for different stakeholders
The same aerospace machining project is evaluated differently by each decision group. Strong process planning should answer all of them.
For manufacturing engineers and operators
- Is the toolpath stable and practical on the actual machine?
- Does the setup control vibration, thermal drift, and part movement?
- Can the process hold tolerance without constant offset chasing?
- Is tool life predictable enough for production scheduling?
For procurement professionals
- Does the supplier demonstrate process capability with real data?
- Are material-specific machining controls documented?
- Is quality performance repeatable or dependent on special intervention?
- What is the supplier’s risk profile for scrap on expensive aerospace materials?
For business leaders and program managers
- Will this process reduce total cost, not just quoted machining hours?
- Does it shorten qualification cycles through better documentation and consistency?
- Can it scale from prototype to low-rate or serial production?
- Does it protect delivery reliability on high-consequence parts?
This multi-layer view is where many sourcing decisions fail. A process may appear efficient in a quote but perform poorly under production conditions because the evaluation focused too narrowly on cycle time.
How to assess whether a supplier is optimizing responsibly
For buyers and technical evaluators, the most useful question is not “How fast can you machine this?” but “How do you control process risk while maintaining output?” A capable aerospace machining supplier should be able to discuss:
- Material-specific strategy for titanium, Inconel, aluminum, or hardened alloys
- Fixturing logic for distortion-prone geometry
- Tool life monitoring and replacement criteria
- In-process probing and final inspection methodology
- Surface integrity controls for critical features
- Evidence of repeatability across multiple runs
- AS9100-aligned process discipline where applicable
Data-rich answers are far more valuable than broad claims about advanced equipment. Parameters, tolerances, and stability metrics tell you more than marketing language. This aligns with a hard-tech procurement reality: in precision aerospace work, engineering truth is measurable.
Practical signs your machining process is optimized for aerospace reality
A process is usually on the right path when the following conditions are present:
- First-pass yield is consistently high
- Surface finish and dimensional accuracy remain stable across tool life
- Operators do not need frequent manual corrections
- Inspection confirms predictable results rather than isolated success
- Cycle time is competitive but not achieved by pushing the process to the edge
- Part distortion after unclamping is understood and controlled
- Engineering teams can explain why each parameter choice exists
In other words, optimization is not the elimination of time. It is the reduction of uncertainty.
Conclusion: the best aerospace machining process is the one you can trust repeatedly
Aerospace machining process optimization without chasing cycle time is not a conservative philosophy. It is a more advanced one. It recognizes that in high-value, tolerance-critical manufacturing, speed matters only when quality, repeatability, and part integrity remain under control.
For engineers, this means building processes around stable cutting conditions, thermal awareness, fixturing discipline, and measured feedback. For procurement teams, it means qualifying suppliers based on capability evidence rather than low quoted hours. For decision-makers, it means evaluating machining strategy through total risk, total cost, and delivery confidence.
The strongest aerospace machining organizations do not ask only how to cut faster. They ask how to machine complex parts correctly, repeatedly, and with less uncertainty. That is the optimization standard that actually protects program performance.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























