
How to Use MES-SCADA Integration APIs for Real-Time Production Data Sync?
Publication Date
author
How to Use MES-SCADA Integration APIs for Real-Time Production Data Sync?
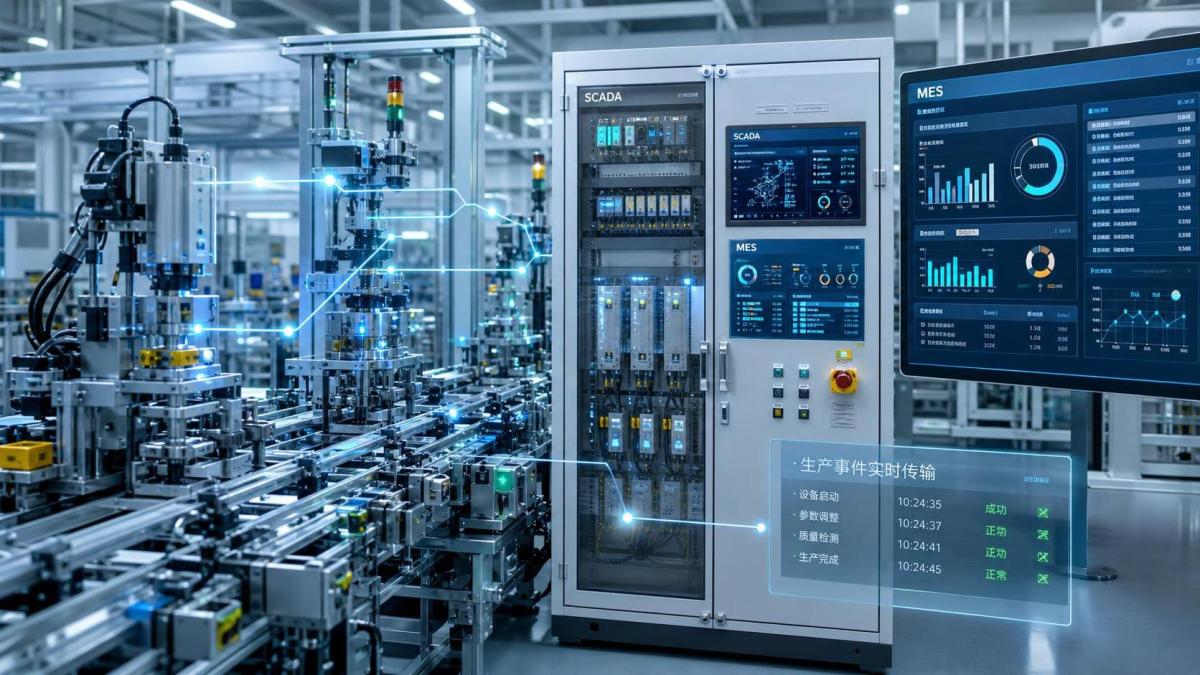
A mes scada integration api is often described as a bridge between shop-floor control and manufacturing execution. That description is directionally correct, but it hides the part that usually decides whether a project succeeds or becomes a long-running source of bad timestamps, duplicate events, and operator mistrust. The real job of the API is not merely moving data from one system to another. It is preserving production meaning while data crosses layers that were designed for different purposes.
SCADA systems are built to supervise equipment states, alarms, process variables, and control context at high frequency. MES platforms care about orders, genealogy, work-in-progress, dispatching, quality records, and traceability. When people say they want “real-time sync,” they often assume the problem is transport speed. In practice, the harder issue is semantic alignment: what exactly counts as a machine cycle, a completed unit, a downtime event, a quality hold, or a shift handoff, and which system is authoritative for each one?
That is why technical evaluation should start with the data contract, not the dashboard demo. If an integration API cannot clearly define payload structure, event timing, update rules, and source-of-truth ownership, low latency alone does not make the sync reliable.
What the API is really synchronizing
In most plants, SCADA emits fast-changing operational signals: tag values, alarm conditions, machine status transitions, counters, recipe parameters, and process measurements. MES consumes only a subset of that stream, but the subset has to be production-relevant and auditable. A good integration layer therefore performs filtering, normalization, and event shaping before the MES ever sees the data.
Consider a packaging line. SCADA may sample line speed every second, track stop causes, and register sensor edges in milliseconds. The MES does not need every raw tag forever. It usually needs structured events such as “job started,” “lot completed,” “micro-stop exceeded threshold,” “reject count incremented,” or “critical process parameter drifted outside recipe limits.” The API’s role is to expose those events in a format the MES can use consistently, whether through REST endpoints, message queues, webhooks, OPC UA-connected middleware, or vendor-specific connectors.
This is where many integrations become noisy. Teams expose raw points because it feels more complete. Later, MES workflows get flooded with data that is technically live but operationally useless. Engineering-grade integration is selective by design.
Real-time does not mean the same thing to every layer
For control engineers, real-time may imply deterministic response in a tightly bounded interval. For MES architects, it usually means data is available quickly enough to support production decisions, quality enforcement, and traceability without manual reconciliation. Those are not the same requirement.
An API used for MES-SCADA synchronization rarely operates under hard real-time control constraints. It operates under near-real-time business and operational constraints. The practical question is not “Is it instant?” but “Is the delay bounded, measurable, and acceptable for the use case?”
For example, order progress updates on a machining cell may tolerate several seconds if downstream planning and labor reporting remain accurate. Electronic batch records in a regulated process environment may need tighter sequencing and stronger timestamp integrity. Alarm escalation for critical quality excursions may require event delivery fast enough to trigger MES holds before nonconforming product advances. So latency targets should be attached to scenarios, not to a generic marketing claim of real-time capability.
The technical core: protocol mapping and data models
Most SCADA environments already speak in industrial protocols or tag architectures that were never intended to be business-friendly APIs. OPC UA is common for structured industrial interoperability, while legacy deployments may still expose Modbus, proprietary drivers, or historian interfaces. MES platforms, by contrast, often expect JSON payloads, service endpoints, or brokered event messages. The integration API sits between those worlds.
This translation layer has to answer several practical questions:
- Is the source signal polled, subscribed, or pushed on change?
- Are timestamps generated at the device, the SCADA node, the middleware layer, or the MES endpoint?
- How are units, scaling factors, and engineering limits represented?
- What turns a stream of changing values into a production event with business meaning?
- How are retries handled without creating duplicate completions or repeated downtime records?
A strong data model usually distinguishes between three layers: raw telemetry, interpreted operational events, and MES transaction records. Keeping those separate prevents a common failure mode where one noisy machine tag is treated as if it were already a validated production fact. That distinction matters in industries where traceability and quality review depend on knowing whether a value was measured, inferred, corrected, or operator-confirmed.
What technical evaluators should examine first
If the API is being assessed for procurement, architecture review, or platform selection, the evaluation should focus less on the UI and more on failure behavior. Under normal load, almost every integration can look competent. The useful questions appear when the line stops, the network blips, the gateway restarts, or a machine sends values out of order.
That last point deserves emphasis. A mes scada integration api should not casually punch a hole through the control network because someone wants easier reporting. In many environments, the architecture has to respect separation between OT and IT zones, often with gateways, brokers, or DMZ patterns that limit direct access. The exact design depends on site policy and sector requirements, but the principle is stable: data flow convenience does not outrank operational resilience.
Common misunderstandings that distort API selection
One recurring misunderstanding is that more data points equal better visibility. In reality, a high-volume feed without event logic, context tags, and quality flags can make MES records less trustworthy, not more. Another is the assumption that vendor support for “API integration” means a complete interoperability model. Often it only means endpoints exist. It does not mean the payloads align with your line states, genealogy requirements, or exception workflows.
There is also a habit of treating synchronization as a one-time interface build. Production systems do not stay still. New SKUs, revised routings, recipe updates, machine firmware changes, and historian tuning all affect what the API has to carry and how the MES interprets it. An integration that works in factory acceptance testing but has weak schema governance can become brittle after the first operational change cycle.
From a hard-tech evaluation perspective, this is where disciplined documentation matters more than polished sales language. Clear field definitions, event state diagrams, retry behavior, and ownership matrices tell you far more about engineering maturity than generic claims about smart manufacturing readiness.
Where standards and compliance enter the conversation
Not every MES-SCADA project is compliance-driven, but many operate in environments where auditability, electronic records, or product traceability cannot be treated casually. Depending on the sector, teams may need to align with internal validation practices, cybersecurity frameworks, or industry data models already used in manufacturing software. ISA-95 is frequently relevant as a reference model for information exchange between enterprise and control functions, even when the deployed systems do not implement it in a pure form.
That does not mean every integration should be forced into a textbook standard map. It means evaluators should recognize whether the API design follows a coherent model for equipment, material, personnel, process segment, and production response data, or whether it is just a bundle of convenient fields accumulated project by project. The former scales. The latter often becomes expensive during expansion, revalidation, or multi-site rollout.
A practical way to judge engineering readiness
A usable test is to walk one production event from origin to record. Start with a physical action on the line: a machine completes a unit, rejects a part, changes recipe, enters fault, or restarts after downtime. Then verify the full chain. What signal changes first? Where is the first timestamp assigned? When does the event become durable? How is context attached, such as work order, operator, material lot, and equipment ID? What happens if the MES is unavailable for five minutes? Can the event be replayed once connectivity returns, and can it do so without duplication?
If those questions can be answered precisely, the API is likely mature enough for serious production use. If the answers depend on manual reconciliation, implied assumptions, or vendor-specific black boxes that no one on the plant side can inspect, the integration may still function, but it is not yet robust by engineering standards.
For organizations operating in advanced manufacturing, where tolerance discipline and data trust are inseparable, that distinction is not academic. The value of a mes scada integration api lies in whether it can turn machine-level signals into production truth that planners, quality teams, and engineers can rely on without constant cleanup. That is the threshold worth evaluating: not whether data moves, but whether the synchronization preserves meaning under real operating conditions.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 25, 2026Hesai Leads Global ADAS Main Lidar Shipments in Yole’s 2026 ReportHesai led global ADAS main lidar shipments with a 43% share in 2025, according to Yole’s 2026 report. Explore what this ranking reveals about its automotive market position.TSV Data Lab
 Oct 25, 2026Choosing an Aerospace Materials Manufacturer: Quality and Traceability ChecksChoosing an aerospace materials manufacturer? Learn how to verify certifications, test reports, and lot traceability to qualify suppliers confidently and reduce costly sourcing risks.Dr. Marcus Vance
 Oct 24, 2026Guotai Haitong: Global Entry-Level 3D Printer Shipments Rose 39% in Q1 2026Entry-level 3D printer shipments rose 39% in Q1 2026, Guotai Haitong reports. Explore how AI, multicolor printing and print farms are shaping market growth.Dr. Marcus Vance
 Oct 24, 2026Choosing an Industrial Vision Inspection Supplier: Acceptance Tests That MatterChoose an industrial vision inspection supplier with confidence. Discover acceptance tests for defect detection, false rejects, production speed, and reliable part rejection before you buy.TSV Data Lab
 Oct 23, 2026US Navy Raises Gecko Robotics Contract Ceiling to $300M for Robotic Fleet MaintenanceUS Navy raises Gecko Robotics’ contract ceiling to $300M for Pacific Fleet robotic inspections. Explore potential opportunities for maintenance suppliers and key procurement considerations.Chen Wei (Automation Lead Engineer)
 Oct 23, 2026Choosing Industrial Sensing Systems for Global Plants: Protocol CompatibilityCompare industrial sensing systems international buyers can trust. Explore protocol compatibility, reduce integration risks, and select proven configurations for reliable global plant deployments.TSV Data Lab
 Oct 22, 2026KUKA Showcases Physical AI and iiQKA.AI Vision at NVIDIA GTC BerlinExplore KUKA’s Physical AI showcase at NVIDIA GTC Berlin and discover how iiQKA.AI Vision aims to simplify robotic vision integration and improve 2D and 3D scene recognition.TSV Data Lab
 Oct 22, 2026Robotic Machining of Advanced Composites: What Tolerances Are Achievable?Explore advanced materials machining robotics: discover what drives achievable composite tolerances and how to validate accuracy before investing in your next machining system.Dr. Marcus Vance
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)























