
Why Aerospace Bearing Grinding Tolerances Shift After Dressing
Publication Date
author
In precision grinding for aerospace bearings, tolerance drift after dressing is rarely random—it reflects wheel condition, thermal behavior, machine dynamics, and process control limits. For engineers, buyers, and technical decision-makers comparing precision grinding surface roughness, cnc spindle runout measurement, and aerospace alloy fatigue life data, understanding why these shifts occur is essential to reducing qualification risk, protecting dimensional stability, and making more reliable machining and sourcing decisions.
Why does tolerance shift appear immediately after dressing?
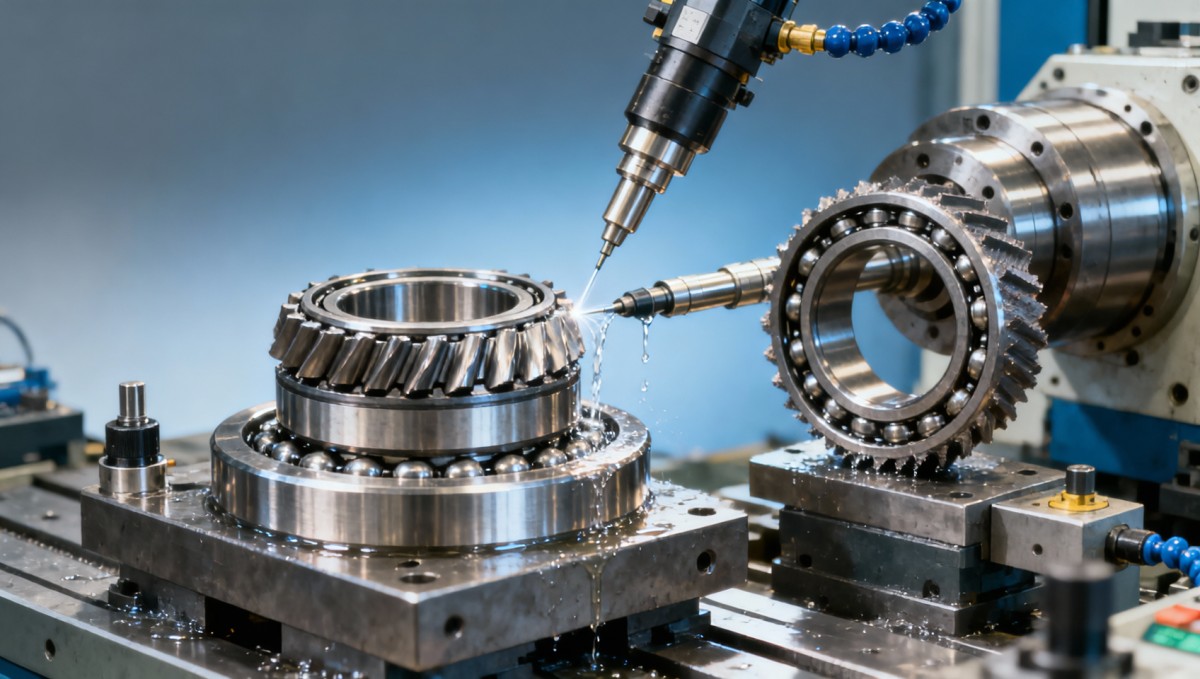
In aerospace bearing grinding, dressing resets the wheel topography, but it also changes the cutting mechanics at the exact moment process stability matters most. A newly dressed wheel often cuts sharper, generates a different force signature, and alters heat partition between the wheel, part, and coolant. That is why the first 3–10 components after dressing frequently show dimensional movement, even when the machine program remains unchanged.
For operators, this shows up as size drift, waviness variation, or a surface finish change that does not match the previous steady-state window. For procurement teams reviewing supplier capability, the issue is more serious: if a vendor reports only final average tolerance without disclosing post-dress stabilization behavior, the quoted capability may not reflect true aerospace process control.
The root cause is that dressing is not a neutral maintenance event. It changes wheel sharpness, grit exposure, bond support, wheel face geometry, and effective contact conditions. In high-precision bearing race grinding, even a few microns of altered wheel behavior can move a process from a stable corrective loop into a scrap-prone zone, especially when the required roundness or size band is already tight.
TSV’s engineering perspective is simple: parameters do not lie. If tolerance shift appears after dressing, the answer is usually found in measurable process interactions rather than vague claims about operator feel or “normal variation.” The right response is to isolate the mechanism, define the stabilization window, and link it to machine, wheel, coolant, and inspection data.
Four direct mechanisms that move size after dressing
- Wheel sharpness changes the specific grinding energy. A sharper wheel often cuts more freely at first, reducing plowing and changing the material removal rate per pass.
- Wheel form changes alter the effective contact patch. Even a small deviation in dress lead or overlap can shift profile transfer to the raceway.
- Thermal balance resets after dressing. During the first 5–15 minutes, spindle, wheel hub, coolant temperature, and workholding can settle into a new equilibrium.
- Machine compensation may lag behind the new wheel condition. If offset logic is based on the previous steady-state trend, the first pieces after dressing can miss the target before the control loop catches up.
This is why high-reliability suppliers often separate “after dressing capability” from “stabilized production capability.” For aerospace buyers, that distinction matters in first-article approval, lot acceptance, and process audit discussions. A shop that cannot explain its first-part-to-tenth-part behavior after dressing may also struggle with repeatability during mixed-batch production.
Which process variables most strongly affect post-dress grinding tolerance?
Not every variable has equal influence. In practice, tolerance shift after dressing is usually driven by a stack of interacting factors rather than a single fault. For aerospace bearing applications, the highest-risk variables are wheel specification, dressing parameters, spindle condition, thermal control, in-process gauging response, and the metallurgy of the ring material. Materials with strong thermal sensitivity or work-hardening behavior can amplify the effect.
Engineers evaluating precision grinding surface roughness and cnc spindle runout measurement should view these variables as a linked system. A supplier may present acceptable roughness values, but if spindle radial error, coolant delivery, and dress consistency are unstable, the process can still drift outside diameter, geometry, or subsurface integrity limits. That becomes a direct risk to bearing life and aerospace alloy fatigue life performance.
The table below summarizes the variables most often associated with immediate tolerance movement after dressing and the practical signals a technical team should review during process validation or supplier qualification.
A useful rule for buyers is to ask for trend evidence, not isolated values. One roughness number, one pass-fail report, or one first-article certificate does not explain whether the supplier can control the 0–30 minute window after dressing. That early interval is often where hidden process weakness appears first.
What operators and engineers should monitor first
Machine and wheel condition checks
Start with spindle error, wheel balance, and dressing repeatability. If spindle runout trends upward or balancing changes after wheel preparation, the tolerance band may widen before any obvious alarm appears. In many shops, a check at the start of shift, after wheel mounting, and after major dressing adjustments provides a practical three-point control routine.
Thermal and gauging checks
Next, verify coolant stability and in-process gauge reaction time. If coolant temperature drifts by several degrees during a 1–2 hour cycle block, size compensation may chase thermal effects rather than actual stock removal changes. On very tight aerospace work, even short thermal transients can distort the interpretation of dress-related drift.
Finally, compare post-dress size movement with final inspection and functional bearing requirements. A dimension that looks recoverable on paper may still reduce fatigue margin if the process introduces burn, residual stress, or shape error at the raceway.
How should procurement teams compare suppliers when post-dress tolerance is a risk?
Supplier comparison should go beyond quoted tolerance capability. In aerospace bearing grinding, the real question is whether the supplier can maintain dimensional stability through repeated dressing cycles, lot changes, and inspection handoffs. A vendor that only shares nominal tolerance but not process behavior after dressing may create hidden qualification cost later, especially if incoming audits reveal unstable first-piece control.
For procurement personnel and enterprise decision-makers, the practical evaluation frame includes at least 5 points: dressing strategy, measurement traceability, thermal management, machine health verification, and corrective action speed. These factors affect not only part acceptance but also delivery predictability, rework exposure, and long-term supplier development cost.
The next table provides a structured comparison model that can be used in RFQ reviews, technical audits, or supplier onboarding discussions for precision grinding programs tied to aerospace alloy fatigue life and bearing reliability requirements.
This comparison matters because the hidden cost of poor post-dress control is rarely limited to scrap. It can expand into delayed PPAP-style submissions, extra sample rounds, slower source approval, and more engineering review cycles. A lower unit price may lose its appeal quickly if qualification extends by 2–4 weeks.
A practical RFQ checklist for bearing grinding suppliers
- Ask how many parts are normally required after dressing before the process is considered stable for release.
- Request evidence of cnc spindle runout measurement and the review interval used for grinding machines.
- Confirm whether precision grinding surface roughness is evaluated together with geometry and burn prevention, not as an isolated finish target.
- Check whether material lot changes trigger a revised dressing or compensation plan.
- Verify response time for nonconformance, replacement samples, and process requalification support.
Teams that use this checklist typically improve supplier discussions because it shifts the conversation from marketing language to measurable process discipline. That aligns well with TSV’s data-first approach to sourcing decisions in hard-tech manufacturing.
What standards, controls, and operating practices reduce qualification risk?
Aerospace bearing grinding does not depend on one universal control plan, but qualification risk falls when suppliers tie process discipline to recognized quality frameworks and measurable shop-floor practice. In this context, common references may include AS9100-aligned quality systems, documented gauge calibration, controlled work instructions, traceable lot routing, and maintenance logs linked to grinding machine condition.
For operators, consistency often comes from repeatable routines more than from sophisticated language. A controlled sequence across wheel preparation, dressing, warm-up, first-piece inspection, and compensation review can reduce the probability that tolerance shift escapes detection. In many facilities, the most effective improvement is not a new machine, but a tighter 4-step discipline around the first parts after dressing.
A practical control sequence
- Step 1: Confirm machine warm-up, coolant condition, and spindle baseline before dressing begins.
- Step 2: Record dressing inputs, including depth, traverse, and interval, so that wheel condition is not treated as an untracked variable.
- Step 3: Inspect the first 3–5 parts with linked dimensional and surface checks rather than relying on a single gauge value.
- Step 4: Release production only after the stabilization trend is within the control window defined by the drawing and internal process limits.
This sequence is especially useful when qualification teams must compare multiple sources across regions. It creates a common review language: not “Can you grind this part?” but “How do you control the first 5 parts after dressing, and what evidence supports your answer?” That is a more reliable way to screen advanced manufacturing partners.
It also helps align production quality with downstream performance goals. Bearings used in aerospace environments are not judged only by dimensional acceptance at shipment. They are judged by durability, friction behavior, noise, and fatigue resistance over service life. Poorly controlled post-dress grinding can quietly undermine those outcomes long before a field issue becomes visible.
Common misconceptions that distort sourcing decisions
“If the wheel is freshly dressed, accuracy should automatically improve.”
Not always. Dressing can improve sharpness while temporarily disturbing thermal and geometric balance. Accuracy often improves only after the process reaches a new stable state.
“A low Ra value guarantees good bearing performance.”
No. Precision grinding surface roughness is only one indicator. Raceway geometry, residual stress, burn avoidance, and material response all influence aerospace alloy fatigue life and final bearing behavior.
“If dimensions pass final inspection, post-dress drift is not a major concern.”
This view ignores hidden cost. Final pass results can conceal unstable production control, extra sorting time, or inconsistent repeat orders. For procurement teams, stable process behavior is as important as single-batch acceptance.
FAQ and next-step decisions for engineering, sourcing, and leadership teams
How many parts after dressing should be checked before release?
There is no universal number, because part geometry, wheel type, machine condition, and tolerance band all matter. In practice, many teams monitor at least the first 3–5 parts, while tighter aerospace work may extend review to 10 parts or a defined time window such as the first 15–30 minutes. The key is documented stabilization logic rather than an arbitrary guess.
What should buyers ask when comparing quotations?
Ask for more than unit price and nominal tolerance. Request the supplier’s post-dress control method, cnc spindle runout measurement practice, first-part inspection routine, expected lead time for sample rework, and how precision grinding surface roughness is linked to functional bearing requirements. These details often explain cost differences better than the quote sheet alone.
Can tolerance drift after dressing affect fatigue life?
Yes, indirectly and sometimes significantly. If post-dress conditions promote grinding burn, geometry distortion, or unstable subsurface stress, the resulting component may still appear dimensionally acceptable while carrying a lower fatigue margin. That is why aerospace alloy fatigue life discussions should include grinding process evidence, not only material certificates.
When does this issue become a management-level concern?
It becomes strategic when qualification cycles are long, supplier change is expensive, or product risk is high. If one unstable grinding process can delay validation by several weeks, increase incoming inspection load, or affect field reliability, leadership should treat post-dress tolerance control as a sourcing and risk-management topic, not just a shop-floor detail.
Why work with a data-driven technical benchmark partner?
When technical claims are inconsistent, engineering teams need a clearer filter. TechStat Vanguard focuses on measurable manufacturing truth: tolerance behavior, process comparability, machine condition evidence, and benchmark-ready technical interpretation. For aerospace and precision machining programs, that means less time sorting through generic claims and more time validating what actually influences performance and qualification risk.
If your team is reviewing bearing grinding suppliers, validating a new source, or trying to understand why tolerance shifts after dressing, TSV can support the decision with structured parameter analysis. That can include guidance on spec-sheet definition, supplier comparison logic, precision grinding surface roughness interpretation, cnc spindle runout measurement review, and risk questions tied to aerospace alloy fatigue life expectations.
You can contact us to discuss six practical topics: parameter confirmation, source selection criteria, expected delivery windows, customization feasibility, applicable certification expectations, and sample support planning. For procurement and technical leaders, these conversations are most useful early—before RFQ release, first-article review, or supplier corrective action escalation.
If you need a more defensible basis for quoting, auditing, or approving aerospace grinding capability, reach out with your drawing requirements, target tolerance band, inspection method, and project timeline. TSV helps transform fragmented technical claims into a decision-ready engineering picture built on evidence rather than noise.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























