
Why 5 axis CNC surface finish Ra varies across complex contours
Publication Date
author
Across sculpted geometries, 5 axis CNC surface finish Ra can shift unexpectedly as tool orientation, feed stability, cutter engagement, and machine dynamics change along the path. For engineers, operators, and sourcing teams, understanding these variations is essential to controlling micro machining tolerance limits, reducing cnc milling chatter frequency analysis risks, and benchmarking real process capability beyond supplier claims.
Why does 5 axis CNC surface finish Ra change on complex contours?
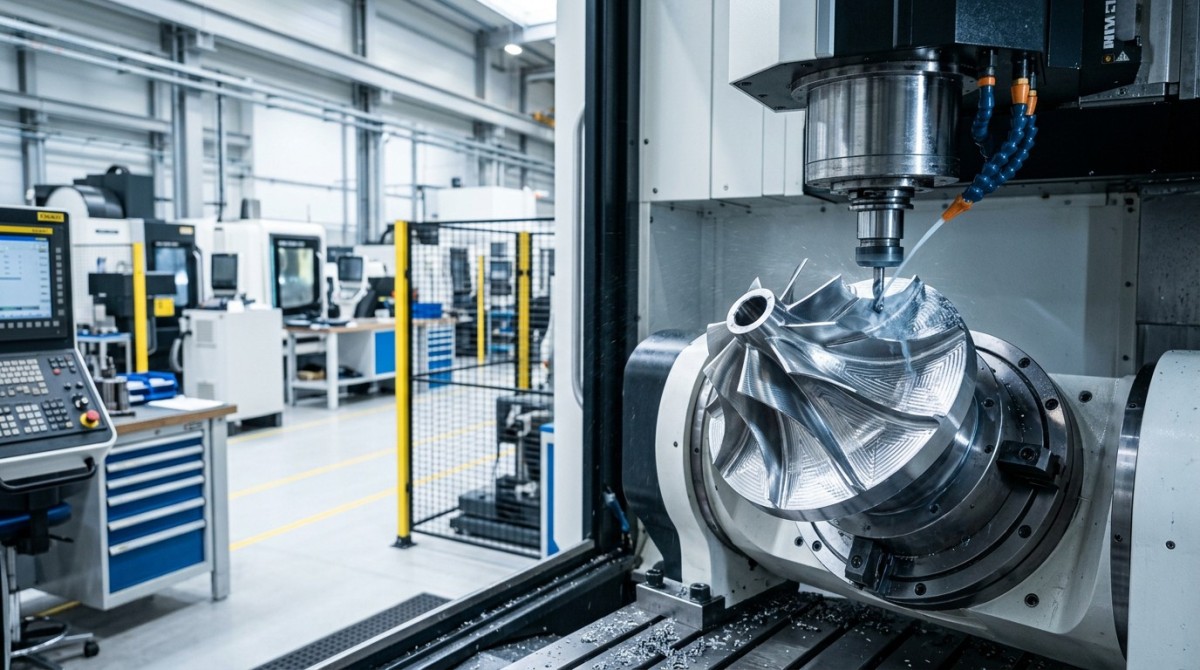
In 5 axis machining, surface finish is not defined by spindle speed and feed rate alone. On complex contours, the cutter continuously changes lead angle, tilt angle, contact point, and effective cutting diameter. That means the same nominal program can produce different Ra values over a single part, especially across deep cavities, twisted airfoil surfaces, organic medical profiles, or multi-radius housings.
For many information researchers and procurement teams, the common mistake is to treat one reported Ra value as a global capability statement. In practice, a supplier may achieve Ra 0.8–1.6 µm on open, stable regions, but see roughness drift when the tool moves into tighter curvature, longer tool stick-out, or less rigid machine postures. The gap between “best point finish” and “full contour finish consistency” is often where real manufacturing risk appears.
Operators face this problem in a more direct way. A path that looks smooth in CAM can still generate visible waviness, cusp variation, or localized chatter marks because the machine is accelerating and decelerating across many small vector changes. Once the machine transitions through 3, 4, or even 5 simultaneous axes, servo following error, jerk limits, and interpolation quality begin to influence the final texture.
This is where TSV’s engineering-first view matters. Instead of accepting broad claims, decision-makers should ask how Ra was measured, where it was measured, under what tool orientation, and across how many contour zones. Parameters do not lie, but incomplete parameter reporting often hides the actual process window.
Four root causes behind Ra variation
- Effective cutter diameter changes as the contact point moves along a ball nose or barrel tool, altering the real cutting speed at the surface.
- Tool engagement becomes unstable on steep-to-shallow transitions, which changes chip thickness and can trigger rubbing instead of clean shearing.
- Machine kinematics vary by position. A trunnion or swivel head may be very stable in one posture but less damped in another, especially at high acceleration.
- CAM smoothing, point density, and controller look-ahead settings influence how well the machine reproduces the intended surface, particularly on freeform geometry.
Which technical factors most strongly affect surface roughness across the toolpath?
When evaluating 5 axis CNC surface finish Ra, it helps to separate causes into geometry, cutting physics, and machine dynamics. Geometry determines whether the cutter is working on a convex ridge, concave pocket, or blended transition. Cutting physics determines whether the edge is cutting, ploughing, or vibrating. Machine dynamics determine whether the commanded path is actually followed under load within a stable tolerance band.
A common engineering range for finish milling uses stepovers from approximately 0.02 mm to 0.20 mm depending on Ra target, tool radius, and part material. However, that range cannot be interpreted in isolation. A 0.05 mm stepover on a shallow area may produce a very fine finish, yet the same setting on a steep wall with unfavorable contact geometry can leave a different peak-to-valley profile. That is why scallop control and actual roughness are related but not identical.
Feed per tooth also behaves differently in 5 axis motion than in simple 3 axis cuts. As rotary axes move, local feed at the tool-workpiece contact zone may effectively speed up or slow down. If the control is not using advanced feed compensation or if post-processed motion contains dense short segments, surface finish can worsen even when the programmed feed appears conservative.
For difficult alloys such as titanium, Inconel, hardened stainless steels, or cobalt-chrome, the margin for error becomes smaller. Heat, work hardening, and tool edge wear amplify any instability. In these conditions, Ra variation may become visible within one cycle if tool wear reaches a threshold before the full contour is completed.
Key variables engineers and buyers should request
The table below translates technical drivers into practical questions for supplier assessment. This is particularly useful when comparing shops that all claim advanced 5 axis capability but report finish quality differently.
A strong supplier can explain not only the target Ra, but also the process envelope behind it: material grade, cutter type, stepover range, spindle speed band, coolant method, and measurement location. That level of reporting supports procurement decisions far better than a single polished sample photo.
Why chatter analysis matters
cnc milling chatter frequency analysis is often treated as a specialist topic, but it is directly tied to visible finish defects. If a machine-tool-holder-workpiece system excites a natural frequency under specific engagement conditions, the result may be repeating marks that push Ra out of specification. On long-reach finishing tools, even a small instability can spread across a 50 mm–200 mm contour span.
For users and operators, this means sound, spindle load, and mark spacing are not secondary observations. They are process evidence. For buyers, it means a supplier that performs practical stability mapping or at least documents chatter-sensitive regions is usually more reliable than one that only promises cosmetic quality.
How should procurement teams compare suppliers for complex contour finishing?
Procurement teams rarely buy “Ra” in isolation. They buy a combination of contour accuracy, repeatability, inspection discipline, cycle time, and delivery confidence. In aerospace, robotics, sensor housings, medical components, and precision fixtures, surface finish often interacts with sealing, fatigue initiation, optical behavior, coating adhesion, or downstream polishing time. That makes the sourcing decision broader than a surface roughness number alone.
A useful approach is to compare suppliers across 5 decision dimensions: achievable Ra range, consistency across contour zones, evidence of micro machining tolerance limits, machine/process stability, and reporting transparency. Shops that only quote a low nominal Ra but cannot explain contour-dependent variation may create hidden cost during qualification, first article approval, or assembly validation.
Typical qualification for a new precision machining source may take 2–6 weeks depending on part criticality, material, and documentation needs. If the supplier provides only a generic finish claim, that window often stretches because engineering teams need extra sample reviews, additional metrology, or revised process sheets. Better front-end questioning reduces this cycle.
For enterprise decision-makers, the issue is risk transfer. A poor understanding of 5 axis CNC surface finish Ra variation can shift risk from the supplier to your own engineering and quality teams. That risk shows up as delayed PPAP-style reviews, extra CMM cycles, repeated polishing, or scrap on expensive near-net-shape material.
Supplier comparison framework
The following comparison matrix helps sourcing teams evaluate whether a machining partner understands complex contour finishing as a controlled process rather than a marketing statement.
This comparison also helps explain price differences. A supplier offering stable finish on complex contours may not be the cheapest quote, but may reduce secondary finishing, rework, and supplier development effort. In B2B procurement, total qualification cost often matters more than the initial machining line item.
A 5-point sourcing checklist
- Ask for Ra data from at least 3 contour regions: shallow, steep, and transition areas.
- Confirm whether micro machining tolerance limits and finish requirements were validated in one setup or after hand blending.
- Request the planned finish tool type, stick-out, and expected tool life window for the material family.
- Review whether cnc milling chatter frequency analysis or equivalent stability checks are used on difficult geometries.
- Tie the quoted Ra to acceptance method, measurement cutoff, and whether filtered or unfiltered values are reported.
What are the most common mistakes in specification, machining, and inspection?
The first mistake is writing a drawing note that demands a uniform Ra over all freeform surfaces without identifying functional zones. Some surfaces are sealing faces, some are aerodynamic, and some are cosmetic only. Applying one blanket requirement may raise cost unnecessarily or create confusion during inspection. In many programs, splitting the part into 3 categories of finish-critical areas leads to better manufacturability and clearer supplier accountability.
The second mistake is ignoring measurement direction and cutoff settings. Roughness values can change depending on whether the stylus crosses tool marks or runs along them. A contour that looks acceptable under one measurement orientation can fail under another. This is not manipulation; it is metrology context. Teams should define where and how Ra is measured before comparing bids or approving first articles.
The third mistake is assuming polishing can always rescue a poor machined finish. Manual blending may alter edge break, profile accuracy, or local tolerance stack-up. On precision contours, especially in aerospace and medical components, uncontrolled post-processing can solve one problem while creating another. That is why machining strategy should aim for process capability first, not rely on downstream correction.
The fourth mistake is separating surface finish from geometric tolerance. A part may show a low Ra on a small patch but still fail functional intent if waviness, form error, or localized deflection exceed allowable limits. Finish, profile, and positional outcomes must be reviewed together, especially when the feature interacts with bearings, seals, optics, fluid flow, or aerodynamic performance.
FAQ for engineers, operators, and buyers
Can one quoted Ra value represent an entire 5 axis part?
Usually no. A single value may represent one sampled location, not the full contour. On freeform parts, it is more practical to define representative zones and acceptable ranges. For example, a function-critical surface may require tighter finish control than a non-contact cosmetic blend area. The key is traceable zoning rather than a universal number with no context.
How many sample locations should be checked?
For complex contours, 3–5 locations is a practical starting point during process qualification: one shallow zone, one steep zone, one transition zone, and additional points on deep cavity or long-reach areas if relevant. Critical programs may require more, but fewer than 3 points often misses the very variation that causes field or assembly problems.
Is lower Ra always better?
Not always. Lower Ra may increase machining time, tool wear, or unnecessary cost if the function does not require it. Some surfaces care more about profile accuracy, waviness, or isotropic texture than the lowest possible roughness average. Procurement teams should match finish requirements to function and downstream process, not to appearance alone.
What delivery questions should be asked before ordering?
Ask for the expected programming time, sample lead time, first article timeline, and any risk factors linked to material or geometry. For prototype work, a machining and inspection cycle may take 7–15 days, while qualified repeat production may stabilize after the initial process window is proven. Surface finish risk is usually highest during first-run development, not mature repetition.
How to reduce finish risk and make better decisions with TSV
TechStat Vanguard approaches precision machining the way advanced manufacturing teams actually need it approached: through traceable parameters, comparative benchmarking, and specification clarity. In the context of 5 axis CNC surface finish Ra, that means separating marketing language from measurable process capability. The goal is not to repeat generic claims, but to help teams understand where finish varies, why it varies, and how to source with fewer surprises.
For information researchers, TSV can help structure what to compare in vendor documentation. For operators and technical users, TSV highlights the interaction between path strategy, machine behavior, and surface outcome. For procurement professionals, TSV supports supplier qualification using measurable checkpoints instead of vague assurances. For enterprise decision-makers, TSV reduces the cost of ambiguity by translating contour finishing into procurement-grade engineering language.
A practical project review often begins with 4 inputs: part geometry category, material family, tolerance and finish zones, and inspection expectations. From there, teams can evaluate whether the supplier’s machine platform, tooling plan, and process controls are aligned with the actual contour risk. This shortens the path from quotation to technical confidence.
If you need support, the most useful discussion topics are specific. Share the target Ra range, the contour areas that matter most, expected micro machining tolerance limits, preferred inspection method, planned batch size, and timeline constraints. That allows a meaningful review of process feasibility rather than a generic sales conversation.
Why choose us for engineering-based sourcing insight?
- We focus on parameter-backed analysis, including finish variation across contour zones rather than isolated best-case samples.
- We help teams compare suppliers using practical criteria such as measurement method, process stability, and documentation quality.
- We connect precision machining benchmarks to broader hard-tech procurement needs in aerospace, robotics, sensors, and advanced manufacturing.
- We support more informed decisions on parameter confirmation, supplier selection, lead-time review, sample strategy, certification expectations, and quotation alignment.
If your team is validating a new 5 axis supplier or reviewing a difficult contour finish requirement, contact TSV with your drawing notes, material, target surface zones, and timeline. We can help frame the right questions around parameter confirmation, process window assessment, inspection logic, sample support, and vendor comparison before hidden manufacturing risk becomes a costly sourcing problem.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026China’s Industrial Robot Exports Near RMB 10 Billion in First Nine Months of 2026China’s industrial robot exports neared RMB 10 billion in January–September 2026, with value rising faster than volume. Explore the data and what it could mean for suppliers.Chen Wei (Automation Lead Engineer)
 Oct 21, 2026Low-Latency Industrial Data Processing: Pricing and Key Cost DriversExplore industrial data latency price drivers, from edge hardware to integration and support. Learn how to compare quotes, verify performance, and avoid unnecessary costs.TSV Data Lab
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)
 Oct 20, 2026How Do You Measure Industrial IoT Gateway Latency Under Load?Measure industrial IoT gateway latency under load with reliable timestamps, realistic traffic, and tail-latency analysis. Discover how to expose bottlenecks and choose the right gateway.TSV Data Lab
 Oct 19, 2026How Do You Verify That Precision Machined Parts Meet Tolerances?Master precision machining tolerance verification with the right tools, datum setups, and acceptance rules. Learn how to validate parts confidently and reduce costly inspection errors.Dr. Marcus Vance
 Oct 18, 2026What Should an AS9100 Machining Supplier Checklist Include?Build an AS9100 machining supplier checklist that verifies capability, traceability, inspection, and outsourced processes. Discover what to check before approving your next aerospace supplier.Dr. Marcus Vance
 Oct 17, 2026How Should You Interpret Industrial Robot Repeatability Specs?Decode industrial robot repeatability specifications, understand ISO 9283 test conditions, and avoid costly selection mistakes. Learn how to verify performance for your process.Chen Wei (Automation Lead Engineer)
 Oct 16, 2026How Can You Fairly Compare MTBF Across Industrial Servo Motors?Make a fair industrial servo motor MTBF comparison with matched operating profiles, failure criteria, and confidence bounds. Discover how to assess reliability beyond advertised numbers.Chen Wei (Automation Lead Engineer)
 Oct 15, 2026How Should You Compare TechStat Vanguard 5-Axis CNC Tolerances?TechStat Vanguard 5-axis CNC tolerance comparison: learn how to verify part accuracy, assess inspection evidence, and choose suppliers that reliably meet your drawing requirements.Dr. Marcus Vance
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab























