
Swiss Turning Concentricity Tolerance How Tight Is Too Tight
Publication Date
author
In precision manufacturing, swiss turning concentricity tolerance can determine whether a part performs flawlessly or fails under load. But how tight is too tight? From cnc spindle runout measurement to aerospace alloy fatigue life data, engineers, buyers, and decision-makers need more than claims—they need measurable limits, process capability, and application-driven judgment grounded in real machining data.
What does swiss turning concentricity tolerance really control?
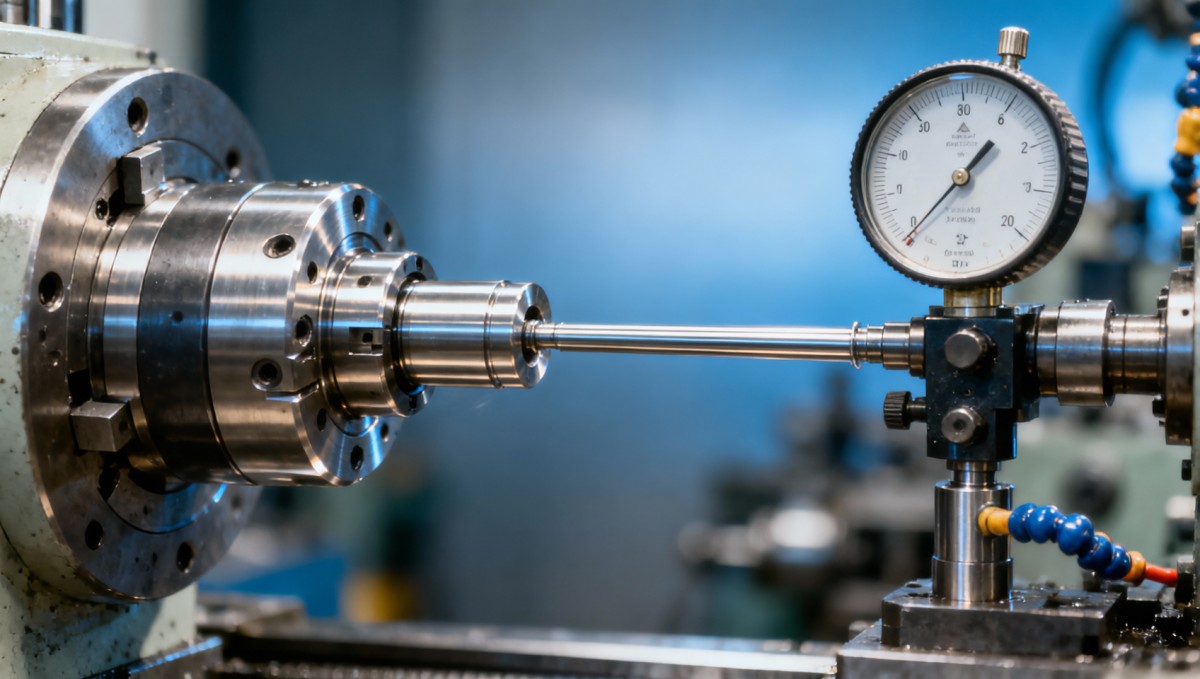
Swiss turning concentricity tolerance is not just a drawing note. It affects shaft alignment, bearing fit, seal performance, rotating balance, and downstream assembly yield. In practical terms, it describes how closely one cylindrical feature shares the same axis with another datum feature. When engineers call for extremely tight concentricity, they are usually trying to control functional runout, vibration, or uneven load transfer rather than chasing a number for its own sake.
In swiss-type machining, the challenge is amplified by long, slender workpieces, guide bushing behavior, thermal drift, insert wear, collet condition, and sub-spindle transfer accuracy. A print calling for 0.005 mm concentricity may be realistic for a short, stable geometry in low-to-medium volume production. The same value can become expensive, unstable, or unnecessary when the part length-to-diameter ratio rises above 8:1, the material is gummy, or the feature is created in multiple setups.
For operators, the key point is that concentricity is rarely controlled by one adjustment. It is the result of a chain: spindle condition, toolpath strategy, guide bushing setup, support timing, cutoff behavior, and inspection method. For procurement teams, this means supplier claims should be tied to process windows, gauge methods, and lot-level capability, not vague statements such as “micron precision.”
TSV’s data-driven view is simple: parameters do not lie. If a supplier promises very tight swiss turning concentricity tolerance, the first questions should be whether the tolerance is measured as concentricity, total indicated runout, or position relative to datum structure, and whether the requirement is demonstrated over 10 parts, 30 parts, or an entire production batch.
Why the drawing symbol alone is not enough
Many teams use concentricity when they actually need circular runout or total runout. This matters because the measurement burden, inspection time, and process implications differ. A requirement that looks small on paper can add 15%–40% to inspection effort if the datum strategy is difficult or if CMM verification is required for every lot.
In purchasing reviews, three questions usually clarify intent fast: what feature is function-critical, what failure mode is being prevented, and what inspection method will be accepted at receiving. If the answer to those questions is unclear, a tighter tolerance may only increase cost without increasing product reliability.
Core factors that shift achievable tolerance
- Material family: free-machining brass and some stainless grades behave differently from titanium, Inconel, or precipitation-hardened alloys.
- Geometry: under 3 mm diameter and long unsupported lengths typically tighten the process window.
- Operation count: single-setup parts usually hold axis relationships better than parts with transfer, back-working, or secondary grinding.
- Inspection strategy: shop-floor runout checks can support faster control, while CMM-based verification improves traceability but adds cycle time.
How tight is too tight in real production, not in theory?
The practical answer depends on function, geometry, material, and volume. For many swiss-turned components used in connectors, medical handles, valve pins, instrument shafts, and sensor housings, a concentricity-related requirement in the 0.01 mm to 0.03 mm range is often manageable when the process is stable and the part is designed for manufacturability. Once requirements approach 0.005 mm or below, cost sensitivity and scrap risk increase sharply unless the part is short, rigid, and made in a highly controlled process chain.
This is where “too tight” begins. A tolerance is too tight when it exceeds the functional need, collapses supplier options, or demands process controls disproportionate to application risk. In aerospace, defense, and high-speed rotating applications, tighter axis control may be justified because imbalance and uneven wear can shorten fatigue life. In less demanding assemblies, the same value may only create inspection bottlenecks and supplier qualification delays of 2–4 weeks.
For information researchers and decision-makers, the useful benchmark is not the smallest achievable number in a lab. It is the repeatable number a qualified supplier can maintain across material lots, machine shifts, and production quantities. That distinction is especially important when comparing prototype capability against serial production capability.
The table below summarizes common decision ranges. These are not universal guarantees; they are practical discussion bands used to frame RFQs, drawing reviews, and supplier conversations in precision machining programs.
The important reading of this table is economic as much as technical. Every step tighter reduces the supplier pool, increases setup sensitivity, and often extends first article preparation by several days. When tolerance drops from 0.02 mm to 0.005 mm, the jump is not linear; process risk and inspection burden tend to rise much faster than the number itself suggests.
Signals that the tolerance may be over-specified
A tolerance may be too tight if the feature is not part of a rotating interface, sealing line, optical path, or press-fit alignment. It may also be over-specified if the mating component itself has a looser positional stack or if assembly compensation already exists. In these cases, a redesign of datum structure or a shift to total runout can preserve function while cutting cost and lead time.
Another warning sign is when no one can define the accepted measurement method. If one supplier uses V-block runout, another uses a spindle fixture, and receiving inspection uses a CMM, disputes become likely even when the part is functionally acceptable.
What should engineers and buyers check before approving a tight tolerance?
The safest approach is to connect the drawing requirement to function, process capability, and inspection. A procurement team should not approve a swiss turning concentricity tolerance based only on quoted confidence. They should request a short capability package showing machine type, spindle runout control method, expected in-process checks, and whether the part is completed in 1 setup or multiple operations.
For operators and quality teams, cnc spindle runout measurement is a starting point, not the whole answer. A spindle may check well at idle, yet the finished axis relationship can drift because of tool pressure, thermal growth over 2–3 hours, guide bushing mismatch, or part pull during cutoff. Capability should therefore be validated at part level, not only machine level.
For enterprise decision-makers, the business question is whether this tolerance improves field reliability enough to justify longer validation cycles and narrower sourcing options. Tight tolerances are often reasonable in medical, aerospace, fluid control, and sensing hardware, but only when backed by use-case evidence such as vibration sensitivity, leakage risk, dynamic balance, or fatigue-related misalignment concerns.
The next table is useful during RFQ screening because it converts a drawing note into a sourcing checklist. It helps avoid a common failure mode: selecting a low quote from a supplier who can machine the geometry but cannot hold the axis relationship consistently across production lots.
A structured review like this typically shortens supplier clarification cycles and improves quote comparability. Instead of comparing prices alone, buyers compare process fit. That is especially valuable when projects involve AS9100-oriented aerospace work, ISO 13485-linked medical components, or sensor hardware where axis alignment affects signal integrity and assembly repeatability.
A practical 4-step approval flow
- Define the failure mode: vibration, leakage, wear, imbalance, or misalignment.
- Confirm the right GD&T control and datum structure with design and quality teams.
- Request sample capability data across at least one pilot lot, not a single showcase part.
- Lock the inspection method, sampling frequency, and reaction plan before purchase order release.
This flow is simple, but it prevents expensive downstream arguments. It also aligns well with TSV’s approach to engineering benchmarking: evaluate the actual process boundary, not a marketing headline.
Where do tight concentricity requirements make sense across industries?
Not all industries value tight swiss turning concentricity tolerance equally. In rotating or pressurized systems, axis accuracy often has a direct functional effect. In static housings or non-critical cosmetic parts, a looser value may perform identically in service. The challenge for sourcing teams is to distinguish real risk from inherited drawing habits.
Aerospace is one of the clearest cases where tighter control may be justified. Shaft-like pins, actuator elements, fluid metering components, and sensor carriers can see cyclical load, vibration, and thermal change across wide ranges. If misalignment contributes to uneven contact stress, fatigue life can degrade faster than expected, especially in high-strength alloys where surface condition and geometric accuracy interact.
Medical and analytical devices present a different logic. Tiny concentricity errors may affect smooth insertion, needle guidance, rotational feel, or instrument calibration. In these environments, repeatability from batch to batch can matter as much as the nominal value. A reliable 0.01 mm process is often more useful than an occasional 0.003 mm result that cannot be sustained.
Industrial automation, sensors, and edge hardware sit somewhere between these extremes. Encoder sleeves, valve spools, miniature shafts, and optical mounts may need controlled axis relationships, but the required level depends on speed, sealing, sensing resolution, and the stack-up of the full assembly.
Typical scenarios where tighter control adds value
- High-speed rotating components where imbalance and runout influence noise, wear, and bearing life.
- Miniature fluid-control parts where off-axis features can affect seal contact or metering consistency.
- Aerospace and UAV subcomponents exposed to vibration cycles, where axis error can magnify fatigue-sensitive load paths.
- Sensor and optical assemblies where misalignment alters calibration, signal path, or insertion force.
When a looser specification may be smarter
If the part is short, non-rotating, and assembled into a forgiving polymer or compliant fixture, a concentricity value tighter than 0.02 mm may offer little return. The same is true when the mating part itself carries larger variation. In these situations, engineering teams should consider whether circular runout, position, or even a better datum scheme can deliver the same field performance at lower total cost.
This is also where procurement can influence design quality. Asking for the functional reason behind a very tight requirement often uncovers opportunities to simplify the part, shorten lead time by 7–15 days, or widen supplier options without degrading end-use performance.
Common mistakes, FAQ, and why data-driven sourcing wins
One of the most common mistakes is assuming that tighter concentricity always means better quality. In reality, quality is the match between requirement and function. Another mistake is reviewing capability on a single polished sample while ignoring tool wear progression, machine warm-up behavior, and lot-to-lot material shifts. A third is separating engineering review from purchasing review, which often leads to expensive tolerances with unclear inspection acceptance.
The most effective organizations use a shared language across design, machining, quality, and sourcing. They define the intended function, lock the measurement method, and compare suppliers based on demonstrated process discipline. That is the logic behind TSV’s positioning as a data-driven hard-tech filter: remove adjectives, compare measurable limits, and make decisions from traceable parameters.
Below are concise answers to the questions most frequently raised by researchers, operators, buyers, and executives when evaluating swiss turning concentricity tolerance in production programs.
How should I choose between concentricity and runout?
Choose the control that best reflects the function and can be inspected consistently. If the concern is how a cylindrical feature behaves when rotated relative to a datum axis, circular runout or total runout is often more practical. If your team keeps debating acceptance results, revisit the GD&T choice before tightening the number.
What is a realistic lead-time impact of tighter tolerance?
For standard swiss-turned work, very tight axis controls can add several days for process development and first article validation. In complex materials or regulated sectors, qualification and metrology alignment can extend sourcing cycles by 2–4 weeks, especially if multiple suppliers need clarification on datums and acceptance method.
What should operators monitor on the shop floor?
Operators should monitor spindle condition, collet wear, guide bushing fit, insert wear pattern, part cutoff behavior, and thermal stability through the shift. Part-level checks at defined intervals are more informative than relying only on initial machine setup. For long-running batches, periodic verification every 30–60 parts may be justified for critical features, depending on cycle time and process sensitivity.
What do buyers need in a quote package?
At minimum, request the proposed process route, planned inspection method, expected first article timing, and any assumptions about material condition or secondary finishing. If the tolerance is below 0.01 mm, ask whether the quote includes additional metrology time, special fixturing, or tighter in-process controls. This prevents surprise cost increases after order release.
Why choose a data-first partner when tolerance decisions affect cost, risk, and supply chain speed?
When a drawing calls for aggressive swiss turning concentricity tolerance, the real challenge is not finding the boldest promise. It is identifying the process boundary that can be repeated in production, verified in inspection, and justified by application need. That is exactly where TSV creates value for engineering teams, procurement leaders, and technical decision-makers working across advanced manufacturing supply chains.
Our approach is built for teams that need more than generic supplier directories. We help translate tolerance questions into measurable decision criteria: parameter confirmation, correct control selection, process-route review, inspection-method alignment, and supply-chain benchmarking grounded in hard technical language rather than unsupported claims.
If you are evaluating a new precision-machined part, revising a specification, or comparing global suppliers, the most productive next step is a focused technical review. That review can cover 5 key items: drawing callout logic, achievable tolerance range, spindle runout and setup considerations, likely lead-time impact, and whether alternative controls could reduce cost without sacrificing function.
Contact TSV to discuss parameter confirmation, supplier capability screening, sample evaluation criteria, certification-sensitive sourcing contexts, delivery window expectations, and quote normalization for precision machining programs. For teams facing complex RFQs, cross-border sourcing, or tolerance disputes, a data-backed review can shorten trial-and-error cycles and turn engineering truth into purchasing confidence.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























