
Industrial Metrology Calibration Standards Explained for Audit Readiness
Publication Date
author
Industrial metrology calibration standards sit at the center of audit readiness because every inspection, release decision, and corrective action depends on trusted measurement data.
When tolerances tighten across aerospace parts, robotics assemblies, sensors, and precision machining, a weak calibration system quickly becomes a business risk.
That is why industrial metrology calibration standards matter beyond compliance. They support traceability, process control, supplier confidence, and defensible evidence during internal or external review.
In a market crowded with vague quality claims, the more practical question is simple: can every critical measurement be linked to a verified standard, a valid method, and a controlled interval?
What calibration standards actually govern
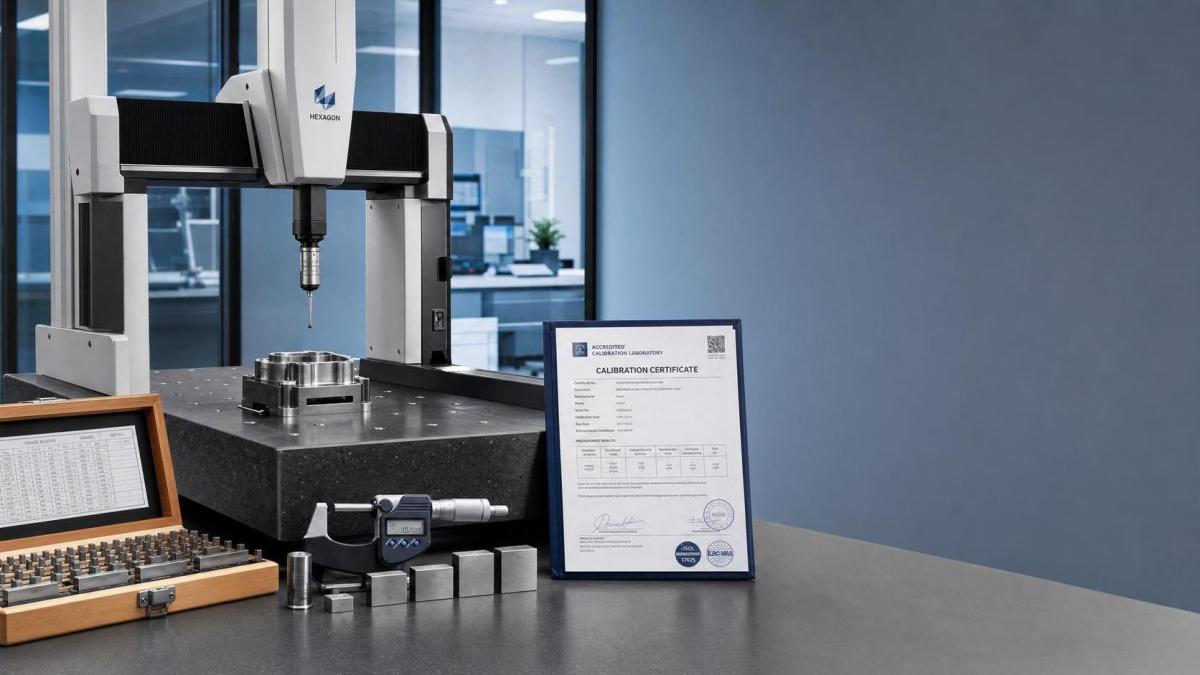
The picture is usually less about one instrument and more about the chain behind it.
Industrial metrology calibration standards define how measurement devices are checked, compared, adjusted, documented, and kept traceable to recognized references.
This applies to coordinate measuring machines, calipers, micrometers, torque tools, pressure gauges, temperature probes, laser systems, vision equipment, and dimensional masters.
The purpose is not merely to prove that a tool works. The purpose is to prove how well it works, under what conditions, and with what uncertainty.
A sound system usually combines international standards, internal procedures, accredited laboratory support, equipment history, and a documented decision rule for acceptance.
In practical terms, calibration answers three questions auditors often test indirectly: Was the instrument suitable, was it controlled, and can the result be trusted?
Why audit pressure has increased
Audit expectations are rising because manufacturing systems are now more automated, more distributed, and more dependent on digital records.
A single measurement may trigger machine compensation, supplier rejection, product release, or field risk assessment. That raises the cost of weak calibration discipline.
This is especially visible in sectors that TechStat Vanguard monitors closely.
In robotics and automation, repeatability claims mean little without calibrated reference artifacts and stable verification methods.
In UAV and aerospace work, structural fit, payload balance, and flight-critical dimensions require tighter traceability and clearer uncertainty evaluation.
In sensors and edge AI, calibration drift can distort machine vision accuracy, LiDAR alignment, or gateway timing validation.
In precision machining, audit findings often come from mismatch between tolerance claims and measurement capability.
The common thread is straightforward. Parameters do not speak for themselves. They need traceable proof.
The core elements auditors look for
Most audits do not fail because a single device is overdue. They fail because the control system around measurement is incomplete or inconsistent.
Industrial metrology calibration standards usually show up through these checkpoints:
- Clear identification of each instrument, standard, or reference artifact.
- Calibration status that is visible, current, and tied to records.
- Traceability to national or international standards through documented certificates.
- Defined intervals based on risk, usage, drift history, and environment.
- Measurement uncertainty appropriate to the tolerance being verified.
- Out-of-tolerance response rules, including impact review on prior product acceptance.
- Protection from damage, unauthorized adjustment, and uncontrolled software changes.
A strong audit trail also shows that calibration is linked to actual process risk, not handled as an isolated paperwork function.
Traceability is broader than a certificate
A certificate alone rarely settles an audit concern.
The record must connect the instrument, the method, environmental conditions, acceptance limits, uncertainty, technician competence, and the reference used.
Without that chain, traceability becomes a label instead of evidence.
How standards affect day-to-day operations
The value of industrial metrology calibration standards becomes clearer on the production floor than in the audit room.
If a bore gauge drifts, process capability may appear stable while actual dimensions move toward rejection.
If a vision system is not calibrated against a suitable artifact, false confidence can spread through automated inspection records.
If a torque device is calibrated at the wrong range, assembly integrity may be overstated.
Calibration standards therefore protect more than instrument accuracy. They protect the decisions built on those readings.
This has direct effects on scrap, rework, warranty exposure, investigation time, and supplier dispute resolution.
Common gaps behind nonconformance
Many nonconformances are predictable because they start with small disconnects between procedure and practice.
One frequent issue is applying the same interval to every device, regardless of usage intensity or historical drift.
Another is relying on vendor certificates without checking accreditation scope or method relevance.
A more subtle gap appears when acceptance limits ignore measurement uncertainty.
That may create a pass result on paper, even when the measurement system is not capable enough for the tolerance under review.
Digital records can create their own problems.
If software versions, offsets, or automated compensation factors are changed without control, the calibration history loses meaning.
Industrial metrology calibration standards are only effective when the full measurement environment is managed, including data handling.
Where fast-moving operations often slip
- Using shop-floor instruments outside their validated range.
- Skipping impact analysis after an out-of-tolerance result.
- Treating master artifacts as permanent references without wear review.
- Ignoring humidity, vibration, or temperature effects in sensitive measurements.
- Separating calibration records from production deviations and CAPA history.
A practical framework for audit readiness
A workable approach starts by ranking measurement points by product risk, not by instrument cost.
Critical dimensions, safety-related parameters, and release criteria should receive the strongest control.
From there, build a calibration map that links each instrument to process steps, tolerance limits, reference standards, and record owners.
This map helps expose missing links before an auditor does.
The next step is to review whether current industrial metrology calibration standards match actual use conditions.
A clean certificate means less if the instrument sees shock loading, contamination, heavy frequency of use, or unstable storage.
Finally, test your evidence chain with sample records.
Choose one critical instrument and confirm that anyone reviewing it can follow the full path from identification to calibration result to product decision.
Questions worth asking before the next inspection
- Does each critical measurement have a defined uncertainty requirement?
- Are intervals based on evidence, or only on historical habit?
- Can out-of-tolerance findings be traced to affected lots or reports?
- Do digital systems preserve calibration status after software updates?
- Are supplier-provided measurements held to the same traceability logic?
What deserves attention next
Industrial metrology calibration standards are becoming more strategic as factories rely on connected inspection, automated decisions, and tighter global qualification requirements.
The useful shift is to stop viewing calibration as an isolated support task and start treating it as measurement governance.
That perspective aligns with TSV’s broader position: engineering truth comes from verified parameters, controlled tolerances, and records that hold up under scrutiny.
A sensible next move is to review the highest-risk measurements first, compare current controls against recognized industrial metrology calibration standards, and close the gaps that could undermine audit confidence.
When the measurement chain is clear, traceable, and technically defensible, audit readiness becomes the result of good engineering practice rather than last-minute preparation.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)
 Oct 12, 2026What should be included in predictive maintenance pricing for factories?Predictive maintenance pricing for factories: compare sensors, software, integration, support, and total cost to secure measurable uptime gains and avoid hidden expenses.TSV Data Lab
 Oct 11, 2026How payload and reach change the cost of an industrial robotCost of industrial robot systems depends heavily on payload and reach. Learn how sizing, torque, tooling, safety, and lifecycle factors shape smarter automation investments.Chen Wei (Automation Lead Engineer)























