How Do You Verify That Precision Machined Parts Meet Tolerances?
Publication Date
author
To verify that precision machined parts meet tolerances, measure each specified characteristic using a suitable method, reproduce the drawing’s datum requirements, and apply an agreed acceptance rule that accounts for measurement uncertainty. A reading inside the tolerance limits is useful evidence only when the measurement setup can reliably distinguish an acceptable part from an unacceptable one.
Reliable precision machining tolerance verification therefore involves more than choosing between a micrometer and a coordinate measuring machine (CMM). The inspection method must match the feature, the required tolerance, and the condition in which the part will be accepted. A shaft diameter, a hole pattern, and a thin sealing surface can require very different approaches.
Start with the drawing: what must actually pass?
Before selecting equipment, establish the current drawing revision, units, general tolerances, material condition, and applicable geometric dimensioning and tolerancing (GD&T) conventions. Include drawing notes and referenced specifications in the inspection plan. They may define requirements that do not appear beside individual dimensions.
Separate size requirements from geometric requirements. A bore can have an acceptable measured diameter while its axis is incorrectly located. A plate can meet its thickness tolerance while failing flatness. Checking one characteristic does not establish compliance with another.
Datum references determine how many geometric checks must be performed. They establish the reference system used to evaluate the part. If an inspector aligns a hole pattern to whichever surfaces produce the smallest deviation, the resulting report may conceal an error relative to the specified mounting interfaces.
Acceptance must also occur at the correct manufacturing stage. Heat treatment, plating, anodizing, grinding, and other finishing operations can change dimensions or geometry. An inspection performed before a dimension-changing operation does not establish final compliance unless the requirement explicitly applies at that earlier stage.
A useful inspection plan connects every requirement to its measurement method, setup, inspection stage, and record. That connection makes omissions visible before parts reach final inspection.
Compare measurement methods by the feature they must verify
No instrument is the strongest choice for every characteristic. Simple tools can provide excellent results for accessible dimensions, while complex geometry may require coordinated measurement or specialized equipment.
For a turned shaft, a micrometer may be the practical choice for diameter control. Measurements at multiple axial and angular positions can reveal taper or variation, but they do not automatically constitute a complete roundness evaluation.
For a mounting bracket with a controlled hole pattern, a CMM can evaluate the holes relative to the specified datums. The report should show the required geometric result; separate coordinate deviations may not be enough to demonstrate compliance with the complete position requirement.
For repeated production of a mating feature, a correctly designed functional gauge can make acceptance faster. Its value depends on representing the specified functional boundary. Trying the part in an arbitrary mating component provides weaker evidence because that component has its own dimensional variation and wear.
Select the method by what it must detect. An instrument that measures diameter accurately may still be unsuitable for proving hole location, surface texture, or full geometric form.
Why a CMM report can still give the wrong impression
A CMM provides powerful measurement capability, but its output reflects the inspection program. A polished report cannot compensate for an unsuitable alignment or an incomplete sampling strategy.
Consider a housing whose mounting face establishes the primary datum. The inspection setup must establish that reference in a way consistent with the drawing. Replacing the required datum alignment with an unrestricted best fit can redistribute errors and make a nonconforming feature appear closer to nominal.
Point distribution matters as well. A sparse set of touches can miss local surface variation between sampled locations. Scanning collects more information, although it still requires appropriate probe settings, filtering, and evaluation. More data helps only when it represents the characteristic being assessed.
For critical features, the inspection record should identify the datum alignment, measurement locations or scanning approach, and relevant evaluation settings. If suppliers report different results, these details often explain the disagreement more effectively than comparing equipment brands.
Resolution, calibration, and uncertainty answer different questions
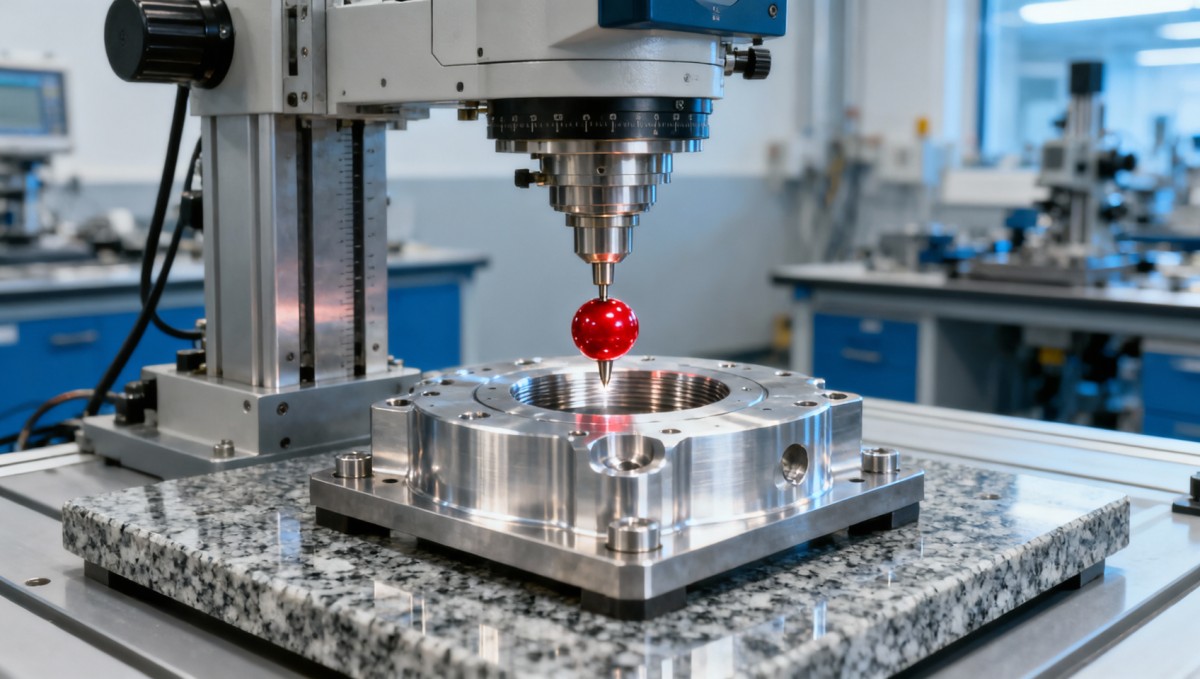
Resolution is the smallest increment an instrument displays or resolves. It does not establish how closely the result represents the actual dimension. Additional decimal places can make an uncertain result look more convincing without improving it.
Calibration establishes the relationship between an instrument’s indications and reference values under specified conditions. A current calibration record supports confidence in the instrument, but the actual task also includes the fixture, part, environment, operator, and method.
Measurement uncertainty describes the uncertainty associated with the reported result. For a particular inspection, relevant contributors can include instrument performance, repeatability, temperature, alignment, contact force, and the method used to sample the surface.
When comparing inspection options, ask whether the complete measurement process has sufficiently small uncertainty for the tolerance being assessed. A broad tolerance may be straightforward to verify with shop-floor equipment. A narrow tolerance may require controlled conditions, a different method, or both.
Borderline results need an agreed decision rule. Under a guard-banded acceptance rule, the acceptance limits are set inside the specification limits to reduce the risk of accepting a nonconforming part. Other rules allocate decision risk differently. The rule should be established before inspection, particularly when results are close to a limit.
A result that does not demonstrate conformity under the chosen rule may require further evaluation; it should not automatically be described as proven nonconforming. Keep the measured value, uncertainty, and acceptance decision distinct in the record.
Control the conditions that can change the verdict
Temperature can change both part dimensions and measuring equipment behavior. A component brought directly from machining may still be cooling, and a large part can retain temperature gradients after its surface feels stable. Measurements should relate to the specified reference conditions, using appropriate stabilization or validated compensation.
Material matters because different materials expand by different amounts. Compensation also depends on suitable material data and representative temperature measurements. It cannot reliably correct an unknown temperature gradient throughout a component.
Clamping can create another source of disagreement. A thin wall may distort under fixture force, while a soft component may deform under a probe or micrometer. The inspection setup must reflect any specified restrained or free-state condition. Otherwise, it may measure the effect of the fixture as much as the manufactured geometry.
Cleanliness and surface condition deserve the same attention. Chips under a datum face, residue in a bore, or a burr at an edge can alter readings. Clean the part using an appropriate method, and distinguish removable contamination from an actual manufacturing defect. Inspection preparation should not alter the feature to obtain a passing result.
If two methods disagree, compare their setups before deciding which reading to trust. Check whether they measured the same locations, used the same references, and applied comparable contact forces and environmental conditions.
First article, sampling, or full inspection?
These approaches answer different questions. A first article inspection establishes whether the evaluated manufacturing output meets the documented requirements. It can reveal misunderstood dimensions, missing operations, and inspection gaps before production continues. It does not establish that every later part will conform.
Sampling reduces inspection effort, but its usefulness depends on the sampling plan, lot definition, process behavior, and consequences of an escaped defect. A passing sample supports a lot acceptance decision under the plan; it does not prove that every unmeasured part is acceptable.
Full inspection checks every part for the selected characteristics. It can be appropriate for critical features or unstable processes, but it still depends on a capable measurement system. An unsuitable method can repeatedly miss the same defect, even when every component passes through inspection.
A practical strategy often combines detailed initial verification, production checks that respond to tool wear or process changes, and final acceptance checks on selected characteristics. Inspection intensity should reflect feature risk and evidence of process control.
Process capability data can support this strategy when the process is stable and the measurement system is adequate. A capability index alone does not prove compliance with all drawing requirements, particularly geometric characteristics that were never included in the study.
What a useful inspection report should contain
A supplier’s inspection report should make the acceptance decision reproducible. A document containing only nominal dimensions and a column of “pass” entries provides little basis for assessing a tight tolerance or investigating an assembly problem.
Look for the following information:
- Part identity: part number, drawing revision, and traceable lot or serial identification.
- Requirement mapping: each reported result linked to a drawing characteristic, with its tolerance and units.
- Actual results: measured values where applicable, plus clear identification of limit-gauge or functional-gauge checks.
- Measurement basis: equipment identification, relevant calibration status, datum setup, and inspection method.
- Acceptance context: manufacturing stage, inspection coverage, and the decision rule where uncertainty affects acceptance.
- Disposition: identification of deviations and any documented authorization affecting acceptance.
Detailed method records need not accompany every routine shipment, but they should be available for critical requirements or disputed results. A report should also distinguish measurements from an initial sample from those obtained on the delivered production lot.
Quality management certifications support assessment of a supplier’s systems; they do not specify the tolerances for an individual component or replace dimensional evidence. Compliance still depends on the drawing, the measurement process, and the results associated with the parts being accepted.
Before ordering, agree on the critical characteristics, inspection stage, datum setup, measurement methods, and required records. For a borderline result, resolve uncertainty and the acceptance rule before authorizing shipment. That preparation gives both parties a common basis for deciding whether the parts meet the requirements—and makes inspection evidence useful when the assembly must work.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)
 Oct 19, 2026How Do You Verify That Precision Machined Parts Meet Tolerances?Master precision machining tolerance verification with the right tools, datum setups, and acceptance rules. Learn how to validate parts confidently and reduce costly inspection errors.Dr. Marcus Vance
 Oct 18, 2026What Should an AS9100 Machining Supplier Checklist Include?Build an AS9100 machining supplier checklist that verifies capability, traceability, inspection, and outsourced processes. Discover what to check before approving your next aerospace supplier.Dr. Marcus Vance
 Oct 17, 2026How Should You Interpret Industrial Robot Repeatability Specs?Decode industrial robot repeatability specifications, understand ISO 9283 test conditions, and avoid costly selection mistakes. Learn how to verify performance for your process.Chen Wei (Automation Lead Engineer)
 Oct 16, 2026How Can You Fairly Compare MTBF Across Industrial Servo Motors?Make a fair industrial servo motor MTBF comparison with matched operating profiles, failure criteria, and confidence bounds. Discover how to assess reliability beyond advertised numbers.Chen Wei (Automation Lead Engineer)
 Oct 15, 2026How Should You Compare TechStat Vanguard 5-Axis CNC Tolerances?TechStat Vanguard 5-axis CNC tolerance comparison: learn how to verify part accuracy, assess inspection evidence, and choose suppliers that reliably meet your drawing requirements.Dr. Marcus Vance
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)