
PLC control for packaging machinery and timing drift
Publication Date
author
In packaging lines, even small timing drift can trigger misfeeds, seal defects, and costly downtime. This article examines how plc control for packaging machinery can reduce synchronization errors, improve cycle stability, and support data-driven troubleshooting. For engineers, operators, buyers, and decision-makers, it offers a practical view of control logic, root-cause analysis, and upgrade paths aligned with real production demands.
For high-speed packaging operations, timing is not an abstract software issue. It is a measurable production variable that affects film registration, product spacing, seal integrity, reject rate, and line utilization. A drift of just 10–30 ms can be enough to create recurring faults on intermittent-motion and continuous-motion machines, especially when conveyors, servo axes, pneumatic actuators, and sensors are not coordinated under a stable control architecture.
In a B2B environment shaped by tighter throughput targets, labor constraints, and traceability requirements, the value of plc control for packaging machinery is not only in machine start-stop logic. It lies in deterministic execution, repeatable sequencing, fault diagnostics, and data visibility that help teams distinguish between control problems, mechanical wear, electrical noise, and process mismatch.
From TSV’s engineering-first perspective, the right question is not whether a machine is marketed as “smart,” but whether its control layer can hold timing consistency within the tolerance window required by the packaging process. That is the baseline for stable output, faster changeovers, and more reliable supplier evaluation.
Why timing drift matters in packaging machinery control
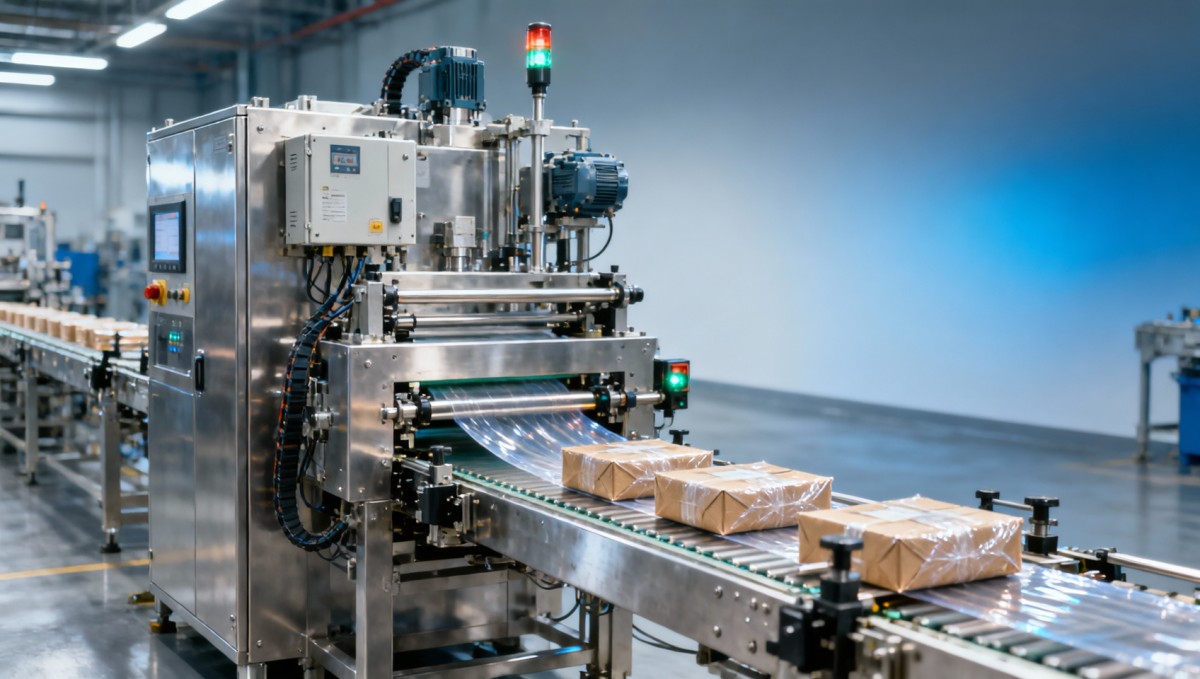
Timing drift in packaging systems refers to a gradual or intermittent loss of synchronization between machine events. In practical terms, a photoeye may detect a product at the right point, but the jaw closes 20 ms late, or a cartoner flight arrives 15 mm out of position because the axis command and actual motion no longer match under load. These errors often begin small, then compound across multiple stations.
The risk profile depends on machine type. On a form-fill-seal line, drift may distort cut position and seal geometry. On a labeling or coding station, it may cause print-to-pack mismatch. On case packing or pick-and-place systems, drift can produce dropped products, skewed infeed timing, or unplanned e-stops. At speeds of 60–300 packs per minute, even minor timing instability can create measurable scrap within a single shift.
For operators, the first visible symptom is usually nuisance faults or inconsistent machine behavior across different SKUs. For maintenance teams, the challenge is that timing drift does not always originate in the PLC itself. It may come from encoder slip, scan-time variation, weak grounding, valve response lag, mechanical backlash, or poor task prioritization in the control program.
For procurement and decision-makers, this is why machine evaluation should include more than nominal throughput. A line rated at 180 ppm but drifting during 3-shift production may deliver lower effective output than a 150 ppm system with tighter synchronization and fewer short stops. OEE, reject rate, mean time between intervention, and recipe repeatability often tell a more useful story than headline speed alone.
Typical operational symptoms
Teams investigating plc control for packaging machinery should look for patterns rather than isolated alarms. The following symptoms are commonly associated with timing drift:
- Seal or cut position shifting by 2–5 mm over a production run
- Product gaps becoming inconsistent after speed changes above 70% of rated output
- Reject spikes during acceleration, deceleration, or recipe transitions
- Frequent sensor timeouts without confirmed hardware failure
- Servo following errors or registration correction loops working harder than usual
Operational impact by machine section
The table below shows how timing drift typically appears at different packaging stations and why the source is often cross-functional rather than isolated to one device.
The key takeaway is that timing drift is rarely a single-point failure. Stable packaging performance usually depends on the interaction between PLC task design, motion control, sensor quality, network timing, and mechanical condition. That is why troubleshooting must follow the process chain rather than chase alarms one by one.
How PLC architecture reduces synchronization errors
Effective plc control for packaging machinery begins with deterministic execution. In many packaging applications, the PLC must manage event timing in the 1–20 ms range while also handling HMI communication, recipe logic, safety interlocks, and diagnostics. If all functions compete in a flat program structure, cycle jitter becomes more likely, especially when production speed rises or optional devices are added later.
A stronger architecture separates critical motion and machine-state logic from lower-priority tasks. High-speed event processing should be tied to motion interrupts, hardware timestamps, or dedicated periodic tasks where supported. Non-critical functions such as reporting, HMI screen refresh, or non-urgent alarms should not consume the same timing path used for seal jaws, registration correction, or synchronized product transfer.
Servo-based packaging equipment also benefits from a consistent master reference. When multiple axes depend on line speed, virtual master axes or electronic line shafts often provide better repeatability than loosely linked start-stop signals. This is especially relevant where one machine platform must run 5–10 product formats with different pitch, dwell, and acceleration profiles.
From a data perspective, robust PLC design should expose actual cycle time, event timestamps, fault sequence records, and key counters for analysis. Without these data points, teams may spend days replacing sensors or valves when the root issue is task overload or badly sequenced logic. A packaging line that stores the last 100–500 alarm events with time context is easier to stabilize than one that reports only a generic stop condition.
Control design elements that matter most
- Use periodic or event-driven tasks for critical timing operations instead of relying only on a continuous scan.
- Align sensor filtering and debounce settings with actual machine speed; a fixed filter may be acceptable at 40 ppm but fail at 180 ppm.
- Apply axis synchronization strategies that include acceleration and deceleration behavior, not just steady-state speed matching.
- Separate machine-state logic, motion commands, and diagnostics into structured function blocks for faster validation and troubleshooting.
- Log timing-related variables such as scan time, trigger latency, axis following error, and reject events by recipe and batch.
Recommended engineering checkpoints
When reviewing a new or retrofit system, technical teams should define target tolerances up front. For example, acceptable registration error may be within ±1 mm, acceptable command-to-actuation delay within 5–15 ms, and normal scan-time variation within a narrow band appropriate to the controller platform. These targets make FAT and SAT discussions more objective.
For buyers and plant managers, this is also where supplier transparency matters. Ask whether the control system supports timestamped diagnostics, motion trend capture, remote troubleshooting, and recipe version management. These functions do not replace good mechanics, but they shorten fault isolation time and reduce dependence on tribal knowledge.
Root-cause analysis: separating PLC issues from mechanical and electrical drift
One of the biggest mistakes in packaging troubleshooting is assuming that repeated timing faults automatically mean the PLC program is wrong. In reality, timing drift often emerges from the boundary between digital control and physical motion. A well-written sequence can still fail if a pneumatic cylinder response changes by 25 ms due to pressure drop, or if an encoder coupling slips after thermal cycling and washdown exposure.
A practical troubleshooting method starts by classifying drift as constant, speed-dependent, load-dependent, or random. Constant offset may indicate recipe setup or calibration issues. Speed-dependent faults often point to motion tuning, sensor response, or task scheduling. Load-dependent drift may come from tension variation, worn gearboxes, or inconsistent product presentation. Random faults are frequently linked to wiring noise, unstable power, loose connectors, or intermittent device health.
For operators, simple observations remain valuable. Does the fault appear only above 120 ppm? Does it worsen after 2 hours of runtime? Does it occur during one SKU with a heavier product or different film? These patterns help engineers decide whether to inspect code execution, axis tuning, air supply stability, or wear components first.
For engineering managers, a repeatable analysis workflow can reduce downtime by hours per event. Instead of replacing multiple parts blindly, the team captures timing traces, checks machine-state transitions, compares commanded and actual axis positions, and reviews recent maintenance activity. Even a 3-step logging discipline can prevent recurring misdiagnosis.
Diagnostic framework for timing drift
The following table outlines a field-friendly approach for identifying where drift is most likely to originate and what to verify first.
This framework helps teams avoid over-attributing problems to software. In many plants, the fastest route to stable plc control for packaging machinery is to combine control review with a disciplined inspection of motion hardware, field wiring, pneumatic consistency, and recipe control.
Common misinterpretations
- A faster PLC does not automatically solve drift if the root cause is poor encoder mounting or loose product tracking logic.
- Replacing sensors without reviewing debounce and trigger alignment often shifts the symptom without removing the cause.
- Higher machine speed can expose existing instability that was already present at lower throughput but hidden by larger process tolerance.
Upgrade paths, selection criteria, and procurement guidance
Not every packaging line requires a full control-system replacement. In many cases, the best investment is a targeted upgrade focused on the highest-risk timing links. That may include replacing aging I/O modules, adding encoder feedback, migrating from relay-heavy sequences to structured PLC logic, or integrating servo control where mechanical cam timing can no longer hold tolerance across multiple SKUs.
For buyers, the right level of investment depends on throughput targets, product variation, validation requirements, and support model. A low-mix line running 40–60 ppm may be stable with simpler architecture. A high-mix line running 150–250 ppm across 8 or more formats usually needs better event timing, recipe control, and diagnostics to keep downtime manageable. The financial test is not purchase price alone, but total cost of instability over 12–36 months.
Decision-makers should also weigh serviceability. If only one programmer can modify the line, each changeover or fault event becomes expensive. Standardized code structure, documented I/O mapping, clear alarm history, and secure remote support often deliver more operational value than a complex feature set that local teams cannot maintain.
In TSV-style evaluation, useful supplier questions include: What timing variables can be logged? What is the normal response time for remote diagnostics? How are recipes version-controlled? What acceptance criteria are used for speed ramp-up, registration stability, and recovery after stop-start cycles? These questions move the discussion from marketing language to measurable performance.
Comparison of common upgrade approaches
The table below can help engineering and procurement teams frame an upgrade path based on production risk, expected benefit, and implementation complexity.
The best option depends on whether drift is structural or localized. A disciplined site assessment can often identify the top 20% of issues causing 80% of production loss. That creates a more credible business case than replacing everything at once.
Procurement checklist for technical buyers
- Define acceptable tolerance windows for seal position, registration, spacing, and recovery after stop-start cycles.
- Ask for controller diagnostics capability, including event logs, timestamp resolution, and trend visibility.
- Review spare-part availability, software backup policy, and expected support response within 24–72 hours.
- Confirm FAT and SAT criteria using actual product formats, not only dry-cycle tests.
- Check whether the supplier can support phased upgrades to reduce installation risk and production disruption.
Implementation, maintenance, and practical FAQ for long-term stability
A stable control platform is only part of the answer. Long-term performance depends on commissioning discipline, maintenance routines, and ownership of data. During implementation, teams should validate timing under at least 3 conditions: nominal speed, maximum qualified speed, and recovery after stop-start interruptions. Each condition should be tested across representative SKUs, not just the easiest product.
Maintenance plans should include more than lubrication and sensor cleaning. Packaging lines with recurrent timing issues often need periodic checks on encoder coupling integrity, air pressure stability, servo following error trends, and recipe governance. A monthly review of reject patterns and alarm frequency can reveal drift long before it becomes a shutdown event.
For plant leadership, one practical target is to reduce time-to-diagnosis rather than promise zero faults. If a line can move from 2–3 hours of uncertain troubleshooting to 20–40 minutes of evidence-based diagnosis, the improvement is economically meaningful. That is especially true in facilities where labor availability and product traceability are under pressure.
The broader lesson is clear: plc control for packaging machinery should be treated as an engineering system, not just a programming task. Stable timing is the result of aligned software logic, reliable field devices, predictable mechanics, and disciplined operational feedback.
FAQ: How often should timing performance be reviewed?
For high-speed or multi-SKU lines, a weekly review of reject trends and timing alarms is sensible, with a deeper monthly technical review. Lines running above 120 ppm or changing formats several times per week usually benefit from tighter monitoring than low-mix systems.
FAQ: Is a PLC upgrade always necessary when timing drift appears?
No. If the drift comes from loose mechanics, unstable air supply, poor grounding, or bad recipe control, upgrading the PLC alone may not solve it. A structured assessment should confirm whether the bottleneck is execution timing, feedback quality, motion response, or physical wear.
FAQ: What delivery and commissioning window is common for upgrades?
Targeted software or I/O improvements may fit within 1–3 weeks, while larger migrations can require 4–12 weeks depending on hardware lead time, FAT scope, and production scheduling. Plants with validation or regulated documentation needs should allow additional time for approval and training.
FAQ: Which metrics should management track after implementation?
Track at least 4 metrics for 8–12 weeks: reject rate, micro-stop frequency, mean time to diagnose, and repeatability across recipes. If possible, add event-timestamp quality and changeover stability. These measurements show whether the upgrade improved real production behavior rather than only machine perception.
For manufacturers seeking better control transparency, lower downtime, and more reliable supplier evaluation, a disciplined approach to timing drift creates immediate operational value. The strongest solutions are not defined by promotional claims but by measurable synchronization, maintainable architecture, and clear diagnostic evidence. If you are reviewing a packaging line upgrade, planning a retrofit, or comparing machine suppliers, contact us to discuss a tailored control assessment and explore solutions grounded in engineering data.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























