
Micro machining parts supplier mistakes that show up in inspection
Publication Date
author
A micro machining parts supplier can look qualified on paper yet fail where it matters most: inspection. From micro machining tolerance limits and 5 axis cnc surface finish ra to edm surface integrity analysis and cnc milling chatter frequency analysis, small process mistakes leave measurable traces. This guide shows buyers, engineers, and decision-makers how to spot the warning signs early and reduce qualification risk.
Why do inspection failures reveal more than a supplier brochure?
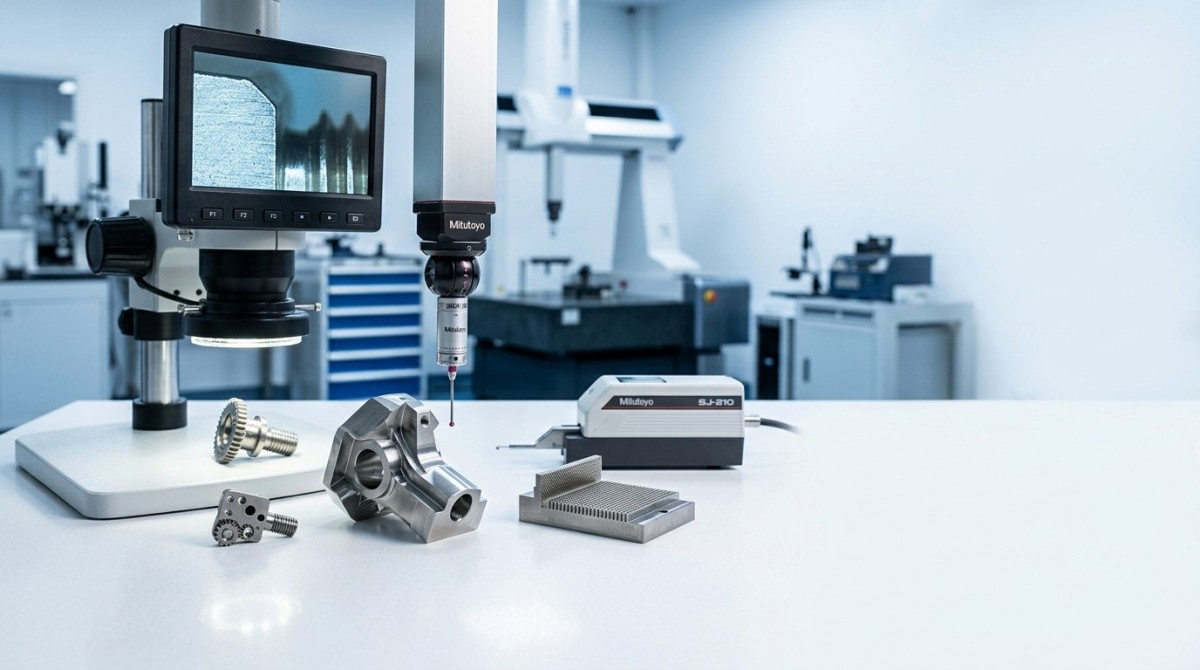
In micro machining, inspection is not just a pass-or-fail gate. It is a forensic tool. A capable micro machining parts supplier should be able to connect drawing requirements, process capability, machine condition, tooling strategy, and final measurement results into one traceable chain. When that chain breaks, inspection exposes it quickly through dimensional drift, burrs, unstable surface roughness, edge breakout, recast layers, or inconsistent lot-to-lot repeatability.
This matters across aerospace, medical, robotics, optics, sensors, and precision automation. In these sectors, one feature may be measured in tens of microns, one hole may control alignment, and one surface can affect sealing, friction, conductivity, or fatigue life. A supplier that talks only about “high precision” without discussing process windows, measurement methods, or capability evidence often creates qualification risk that appears after sample approval or during incoming inspection.
For procurement teams, the problem is practical. You may compare 3–5 suppliers with similar claims, similar lead times of 2–4 weeks, and similar quotations. Yet the true difference appears when you ask how they control micro machining tolerance limits, how they verify 5 axis CNC surface finish Ra, or how they detect chatter before geometry moves out of tolerance. Inspection data turns marketing language into engineering evidence.
This is also where a data-driven review model matters. TechStat Vanguard focuses on engineering truth rather than adjectives. For buyer qualification, that means asking for measurable thresholds, inspection plans, and traceable process controls. Parameters do not lie. If a supplier cannot define the measurement method, the control frequency, or the risk threshold, the part may still be manufactured, but it is not yet under control.
The inspection-first mindset for supplier evaluation
A strong supplier review starts by reversing the usual sequence. Instead of asking what machines they own, ask what defects are most likely to appear at inspection and how they prevent them within the first article, pilot lot, and recurring batch stages. A practical qualification cycle usually has 3 stages: drawing review, sample validation, and production monitoring. Each stage should have documented measurement outputs.
- At drawing review, confirm critical-to-function features, tolerance stack, datum strategy, and material condition before release.
- At sample validation, compare dimensional results, surface condition, burr control, and edge quality against actual use requirements.
- At production monitoring, verify repeatability over at least several setups or multiple lots rather than a single “best sample.”
For operators and engineers, the value is equally direct. If the supplier understands how inspection findings map back to spindle dynamics, electrode wear, fixture stress, coolant delivery, or tool runout, corrective action can happen within hours instead of after multiple rejected lots. That reduces trial-and-error cost and shortens qualification cycles.
Which supplier mistakes most often show up in micro machining inspection?
Most inspection failures are not random. They are signatures of upstream process choices. A micro machining parts supplier may have adequate equipment but still fail because process discipline is weak. Common issues include using unstable workholding on thin-wall geometry, selecting aggressive cutting parameters on micro features, ignoring heat accumulation in EDM, or treating deburring as a cosmetic step rather than a dimensional risk.
The table below organizes the most common mistakes by the inspection symptom they create and the commercial risk they trigger. This structure helps procurement, quality, and engineering teams review quotations and supplier audit responses using the same framework.
These failures are especially costly because they often appear late. A supplier may produce one acceptable sample with a fresh tool and careful setup, then lose control when the batch reaches 20, 50, or 200 pieces. That is why incoming inspection should be linked to process capability discussion, not treated as an isolated quality activity.
Dimensional errors are only the first layer
Buyers often focus first on nominal dimensions and tolerances, but micro machining inspection should go further. Surface integrity, edge condition, and residual process effects can be more important than size alone. A 20 µm dimensional deviation is easy to see on a report. A hidden microcrack, smeared edge, or heat-affected layer is harder to spot but can cause field failure.
This is why supplier qualification should separate at least 4 inspection layers: geometry, surface roughness, edge quality, and material/process integrity. In regulated or high-reliability sectors, these layers often define whether a part works under fatigue, vibration, sterilization, thermal cycling, or repeated actuation.
Warning signs during sample review
- Inspection reports list dimensions but omit measurement equipment, probe strategy, or sampling frequency.
- Surface finish is stated as “fine” or “smooth” without Ra range, cutoff method, or area of measurement.
- Deburring is performed manually with no defined edge-break window, increasing variation lot to lot.
- Corrective action is described in general terms rather than tied to a measurable process change.
If 2 or more of these signs appear in the same audit or sample review, qualification should slow down until the supplier provides a more rigorous control plan. A low unit price rarely offsets the cost of delayed launches, line stoppage, or repeated source changes.
What should buyers check for tolerance, surface finish, and EDM integrity?
A useful supplier review should test whether the vendor can explain not only the target specification but also the process route used to reach it. For micro machining tolerance limits, ask how capability changes by material, feature depth, wall thickness, and batch size. For example, repeatability on aluminum micro pockets may differ significantly from stainless steel or titanium because tool load, heat, and burr behavior change.
For 5 axis CNC surface finish Ra, the right question is not “Can you achieve low Ra?” but “Under what geometry, material, step-over, and tool condition can you maintain the required Ra consistently?” Complex freeform surfaces, steep walls, and miniature radii often create different roughness behavior within the same part. A single average number does not describe real process capability.
For EDM surface integrity analysis, buyers should review whether the supplier distinguishes roughing, semi-finishing, and finishing passes. Surface integrity depends on pulse energy, flushing, electrode condition, and final skim strategy. If the supplier cannot describe the expected recast risk, white layer tendency, or post-process inspection route, the process may still meet dimensions while failing durability expectations.
The checklist below helps align engineering and sourcing teams before issuing RFQs or approving samples. It covers 6 key inspection items that commonly separate a stable micro machining parts supplier from one that only performs well on isolated trials.
When suppliers answer these questions with process-specific details rather than generic confidence statements, qualification becomes faster and less risky. Even when exact values differ by part family, the discipline of the answer reveals maturity. Good suppliers talk in ranges, control points, and method limitations, not slogans.
How CNC milling chatter frequency analysis supports inspection stability
Chatter is one of the clearest examples of a process issue that leaves visible inspection traces. On micro features, even small vibration can alter edge sharpness, wall waviness, slot geometry, and surface roughness. If a supplier only reacts after parts fail surface or profile inspection, the root cause remains expensive. If the supplier monitors spindle-tool-workholding behavior during setup, defects are reduced before measurement.
For buyers, this does not mean requesting advanced machine data from every source. It means checking whether the supplier has a structured approach: test cuts, parameter revision, tool stick-out control, and documented setup windows. In practice, a disciplined process review over the first 1–3 setups is often more valuable than a polished presentation about machine quantity.
How should procurement teams compare suppliers before placing repeat orders?
After a sample passes, the bigger question begins: can the supplier repeat the result under normal production pressure? This is where procurement teams should move from one-time sample approval to a weighted comparison model. The goal is not simply to find the lowest quoted part price, but to reduce the total cost of qualification, incoming inspection, rework, line disruption, and supplier switching.
A practical scorecard uses 5 dimensions: technical clarity, process control, inspection transparency, change responsiveness, and commercial reliability. This is especially important for organizations sourcing for multiple plants, cross-border programs, or mixed portfolios such as aerospace hardware, robotic mechanisms, sensor housings, and medical assemblies. A supplier that performs well in one prototype project may struggle in ongoing delivery if process governance is weak.
The comparison matrix below is designed for information researchers, operators, buyers, and decision-makers to use together. It turns abstract supplier evaluation into a measurable review process that can be updated every quarter or at each major design revision.
The matrix is useful because it captures what inspection alone cannot. A part can pass once and still be commercially unstable. Repeat-order success depends on whether the supplier manages changes in material batch, tool life, setup variation, operator shift, and fixture wear. Those variables usually emerge over 2–3 production cycles, not during the first sample run.
A 4-step procurement screening method
- Request a drawing-based risk review before requesting price confirmation.
- Validate sample parts with both dimensional and surface integrity checks.
- Review repeatability over more than one setup, lot, or delivery cycle.
- Approve for volume only after nonconformance handling and communication speed are tested.
This method protects budgets. It also gives enterprise decision-makers a clearer way to compare apparent low-cost options against suppliers that may quote slightly higher but reduce hidden quality cost across the full program lifecycle.
Which standards, documentation, and process evidence matter most?
Standards and certifications matter, but they should be treated as a starting point rather than a final answer. In precision machining programs linked to aerospace, medical, or high-reliability industrial systems, buyers may review frameworks such as AS9100 or ISO 13485 depending on product category and regulatory context. However, a certificate does not automatically prove micro feature control, EDM surface integrity discipline, or superior inspection planning.
What matters more is whether documentation reflects actual process behavior. A useful supplier dossier should include at least 4 evidence groups: drawing review output, process flow, inspection plan, and nonconformance response logic. For high-risk parts, add material traceability, outsourced special-process controls, and revision management records. These documents shorten technical review and reduce misunderstanding between engineering and sourcing teams.
TechStat Vanguard’s data-driven approach is particularly valuable here because it separates label value from engineering value. Instead of asking whether a supplier sounds advanced, ask whether they can support the spec sheet with measurable controls. In hard-tech procurement, trust is built through tolerances, thresholds, and traceability, not through broad branding claims.
For multinational teams, this discipline also improves communication. When supplier evaluation is based on 5–7 clearly defined control items, cross-functional reviews become faster. Quality teams know what to measure, operators know what to protect, and procurement knows what to negotiate without weakening technical requirements.
Documents worth requesting before supplier approval
- A first article or sample inspection format showing actual measured values, not only pass marks.
- A process flow identifying where critical dimensions and surface features are created and verified.
- A control plan that states sampling frequency, escalation steps, and re-inspection triggers.
- A revision control method to prevent mixing obsolete drawings, tools, or setup instructions.
If a supplier can provide these materials quickly, discuss them clearly, and link them to actual inspection outcomes, qualification confidence rises. If they avoid documentation and rely mainly on verbal assurances, incoming inspection is likely to carry a higher burden in the first 30–90 days of supply.
FAQ and next step: how to reduce qualification risk with a data-driven review
Many teams searching for a micro machining parts supplier are not looking for generic capability claims. They need faster answers on qualification risk, inspection readiness, and how to compare suppliers without wasting engineering time. The questions below address the most common decision points before RFQ release or repeat-order approval.
How should we evaluate a micro machining parts supplier if sample quantities are small?
Use a layered review. Even if the initial quantity is only 5–20 pieces, check more than dimensions. Review surface finish consistency, burr behavior, measurement method, and the supplier’s explanation of process limits. Small sample sizes can hide instability, so ask how the same part will be controlled over the next 2–3 lots. The maturity of that answer is often more important than the first sample alone.
What is a common mistake when reviewing 5 axis CNC surface finish Ra?
A common mistake is accepting one Ra number without checking where and how it was measured. On complex surfaces, roughness may vary by toolpath direction, slope angle, or tool access. Always confirm the measurement location, instrument method, and whether the reported value represents a critical functional zone or only the easiest area to machine.
Why does EDM surface integrity analysis matter if dimensions already pass?
Because dimensional conformance does not guarantee material integrity. EDM can leave recast effects or thermal damage if finishing strategy is weak. For parts exposed to fatigue, motion, pressure, or repeated sterilization cycles, hidden surface damage may reduce service life even when the inspection report shows dimensions within tolerance. That is why high-reliability programs treat geometry and surface integrity as separate approval gates.
How long does supplier qualification usually take?
For standard industrial parts, initial screening to sample review may take 2–6 weeks depending on drawing clarity, material lead time, and inspection complexity. For tighter micro machining tolerance limits, multi-operation parts, or regulated sectors, the cycle can be longer because process validation and documentation review take more effort. A realistic schedule is better than a rushed approval followed by repeated quality escapes.
Why choose a data-driven evaluation partner?
Because hard-tech sourcing becomes expensive when teams qualify on language instead of evidence. TechStat Vanguard helps engineering, procurement, and leadership teams filter supplier claims through measurable criteria: tolerance interpretation, inspection logic, surface integrity discussion, traceability depth, and process benchmarking. That reduces information noise and supports better decisions across robotics, aerospace, sensors, automation, and precision machining programs.
If you need support, the most useful next conversation is specific. Ask for parameter confirmation on critical dimensions, review of micro machining tolerance limits, guidance on 5 axis CNC surface finish Ra, discussion of EDM surface integrity analysis, clarification of CNC milling chatter frequency analysis expectations, or a structured comparison of supplier qualification risk. You can also request input on lead time windows, sample strategy, drawing review priorities, certification expectations, and quotation alignment before committing to a new source.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 20, 2026KUKA Launches iiQKA.AI Vision to Simplify Industrial Image ProcessingKUKA iiQKA.AI Vision simplifies industrial image processing with controller-based 2D and 3D vision. Explore drag-and-drop setup for vision-guided automation.TSV Data Lab
 Oct 20, 2026Smart Industrial Edge Devices: Key Criteria for Legacy PLC IntegrationChoose smart industrial edge devices for legacy PLC integration. Discover key criteria for compatibility, data quality, security, and reliable collection without disrupting control.TSV Data Lab
 Oct 19, 2026Choosing a Radar Sensor by Application: Range, Resolution, and Field of ViewSimplify radar sensor application based product selection. Compare range, resolution, and field of view to avoid blind spots and choose with confidence. Explore the guide.TSV Data Lab
 Oct 18, 2026Comparing Material Options for Procurement: Specs, Costs, and Supply RisksExplore procurement oriented technical content on material options, specs, costs, and supply risks. Compare alternatives to cut hidden expenses and make confident sourcing decisions.Dr. Marcus Vance
 Oct 17, 20265-Axis CNC Positioning Accuracy: How to Interpret ISO 230-2 Test ResultsAssess 5 axis CNC machining positioning accuracy with ISO 230-2. Learn to interpret repeatability, reversal error, and test conditions to compare suppliers and make confident acceptance decisions.Dr. Marcus Vance
 Oct 16, 2026Choosing a Rugged Edge AI Box Supplier: Thermal Tests and Lifecycle SupportChoose a rugged edge AI box supplier with proven thermal performance and reliable lifecycle support. Discover the tests and commitments to verify before you buy.TSV Data Lab
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)
 Oct 20, 2026How Do You Measure Industrial IoT Gateway Latency Under Load?Measure industrial IoT gateway latency under load with reliable timestamps, realistic traffic, and tail-latency analysis. Discover how to expose bottlenecks and choose the right gateway.TSV Data Lab
 Oct 19, 2026How Do You Verify That Precision Machined Parts Meet Tolerances?Master precision machining tolerance verification with the right tools, datum setups, and acceptance rules. Learn how to validate parts confidently and reduce costly inspection errors.Dr. Marcus Vance
 Oct 18, 2026What Should an AS9100 Machining Supplier Checklist Include?Build an AS9100 machining supplier checklist that verifies capability, traceability, inspection, and outsourced processes. Discover what to check before approving your next aerospace supplier.Dr. Marcus Vance
 Oct 17, 2026How Should You Interpret Industrial Robot Repeatability Specs?Decode industrial robot repeatability specifications, understand ISO 9283 test conditions, and avoid costly selection mistakes. Learn how to verify performance for your process.Chen Wei (Automation Lead Engineer)
 Oct 16, 2026How Can You Fairly Compare MTBF Across Industrial Servo Motors?Make a fair industrial servo motor MTBF comparison with matched operating profiles, failure criteria, and confidence bounds. Discover how to assess reliability beyond advertised numbers.Chen Wei (Automation Lead Engineer)
 Oct 15, 2026How Should You Compare TechStat Vanguard 5-Axis CNC Tolerances?TechStat Vanguard 5-axis CNC tolerance comparison: learn how to verify part accuracy, assess inspection evidence, and choose suppliers that reliably meet your drawing requirements.Dr. Marcus Vance
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab























