
EDM for Plastic Injection Molds Where Surface Finish Changes Cycle Time
Publication Date
author
In EDM for plastic injection molds, surface finish is not just a quality metric—it directly shapes cycle time, tool wear, and downstream polishing demands. For engineers, buyers, and operations teams comparing precision processes such as industrial robots integration, custom machining for robotics joints, or precision grinding surface roughness control, understanding how EDM parameters influence molding efficiency is essential to making faster, data-backed manufacturing decisions.
Why does EDM surface finish change injection molding cycle time in real production?
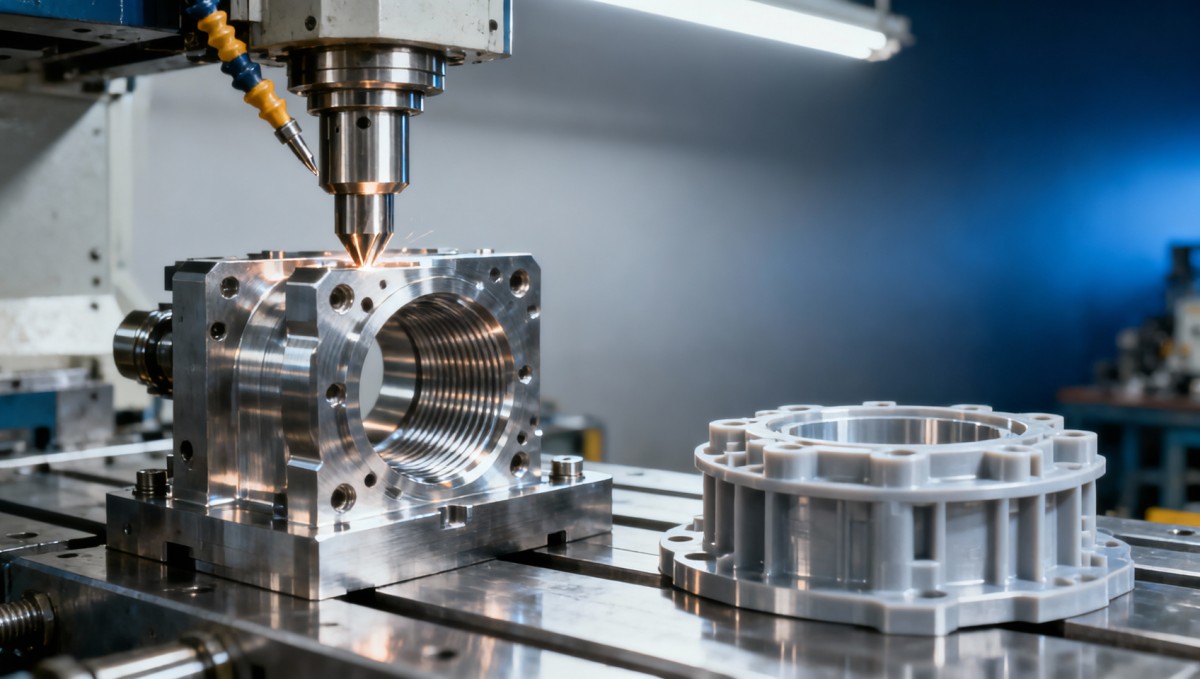
For plastic injection molds, EDM surface finish affects more than cavity appearance. It changes how molten polymer flows, how quickly trapped gas escapes, how easily the molded part releases, and how much secondary polishing is required before production approval. In many plants, the discussion starts with Ra value or spark grade, but the real business impact appears later in cycle time, reject rate, and mold maintenance intervals.
A rougher EDM texture can increase drag during ejection, especially on deep ribs, textured walls, and tight shutoff areas. When release force rises, processors often compensate by adding 0.5–2.0 seconds of cooling time, adjusting ejector sequencing, or reducing injection speed. That may look small in isolation, but over medium- to high-volume runs, even a 1-second increase can materially change machine utilization and part cost.
A finer surface finish may improve release and reduce polishing labor, yet it can also raise machining time in the toolroom if multiple skim passes are required. The practical question is not whether smoother is always better. The correct question is whether the chosen EDM finish aligns with resin type, geometry, venting design, cosmetic requirement, and target cycle window, typically evaluated during T0 to T2 mold trials.
This is where a data-driven evaluation matters. TechStat Vanguard (TSV) focuses on engineering truth rather than vague quality claims. For procurement teams and decision-makers, that means comparing process routes through measurable indicators: expected finishing passes, polishing burden, release behavior, cavity wear exposure, and the likely effect on a cycle target such as 18–25 seconds for a standard technical plastic housing.
- Surface finish influences polymer flow marks, gas evacuation, and ejection friction rather than acting as a purely visual specification.
- Cycle time changes often appear indirectly through longer cooling, slower opening speed, or added mold release interventions.
- Toolroom labor can shift from EDM machine time to bench polishing time depending on the selected finish strategy.
- The best decision usually comes from balancing 3 variables together: cavity finish, molding stability, and total cost per accepted part.
What operators and buyers usually miss
Operators often focus on machine settings after the mold enters production, while buyers may focus on upfront tooling cost. Both viewpoints are incomplete. If the EDM finish causes sticking, blush, or unstable demolding, the press team may spend several shifts adjusting hold pressure, cooling, and ejection timing without solving the root cause. What looked like a cheaper tool at RFQ stage can become the more expensive option in the first 3–6 months of production.
For technical procurement, the key is to request finish-related process information before purchase order release. That includes electrode strategy, number of finishing passes, intended polishing allowance, steel grade compatibility, and trial validation criteria. These are not abstract details. They directly affect launch timing, maintenance planning, and whether the mold can consistently hold dimensional and cosmetic targets under normal plant variation.
Which EDM parameters matter most when surface finish drives molding efficiency?
EDM for plastic injection molds is a controlled trade-off between removal rate, recast layer, electrode wear, and final surface texture. In roughing, higher discharge energy removes material faster but leaves a deeper crater structure. In finishing and skimming, lower energy settings reduce surface roughness and help minimize the damaged layer. For many mold shops, the commercial risk is using roughing efficiency logic on areas that later control venting, release, or optical appearance.
The most relevant parameters usually include pulse on-time, pulse off-time, peak current, electrode material, flushing conditions, and the number of finish passes. Shops may describe results through internal spark grades, but buyers should translate those descriptions into practical outputs: expected surface roughness range, benching requirement, and whether manual correction will be needed in narrow ribs, deep pockets, or shutoff details.
For mold applications with engineering plastics, thin-wall parts, or visually sensitive surfaces, a small difference in cavity condition can influence process stability. A finish suitable for hidden structural geometry may be unacceptable for a glossy exterior face or a lens-adjacent component. This is also why TSV emphasizes parameter-backed benchmarking: process names alone do not provide enough decision quality.
The table below summarizes how common EDM process choices can influence downstream molding behavior. These are practical manufacturing tendencies rather than universal guarantees, and they should always be validated against resin, steel, geometry, and texture requirements.
From a sourcing perspective, this table shows why EDM surface finish should be reviewed as part of process capability, not left as a cosmetic footnote. A quote that lacks detail on finish passes, polishing allowance, and cavity-specific strategy often transfers uncertainty downstream to mold trials, production engineering, and maintenance budgets.
Three parameter groups that deserve review
1. Energy settings and pass structure
Ask whether the mold area receives only rough plus one finish pass, or a staged route such as roughing, semi-finishing, and 2–4 skim passes. The difference affects both texture quality and polishing workload. On complex molds, a staged route can reduce handwork variability and improve repeatability across multiple cavities.
2. Electrode and compensation method
Graphite and copper each have advantages depending on geometry and target finish. What matters commercially is not only material choice but how wear is modeled and measured. If the supplier cannot explain compensation on corners, ribs, and deep pockets, the finish quality may vary across the tool.
3. Planned post-EDM finishing
A quoted EDM finish is rarely the whole story. Buyers should confirm whether stone polishing, paper polishing, diamond paste work, or texture preparation is part of scope. A surface that looks acceptable at delivery may still add 8–20 bench hours if cosmetic approval is strict.
How should engineers and procurement teams compare EDM, polishing, and alternative finishing routes?
Not every mold surface should be pushed to the same EDM finish level. The correct route depends on part function, visibility, resin sensitivity, and cost target. Some cavities benefit from fine EDM followed by light polishing. Others need aggressive polishing from a machined base condition. In textured molds, the optimal path may focus on texture consistency rather than mirror quality.
Cross-functional teams often compare machining cost without comparing production impact. That creates blind spots. A lower-cost EDM approach may increase manual polishing and delay sampling by 3–7 days. A premium finishing route may reduce launch friction but make sense only for Class A appearance parts or for tools running high annual volumes. Decision quality improves when the comparison includes total manufacturing effect, not just toolroom hours.
The following comparison helps separate these choices in practical terms for information researchers, mold users, and enterprise buyers evaluating injection mold finishing strategy.
A useful rule for buyers is to compare at least 4 dimensions together: cavity accessibility, annual part volume, appearance requirement, and target trial timeline. When these factors are separated, teams tend to overspecify finish on low-risk surfaces or underspecify finish in areas that control release and part consistency.
Decision logic for common B2B scenarios
For robotics housings, sensor brackets, connectors, and industrial covers, the surface finish strategy should support predictable throughput rather than decorative perfection. If the part has draft-sensitive geometry or glass-filled resin, prioritize release reliability and wear resistance. If the part is customer-facing and lightly textured, focus on finish uniformity and texture readiness rather than maximum smoothness everywhere.
For enterprise decision-makers managing launch deadlines, it is often better to define finish by functional zones. For example, specify one level for hidden structural faces, another for ejection-critical ribs, and a third for cosmetic or texture surfaces. This structured approach can reduce unnecessary tooling cost while improving first-trial readiness.
- Use zone-based finish planning for molds with mixed cosmetic and structural requirements.
- Review annual volume before paying for a premium finish across the full cavity.
- Link finish decisions to resin behavior, especially for filled polymers and tight draft conditions.
- Ask suppliers to separate EDM cost, polishing cost, and texture-prep cost in quotations.
What should a procurement checklist include before approving an EDM-based mold finish?
A strong procurement decision for EDM in plastic injection molds requires more than a drawing note. The RFQ package should define functional surfaces, expected finish route, validation method, and acceptance checkpoints. In practice, many disputes come from vague wording such as “fine EDM finish” or “polish as needed,” which leaves too much room for interpretation between tooling, quality, and production teams.
A disciplined review process usually has 4 stages: design clarification, supplier process confirmation, sample trial review, and production release. Each stage should include measurable checks. For example, before PO award, confirm which surfaces are EDM-only, EDM-plus-polish, or prepared for texturing. Before T1 sampling, confirm cavity release behavior, visible defects, and any areas still requiring bench correction.
The checklist below is especially relevant for procurement managers and CTO-level reviewers who need a compact but technical framework for supplier comparison.
Using a checklist like this helps prevent a common failure mode in hard-tech sourcing: evaluating vendors on headline price while leaving process risk undefined. TSV’s position is straightforward: parameters, tolerances, and verification logic create trust; generic claims do not.
A practical 5-point review before PO release
- Confirm whether critical surfaces are identified by function, not only by appearance.
- Ask for the intended EDM and polishing sequence, including how many finish passes are planned.
- Define whether sample approval depends on visual inspection, release force behavior, or both.
- Review expected lead time impact if polishing correction is needed after T1 or T2 trials.
- Separate upfront tooling cost from production cost effect across the first 6–12 months.
For most procurement teams, this review can be completed in one structured technical meeting if the supplier provides process transparency. If not, that lack of clarity is itself a sourcing signal.
Common misconceptions, implementation risks, and FAQ
Many mold programs underperform not because EDM is the wrong process, but because its finish implications are misunderstood. Rougher is not always cheaper once polishing labor and cycle penalties are counted. Finer is not always better if it delays tooling without adding release or cosmetic value. What matters is matching surface finish strategy to the production objective.
There are also implementation risks beyond the EDM machine itself. Deep cavities may suffer unstable flushing. Narrow ribs may hide overburn or shape drift. Excessive benching can alter geometry that EDM originally held well. In other words, finish quality is a system outcome involving design, machining, inspection, and molding trials over a typical 2–4 week refinement window after first sampling.
The FAQ below addresses the questions most often raised by researchers, users, procurement staff, and business leaders comparing EDM-based mold finishing decisions.
How do I know if EDM surface finish is causing longer cycle time?
Look for indirect symptoms rather than only visual clues. If the press team adds cooling time, uses more aggressive ejector settings, applies mold release, or sees sticking in specific ribs and pockets, the cavity finish may be part of the cause. Compare cycle performance before and after local polishing or insert correction. A recurring 1–2 second gain after finish adjustment is a strong practical indicator.
Which surfaces should receive the highest EDM finishing attention?
Prioritize surfaces that control ejection, sealing, visible appearance, or texture uniformity. Deep ribs, low-draft walls, shutoff-adjacent zones, and customer-facing areas usually deserve more attention than hidden structural pockets. This zone-based strategy is often more cost-effective than specifying the same finish standard across the entire mold.
What delivery questions should buyers ask a mold supplier?
Ask for the process route, expected lead time impact of finish level, polishing scope, and trial correction plan. In many tooling programs, a finish upgrade or unexpected benching step can change delivery by several days to over 1 week. It is better to clarify that at quotation stage than during launch escalation.
Are there standard certifications that guarantee the right EDM finish result?
No single certification can guarantee the correct mold surface finish outcome. Quality management frameworks such as ISO 9001 can support process control, and sector-specific systems like AS9100 or ISO 13485 may matter in adjacent precision industries, but the correct result still depends on process planning, measurement discipline, and mold trial validation. Buyers should rely on documented process capability and inspection logic rather than labels alone.
Why work with a data-driven technical partner when evaluating EDM for plastic injection molds?
When surface finish changes cycle time, a mold decision becomes a business decision. Engineering teams need clear process logic. Operators need stable release and less firefighting. Procurement needs comparable supplier data. Executives need confidence that tooling cost, timeline, and production economics are aligned. That is exactly the gap TSV is built to address.
TechStat Vanguard filters out inflated claims and focuses on verifiable manufacturing criteria: tolerance logic, process transparency, benchmark-style comparison, and supply chain traceability. For organizations sourcing molds, precision machining, robotics-related components, or advanced industrial hardware, that approach reduces information noise and shortens qualification cycles.
If you are reviewing EDM for plastic injection molds, you can contact TSV for support on parameter confirmation, process route comparison, supplier evaluation logic, expected delivery windows, polishing versus EDM trade-offs, sample validation criteria, and RFQ language that better reflects production reality. These discussions are especially valuable when tooling must support tight launch schedules, multi-cavity consistency, or technically demanding resin and geometry combinations.
Bring your drawing notes, finish requirements, target cycle time, and any open questions on mold trials or supplier quotes. A well-structured technical review at the front end can save weeks of iteration later and help your team make decisions based on engineering truth through data.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























