
CNC Milling for Engine Blocks What Really Drives Scrap Rates
Publication Date
author
In cnc milling for automotive engine blocks, scrap rates rarely come from one obvious flaw. They are driven by a chain of variables—tool wear, fixture stability, thermal distortion, material inconsistency, and cnc spindle runout measurement—that directly affect yield, cost, and delivery. For engineers, operators, buyers, and decision-makers, understanding these root causes is the first step toward tighter process control and more reliable machining outcomes.
Why do scrap rates rise so quickly in CNC milling for engine blocks?
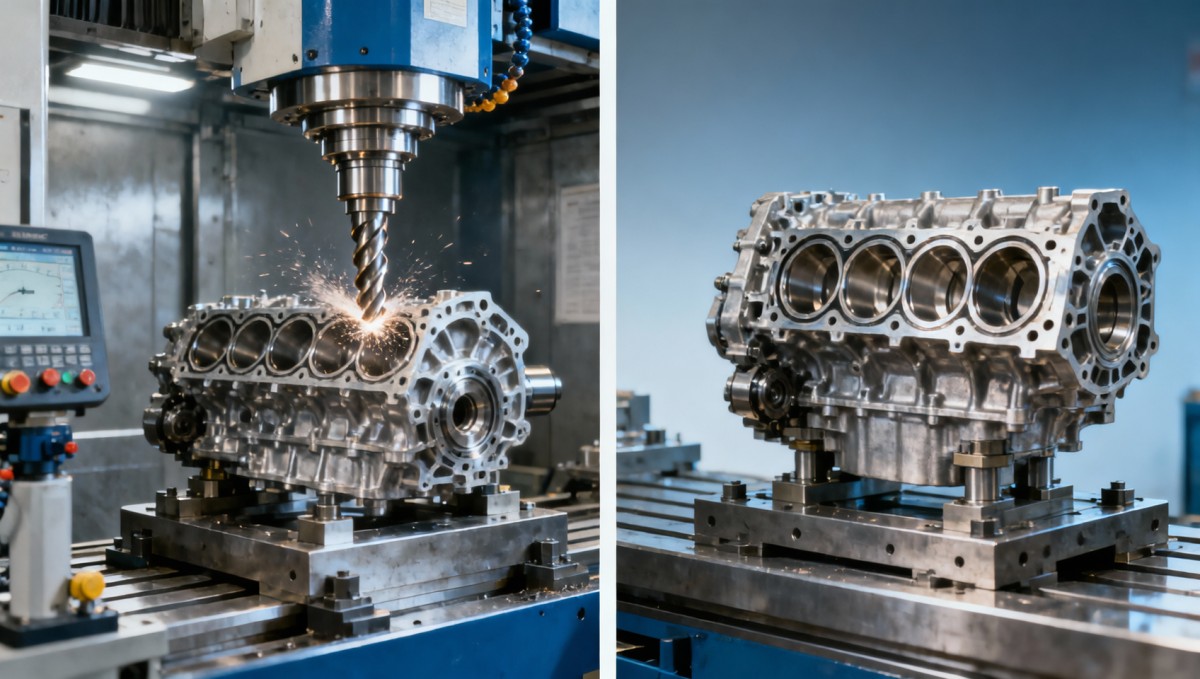
Engine block machining is a high-stakes process because multiple datums, cylinder bores, deck faces, oil galleries, and threaded features must remain aligned across several operations. In a typical production route, rough milling, semi-finishing, boring, drilling, and final finishing may be spread across 3–6 setups or transferred through a linked machining cell. A small shift in one stage can cascade into dimensional rejection at the end.
For operators, the practical issue is not only whether a part is in tolerance, but when the process starts drifting. A cutter that remains usable for 80–120 parts in one alloy may fail much earlier in another heat lot. A spindle that looks acceptable during idle inspection can create taper, chatter marks, or bore mismatch under thermal load after 2–4 hours of continuous running.
For procurement teams and plant managers, scrap rate is also a hidden sourcing metric. A supplier may quote an attractive unit price, but if process capability is unstable, the real cost appears later in replacement parts, delayed PPAP-style validation, emergency overtime, and line stoppage. That is why TechStat Vanguard focuses on measurable process signals rather than marketing language.
In engine block work, the most common scrap drivers usually fall into five groups: machine condition, tooling behavior, workholding integrity, material variation, and inspection discipline. None of these should be reviewed in isolation. A data-driven shop connects spindle condition, tool life trend, coolant control, fixture repeatability, and in-process measurement into one decision chain.
- Machine-side drift: spindle runout, axis backlash, thermal growth, and vibration under load.
- Tool-side instability: uneven wear, edge chipping, built-up edge, and incorrect replacement intervals.
- Fixture-side errors: clamping distortion, poor locating repeatability, and chip contamination at contact points.
- Material-side inconsistency: casting porosity, hardness variation, and residual stress release during machining.
- Inspection-side gaps: delayed feedback, insufficient bore trend monitoring, and weak first-off to last-off control.
What makes engine blocks harder than many other machined parts?
Unlike simpler housings or plates, engine blocks combine thin-wall sections, deep cavities, intersecting fluid passages, and tight positional relationships. A deck face may be flat within a narrow range, while bore geometry, center distance, and perpendicularity must also hold after heat, coolant exposure, and prolonged machining. That means the process window is often narrower than it first appears on the drawing.
Complexity also increases inspection burden. Some nonconformities are visible immediately, such as burrs or chatter. Others emerge only when CMM, air gauge, or bore gauge data is reviewed in sequence. If the feedback loop takes 30–60 minutes instead of near-real-time sampling, one unstable tool can create a batch problem before anyone intervenes.
Which technical variables usually drive scrap first?
When a machining team investigates rising rejection in cnc milling for automotive engine blocks, the first priority should be to separate symptom from cause. Poor surface finish, bore taper, or datum mismatch are symptoms. The true causes are typically traceable to a small set of measurable variables. The table below summarizes the process factors that most often push scrap upward in production environments.
The important point is interaction. A shop may blame tooling, but the actual trigger could be spindle condition or thermal drift that shortens tool life. This is why TSV emphasizes engineering benchmarking and traceability logic. If one parameter changes, the surrounding process data must be reviewed together, not as isolated snapshots.
Why spindle runout deserves early attention
CNC spindle runout measurement is often underestimated because it sounds like a maintenance detail rather than a scrap driver. In reality, even a modest increase in runout can unevenly load cutting edges, accelerate wear, and distort bore quality. In cylinder and deck-related work, this directly affects size, cylindricity, and finish consistency over a full shift.
A disciplined shop usually checks spindle condition at defined intervals: after tool crashes, after preventive maintenance, during machine qualification, and whenever bore drift appears without a clear tooling explanation. The exact threshold depends on machine design, holder quality, cutter type, and feature tolerance, so procurement teams should ask for the supplier’s inspection method and reaction plan rather than a vague statement of “machine accuracy.”
A practical 4-point monitoring sequence
- Verify spindle warm-up routine before first-off parts, especially after overnight shutdowns of 8–12 hours.
- Record runout and vibration trend after any crash, holder change issue, or repeated finish defect.
- Correlate spindle data with tool life history instead of reviewing either dataset alone.
- Tie corrective action to a documented response window, such as same shift, next maintenance slot, or immediate stop.
How should buyers and production teams evaluate suppliers before scrap becomes a cost issue?
A strong sourcing decision in precision machining is not based only on quoted price, machine count, or lead time. For engine block work, buyers should evaluate whether a supplier can maintain process stability over low-volume validation, mid-volume ramp-up, and sustained serial production. In many cases, the difference between a stable partner and a risky one becomes visible through controls rather than brochures.
For information researchers and decision-makers, the most useful question is simple: what evidence shows that scrap is controlled before shipment? The answer should include maintenance intervals, gauge strategy, first-off approval logic, reaction to drift, and lot traceability. TSV’s data-driven approach is built around these concrete procurement questions because they reduce supplier qualification uncertainty.
The table below can be used as a procurement checklist when comparing machining suppliers for automotive or adjacent hard-tech applications. It is intentionally practical and avoids vague claims. Each item should be tied to documents, sample reports, or live process evidence during supplier review.
For buyers, this checklist also helps compare low-cost and high-control suppliers on equal terms. A lower quoted piece price may not remain lower if the supplier needs rework loops, sorting labor, or repeated containment. In precision machining, stable process evidence often protects total landed cost better than the cheapest initial quotation.
Three decision signals procurement should not ignore
First, ask how the supplier handles process changes. If a cutter grade, fixture element, or coolant condition changes, the response should be documented within a controlled revision flow. Second, ask how fast nonconformity feedback reaches the machine. A delay of one shift is much riskier than a feedback loop measured in minutes. Third, ask whether the supplier can explain scrap trends with parameter logic rather than broad claims.
This is exactly where TSV provides value for technical procurement and senior leadership. We help teams read beyond adjectives and focus on tolerance discipline, benchmarking logic, and supply chain traceability. In an environment overloaded with promotional noise, measurable process transparency is the more reliable path to supplier confidence.
What process controls reduce engine block scrap in day-to-day production?
A lower scrap rate does not come from one heroic fix. It usually comes from several controls working together across setup, machining, inspection, and maintenance. For operators and production engineers, the goal is to shorten the gap between process drift and corrective action. In many facilities, improving that response window from several hours to one setup cycle can change yield more than changing cutting parameters alone.
A practical process-control strategy often begins with a structured first-off routine, a stable warm-up sequence, and clear replacement rules for critical tools. It then extends into in-process checks on bores, deck surfaces, and positional features. For engine blocks, especially where multiple features reference one another, controlling stack-up is just as important as controlling individual dimensions.
Teams should also treat coolant and chip evacuation as quality variables, not housekeeping details. In high-volume or medium-volume work, clogged evacuation around deep cavities or galleries can change cutting load and local temperature, which in turn affects finish and size. This is especially relevant in long-cycle operations that run continuously for 6–10 hours per shift.
The following checklist is useful when reviewing a line that shows repeat scrap, intermittent drift, or unstable yield after setup changes.
- Confirm a documented machine warm-up period before finishing operations, especially on temperature-sensitive features.
- Clean and verify fixture contact points every setup and at defined intervals such as every 20–50 parts in chip-heavy operations.
- Track tool life by feature family rather than using one universal replacement rule for every cutter.
- Review cnc spindle runout measurement whenever unexplained bore or surface anomalies repeat across different tools.
- Use trend charts for critical features so drift is visible before parts exceed tolerance limits.
- Link nonconforming parts to machine, program revision, operator, and material lot within the same shift.
Common misconceptions that keep scrap high
“If the machine passed calibration, the spindle cannot be the issue.”
Calibration confirms an important baseline, but it does not automatically cover every under-load condition. Thermal growth, holder condition, and recent crash history can still influence spindle behavior during actual cutting. That is why routine machine checks and process-linked spindle review should work together.
“Scrap is mostly a tooling cost problem.”
Tooling is visible, so it gets blamed first. Yet many repeated tool failures originate from unstable fixturing, excessive vibration, poor chip evacuation, or inconsistent casting condition. Replacing a cutter without addressing these upstream causes only resets the clock for the next reject batch.
“100% final inspection will solve the issue.”
Final inspection catches defects after value has already been added. It is necessary for critical features, but it does not prevent scrap generation. Better economics usually come from earlier controls: first-off validation, in-process sampling, trend monitoring, and fast reaction plans.
FAQ and next-step guidance for engineers, buyers, and decision-makers
Search intent around engine block machining usually combines technical diagnosis with supplier evaluation. The questions below address both sides. They are especially relevant for teams comparing new machining partners, auditing current production risk, or trying to reduce scrap without disrupting delivery commitments over the next 2–8 weeks.
How often should critical process variables be reviewed?
There is no universal interval, but stable production usually combines three layers: first-off verification at each setup, in-process checks every defined part count or time window, and scheduled maintenance review weekly or monthly depending on utilization. High-risk features such as cylinder bores or sealing surfaces usually justify tighter monitoring than secondary geometry.
What should buyers ask about cnc spindle runout measurement?
Ask when it is checked, how it is recorded, what events trigger re-check, and how the supplier links it to surface finish or bore quality issues. A useful answer includes method, frequency, and action threshold. A weak answer usually stays at the level of general machine precision claims and offers no reaction workflow.
How long does process stabilization usually take for a new engine block program?
The exact timeline depends on feature count, tooling maturity, casting consistency, and inspection readiness. In practice, teams often move through 3 stages: initial prove-out, controlled pilot production, and stable serial release. What matters most is not speed alone, but whether each stage closes open risks in fixturing, tool wear, thermal control, and measurement repeatability.
What is the best way to compare suppliers beyond price?
Use a scorecard that weighs machine control, process discipline, inspection response time, traceability, and change management. A quote is only one layer of cost. Scrap, rework, premium freight, and delayed qualification can easily outweigh a small unit-price difference when the part is complex and delivery windows are tight.
Why choose TSV for this type of evaluation?
TechStat Vanguard is built for teams that need engineering truth rather than promotional claims. We focus on parameters, tolerances, benchmarking logic, and supply chain traceability across advanced manufacturing sectors. If your team needs support in parameter confirmation, supplier comparison, machining risk review, delivery-window assessment, tolerance discussion, or technical quotation alignment, TSV can help frame the right questions before cost and scrap escalate.
Contact us when you need a practical review of machining capability, a clearer procurement checklist, guidance on process-control evidence, or support in aligning sample validation with production expectations. The most productive conversations usually begin with six concrete topics: feature tolerance range, material condition, target volume, inspection plan, delivery timeline, and corrective-action speed. In hard-tech manufacturing, better decisions start when data replaces noise.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























