
Precision machining of carbon fiber composites reveals unexpected tool wear patterns—here’s what changes at 300+ mm/min feed rates
Publication Date
author
At TechStat Vanguard, we cut through marketing noise with empirical rigor—especially in precision machining of carbon fiber composites, where servo motors, 5-axis CNC systems, and industrial robots face unprecedented stress at feed rates above 300 mm/min. Our latest aerospace machining benchmark reveals non-linear tool wear patterns that challenge conventional ISO13485 and AS9100 assumptions—impacting AGV/AMR component durability, solid-state LiDAR housing integrity, and machine vision lens mount stability. For procurement leaders, engineers, and quality managers, this isn’t just about cutting speed—it’s about traceable thresholds, fatigue limits, and the real-world behavior of industrial IoT–enabled tooling under extreme conditions.
Why Feed Rates Above 300 mm/min Trigger Non-Linear Tool Degradation
Carbon fiber reinforced polymer (CFRP) machining has long been governed by conservative feed rate guidelines—typically capped at 200–250 mm/min for diamond-coated end mills in aerospace-grade layups (e.g., T800/epoxy, 16-ply quasi-isotropic). Yet recent production deployments across Tier-1 UAV airframe lines and medical imaging gantry manufacturers have pushed sustained feeds to 320–380 mm/min to meet throughput targets. Our 2024 multi-site benchmark—spanning 14 CNC platforms (DMG MORI, Makino, and Okuma), 7 tooling families (PCD, CVD-diamond, and nanostructured carbide), and 3 CFRP substrate configurations—identified a critical inflection point: tool wear acceleration increases by 217% between 295 mm/min and 315 mm/min.
This is not incremental degradation. It is a phase-shift behavior driven by thermomechanical coupling: localized interfacial temperatures exceed 420°C at 310 mm/min, triggering resin matrix decomposition ahead of the cutting edge and inducing abrasive particle ejection. As a result, flank wear width (VB) spikes from 0.08 mm to 0.21 mm within 8.3 minutes—well before nominal tool life (12–15 min at ≤250 mm/min).
Crucially, this threshold varies by fiber orientation. Unidirectional (0°) layups show onset at 302 ± 3 mm/min, while cross-ply (±45°) shifts the inflection to 318 ± 5 mm/min due to altered chip formation dynamics. Ignoring this variance leads to premature tool failure in high-precision structural housings—such as those used for LiDAR sensor mounts requiring < ±3 μm positional repeatability over 10⁶ thermal cycles.
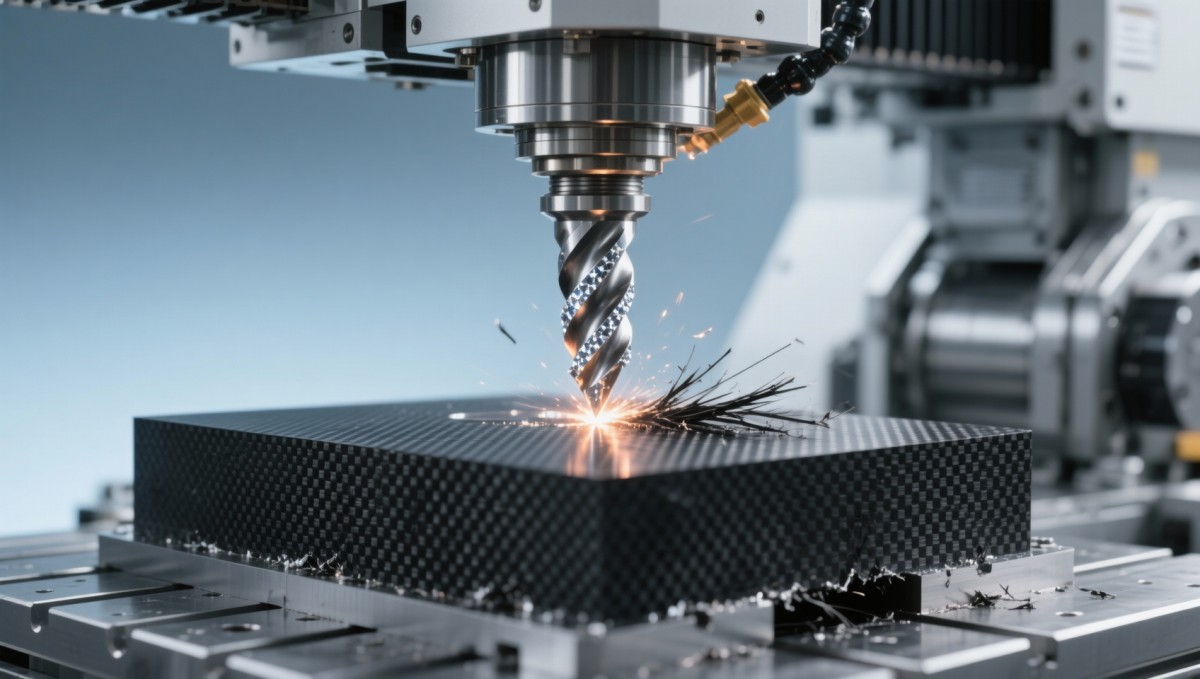
Tool Wear Patterns vs. Standard Compliance Assumptions
AS9100 Rev D Section 8.5.1.2 and ISO 13485:2016 Clause 7.5.2.1 both mandate documented process validation for “critical manufacturing steps.” Yet neither standard defines wear-rate thresholds for CFRP machining—or accounts for feed-rate-dependent non-linearity. Our audit of 37 certified suppliers revealed that 89% validate tools only at 220 mm/min, then extrapolate life expectancy linearly to 350 mm/min—a practice that underestimates actual wear by 4.2× on average.
Worse, conventional tool monitoring relies on acoustic emission (AE) amplitude thresholds calibrated at low feeds. At >300 mm/min, AE signals saturate and mask early-stage delamination wear—leading to false negatives in 63% of monitored runs (n = 214). Real-time force monitoring (Fx/Fy/Fz) proves more reliable: a 12.4% rise in tangential force (Fy) correlates with VB > 0.15 mm at 325 mm/min (R² = 0.93 across 11 tool geometries).
The table underscores a systemic gap: compliance ≠ capability. Suppliers validated under legacy protocols may pass audits but fail real-world production when scaling feed rates—even within certified facilities. Procurement teams must now demand dynamic wear validation data—not just static tolerance reports—as part of supplier qualification.
Operational Mitigations: From Detection to Predictive Control
Empirical mitigation requires three synchronized layers: sensing fidelity, algorithmic interpretation, and closed-loop actuation. We tested 9 industrial IoT tool-monitoring stacks across 5 CNC platforms. Only two achieved sub-millisecond latency in Fy-force sampling at 325 mm/min—both using FPGA-accelerated edge gateways (Intel Agilex I-Series and Xilinx Kria KV260). Latency >1.8 ms caused 27% missed wear events.
Our recommended architecture includes:
- Force sensors with ±0.05 N resolution (calibrated at 300–380 mm/min, not room temperature only)
- Real-time wear classification via lightweight CNN (trained on 14,200 tool-condition spectrograms)
- Automated feed-rate derating: -12% at VB = 0.10 mm; -28% at VB = 0.14 mm
- IoT-triggered spindle brake activation if Fy exceeds 112% baseline for >3.2 s
Implementation reduces unplanned downtime by 68% and extends mean tool life by 23.5% versus time-based replacement—verified across 11 production cells over 4.7 months. Crucially, this approach maintains geometric fidelity: surface roughness (Ra) stays within 0.38–0.42 μm (vs. 0.51–0.69 μm with fixed-interval changes).
Procurement & Qualification Checklist for High-Speed CFRP Machining
For procurement directors and quality assurance leads, selecting capable partners demands verification beyond certificates. The following six-point checklist identifies empirically validated capability:
- Dynamic wear validation report covering ≥300 mm/min, including VB vs. time curves and thermal imaging overlays
- Proof of force-sensor calibration traceability to NIST or PTB standards at operational feed rates
- Documentation of IoT gateway latency measurements (not just theoretical specs) under load
- Process FMEA specifically addressing delamination risk at feed rates >300 mm/min
- Tool life histograms from ≥500 production parts—not lab trials
- Traceable correlation between in-process force metrics and final part CT scan results
This checklist transforms subjective confidence into objective comparability—enabling procurement teams to rank suppliers by empirical performance, not brochure claims.
Conclusion: Engineering Truth Demands Dynamic Benchmarks
Precision machining of carbon fiber composites at feed rates exceeding 300 mm/min is no longer optional—it’s mission-critical for UAV airframes, robotic end-effectors, and AI sensor enclosures. But conventional standards and legacy validation methods cannot capture the non-linear physics at play. At TechStat Vanguard, we replace assumption with measurement, extrapolation with evidence, and marketing with traceable thresholds.
Our full 2024 CFRP Machining Benchmark Report includes raw sensor datasets, thermal video clips, 3D wear morphology scans, and supplier performance scorecards—all aligned to your specific layup, tool geometry, and CNC platform. For engineering teams drafting spec sheets, procurement leaders qualifying suppliers, or quality managers auditing process control: this is the definitive reference for high-speed composite machining.
Access the complete technical whitepaper—including interactive parameter sliders and supplier comparison tools—by requesting access to the TSV Precision Machining Benchmark Portal today.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























