
Vision based quality inspection software needs better false reject control
Publication Date
author
For manufacturers relying on vision based quality inspection software, false rejects are more than a nuisance—they drain throughput, inflate labor costs, and distort quality data. As production teams push for tighter tolerances and faster cycle times, better false reject control becomes essential for operators, buyers, and decision-makers seeking reliable automation performance without sacrificing inspection accuracy.
Why false reject control has become a board-level issue in vision inspection
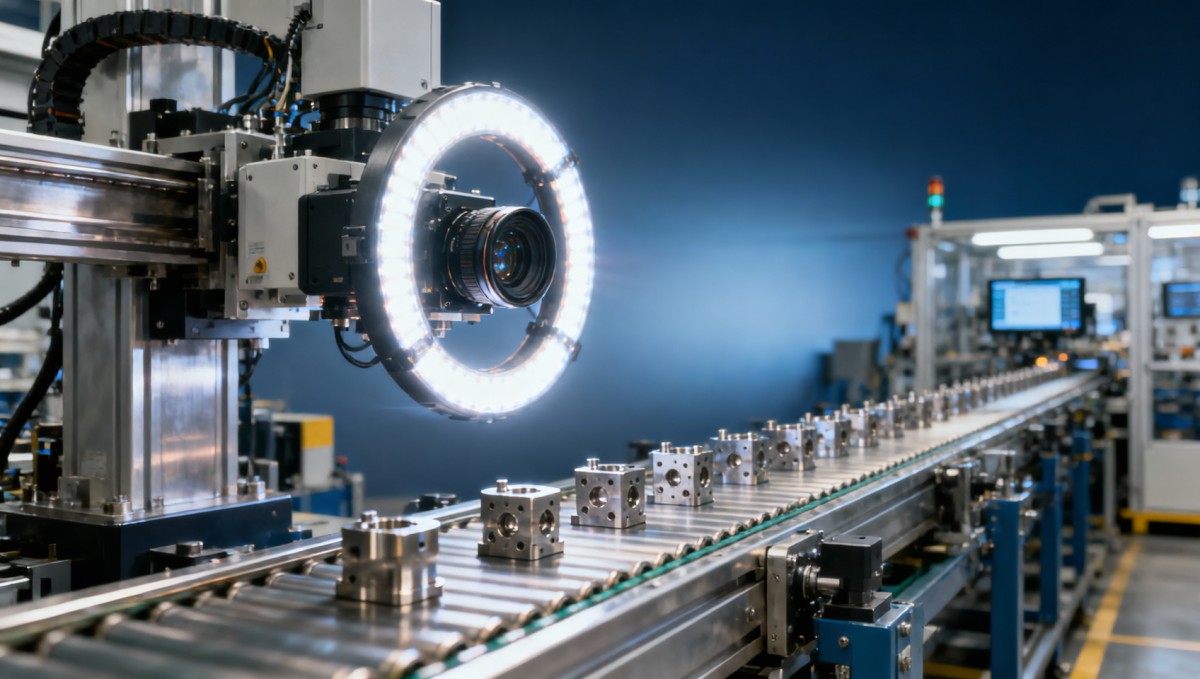
In machine vision inspection, a false reject happens when the software flags a conforming part as defective. On a busy line, that single classification error is rarely isolated. It can trigger manual rechecks, line slowdowns, unnecessary scrap segregation, and avoidable operator intervention. In mixed manufacturing environments, where batches shift every 2–4 hours and tolerances can vary by application, false reject control directly affects cost, capacity, and trust in automation.
For operators, the pain is practical: too many rejects create alarm fatigue and extra handling. For procurement teams, the issue is financial: the quoted software price is only a fraction of the lifecycle cost if the system forces constant human review. For enterprise decision-makers, the concern is strategic: distorted reject data can mislead supplier evaluation, process capability reviews, and capital planning.
This is why vision based quality inspection software must be judged on more than detection sensitivity. A system that captures every theoretical defect but rejects too many good parts can underperform in real production. In TSV’s data-first view, parameters matter more than broad claims. Teams should ask how the software behaves under lighting variation, fixture drift, lens contamination, part presentation changes, and normal process noise over 8-hour, 16-hour, or 24-hour operating windows.
Across robotics, sensors, edge AI, and precision machining workflows, the real question is not whether inspection is automated, but whether the software can preserve decision quality under production pressure. Better false reject control means more stable throughput, cleaner quality data, shorter review loops, and fewer arguments between quality engineering, operations, and purchasing.
What usually drives false rejects in real factories?
- Natural variation in acceptable parts, especially where surface texture, color shade, reflectivity, or edge burr profile changes slightly between lots.
- Inconsistent illumination, including glare, shadowing, flicker, or gradual intensity drift during a shift or across seasonal temperature changes.
- Part positioning errors from conveyors, feeders, robots, or fixtures, often within small but consequential ranges such as sub-millimeter offsets or angle deviations.
- Over-tuned inspection thresholds that perform well in pilot validation but become unstable after 3–6 weeks of full production variation.
Which technical factors matter most when evaluating vision based quality inspection software?
The best evaluation framework separates image quality, decision logic, and deployment stability. Many teams spend too much time discussing camera resolution and too little time examining threshold governance, recipe management, and response to process drift. Better false reject control usually comes from system design discipline, not one isolated hardware upgrade.
A practical buying review should examine at least 5 core dimensions: image acquisition stability, inspection repeatability, recipe changeover control, operator override workflow, and traceable reject analytics. If one of these is weak, false reject rates often rise as production complexity grows. This is especially true in plants that inspect multiple SKUs, run small- to mid-size lots, or use several part finishes on the same line.
TSV’s engineering-oriented approach is useful here because it cuts through generic software claims. Instead of asking whether a platform is “smart,” manufacturers should ask whether it can maintain stable pass/fail decisions under typical plant conditions: dust, vibration, variable ambient light, tool wear, and recipe switching 3–10 times per day.
The table below summarizes the technical checkpoints that most strongly influence false reject control during software selection and line validation.
Notice that none of these checkpoints is purely theoretical. Each one can be tested during factory acceptance or pilot runs over 3 stages: baseline setup, controlled variation, and live-production observation. That sequence helps buyers see whether a vendor’s false reject claims hold up outside demo conditions.
Key technical signals buyers should request
1. Repeatability under controlled variation
Ask for demonstration data showing the same conforming sample set inspected multiple times under slight changes in position, brightness, or orientation. Even a modest test plan of 30–50 parts across 3 conditions can reveal whether the software is stable or over-sensitive.
2. Reject reason transparency
A usable platform should show why a part failed, not just that it failed. Edge mismatch, contrast anomaly, missing feature, dimensional deviation, and contamination should be visible as separate logic paths wherever possible.
3. Change management control
If recipes can be edited without permission levels or revision history, false rejects often become a governance issue rather than an algorithm issue. Plants with 2–3 shifts especially need traceable parameter control.
How do application scenarios change the right false reject strategy?
Not every production environment needs the same inspection logic. A high-speed packaging line, a CNC machining cell, a UAV component assembly station, and an electronics sensor line all present different visual challenges. The correct false reject control strategy depends on surface behavior, defect criticality, cycle time, and the cost of secondary review.
For example, cosmetic inspection on reflective metal often suffers from lighting-induced variability, while dimensional feature checks may be more sensitive to positioning repeatability. In edge AI and sensor assembly, sub-feature contrast and micro-scale component placement can require more disciplined calibration intervals, often every shift or every lot depending on process stability.
This is why buyers should avoid one-size-fits-all vendor promises. A software package that works well for barcode verification may not control false rejects effectively for machined edge inspection, adhesive bead checks, carbon fiber surface review, or fastener presence validation. The inspection model must fit the process physics.
The next table maps typical industrial scenarios to false reject risks and practical control methods. It is intended for information researchers, plant users, and procurement teams comparing deployment fit rather than just software feature lists.
A key lesson from these scenarios is that false reject control improves when inspection logic is linked to process capability. If the upstream process naturally varies within an acceptable band, the software must be validated against that real band—not against a perfect sample captured once during setup.
Scenario-specific implementation checklist
- Define defect criticality in 3 levels: cosmetic, functional, and safety-related. This prevents low-risk visual deviations from being treated like mission-critical faults.
- Validate with samples from at least 2–3 production lots rather than a single golden batch, especially when raw material finish or supplier source can vary.
- Set review rules for borderline cases so that operators do not create inconsistent pass/fail decisions across shifts.
- Recheck performance after fixture maintenance, camera cleaning, lens replacement, or lighting changes, because small hardware changes can alter false reject behavior.
What should procurement and decision-makers compare before buying?
When sourcing vision based quality inspection software, many buying teams compare license cost, camera count, and integration scope first. Those factors matter, but they do not reveal whether the software will produce usable results on day 60 of production. A stronger procurement model compares technical fit, operational burden, and quality data reliability together.
The most effective evaluation process usually takes 4 steps: requirement definition, sample-based proof test, pilot deployment, and acceptance review. Depending on line complexity, this can span 2–6 weeks. Shorter cycles may be realistic for simple presence checks; complex cosmetic or multi-feature inspection often needs more iteration to control false rejects without increasing false accepts.
Procurement teams should also separate vendor capability from project assumptions. If a quotation does not specify calibration responsibility, recipe tuning scope, operator training hours, or post-launch support windows, the line may absorb hidden costs later. Those hidden costs typically appear as engineering overtime, manual sorting, and delayed ramp-up.
The table below can be used as a practical procurement guide for comparing suppliers or internal solution options with a stronger focus on false reject control.
If your organization buys across multiple sites, standardizing these checkpoints can shorten supplier qualification cycles. It also aligns with TSV’s philosophy that engineering truth comes from measurable criteria, not broad sales language. A good decision document should compare not only what the software can detect, but how consistently it performs within the tolerance reality of your line.
Common procurement mistakes
Choosing maximum sensitivity by default
Extreme sensitivity may look attractive during demos, but in production it can increase false rejects if the acceptance window is not tied to process capability and defect severity.
Ignoring support after commissioning
Inspection conditions evolve. Materials change, tools wear, and fixtures drift. Without a defined review cycle every month or quarter, false reject control can degrade quietly.
Underestimating data governance
If image data, reject categories, and recipe revisions are not tracked clearly, teams struggle to distinguish software instability from upstream process change.
How can plants reduce false rejects after deployment?
Post-launch control is where many projects succeed or fail. Even a well-selected vision based quality inspection software platform needs disciplined implementation. Plants should build a routine around baseline confirmation, drift checks, review of reject images, and controlled threshold updates. In most facilities, the first 30–90 days are the most important period for stabilizing false reject behavior.
A strong implementation plan usually includes 6 practical elements: sample library creation, lighting verification, operator instruction, recipe lock rules, periodic performance review, and escalation logic for abnormal reject spikes. These actions do not require exaggerated budgets. They require ownership and measurable review points.
In regulated or quality-critical sectors, this discipline also supports better compliance readiness. While exact certification requirements vary by product and industry, documented inspection settings, version control, and traceable quality evidence are widely useful for audits, supplier reviews, and corrective action workflows.
Most importantly, plants should avoid reacting to every reject spike with immediate threshold relaxation. That can mask real defects. Better false reject control means separating three root causes: actual process change, imaging environment instability, and software parameter misalignment. When teams diagnose in that order, decision quality improves.
A practical 4-step control process
- Establish a baseline using approved samples from current production and verify inspection behavior at startup, mid-shift, and end of shift.
- Review rejected images daily during the early ramp-up phase, then weekly once the process stabilizes.
- Control parameter edits through named approval, revision logging, and rollback rules, especially when multiple engineers support the same line.
- Revalidate after changes in material source, fixture, lens, lighting angle, conveyor speed, or upstream process settings.
FAQ on false reject control in machine vision
How low should the false reject rate be?
There is no universal target because acceptable performance depends on defect criticality, manual review cost, and part volume. A realistic benchmark is whether the system maintains stable decision quality across normal variation, rather than only under ideal test conditions. Buyers should define acceptable ranges before pilot approval.
Can AI alone solve false rejects?
Not by itself. AI can improve classification in complex patterns, but poor lighting, unstable fixtures, limited training data, or uncontrolled recipe changes can still produce unnecessary rejects. Good engineering around optics, process variation, and governance remains essential.
What is the usual validation period before full rollout?
For many industrial applications, a structured proof process spans 2–6 weeks, including sample testing, line trial, and acceptance review. High-mix or cosmetic inspection projects may need longer because more variation must be captured.
Which teams should be involved in the purchase decision?
At minimum, involve quality engineering, production operations, maintenance or automation support, and procurement. For strategic lines, enterprise decision-makers should also review data traceability, support model, and scalability across sites.
Why work with a data-driven evaluation partner?
When false reject control is treated as a technical benchmark rather than a marketing phrase, purchasing becomes more rational and implementation risk falls. That is the value of TSV’s approach. We focus on measurable inspection behavior, parameter clarity, and engineering reality across robotics, sensors, edge AI, aerospace-related systems, and precision manufacturing environments.
For information researchers, we help convert vague vendor language into comparable technical checkpoints. For users and operators, we clarify what settings, workflows, and review logic affect day-to-day inspection stability. For procurement teams, we support supplier comparison through practical evaluation dimensions. For enterprise leaders, we connect inspection performance to throughput, qualification cycles, and long-term automation trust.
If you are assessing vision based quality inspection software and need better false reject control, contact us to discuss parameter confirmation, sample evaluation scope, inspection scenario fit, delivery planning, compliance expectations, and vendor comparison criteria. These are the discussions that reduce trial-and-error cost and improve decision quality before capital is committed.
You can also consult TSV for support on spec-sheet drafting, tolerance interpretation, pilot validation structure, image review workflow design, and cross-supplier benchmarking. In hard-tech procurement, clearer parameters lead to stronger outcomes. Engineering truth starts with asking the right technical questions.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























