Industrial Vision Systems OEM Guide: Camera, Lighting, and Integration Factors
Publication Date
author
Industrial vision adoption is accelerating across electronics, automotive, food processing, aerospace, packaging, and warehouse automation. Yet selecting an industrial vision systems OEM is rarely a catalog exercise. Camera architecture, lighting stability, software compatibility, and integration discipline all shape whether an inspection cell delivers measurable yield gains or creates a long debugging cycle.
That is why the current market deserves closer scrutiny. In a supply chain crowded with broad claims, the useful signal comes from verified parameters: sensor performance under real line speed, lighting repeatability over time, and evidence that the system can connect cleanly with PLCs, robots, MES, and edge computing infrastructure.
Why OEM Selection Has Become a Strategic Issue
An industrial vision systems OEM is more than a hardware vendor. The OEM defines the imaging stack, integration logic, service model, and future upgrade path. In practice, that means one supplier decision can affect inspection accuracy, commissioning speed, maintenance cost, and production flexibility for years.
This matters even more in sectors where tolerance bands are narrow and documentation standards are strict. TSV has consistently argued that engineering truth depends on measurable evidence, not generic quality language. The same standard applies when assessing an industrial vision systems OEM for defect detection, dimensional measurement, code reading, guidance, or traceability.
A strong OEM partner usually shows three things early. It can explain the inspection physics clearly, provide application-specific benchmarks, and discuss failure modes without hiding behind marketing terminology.
What an Industrial Vision Systems OEM Actually Delivers
The term covers a broader scope than cameras alone. A complete offer may include image sensors, lenses, lighting modules, controllers, embedded AI tools, industrial PCs, software libraries, operator interfaces, and integration services.
In many projects, the real risk sits between those components. A camera may be technically impressive, but if the lighting cannot hold contrast across ambient variation, the system misses defects. A good algorithm may still fail if trigger timing drifts against conveyor motion.
For business evaluation, it helps to frame the OEM role around four layers:
- Imaging performance: sensor, optics, frame rate, dynamic range, and image stability.
- Application engineering: fixture design, illumination method, triggering, calibration, and acceptance criteria.
- System integration: communication protocols, software interfaces, edge deployment, and factory connectivity.
- Lifecycle support: spare parts policy, firmware management, validation records, and field service capability.
Camera Choices That Influence Real Inspection Results
Camera selection is often oversimplified into megapixels. That is useful, but incomplete. Resolution only matters in relation to defect size, field of view, working distance, line speed, and the minimum pixels required per feature.
Sensor format and pixel strategy
Smaller pixels can raise nominal resolution, but they may reduce sensitivity in challenging light. Larger pixels can improve signal quality, especially in fast inspections or low-reflectance materials. The right tradeoff depends on application physics, not brochure rankings.
Global shutter versus rolling shutter
Motion-heavy production lines typically favor global shutter cameras. They reduce distortion when parts move quickly or when robotic pick-and-place timing is tight. Rolling shutter may still work in static or slower stations, but it needs careful validation.
Monochrome, color, line scan, and 3D
Monochrome cameras often outperform color models for contrast-driven defect inspection. Color becomes important when classification depends on print consistency, label verification, or material sorting. Line scan suits continuous webs and large surfaces. 3D imaging becomes valuable when height, volume, or profile deviation matters more than texture alone.
Lighting Is Usually the Real Differentiator
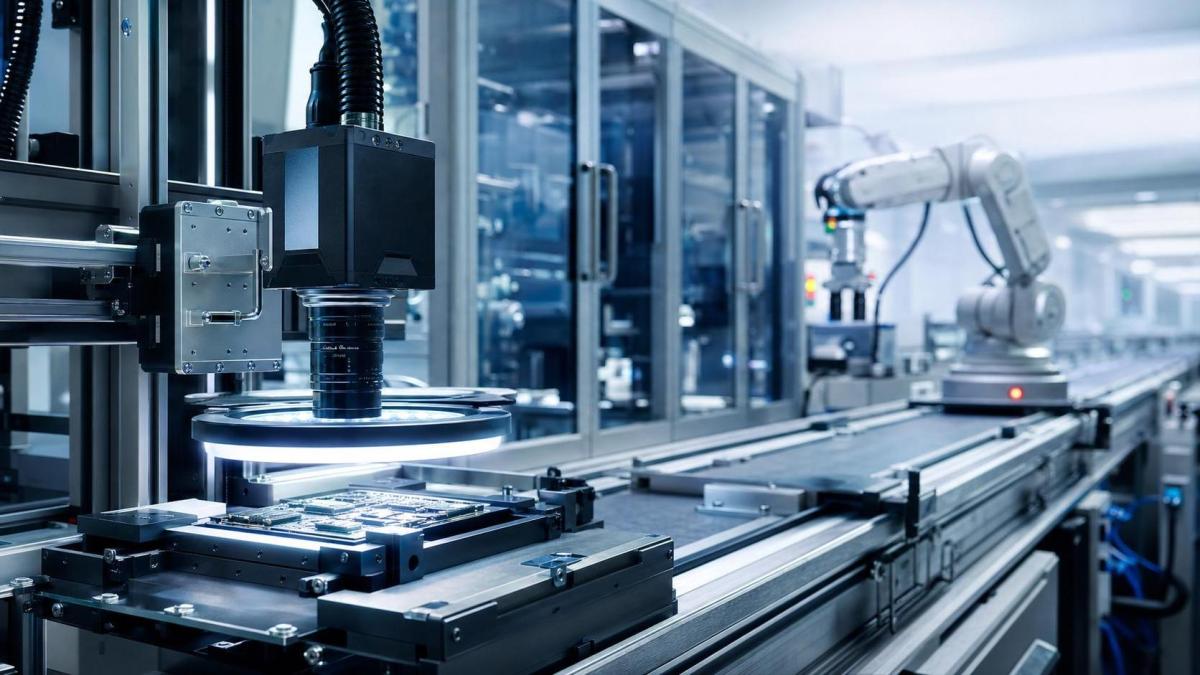
Many failed inspections are lighting failures disguised as software problems. The best industrial vision systems OEM teams treat illumination as a controlled engineering variable, not an accessory.
Part geometry, surface reflectivity, finish variation, and ambient light all influence image quality. Backlighting can isolate outer dimensions. Dark field lighting can reveal scratches and embossed defects. Dome lighting can reduce glare on curved or glossy surfaces. Structured lighting may support 3D reconstruction.
The stronger question is not which light type sounds advanced. It is whether the OEM can show repeatable contrast levels across production shifts, thermal drift, lens contamination, and part-to-part variation.
What to ask about illumination design
- Intensity stability over operating temperature and service life.
- Strobe synchronization with exposure and motion.
- Tolerance to dust, washdown, vibration, and enclosure constraints.
- Field adjustability without breaking validation records.
Integration Factors That Decide Deployment Speed
A capable industrial vision systems OEM should be judged on integration discipline as much as image quality. Many projects slow down because the vision cell works in isolation but not in the production environment.
Typical interfaces include Ethernet/IP, PROFINET, Modbus TCP, OPC UA, robot controller APIs, and MES or SCADA connections. If the OEM cannot define data flow, trigger logic, reject handling, and alarm escalation early, the commissioning schedule becomes fragile.
This is where TSV’s broader view of sensors and edge AI becomes useful. Vision systems are no longer standalone checkpoints. They are part of a digital manufacturing stack, feeding quality records, traceability events, process optimization, and in some cases machine learning refinement at the edge.
Integration areas worth checking
- Latency from trigger to result output.
- Version control for recipes, firmware, and models.
- Cybersecurity practice for networked devices.
- Support for audit trails and image retention.
- Recovery behavior after power loss or network interruption.
Typical Use Cases Across Industries
The value of an industrial vision systems OEM changes with the production context. Discrete manufacturing often focuses on presence-absence checks, dimensional verification, and robot guidance. Process industries may emphasize packaging integrity, code reading, fill level, and label compliance.
In aerospace and precision machining, traceable metrology and defect documentation may outweigh raw speed. In electronics, tiny solder defects and reflective surfaces push camera and lighting design harder. In logistics, barcode and parcel identification require robust performance under mixed orientation and variable handling speed.
That variation is why a credible industrial vision systems OEM should provide evidence from comparable materials, defect classes, and throughput conditions. Cross-industry experience helps, but application similarity matters more than a long customer logo list.
How to Compare Suppliers Without Getting Lost in Claims
A practical evaluation framework keeps the discussion grounded. Rather than asking which supplier is best in general, define what must be measured, how often it fails today, and what level of false reject or missed defect is acceptable.
Then review each industrial vision systems OEM against the same evidence set:
- Application feasibility data using representative samples.
- GRR, repeatability, and calibration approach where measurement is involved.
- Acceptance test criteria for FAT and SAT.
- Spare parts lead time and obsolescence management.
- Named responsibility for software, controls, and mechanical interfaces.
This approach aligns with TSV’s data-first view of industrial procurement. The aim is not to eliminate uncertainty completely. It is to reduce avoidable uncertainty by replacing broad promises with verified engineering detail.
A Better Next Step for Evaluation
The most useful next move is usually a structured requirement sheet. Define target defects, part variation, cycle time, environmental limits, data retention needs, and interface standards before comparing proposals. That will reveal which industrial vision systems OEM can think through the full inspection problem.
From there, request sample imaging results, integration architecture, and a clear validation plan. Camera specifications matter. Lighting design matters just as much. Integration maturity often decides whether the system creates value quickly or remains an expensive experiment.
For any shortlist, keep the standard simple: measurable parameters, comparable evidence, and a deployment path that fits the production reality. That is usually where a dependable industrial vision systems OEM becomes visible.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 11, 2026How payload and reach change the cost of an industrial robotCost of industrial robot systems depends heavily on payload and reach. Learn how sizing, torque, tooling, safety, and lifecycle factors shape smarter automation investments.Chen Wei (Automation Lead Engineer)
 Oct 10, 2026When does the cost of industrial robots pay back in high-volume production?Cost of industrial robots: discover how high-volume manufacturers calculate payback through uptime, cycle time, labor, quality, and integration before investing.Chen Wei (Automation Lead Engineer)
 Oct 09, 2026What does a manufacturing robot really cost beyond the purchase price?Manufacturing robot cost goes far beyond the purchase price. Explore integration, tooling, safety, uptime, and total ownership factors for smarter automation investments.Chen Wei (Automation Lead Engineer)
 Oct 08, 2026AGV vs. AMR: Which Is Better for Frequently Changing Routes?Which is better for changing routes? Compare AGVs and AMRs for flexible navigation, docking precision, traffic control, and faster facility reconfiguration.Chen Wei (Automation Lead Engineer)