How to Verify RoHS Compliance in Industrial Sensing Systems Before Deployment
Publication Date
author
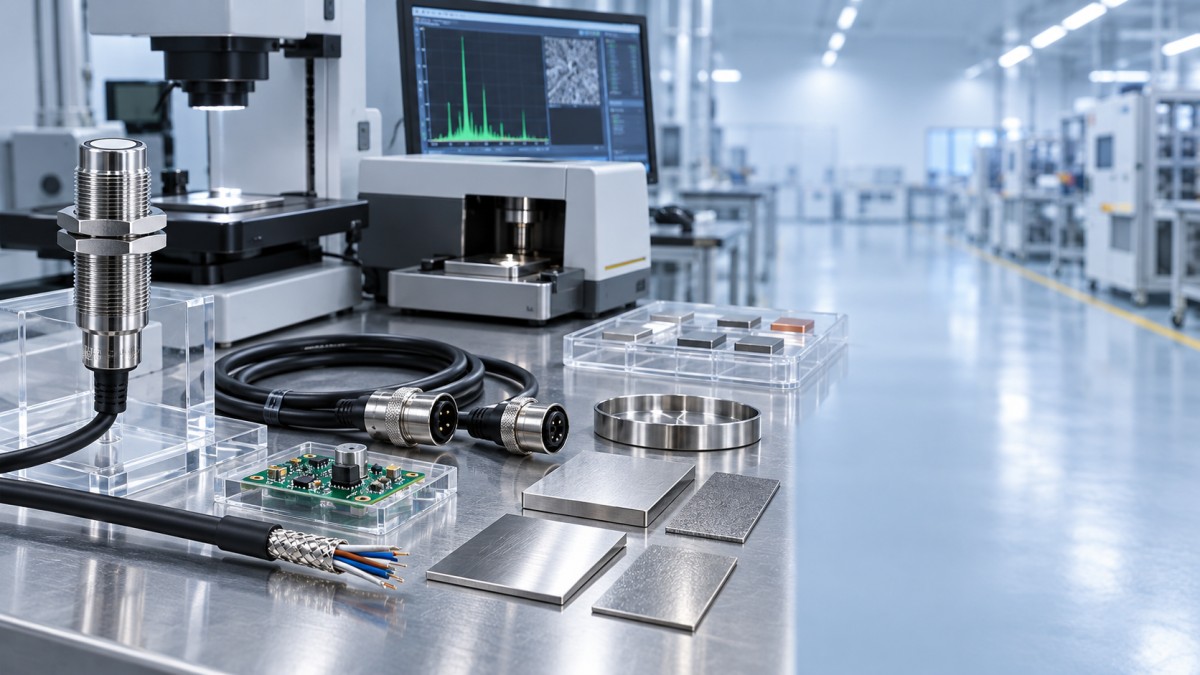
RoHS verification for an industrial sensor should begin with the exact item that will be deployed, not with a generic statement on a product family page. A sensor assembly can contain a sensing element, printed circuit board, connector, cable, potting compound, housing, mounting hardware, labels, and packaging. A declaration that covers only the main sensor body leaves uncertainty around accessories and configuration-specific parts.
Before release, establish a controlled bill of materials for the deployed configuration: part number, revision, connector option, cable length, enclosure material, mounting kit, firmware-related hardware variant, and country or market of placement. This baseline is the reference against which every RoHS document and material record should be reviewed. Without it, evidence can be technically genuine yet attached to a different construction than the item entering the installation.
Start with the applicable substance restrictions and scope
RoHS compliance concerns restricted substances in homogeneous materials, rather than the total mass of an assembled sensor. A homogeneous material is a material that cannot be mechanically separated into different materials. The nickel plating on a connector contact, solder on a PCB joint, PVC or elastomer insulation on a cable, and pigment in a molded polymer may each need separate consideration.
The familiar restricted-substance groups include lead, mercury, cadmium, hexavalent chromium, certain brominated flame retardants, and specified phthalates. The relevant concentration limits apply at the homogeneous-material level under the applicable RoHS framework. A heavy stainless-steel housing does not dilute the concentration of a restricted substance present in a small solder joint or cable jacket. This is why a system-level statement based solely on total product mass is inadequate.
Scope must be confirmed before evidence is judged. The intended product category, destination market, electrical operating characteristics, whether the equipment is supplied as a complete assembly or a replaceable part, and any applicable exclusions affect the evaluation. Do not assume that a component described as “industrial” sits outside the relevant requirements. Likewise, do not treat an exemption as a permanent property of a material. An exemption must be applicable to the exact use, be documented with its legal basis, and remain valid at the point of placing the equipment on the market.
Read a declaration as evidence, not as a label
A supplier declaration of conformity can be useful, but its evidentiary value depends on precision. A robust document identifies the legal framework or restricted-substance requirements being addressed, the legal entity making the declaration, the product or part number, revision or date, and a responsible signatory. Vague statements such as “environmentally friendly,” “RoHS ready,” or “meets green requirements” do not establish compliance.
Match every identifier in the declaration to the controlled configuration. A family-level part number can conceal differences that matter: an M12 connector may use a different plating stack than a cable-gland version; a high-temperature cable may use a different insulation formulation than a standard lead; a conformally coated PCB may introduce a material absent from an uncoated version. When a document covers a series, obtain a mapping that explicitly includes the ordered suffix and revision.
Document dates also deserve attention. A current declaration does not automatically establish the status of older warehouse stock, while an old declaration may predate a redesign or supplier change. Record the manufacturing lot or date code where practical, particularly when sensors are delivered over an extended program or held as service spares. Compliance evidence needs a traceable relationship to the physical units installed.
Decompose the sensor assembly where noncompliance is most likely to hide
Industrial sensing systems often fail verification at interfaces rather than at the sensing element. The following areas deserve targeted evidence because material choices change frequently and are not obvious from an external inspection.
- PCB assemblies: Review solder alloy, component terminations, surface finish, relays, ceramic parts, fuses, batteries, displays, and any legacy modules. A lead-free board finish does not prove that every termination or soldered subassembly satisfies the applicable limits.
- Connectors and cable harnesses: Ask for records covering contact plating, brass or copper-alloy bodies, overmolding, wire insulation, shielding, strain relief, seals, and ink markings. Connector compliance documentation that excludes the attached cable is common and insufficient for an integrated sensor lead.
- Polymeric materials: Cable jackets, molded housings, gaskets, encapsulants, adhesives, heat-shrink tubing, labels, and conformal coatings can contain flame retardants, plasticizers, pigments, or curing additives. Material grade names alone are not proof because the same base polymer can be compounded differently.
- Metal finishes and mechanical hardware: Fasteners, brackets, threaded inserts, plated housings, terminal blocks, and shield cans require attention when plating, passivation, or alloy composition is outside the primary electronics supply chain.
For each item with elevated uncertainty, request a full material declaration, homogeneous-material breakdown, or a controlled supplier material statement. A declaration should distinguish deliberate use from analytical presence where that distinction matters, identify the material or component to which it applies, and state the basis of the claim. A material database export is valuable only when its part numbers, revisions, and material classifications are unambiguous.
Trace evidence through the supply chain
RoHS compliant sensing systems depend on evidence flowing through several tiers. The sensor assembler may rely on a PCB fabricator, cable assembler, connector producer, molding compound supplier, plating house, and distributors of passive or semiconductor devices. A certificate from the final assembler is stronger when it is supported by a documented process for collecting, reviewing, and updating lower-tier declarations.
Traceability should be proportional to the risk and the ability to substitute parts. Commodity passives supplied through authorized channels may be managed through established component declarations and approved manufacturer lists. Custom cable assemblies, legacy sensors, low-volume adapter boards, and altered field harnesses need closer control because a small undocumented substitution can change the material profile of the delivered unit.
Distributor paperwork should not be mistaken for original manufacturing evidence. It can establish chain of custody and lot traceability, but it rarely resolves the composition of a connector, cable, or encapsulated electronic module. Where the original source is unavailable, classify the item as an evidence gap rather than converting a distributor assurance into a material declaration.
Use test data correctly when documentation is incomplete
Analytical testing is a verification tool, not a substitute for a controlled compliance program. Screening methods are useful for identifying metals, brominated compounds, or suspect regions, but a screening result alone may not distinguish the restricted chemical form, establish concentration in a complex polymer, or represent an entire product lot. Follow-up laboratory analysis must be selected for the substance and material under question.
Sampling is especially important for sensors with mixed construction. Testing only the aluminum enclosure or stainless mounting face says little about the cable jacket, molded connector, soldered board, or black elastomer seal. Conversely, destructive testing of every part may be unreasonable when robust declarations, traceability, and change controls exist. The most defensible approach directs testing toward uncertainty: undocumented legacy stock, mixed lots, unusual coatings, custom overmolds, repaired assemblies, or parts changed without an updated declaration.
Record the sampled unit, lot, physical sampling point, preparation method, laboratory method, detection limits, and result interpretation. A report that states only “pass” cannot be reconciled later with a drawing revision or a material substitution. When test evidence conflicts with a declaration, quarantine the affected configuration until the discrepancy is resolved. The declaration may refer to a prior revision, the tested unit may be counterfeit or incorrectly sourced, or the selected test method may be unsuitable; none of these explanations should be assumed without investigation.
Control modifications made after the sensor arrives
Deployment activities can alter the compliance status of an otherwise documented product. Field-installed connectors, replacement cables, soldered terminations, heat-shrink, adhesive labels, protective coatings, mounting pads, and repair materials become part of the supplied or installed assembly according to the applicable product boundary. A compliant sensor connected to an undocumented extension lead has not automatically produced a compliant sensing system.
Installation environments also create choices that affect materials. Outdoor and washdown applications may require a different cable jacket, corrosion-resistant coating, or sealed gland. High-temperature zones can drive the selection of fluoropolymer insulation, specialized potting, or high-temperature adhesives. Motion axes introduce repeated flexing, which may lead to a cable change after qualification. Treat each of these as an engineering change with both performance and material-compliance review, rather than as a maintenance detail.
Repair is a separate concern. Replacing a failed connector with a locally sourced equivalent, reworking a PCB with an uncontrolled solder alloy, or repotting a damaged sensor can break the evidence chain. Repair instructions should identify approved materials and define when a repaired item needs new documentation or must be removed from the compliant configuration baseline.
Release only after the evidence is internally consistent
A deployment file should allow an independent reviewer to move from the installed sensor’s identifier to the conformity statement, component-level evidence, applicable exemptions, test reports where used, and any approved deviations. The file should also show that accessories and modifications were included in the review. The goal is not document volume; it is a clear line from the assembled unit to substantiated material claims.
Before release, resolve mismatched revisions, unsigned declarations, missing cable or connector data, expired or unsupported exemptions, unexplained test results, and generic certificates that do not name the actual part. A controlled exception can be recorded when the applicable framework permits it, but an unresolved gap should remain visible rather than being buried in a purchasing record.
After deployment, retain the evidence with change notifications, incoming inspection records where applicable, and replacement-part approvals. RoHS verification is most reliable when it survives a cable substitution, a sensor revision, and a later audit without relying on memory or a marketing claim.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 11, 2026How payload and reach change the cost of an industrial robotCost of industrial robot systems depends heavily on payload and reach. Learn how sizing, torque, tooling, safety, and lifecycle factors shape smarter automation investments.Chen Wei (Automation Lead Engineer)
 Oct 10, 2026When does the cost of industrial robots pay back in high-volume production?Cost of industrial robots: discover how high-volume manufacturers calculate payback through uptime, cycle time, labor, quality, and integration before investing.Chen Wei (Automation Lead Engineer)
 Oct 09, 2026What does a manufacturing robot really cost beyond the purchase price?Manufacturing robot cost goes far beyond the purchase price. Explore integration, tooling, safety, uptime, and total ownership factors for smarter automation investments.Chen Wei (Automation Lead Engineer)
 Oct 08, 2026AGV vs. AMR: Which Is Better for Frequently Changing Routes?Which is better for changing routes? Compare AGVs and AMRs for flexible navigation, docking precision, traffic control, and faster facility reconfiguration.Chen Wei (Automation Lead Engineer)