Prepreg Composite Selection: Key Criteria for Strength, Weight, and Process Fit
Publication Date
author
Prepreg composite selection is rarely about finding the “best” material in the abstract. For technical evaluators, the real task is narrower and more consequential: identifying the fiber-resin system, form, and cure route that can meet structural targets without creating hidden manufacturing, certification, or supply-chain risk. In aerospace, UAVs, robotics, and other advanced industrial programs, prepreg choices often look similar on a data sheet but behave very differently once layup complexity, storage rules, out-time exposure, cure pressure, and inspection requirements enter the picture.
That is why this topic deserves attention well beyond materials engineering. A prepreg decision affects part mass, stiffness retention, production takt time, scrap rate, freezer logistics, requalification burden, and even supplier concentration risk. If the application is weight-sensitive and structurally loaded, prepreg composite selection becomes a system-level decision, not a purchasing line item.
What buyers and evaluators are usually trying to decide
Most searchers looking into prepreg composite selection are not asking for a definition of prepreg. They are trying to answer four practical questions:
- Will prepreg deliver a measurable advantage over wet layup, infusion, or metallic alternatives in this program?
- Which performance claims actually matter for the intended load case and operating environment?
- Can the factory repeatedly process this material without cost and schedule instability?
- What qualification evidence is enough before locking a material into a design or approved supplier list?
Those questions matter because prepreg can be an excellent solution for high-performance structures, but it is unforgiving of weak process control. The common industry shorthand that “prepreg equals high strength and low weight” is directionally true, yet incomplete. The better statement is that prepreg can enable high fiber volume, controlled resin content, and repeatable laminate properties when the process window is understood and maintained. Without that discipline, the theoretical advantage can erode quickly.
Start with the load case, not the marketing class of the material
A recurring mistake in selection reviews is beginning with broad labels such as “aerospace-grade carbon prepreg” or “high-modulus system.” Those labels are too coarse to support a decision. The first filter should be the actual structural demand: tensile load, compressive stability, interlaminar shear, impact tolerance, fatigue exposure, vibration, thermal cycling, or a combination of these.
For example, a UAV wing skin, a robotic arm shell, and a satellite bracket may all use carbon prepreg, but the governing failure modes can be completely different. One design may be buckling-limited, another impact-sensitive, and another driven by thermal dimensional stability. In these cases, fiber modulus alone does not decide suitability. Evaluators need to look at laminate-level behavior, not just constituent-level prestige.
In practical terms, selection should begin with a question set like this: what load is dominant, what failure mode is least tolerant, what environmental condition shifts the margin most, and what defect type is most likely in production? Those answers narrow the field faster than brand comparisons do.
Strength-to-weight only matters if the laminate can keep it in service
Weight reduction is a legitimate driver, but many selection discussions stop at nominal tensile strength or stiffness. That is not enough. The useful comparison is retained performance at the operating temperature, humidity, fatigue spectrum, and damage state that the part will actually see.
A resin system with attractive room-temperature properties may lose margin if the part lives near elevated service temperatures. Another system may tolerate impact or drilling damage better, which can matter more than peak coupon strength in fielded equipment. For UAV, aerospace, and mobile robotics applications, compressed development timelines often push teams toward familiar systems, but familiarity should not substitute for retained-property data.
Technical evaluators should ask for evidence around these points, ideally at laminate level or subcomponent level where available:
- Compression after impact behavior
- Fatigue retention over relevant cycle bands
- Open-hole tensile and compression performance
- Hot-wet property retention
- Glass transition temperature and usable design margin below it
- Interlaminar toughness, especially for complex geometries or bonded assemblies
If those data are unavailable, incomplete, or only presented as best-case coupon values, that is not an automatic rejection. But it does mean the selection carries more qualification burden than the headline numbers suggest.
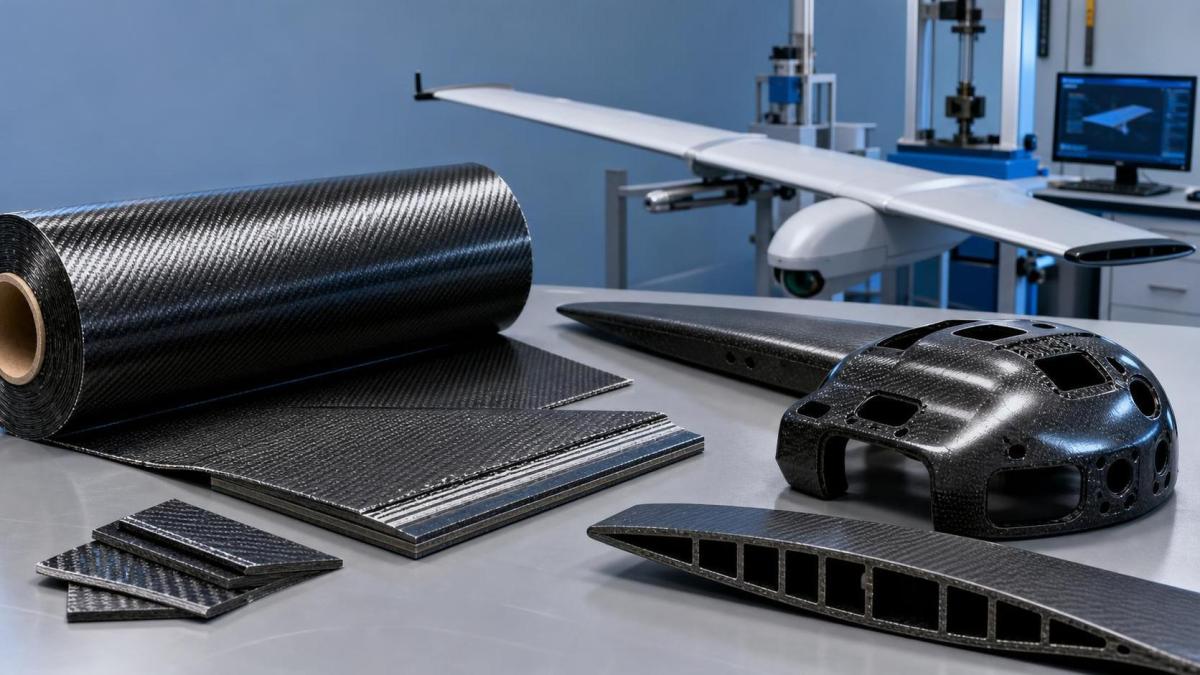
Process fit is often the real divider between viable and non-viable options
In many programs, two prepreg systems can both meet structural requirements on paper. The deciding factor then becomes manufacturing compatibility. This is where selection decisions usually become expensive if handled too late.
Prepreg materials differ materially in cure temperature, pressure requirements, drape behavior, tack, layup speed, and sensitivity to out-time. Those variables shape labor efficiency and defect risk far more than early-stage teams sometimes assume. A material that performs well in a controlled aerospace autoclave environment may be difficult to scale in a mixed industrial setting with frequent work interruptions, variable ambient conditions, or limited freezer capacity.
Several process-fit questions should be treated as first-order criteria:
- Is the program built around autoclave, out-of-autoclave, press cure, or oven/vacuum bag processing?
- Can the plant maintain the required cold storage and out-life discipline?
- How complex is the layup geometry, and does the prepreg conform without bridging or wrinkling?
- What is the acceptable cure cycle length relative to takt time?
- How much rework is realistic if debulking, bagging, or ply placement drifts off target?
- What inspection method will verify laminate quality at production volume?
This is where “high performance” materials can fail the business case. A resin system that needs tighter timing, more aggressive debulking control, or longer cure cycles may still be the right answer for a flight-critical part. But for medium-volume industrial structures, a slightly lower-performing system with a wider process window can produce a better delivered result.
Fiber architecture and form factor matter more than many procurement teams expect
Selection is not only about resin chemistry or fiber grade. Fabric style, unidirectional versus woven formats, areal weight, and backing/carrier details all influence how the part behaves and how easy it is to manufacture.
Unidirectional prepreg can maximize directional performance, but it demands disciplined stacking strategy and may complicate handling for intricate parts. Woven prepregs may improve handling and damage tolerance in some cases, while trading away some directional efficiency. Heavier areal weights can improve layup speed but may reduce conformability around tight radii or complex transitions.
These are not secondary details. They affect wrinkling risk, resin-rich zones, ply drops, local thickness control, and ultimately repeatability. For technical evaluators, it is worth checking whether the proposed form has already been used in a geometrically similar part, not just in the same sector.
Supply chain risk is part of material performance
A prepreg that meets every engineering target but sits on a fragile supply base is not a stable selection. This has become more visible as aerospace recovery, defense demand, regionalization strategies, and raw material constraints have tightened parts of the composites value chain. Availability can vary by fiber type, resin family, cure format, export controls, and geography. Specific lead-time claims are highly supplier- and region-dependent and should be treated as 【待核实】 unless contractually confirmed.
For that reason, technical evaluation should include commercial and operational questions early:
- Is there a qualified second source, or is the system effectively single-source?
- Will a future form-fit-function change trigger full requalification?
- Are minimum order quantities aligned with program ramp and shelf life?
- How much usable material is lost through expiry, kit complexity, or cutting scrap?
- Can the supplier provide consistent batch traceability and change notification discipline?
This is especially important for organizations trying to reduce supplier qualification cycles. A disciplined spec is not only a set of target properties; it is also a statement about what process and sourcing variability the business is prepared to absorb.
Qualification data should match the application, not just the brochure
One of the most common traps in prepreg composite selection is over-relying on generic technical data sheets. These documents are useful screening tools, but they do not close the gap between nominal material capability and application-specific confidence. Different cure tools, laminate schedules, part thicknesses, and inspection criteria can materially change the outcome.
For non-trivial programs, evaluators should push for a staged evidence approach. Start with supplier data and internal screening, then move to representative laminate testing, then to subcomponent or prototype validation under realistic process conditions. This is slower than brochure-based selection, but it usually shortens the total decision cycle by avoiding late redesigns.
A practical evaluation sequence often looks like this:
The point is not to make every selection process heavy. It is to scale the evidence to the risk. A secondary cover panel and a flight- or safety-relevant primary structure should not be qualified with the same level of confidence.
Common claims that deserve a harder look
Several industry claims around prepreg materials are partly true but often oversimplified in sourcing conversations.
“Higher modulus is better.” Not necessarily. Higher modulus may improve stiffness, but it can also affect brittleness, impact response, and cost. The right answer depends on the load path and failure tolerance.
“Autoclave prepreg always outperforms out-of-autoclave systems.” In some demanding applications, autoclave processing still offers strong advantages. But application requirements, void tolerance, geometry, and production economics matter. “Always” is too broad.
“If the coupon data are strong, the part will be strong.” Only if the manufacturing route can repeatedly reproduce the laminate quality behind those numbers. Part geometry and processing discipline can dominate real outcomes.
“Prepreg reduces weight, so it reduces total cost.” Sometimes. In mobility or aerospace systems, lower weight can create downstream system value. But storage, handling, cure time, tooling, scrap, and qualification can offset that advantage if the program is not volume- or performance-aligned.
Where this matters most right now
Prepreg composite selection is becoming more strategic in segments where structural efficiency and system integration are tightening simultaneously. Commercial UAV platforms, lightweight robotic manipulators, satellite substructures, advanced enclosures for sensing payloads, and high-precision industrial motion systems all face stronger demands for lower mass, tighter control, and faster development cycles.
At the same time, procurement teams are being asked to reduce supplier risk, engineering teams are being pushed to qualify faster, and manufacturing teams are expected to industrialize more quickly. That combination increases the value of data-backed material selection and reduces tolerance for vague claims.
For organizations operating in that environment, the strongest prepreg decision is usually the one that connects five layers clearly: the load case, the service environment, the process window, the quality assurance method, and the supply base. If one of those layers remains speculative, the selection is still provisional no matter how impressive the material branding sounds.
Technical evaluators do not need a perfect material. They need a material system whose performance is credible in the actual factory, under the actual duty cycle, with the actual supplier discipline available to the program. That is the threshold where prepreg composite selection becomes a decision you can defend in design review, procurement review, and production ramp at the same time.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 10, 2026When does the cost of industrial robots pay back in high-volume production?Cost of industrial robots: discover how high-volume manufacturers calculate payback through uptime, cycle time, labor, quality, and integration before investing.Chen Wei (Automation Lead Engineer)
 Oct 09, 2026What does a manufacturing robot really cost beyond the purchase price?Manufacturing robot cost goes far beyond the purchase price. Explore integration, tooling, safety, uptime, and total ownership factors for smarter automation investments.Chen Wei (Automation Lead Engineer)
 Oct 08, 2026AGV vs. AMR: Which Is Better for Frequently Changing Routes?Which is better for changing routes? Compare AGVs and AMRs for flexible navigation, docking precision, traffic control, and faster facility reconfiguration.Chen Wei (Automation Lead Engineer)
 Oct 07, 2026How Much Does an Automated Guided Vehicle Cost in 2026?How much does an automated guided vehicle cost in 2026? Explore AGV price ranges, hidden deployment costs, and smart buying factors for stronger ROI.Chen Wei (Automation Lead Engineer)
 Oct 06, 2026Are Collaborative Robots Safe Enough to Operate Without Fencing?Are collaborative robots safe enough to work without fencing? Explore risk assessment, safeguarding options, and practical guidance for safer, productive cobot cells.Chen Wei (Automation Lead Engineer)