
CAD to CAM conversion data loss in complex toolpaths
Publication Date
author
In complex machining environments, CAD to CAM conversion data loss can silently distort toolpath fidelity, surface finish, and cycle-time predictability. For engineers, operators, buyers, and technical decision-makers, understanding how geometry translation interacts with cnc controller interpolation cycle, robotic welding offline programming, and predictive maintenance software for cnc is essential to reducing scrap, qualification delays, and hidden production risk.
In practice, the problem rarely appears as a dramatic system failure. It usually shows up as a 0.02 mm contour deviation on a tight radius, an unexpected slowdown in a 5-axis finishing pass, or a weld path that looks correct in simulation but drifts at the robot controller. Those small mismatches accumulate into rework, machine idle time, inspection escapes, and supplier disputes.
For organizations that operate under aerospace, medical, automation, or high-mix precision machining requirements, CAD to CAM conversion data loss is not only a programming inconvenience. It is a supply chain risk that affects quoting accuracy, process capability, digital thread integrity, and confidence in production scaling. A data-driven approach is the only reliable way to identify where translation errors begin and how to contain them before they reach the shop floor.
Why CAD to CAM Conversion Data Loss Happens in Complex Toolpaths
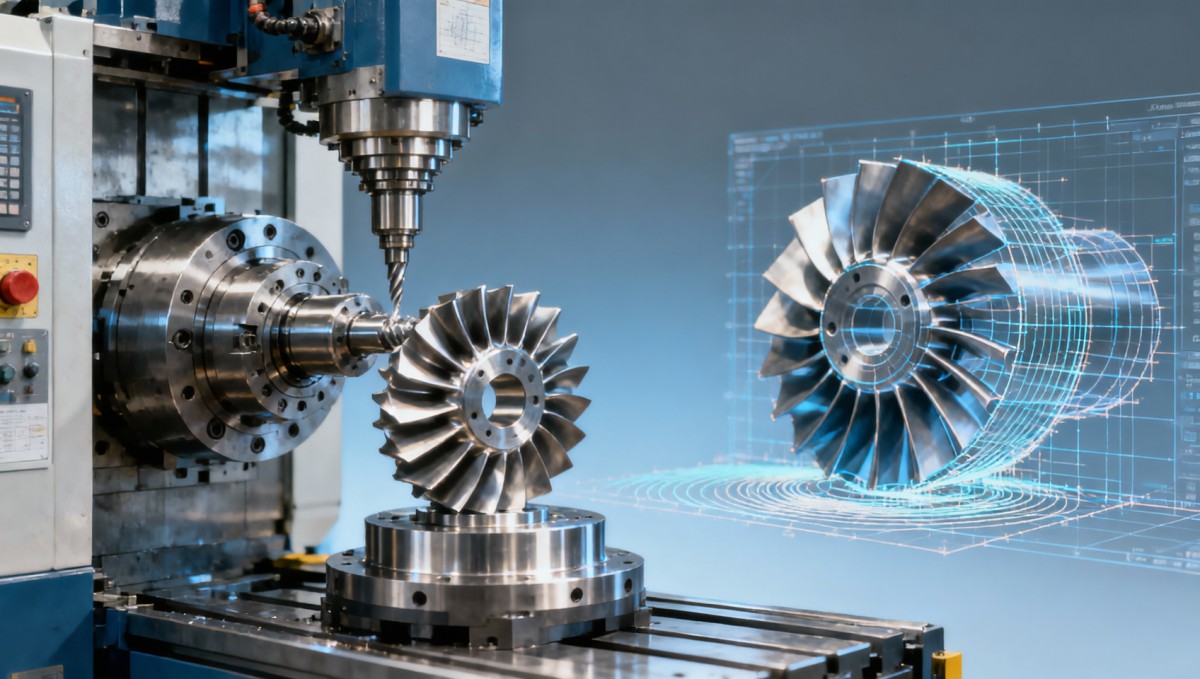
Complex toolpaths depend on more than visible geometry. A CAD model may contain NURBS surfaces, trimmed faces, spline edges, tiny gaps, mixed tolerances, and metadata created in different design systems. When that model is exported through STEP, IGES, Parasolid, or STL, some of the mathematical definition can be approximated, simplified, or reinterpreted. The CAM system then generates motion based on what it receives, not on what the designer intended.
The risk increases in 3-axis sculptured surfaces, 5-axis swarf cutting, impeller machining, turbine blade finishing, mold texturing, and robotic welding offline programming. In these scenarios, even a small mismatch between surface continuity and tool orientation can change cusp height, feed consistency, or collision margin. A tolerance shift from 0.005 mm to 0.05 mm may look minor in software, yet it can materially alter the machine path over thousands of interpolation points.
Another common source is tessellation. If the CAD model is converted into a faceted representation too early, smooth curves become short line segments. That may overload the cnc controller interpolation cycle, especially on older controls operating at 1 ms to 4 ms interpolation intervals. The controller has to process more blocks, acceleration changes become harsher, and actual feedrate can drop well below programmed feedrate.
Data loss also occurs when feature intent disappears. Hole axes, tangent relations, blend hierarchy, weld seam definitions, and stock allowance assumptions are not always preserved across software environments. For operators, that means more manual edits. For buyers and decision-makers, it means the quoted process may not match the real process capability once the part enters production.
Typical translation weak points
- Surface healing issues such as gaps below 0.01 mm that become open edges after export.
- Loss of spline continuity, where G2 or G3 curvature becomes segmented geometry.
- Coordinate system mismatch between CAD origin, CAM setup, and machine work offset.
- Post-processor rounding that converts smooth tool vectors into coarse angular steps.
- Controller memory and block-processing limits that force path smoothing or deceleration.
The table below summarizes how different data conversion issues affect machining behavior, inspection outcomes, and operational cost. It is especially useful for procurement teams comparing software stacks or outsourced programming vendors.
The key takeaway is that conversion data loss is rarely isolated to geometry. It propagates into control behavior, verification time, and supplier performance. Teams that treat CAD export, CAM import, and controller execution as one connected chain typically identify errors 1 to 2 process stages earlier than teams that validate each system separately.
How Data Loss Affects Surface Finish, Tolerance, and Cycle Time
From an engineering standpoint, the first measurable impact is often on surface quality. When a freeform surface is converted with insufficient precision, the CAM system may generate an excessive number of micro-segments. The machine then accelerates and decelerates repeatedly, which can leave witness marks, waviness, or inconsistent scallop patterns. On hardened steel molds or aerospace aluminum skins, that can turn a Ra 0.8 µm target into a surface that needs secondary polishing.
Tolerance performance is affected in a different way. A part can pass nominal toolpath simulation and still fail in-machine due to interpolation load, look-ahead limits, servo lag, or mismatched arc fitting. If the machine controller can process only a certain number of blocks per second, actual motion will not match ideal CAM motion. On tight profiles, a deviation band of ±0.01 mm may widen toward ±0.03 mm or more under aggressive high-speed settings.
Cycle time predictability is another hidden loss. CAM may estimate a finishing routine at 42 minutes, but the machine may take 54 minutes because it cannot sustain the programmed feed through segmented geometry. For production planners, that 20% to 30% gap affects capacity planning, labor scheduling, and quotation accuracy. For procurement, it also changes the true cost comparison between two machining suppliers that appear similar on paper.
In robotic welding offline programming, comparable distortion occurs when seam curves are simplified or tool center point orientation is not preserved accurately. The result may be underfill, inconsistent bead width, or more touch-up. The lesson is the same across subtractive and robotic processes: if geometry fidelity declines upstream, process stability declines downstream.
Operational symptoms that should trigger investigation
- Cycle time on the machine is consistently more than 10% higher than CAM simulation.
- Surface finish varies by region even though tool, feed, and stepover are unchanged.
- First-article deviations cluster around blends, fillets, and multi-axis transitions.
- Operators need repeated hand edits to lead-in, lead-out, smoothing, or arc-fit settings.
- Robot welds pass simulation but require frequent seam tracking corrections.
Controller behavior matters as much as geometry quality
Many teams focus on export format but underestimate controller execution. A modern control with advanced look-ahead, jerk management, and spline support may handle dense data far better than a legacy platform. That is why cnc controller interpolation cycle should be reviewed during process planning. A machine running a 0.5 ms to 1 ms internal processing cycle with robust smoothing can maintain contour accuracy more effectively than a system limited by older block-handling architecture.
For decision-makers, this means software selection cannot be separated from machine fleet capability. A premium CAM license does not automatically produce premium output if the downstream controller, post-processor, and networked data workflow are not aligned to the same tolerance and throughput requirements.
Selection Criteria for Engineers, Buyers, and Technical Decision-Makers
When evaluating CAD, CAM, post-processing, or outsourced programming services, the most useful question is not whether a platform supports complex toolpaths. Most major systems do. The better question is how reliably the full chain preserves geometry intent from native model to executable machine code. That requires measurable selection criteria, not marketing language.
Engineering teams should first define the tolerance class they actually need. A mold shop finishing cosmetic surfaces may prioritize smoothness and cusp control. An aerospace supplier machining thin-wall titanium may prioritize vector stability and chatter avoidance. A robotic cell integrator may prioritize path continuity and tool orientation repeatability over pure geometric density. The right benchmark depends on whether the process window is ±0.005 mm, ±0.02 mm, or broader.
Procurement teams should ask vendors for evidence around translation reliability, not just software compatibility. Useful evidence includes import/export tolerance settings, supported native kernels, post-processor validation workflow, sample first-pass yield, and machine-controller matching experience. Even a 5-step workflow review can reveal whether a supplier understands the true source of conversion risk.
Technical leaders should also review how predictive maintenance software for cnc fits into the digital workflow. While predictive tools do not fix geometry errors, they help distinguish path-related instability from mechanical degradation. If spindle load spikes, servo following error, or vibration anomalies increase only on certain converted paths, the issue may be digital rather than mechanical.
Practical evaluation checklist
- Verify whether native CAD import is available or whether the process depends on neutral formats only.
- Check if tolerances can be controlled at export, CAM calculation, verification, and post levels separately.
- Confirm support for arcs, splines, NURBS, and controller-specific smoothing functions.
- Review a sample part with at least 3 critical features such as freeform surfaces, deep cavities, and 5-axis transitions.
- Ask for real machine comparison between simulated cycle time and actual cycle time over at least 2 trial runs.
The following table can be used as a structured procurement and qualification reference when comparing internal solutions, contract manufacturers, or integration partners.
A disciplined evaluation framework prevents expensive false confidence. Two vendors can both claim 5-axis capability, yet only one may consistently maintain acceptable path fidelity across 50,000 to 200,000 motion blocks on a demanding component. Measured process evidence is the only credible differentiator.
Implementation Strategy: From Digital Model to Stable Production
Reducing CAD to CAM conversion data loss requires a workflow that treats design, programming, machine execution, and maintenance as one closed loop. The strongest implementations begin with data governance. Teams standardize acceptable file formats, define export tolerances by part family, and lock post-processor revisions. Without that discipline, even a well-programmed process becomes inconsistent from shift to shift or supplier to supplier.
A practical rollout often follows 4 stages. Stage 1 is geometry validation, including gap checks, surface continuity review, and model simplification rules. Stage 2 is CAM validation, where teams compare toolpath density, smoothing options, and stock-to-finish transitions. Stage 3 is machine validation, including dry run, prove-out, and actual feed comparison. Stage 4 is monitored production, where predictive maintenance software for cnc and quality data are used to detect drift over time.
For robotic welding offline programming, the same structure applies with different checkpoints: seam extraction quality, TCP orientation integrity, simulation-to-robot frame mapping, and weld result verification. If conversion quality is not checked before deployment, operators end up correcting path problems manually at the cell, which defeats the purpose of offline programming and stretches commissioning time from days into weeks.
A mature organization also creates escalation thresholds. For example, if actual cycle time differs from simulation by more than 12%, if measured surface error exceeds the target band by more than 25%, or if robot path correction exceeds a set number of points per program, the file chain should be reviewed before additional batches are released.
Recommended control points in the workflow
Before programming
- Run model healing and record the number of repaired faces, edges, and gaps.
- Set part-family export tolerance, such as 0.001 mm to 0.01 mm depending on feature class.
- Preserve datum and coordinate references for downstream setup and inspection.
During CAM and posting
- Compare smoothing, arc fitting, and segmentation settings on a representative feature.
- Verify post output against controller capabilities instead of generic machine definitions.
- Check whether tool vector changes remain within the machine’s stable motion envelope.
During production
- Track actual versus programmed feedrate on selected high-density toolpath zones.
- Monitor spindle load, axis following error, and vibration signatures on recurring jobs.
- Feed inspection and maintenance data back to programming within the same revision cycle.
This closed-loop method is aligned with TSV’s data-first perspective. Parameters, tolerances, and execution evidence should determine process confidence. Organizations that formalize these checkpoints typically reduce non-value-added prove-out iterations, shorten supplier qualification cycles, and improve confidence in quoting repeat jobs.
FAQ for Research, Procurement, and Operations Teams
How can a team tell whether poor finish comes from conversion data loss or machine condition?
Look for pattern consistency. If finish defects appear only on geometrically dense areas, only after a file format change, or only on programs created through a certain export route, the issue may be conversion-related. If defects appear across different programs and increase gradually over 2 to 6 weeks, spindle wear, backlash, or servo condition may be more likely. Predictive maintenance software for cnc is valuable here because it adds load, vibration, and temperature context to the programming data.
What file formats are usually safest for complex toolpaths?
There is no universal answer because safety depends on the CAD kernel, CAM engine, and machine target. Native formats often preserve more intent, while STEP or Parasolid may offer stable exchange when systems are compatible. IGES is still used, but it may require more healing in complex surfaces. STL should be treated carefully for machining because it is faceted by definition and can create unnecessary path density for high-precision finishing.
What should buyers ask a machining supplier before approving a complex part?
Ask for their import workflow, healing process, post-processor validation method, and a comparison between simulated and actual cycle time on similar geometry. It is reasonable to request evidence of how they handle 3 to 5 critical features, what tolerance band they use during model exchange, and whether their machines support advanced smoothing or spline interpolation. These answers are more useful than generic claims about quality.
Does robotic welding offline programming face the same conversion risks as CNC machining?
Yes, although the symptoms differ. In CNC machining, the result may be poor finish or contour deviation. In robotic welding offline programming, the result may be torch angle drift, seam offset, inconsistent bead geometry, or more touch-up on the floor. In both cases, the core issue is loss of path intent between the digital model and executable motion.
CAD to CAM conversion data loss should be treated as a measurable engineering and sourcing problem, not as an unavoidable software nuisance. The strongest organizations control geometry fidelity, align CAM output with cnc controller interpolation cycle behavior, and use predictive maintenance software for cnc to separate digital path issues from mechanical instability. They also apply the same discipline to robotic welding offline programming, where path continuity and orientation accuracy directly affect production quality.
For engineers, operators, buyers, and enterprise decision-makers, the commercial value is clear: fewer prove-out loops, tighter surface and tolerance control, more realistic cycle-time forecasting, and faster supplier qualification. If your team is assessing digital manufacturing workflows, evaluating precision machining partners, or trying to reduce hidden risk in complex toolpaths, now is the right time to review the entire data chain. Contact us to discuss your application, request a tailored evaluation framework, or explore more data-driven solutions for high-precision production.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 15, 2026R&D Cost Reduction Services: How to Evaluate Fees, Savings, and ROIEvaluate R&D cost reduction services with confidence. Compare fees, verify savings, and calculate ROI without compromising performance. Discover how to choose a provider that delivers real value.Chen Wei (Automation Lead Engineer)
 Oct 15, 2026How Should You Compare TechStat Vanguard 5-Axis CNC Tolerances?TechStat Vanguard 5-axis CNC tolerance comparison: learn how to verify part accuracy, assess inspection evidence, and choose suppliers that reliably meet your drawing requirements.Dr. Marcus Vance
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)























