
CNC Turning for Aerospace Fasteners and the Risk of Hidden Runout
Publication Date
author
In aerospace fastening, the biggest quality threat is often invisible: hidden runout. For engineers, operators, buyers, and decision-makers evaluating cnc turning for aerospace fasteners, understanding how cnc spindle runout measurement and swiss turning concentricity tolerance affect fit, fatigue, and assembly reliability is essential. This article examines where hidden runout begins, why it distorts aerospace alloy fatigue life data, and how precision-driven machining controls reduce risk before defective parts reach critical applications.
Why hidden runout matters more than many aerospace fastener teams expect
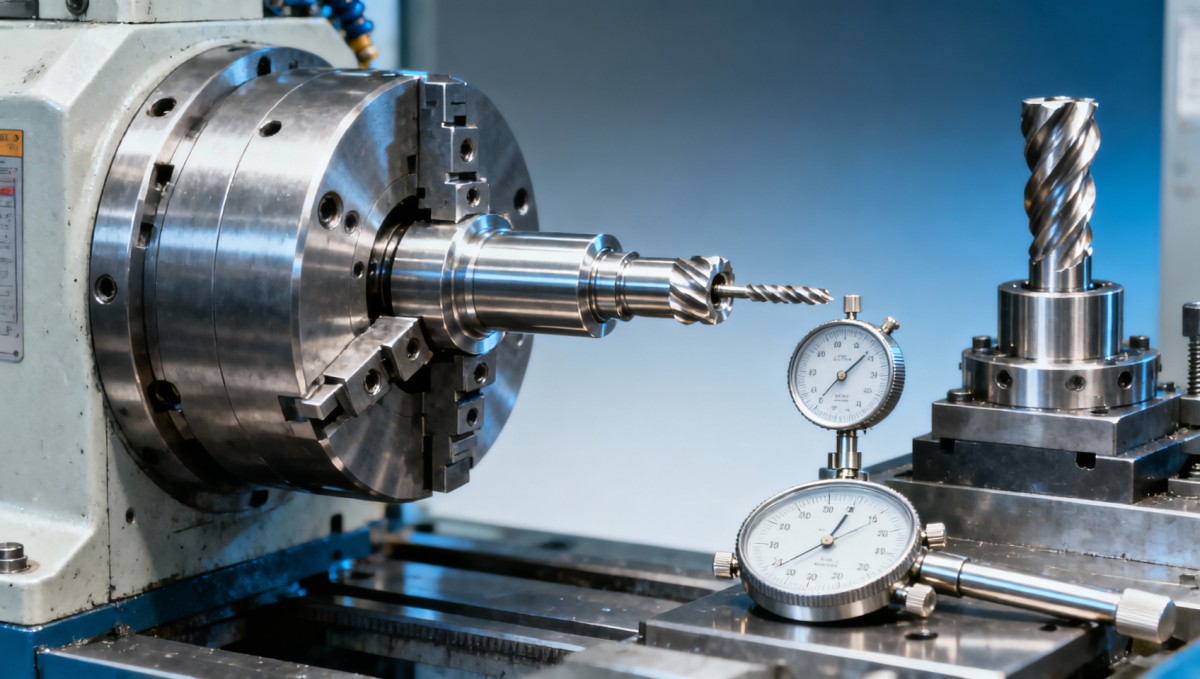
In aerospace production, fasteners are not simple commodity parts. A turned pin, screw blank, collar, bushing, or threaded shaft may sit inside a vibration-rich, thermally variable, and fatigue-sensitive assembly for thousands of flight hours. When hidden runout is introduced during turning, the part can still appear dimensionally acceptable on a basic diameter check, yet fail to rotate concentrically during assembly or service.
That is why cnc turning for aerospace fasteners cannot be assessed only by nominal size and surface finish. Procurement teams often receive drawings with diameter tolerances, length tolerances, and material callouts, but insufficient emphasis on axis integrity. In practice, a few microns of radial deviation can amplify thread engagement variation, seating inconsistency, and clamp load imbalance, especially in small-diameter parts produced in medium to high volumes.
For operators, hidden runout often begins upstream: spindle condition, guide bushing wear, collet mismatch, tool deflection, bar stock straightness, or workholding contamination. For engineers, the issue becomes harder because poor concentricity can distort fatigue test interpretation. A fastener thought to have failed because of alloy limitation may actually have failed because the loading axis was no longer true.
At TSV, the central principle is straightforward: parameters do not lie. In a market crowded with generic quality claims, the useful question is not whether a supplier says a part is “precision machined,” but whether the supplier can define spindle runout checks, in-process concentricity control intervals, and part-specific acceptance logic for aerospace fastening geometry.
What “hidden” really means in turning operations
Runout is called hidden when it escapes routine inspection but remains functionally significant. This often happens in parts with a total length of 10 mm–80 mm, slender shanks, underhead features, or thread roots that are measured separately instead of as one continuous axis system. A component can pass individual feature checks while failing the assembled rotational truth requirement.
In Swiss turning, the problem can be even more subtle. The process is excellent for small aerospace fasteners because it stabilizes slender workpieces, but that advantage depends on guide bushing condition, bar quality, thermal behavior, and tooling alignment. Swiss turning concentricity tolerance is not only a machine capability question; it is also a process discipline question checked over time, not once at setup.
Aerospace buyers should therefore separate visible defects from latent geometric defects. Burrs, scratches, and obvious taper are easy to detect. Hidden runout is different because it may only appear when the part is indicated between centers, spun in a precision fixture, or correlated with downstream assembly force variation.
- Visible nonconformance: burrs, chatter marks, thread damage, incorrect length, obvious taper.
- Hidden nonconformance: spindle-induced axis deviation, concentricity drift over batch time, collet seating variation, and bar whip effects.
- High-risk timing: first-off approval without mid-batch verification, long unattended runs, tool life transitions, and machine warm-up periods in the first 30–90 minutes.
Where hidden runout starts: machine, setup, material, and inspection links
Most hidden runout problems do not come from one catastrophic error. They result from stacked contributors that stay below attention thresholds until the part reaches assembly. This is why cnc spindle runout measurement should be treated as one element in a larger chain including spindle nose condition, collet repeatability, bar feed stability, insert wear, coolant behavior, and measurement fixture quality.
For purchasing teams comparing suppliers, asking only for machine brand or machine age is not enough. A newer lathe can still produce unstable axis geometry if preventive maintenance intervals are weak or if workholding is poorly matched to the part. Conversely, a mature machine in a tightly controlled cell may deliver stable results if spindle checks, fixture cleaning, and process capability review are done every shift or every defined production lot.
The table below helps separate common runout sources by process stage. This is useful when evaluating cnc turning for aerospace fasteners because it turns a vague quality discussion into a traceable list of controllable variables.
The important takeaway is that hidden runout is usually systemic. If a supplier cannot explain how these four stages connect, the risk does not disappear simply because first article dimensions look clean. The more flight-critical the fastening function, the more valuable it is to map defect origin before purchase approval.
Three operator-level triggers that often go unnoticed
Operators and cell supervisors are often the first line of defense. Yet hidden runout grows quietly when daily controls become visual only. Three triggers deserve attention in runs lasting 2–8 hours or across multiple bar changes.
1. Thermal drift after setup approval
A machine may indicate well when cold, then shift after a stable production load develops. This is especially relevant in high-speed small-part turning, where heat accumulation changes spindle and tooling behavior over the first production window.
2. Collet reuse beyond stable life
Repeated clamping cycles reduce repeatability. The issue is not always dramatic enough to fail diameter control, but it can move axis alignment enough to challenge swiss turning concentricity tolerance on thin shanks and thread preforms.
3. Measurement mismatch
If production checks use one fixture and final inspection uses another, teams may compare numbers that are not directly equivalent. For aerospace fasteners, a measurement plan should define datum logic, support conditions, and acceptable sampling intervals such as every 30 pieces, every hour, or every bar change depending on criticality.
How hidden runout changes fit, torque, and fatigue interpretation
The mechanical impact of hidden runout is rarely isolated to one symptom. In mating assemblies, a non-true axis changes how contact begins, how threads seat, and how clamp force distributes. This can produce installation scatter that users notice as variable torque feel, erratic seating depth, or unexplained locking behavior even when thread gauges pass.
For design and validation teams, the larger risk is analytical distortion. If aerospace alloy fatigue life is evaluated on parts affected by unnoticed runout, the test no longer represents material behavior alone. It now reflects a geometry-induced loading bias. That can mislead material selection, process approval, and supplier comparison, especially when the sample size is limited to 10–30 pieces in early qualification.
This is why TSV emphasizes engineering truth through data. A fatigue curve, pull test, or torque-tension result has little decision value unless the axis quality of the tested fastener is understood. Without that context, procurement may reject a capable material or approve a risky process based on incomplete signals.
Practical effects by downstream function
The table below links hidden runout to what different teams actually observe. It is useful in cross-functional reviews because engineering, quality, and sourcing often describe the same problem in different language.
For decision-makers, this means unit price alone is a weak selection metric. If hidden runout increases assembly time by even a small amount per part across thousands of installations, the total cost quickly exceeds an apparent machining saving. In aerospace and UAV programs, the cheapest turned fastener is often the one that generates the highest quality-management burden later.
- Engineering impact: misread design margin and unclear fatigue root cause.
- Operator impact: unstable fit, inconsistent torque feel, more line-side sorting.
- Procurement impact: slower supplier approval, higher incoming inspection cost, and more NCR investigation cycles.
- Executive impact: delayed launch timing, greater compliance exposure, and weaker confidence in technical reports.
What buyers should ask before approving cnc turning for aerospace fasteners
A strong sourcing decision does not start with a marketing brochure. It starts with a disciplined question set. Whether the application is commercial aerospace, UAV subsystems, precision connectors, or safety-related industrial hardware, buyers should ask for process evidence that ties dimensional compliance to axis integrity. This is where many RFQs remain too vague.
Instead of asking, “Can you machine tight tolerances?” ask how the supplier defines and controls those tolerances over a batch. Ask how often cnc spindle runout measurement is performed, how Swiss turning concentricity is monitored during long runs, and what the reaction plan is when drift appears after tool change or thermal stabilization.
The checklist below is designed for information researchers, users, buyers, and enterprise decision-makers who need faster technical screening without relying on generic claims.
Five procurement checks that add real value
- Ask for the control method, not only the target number. A supplier should explain whether runout is checked at setup, every shift, every lot, or after each bar change.
- Confirm datum strategy. The part may include head, shank, undercut, and thread features; concentricity logic should reflect the actual functional axis of the fastener.
- Review material handling. Aerospace alloys and stainless grades can react differently to cutting load and residual stress, especially in diameters below 6 mm or with long unsupported ratios.
- Define sampling intervals. For critical parts, one first article is not enough. The plan should state lot size, in-process frequency, and final release criteria.
- Request deviation response rules. If mid-run drift is detected, what is quarantined, what is rechecked, and how are affected pieces traced?
Which standards and compliance signals are relevant?
Not every project needs the same compliance depth, but aerospace-related turning projects commonly intersect with quality-system expectations such as AS9100-aligned production environments, controlled traceability, lot discipline, material certification review, and calibrated inspection practice. The exact requirement depends on program risk and part classification.
A mature supplier discussion should also cover drawing interpretation, revision control, first article expectations, and special process handoffs if coating, heat treatment, or secondary grinding are involved. Hidden runout can be created in turning and amplified later, so the full route matters.
For buyers comparing options across regions, a practical review window is often 2–4 weeks for technical clarification, sample planning, and document exchange before serious approval discussions begin. Rushing this stage usually pushes the same uncertainty into production launch.
How to reduce hidden runout risk in implementation and supplier management
Once a supplier is shortlisted, the next objective is not only to buy parts but to build a control loop. In precision turning, hidden runout is best prevented through layered process governance: machine condition verification, setup approval, in-process monitoring, final inspection logic, and feedback from assembly or testing. Each layer catches a different failure mode.
For aerospace fasteners, implementation teams should define a simple but strict pathway from drawing to release. This is especially useful when supply chains span multiple sites, languages, or subcontractors. A short, data-based workflow reduces noise and helps teams align on measurable signals instead of assumptions.
A practical 4-step control framework
Step 1: Pre-production alignment
Confirm drawing datums, critical features, material condition, and the intended use environment. If the fastener will see vibration, cyclic load, or precise torque targets, runout significance should be explicitly stated before the first bar is cut.
Step 2: Machine and setup verification
Review cnc spindle runout measurement records, collet condition, tool package, and warm-up practice. A setup that looks stable at minute 5 may behave differently at minute 50, so the verification window should reflect actual production conditions.
Step 3: In-process sampling
Use time-based or quantity-based checks such as every hour, every 50–100 parts, or at each tool change depending on part criticality. The method matters less than consistency and documented reaction when drift appears.
Step 4: Closed-loop feedback
Link assembly findings, fatigue test anomalies, and customer complaints back to turning data. If seating variation or torque scatter rises, review axis-quality records before changing alloy, coating, or design assumptions.
- Use pilot lots to validate both dimensions and behavior, not dimensions alone.
- Separate machine capability claims from demonstrated process control over time.
- Tie supplier reviews to measurable items: runout records, inspection frequency, scrap reaction, and traceability discipline.
FAQ: common questions about runout, concentricity, and supplier selection
How is hidden runout different from a simple diameter problem?
A diameter problem is usually a size error measured directly on one feature. Hidden runout is an axis relationship problem. A part can show acceptable diameters on several features yet still rotate off-center when referenced as a complete functional component. That is why aerospace fastening programs should review both size and axis behavior.
Does Swiss turning automatically solve concentricity risk?
No. Swiss turning is highly effective for slender and small-diameter parts, but swiss turning concentricity tolerance still depends on guide bushing condition, bar stock consistency, thermal control, and inspection discipline. It improves the opportunity for stability; it does not remove the need for process verification.
What should procurement request in an RFQ?
Request the dimensional drawing review, inspection plan, runout control approach, sampling frequency, material traceability expectations, and a clear statement of how nonconforming product is contained. If the part supports fatigue-critical service, ask how axis integrity is protected before fatigue or torque testing data are used for decision-making.
What is a realistic evaluation timeline for a new supplier?
For technically demanding turned fasteners, a common planning window is 2–6 weeks for drawing review, manufacturability discussion, sample preparation, and initial data exchange. More complex routes involving secondary processing or multi-site approval may take longer, but compressing review time usually increases downstream corrective-action effort.
Why work with TSV when evaluating precision machining risk
TSV exists for teams that need engineering truth rather than generic supplier language. In precision machining benchmarks, we focus on what procurement and R&D teams actually need to compare: tolerance logic, inspection discipline, performance interpretation, and supply-chain traceability signals that affect risk. That is especially valuable when cnc turning for aerospace fasteners is being assessed across multiple vendors or regions.
If your team is reviewing fastener drawings, supplier samples, or process capability statements, we can help structure the technical questions that matter. That may include parameter confirmation, cnc spindle runout measurement expectations, Swiss turning concentricity review, supplier screening criteria, likely delivery evaluation checkpoints, and compliance-related documentation planning.
For engineering researchers, we help convert vague claims into measurable acceptance logic. For operators and quality teams, we help identify where hidden runout most likely starts. For procurement and executives, we help shorten qualification cycles by focusing attention on a small number of high-value indicators instead of broad, low-value marketing comparisons.
If you need support, contact TSV to discuss sample review, supplier comparison, tolerance-risk interpretation, expected lead-time checkpoints, certification-related questions, or a tailored benchmark framework for aerospace fastening programs. The fastest way to reduce sourcing uncertainty is to define the right parameters before production risk becomes field risk.
Search News
Hot Articles
- Carbon Fiber StructuresHow to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsJul 11, 2026
- Machine VisionXiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsMar 30, 2026
- Cobots & ArmsShanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsMar 30, 2026
Popular Tags
Recommended News
 Jul 11, 2026How to Specify Aerospace Carbon Fiber Assemblies for Lightweight, Load-Bearing PartsAerospace carbon fiber assemblies: learn how to specify laminate design, load data, joining methods, and inspection controls for lighter, reliable load-bearing aerospace parts.Elena Rostova (UAV Systems Researcher)
 Mar 30, 2026Xiaomi, Alibaba DAMO Academy Drive Open-Source Robotics Model Ecosystem, Lowering Algorithm Development Barriers for Overseas SMEs Adopting Chinese Robotics SolutionsXiaomi & Alibaba DAMO Academy's open-source robotics models lower algorithm barriers for global SMEs. Boost efficiency in manufacturing, logistics & smart retail with ROS 2 compatible solutions.TSV Data Lab
 Mar 30, 2026Shanxi 'AI+' Conference Showcases Embodied Intelligence with Multinational Buyer Engagement: Key Industry ImplicationsShanxi 'AI+' Conference highlights embodied intelligence with Tesla, Ubtech & Jiantao showcasing multimodal robotics. 40+ global buyers validated tech on-site, creating new B2B channels for industrial automation & AI solutions.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Zhongguancun Unveils 6G Integrated Sensing-Computing-Intelligence Platform to Empower Embodied Robots for Global Industrial ApplicationsZhongguancun's new 6G platform revolutionizes industrial robotics with <10ms latency, empowering global automotive, logistics & port automation. Discover how this tech boosts China's smart manufacturing exports.TSV Data Lab
 Mar 30, 2026Mech-Mind Tianjin Embodied Intelligence R&D and Production Base Goes Live, Cutting Delivery Time by 20%–30% for Global Customized AMR+Vision SolutionsMech-Mind's Tianjin AMR+Vision production base cuts delivery time by 20%-30% for欧美 & Latin American markets. Discover how this PLd-certified facility accelerates customized robotics solutions for smart manufacturing and logistics.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026Boao Forum Reveals 'Co-evolution of Big and Small Brains' Trend in Humanoid Robots, China's Embodied Intelligence Accelerates Adaptation to Overseas Manufacturing Service ScenariosDiscover how China's humanoid robots, featuring 'Co-evolution of Big and Small Brains,' are revolutionizing global manufacturing. Learn about Embodied Tian Gong 3.0's ISO compliance and overseas deployment at Boao Forum 2026.Chen Wei (Automation Lead Engineer)
 Mar 30, 2026China Railway Industrial Secures Patent for Embodied Robotics in Material Handling, Boosting High-Precision Delivery Capabilities for Overseas Infrastructure and Manufacturing ProjectsChina Railway Industrial's new patent for embodied robotics in material handling boosts high-precision delivery for global infrastructure & manufacturing. Discover how this innovation enhances logistics accuracy in automotive, rail transit & EPC projects.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026Drone Frame Composites: Carbon Fiber vs. Fiberglass for Weight and StiffnessExplore drone structural materials composites: compare carbon fiber and fiberglass for weight, stiffness, cost, and antenna compatibility. Find the right material for your drone frame.Elena Rostova (UAV Systems Researcher)
 Oct 13, 2026Smart Cameras vs. PC-Based Machine Vision: Which Fits High-Speed Inspection?This industrial product comparison for machine vision weighs smart cameras vs. PC-based systems on latency, throughput, and cost. Discover your best fit for high-speed inspection.TSV Data Lab
 Oct 12, 2026How to Verify RoHS Compliance in Industrial Sensing Systems Before DeploymentRoHS compliant sensing systems: learn how to verify materials, supplier declarations, testing, and configuration controls before industrial deployment.TSV Data Lab
 Oct 11, 2026How Procurement-Oriented Content Taxonomy Improves B2B Buying JourneysProcurement-oriented content taxonomy streamlines B2B buying journeys with clearer evidence, supplier comparisons, risk visibility, and faster approvals.TSV Data Lab
 Oct 10, 2026How to Select a Machine Performance Monitoring Platform for OEE and Downtime ReductionMachine performance monitoring platform selection guide: validate machine states, OEE data, downtime reasons, integrations, and scalability to reduce losses with confidence.TSV Data Lab
 Oct 08, 2026How to Machine Inconel 625 Blades Without Heat Cracks or Edge ChippingInconel 625 blade machining guide: prevent heat cracks, edge chipping, chatter, and work hardening with proven tooling, cooling, fixturing, and inspection strategies.Dr. Marcus Vance
 Oct 07, 2026How to Evaluate an HMI Panel Distributor for Industrial Automation ProjectsHMI panel distributor evaluation guide: verify technical compatibility, traceability, supply reliability, lifecycle support, and total cost for automation projects.Victor Lin (Chief Software Architect)
 Oct 06, 2026Navigation Fault Tolerance Standards for AMRs: What Safety Teams Must VerifyNavigation fault tolerance standards: learn what AMR safety teams must verify, from localization loss and sensor faults to stopping distance, safe restart, and site-specific validation.Chen Wei (Automation Lead Engineer)
 Oct 05, 2026Calculating Edge Computing Total Cost of Ownership Across Distributed SitesEdge computing ownership cost explained: calculate deployment, energy, connectivity, security, remote support, and refresh costs across distributed sites.TSV Data Lab
 Oct 04, 2026CAD/CAM Benchmarking in the GCC: What Manufacturers Should Ask a ConsultantCAD CAM benchmark consultant GCC guide: learn the key questions manufacturers should ask to validate post-processors, workflows, machine performance, and production risk.Victor Lin (Chief Software Architect)
 Oct 03, 2026Selecting Automotive Radar Sensor Modules for ADAS Range, Resolution, and IntegrationAutomotive radar sensor module selection guide for ADAS: compare range, resolution, field of view, latency, and integration to build safer, reliable vehicle systems.TSV Data Lab
 Oct 02, 2026How to Qualify Machined Parts Suppliers for Hard Tech ProgramsHard tech supply chain machined parts demand rigorous supplier qualification. Learn how to assess capability, traceability, quality controls, and delivery resilience.Dr. Marcus Vance
 Oct 01, 2026How to Select an Outdoor Security Radar Sensor for Perimeter Detection?Outdoor security radar sensor selection guide: compare range, accuracy, false-alarm control, integration, and field testing for reliable perimeter detection.TSV Data Lab
 Sep 30, 2026How to Evaluate Solid-State LiDAR Hardware for Outdoor Autonomous VehiclesSolid state LiDAR hardware evaluation guide for outdoor autonomous vehicles—compare range, point-cloud quality, environmental resilience, integration, and safety.TSV Data Lab
 Sep 29, 2026ISO 9283 Repeatability: How to Evaluate Cobot Positioning PerformanceISO 9283 cobot repeatability explained: learn how payload, reach, approach direction, and test conditions affect positioning performance and cell capability.Chen Wei (Automation Lead Engineer)
 Oct 14, 2026How tight can micro machining aerospace tolerances be in production?Micro machining aerospace tolerances can reach low-micron levels in production. Learn what controls repeatability, inspection confidence, and flight-critical quality.Dr. Marcus Vance
 Oct 13, 2026How to keep an industrial robotic integration project on scheduleIndustrial robotic integration project management: keep automation on schedule with proven controls for interfaces, suppliers, FAT, commissioning, and change risk.Victor Lin (Chief Software Architect)























